CN110064799B - A kind of wire gear numerical control gear grinding machine and wire gear grinding processing method - Google Patents
A kind of wire gear numerical control gear grinding machine and wire gear grinding processing method Download PDFInfo
- Publication number
- CN110064799B CN110064799B CN201910407772.XA CN201910407772A CN110064799B CN 110064799 B CN110064799 B CN 110064799B CN 201910407772 A CN201910407772 A CN 201910407772A CN 110064799 B CN110064799 B CN 110064799B
- Authority
- CN
- China
- Prior art keywords
- gear
- wire
- axis
- grinding
- grinding wheel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23F—MAKING GEARS OR TOOTHED RACKS
- B23F19/00—Finishing gear teeth by other tools than those used for manufacturing gear teeth
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23F—MAKING GEARS OR TOOTHED RACKS
- B23F23/00—Accessories or equipment combined with or arranged in, or specially designed to form part of, gear-cutting machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23F—MAKING GEARS OR TOOTHED RACKS
- B23F23/00—Accessories or equipment combined with or arranged in, or specially designed to form part of, gear-cutting machines
- B23F23/02—Loading, unloading or chucking arrangements for workpieces
- B23F23/06—Chucking arrangements
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Grinding Of Cylindrical And Plane Surfaces (AREA)
- Grinding-Machine Dressing And Accessory Apparatuses (AREA)
Abstract
本发明公开了一种线齿轮数控磨齿机及线齿轮磨削加工方法,所述线齿轮数控磨齿机包括床身、立柱、砂轮主轴箱、砂轮修整装置、工件夹持机构、分度盘、旋转工作台以及数控系统;所述线齿轮磨削加工方法通过使待加工的线齿轮工件和成形砂轮呈啮合状态并以规定的轴交叉角同步旋转,同时待加工的线齿轮工件以规定的方向进行相对的进给运动,从而实现成形砂轮磨削所述线齿轮工件的加工过程。本发明的线齿轮数控磨齿机及线齿轮磨削加工方法,简化了线齿轮的磨削加工工艺过程,提高了线齿轮磨削加工效率和加工精度,同时扩大了其适用范围,可用于磨削加工圆柱线齿轮、圆锥线齿轮及其它类型的螺旋齿轮的加工。

The invention discloses a wire gear numerical control gear grinding machine and a wire gear grinding processing method. The wire gear numerical control gear grinding machine includes a bed, a column, a grinding wheel spindle box, a grinding wheel dressing device, a workpiece clamping mechanism, and an indexing plate , a rotary table and a numerical control system; the wire gear grinding method makes the wire gear workpiece to be processed mesh with the forming grinding wheel and rotate synchronously at a specified axis crossing angle, while the wire gear workpiece to be processed is rotated at a specified The relative feed motion is carried out in the direction, so as to realize the machining process of the profiled grinding wheel grinding the wire gear workpiece. The wire gear numerical control gear grinding machine and the wire gear grinding method of the present invention simplify the grinding process of the wire gear, improve the grinding efficiency and processing accuracy of the wire gear, and expand its applicable scope at the same time, and can be used for grinding Machining of cylindrical wire gears, conical wire gears and other types of helical gears.
Description
技术领域technical field
本发明涉及齿轮加工设备及齿轮加工方法领域,尤其涉及一种线齿轮数控磨齿机及线齿轮磨削加工方法。The invention relates to the field of gear processing equipment and a gear processing method, in particular to a wire gear numerical control gear grinding machine and a wire gear grinding method.
背景技术Background technique
线齿轮是一种基于空间共轭曲线啮合原理的新型齿轮,线齿轮副以点接触的方式进行传动,为了进一步提升线齿轮的承载能力和使用寿命,需要对铣削加工后的线齿轮进行热处理,为了高效地对热处理后的线齿轮的齿面进行精加工,需要对线齿轮进行磨削加工。The wire gear is a new type of gear based on the principle of space conjugate curve meshing. The wire gear pair is transmitted in a point-contact manner. In order to further improve the load-bearing capacity and service life of the wire gear, it is necessary to heat-treat the wire gear after milling. In order to efficiently finish the tooth surface of the heat-treated wire gear, it is necessary to grind the wire gear.
不同于传统的渐开线直齿轮和螺旋锥齿轮,线齿轮轮齿啮合线包括圆柱螺旋线和圆锥螺旋线两种形式,因此目前用于磨削加工渐开线直齿轮齿轮和螺旋锥齿轮的磨齿机无法适应不同类型线齿轮的磨削加工,六轴加工中心虽然能够满足不同类型线齿轮磨削加工时的运动要求,但是加工成本高,因此,结合线齿轮的结构特点,本发明提出了一种线齿轮数控磨齿机及线齿轮磨削加工方法。本发明的线齿轮数控轮磨齿机及线齿轮磨削加工方法,简化了线齿轮的磨削加工工艺过程,提高了线齿轮磨削加工效率和加工精度,同时适用范围广,可以磨削加工圆柱线齿轮、圆锥线齿轮及其他类型的螺旋齿轮。Different from traditional involute spur gears and spiral bevel gears, the tooth meshing lines of linear gears include cylindrical helix and conical helix. Therefore, it is currently used for grinding involute spur gears and spiral bevel gears. The gear grinding machine cannot adapt to the grinding of different types of wire gears. Although the six-axis machining center can meet the motion requirements of different types of wire gears during grinding, the processing cost is high. Therefore, combined with the structural characteristics of wire gears, the present invention proposes A CNC gear grinding machine for wire gears and a grinding method for wire gears are disclosed. The wire gear numerical control gear grinding machine and the wire gear grinding method of the present invention simplify the wire gear grinding process, improve the wire gear grinding efficiency and processing accuracy, and at the same time have a wide range of applications and can be ground. Cylindrical wire gears, conical wire gears and other types of helical gears.
发明内容Contents of the invention
为了解决现有齿轮磨削加工设备和齿轮磨削方法磨削线齿轮时存在的问题,本发明提供了一种可以实现四轴联动的线齿轮数控轮磨齿机及线齿轮磨削加工方法,简化了线齿轮的磨削加工动作,提高了线齿轮的加工精度和加工效率,降低了加工成本。In order to solve the problems existing in the existing gear grinding equipment and gear grinding method when grinding wire gears, the present invention provides a wire gear numerical control wheel gear grinding machine and a wire gear grinding method that can realize four-axis linkage, The grinding processing action of the wire gear is simplified, the processing accuracy and processing efficiency of the wire gear are improved, and the processing cost is reduced.
本发明的目的至少通过如下技术方案之一实现:The object of the present invention is achieved at least by one of the following technical solutions:
一种线齿轮数控磨齿机,包括床身、立柱、砂轮主轴箱、砂轮修整装置、工件夹持机构、分度盘、旋转工作台以及数控系统,其特征在于:所述床身上固定安装有立柱,所述立柱的竖直方向上设置有沿Z轴方向移动的Z轴导轨和驱动装置,所述砂轮主轴箱安装在Z轴导轨上沿Z轴导轨移动,所述床身上设置有X轴导轨、与X轴导轨滑动配合的X向移动机座、驱动所述X向移动机座沿所述X轴导轨往复移动的驱动装置;所述X向移动机座上设置有Y轴导轨、与所述Y轴导轨滑动配合的Y向移动机座、驱动所述Y向移动机座沿所述Y轴导轨往复移动的驱动装置;所述砂轮修整装置安装在所述Y向移动机座上;所述旋转工作台的一端通过绕B轴旋转的转动机构与Y向移动机座相连接,所述B轴平行于所述Y轴导轨;所述分度盘固定在所述旋转工作台中间且可绕垂直于所述旋转工作台所在平面的C轴转动;所述工件夹持机构安装在所述分度转盘上,用于夹紧并驱动工件沿垂直于C轴的A轴旋转,所述数控系统分别与所述砂轮主轴箱、各驱动装置、转动机构、分度盘、砂轮修整装置电气连接。A numerical control gear grinding machine for wire gears, comprising a bed, a column, a grinding wheel spindle box, a grinding wheel dressing device, a workpiece clamping mechanism, an indexing plate, a rotary table and a numerical control system, characterized in that: the bed is fixedly installed with A column, the vertical direction of the column is provided with a Z-axis guide rail and a driving device moving along the Z-axis direction, the grinding wheel headstock is installed on the Z-axis guide rail and moves along the Z-axis guide rail, and the bed is provided with an X-axis guide rail, an X-direction mobile base slidingly matched with the X-axis guide rail, and a driving device for driving the X-direction mobile base to reciprocate along the X-axis guide rail; the X-direction mobile base is provided with a Y-axis guide rail, and The Y-direction mobile base that is slidingly matched with the Y-axis guide rail, and the driving device that drives the Y-direction mobile base to reciprocate along the Y-axis guide rail; the grinding wheel dressing device is installed on the Y-direction mobile base; One end of the rotary table is connected to the Y-direction mobile base through a rotating mechanism that rotates around the B axis, and the B axis is parallel to the Y-axis guide rail; the index plate is fixed in the middle of the rotary table and It can rotate around the C-axis perpendicular to the plane where the rotary table is located; the workpiece clamping mechanism is installed on the indexing turntable for clamping and driving the workpiece to rotate along the A-axis perpendicular to the C-axis. The numerical control system is electrically connected with the grinding wheel spindle box, each driving device, the rotating mechanism, the indexing plate and the grinding wheel dressing device respectively.
进一步地,所述工件夹持机构包括相对设置的卡盘和顶尖尾座,所述卡盘用于装夹工件,所述顶尖尾座用于辅助装夹工件,卡盘在伺服电机的驱动下绕所述A轴旋转。Further, the workpiece clamping mechanism includes a chuck and a top tailstock oppositely arranged, the chuck is used to clamp the workpiece, the top tailstock is used to assist in clamping the workpiece, and the chuck is driven by a servo motor Rotate around the A axis.
进一步地,所述卡盘在伺服电机的驱动下绕自身轴线A轴转动,所述数控系统用于分别控制X轴伺服电机驱动X向移动机座沿X轴方向移动、Y轴伺服电机驱动Y向移动机座沿Y轴方向移动、Z轴伺服电机驱动砂轮主轴沿Z轴方向移动,实现A轴转动、X轴移动、Y轴移动、Z轴移动这四轴联动。Further, the chuck is driven by the servo motor to rotate around its own axis A, and the numerical control system is used to respectively control the X-axis servo motor to drive the X-direction mobile base to move along the X-axis direction, and the Y-axis servo motor to drive the Y axis. The moving base moves along the Y-axis, and the Z-axis servo motor drives the grinding wheel spindle to move along the Z-axis, realizing the four-axis linkage of A-axis rotation, X-axis movement, Y-axis movement, and Z-axis movement.
进一步地,在装夹所述待加工线齿轮时,调节旋转工作台绕B轴转过一定的角度,调节分度盘使工件夹持装置绕C轴转过一定的角度,使砂轮轴线和线齿轮轴线的夹角为设计值,所述旋转工作台绕B轴的转动以及分度盘绕C轴的转动为独立运动或与其他运动机构相联动。Further, when the gear to be processed is clamped, the rotary table is adjusted to rotate a certain angle around the B axis, and the index plate is adjusted to make the workpiece clamping device rotate a certain angle around the C axis, so that the axis of the grinding wheel and the line The included angle of the gear axis is a design value, and the rotation of the rotary table around the B axis and the rotation of the index disk around the C axis are independent motions or linked with other motion mechanisms.
进一步地,所述分度盘上设置有带动工件沿径向移动的T型槽,用于所述卡盘和顶尖尾座的安装调整。Further, the index plate is provided with a T-shaped slot that drives the workpiece to move in the radial direction, and is used for the installation and adjustment of the chuck and the center tailstock.
进一步地,所述数控系统通过控制Y向移动机座和砂轮主轴箱的相对运动实现对砂轮的修形。Further, the numerical control system realizes the modification of the grinding wheel by controlling the relative movement of the Y-direction mobile base and the grinding wheel headstock.
进一步地,所述成形砂轮安装在砂轮握把上,所述砂轮握把安装在砂轮主轴上,同时所述立柱上还安装有对刀测头机构,用于磨削加工开始的定位对刀。Further, the forming grinding wheel is installed on the grinding wheel handle, and the grinding wheel handle is installed on the grinding wheel spindle, and the tool setting probe mechanism is also installed on the column, which is used for positioning and tool setting at the beginning of the grinding process.
一种线齿轮磨削加工方法,包括以下步骤:A grinding method for wire gears, comprising the steps of:
S1:确定待磨削线齿轮的参数:所述线齿轮主要包括圆柱线齿轮和圆锥线齿轮两种形式,其中圆柱线齿轮轮齿啮合线为圆柱螺旋线,圆锥线齿轮轮齿啮合线为圆锥螺旋线,在坐标系oj-xjyjzj中,线齿轮轮齿啮合线的通用数学表达为:S1: Determine the parameters of the wire gear to be ground: the wire gear mainly includes two types: cylindrical wire gear and conical wire gear. Helical line, in the coordinate system o j -x j y j z j , the general mathematical expression of the meshing line of the wire gear teeth is:

式中θj为线齿轮轮齿啮合线的半圆锥顶角,当θj=0时,线齿轮轮齿啮合线是圆柱螺旋线,当
kj是旋向参数,当kj=1时,轮齿啮合线为左旋,kj=-1时,轮齿啮合线为右旋,k j is the rotation direction parameter, when k j =1, the tooth meshing line is left-handed, when k j =-1, the gear tooth meshing line is right-handed,
nj为线齿轮啮合线的螺旋参数,tj为线齿轮啮合线方程的参变量,tjs≤tj≤tje;tjs为初始啮合点,tje为终端啮合点;n j is the helical parameter of the wire gear meshing line, t j is the parameter variable of the wire gear meshing line equation, t js ≤t j ≤t je ; t js is the initial meshing point, t je is the terminal meshing point;
S2:确定成形砂轮的参数:线齿轮的齿面是一条圆弧母线沿轮齿啮合线切线方向扫掠得到,成形砂轮在磨削线齿轮时,在线齿轮轮齿啮合线法向截面上,成形砂轮截面廓形与线齿轮齿廓形状一致,同时所述成形砂轮截面廓形有效部分高度应该大于被加工线齿轮的最大齿全高,砂轮宽度小于被加工线齿轮的最小齿槽宽度,避免砂轮的非工作侧与被加工线齿轮齿面干涉;S2: Determine the parameters of the forming grinding wheel: the tooth surface of the wire gear is obtained by sweeping an arc generatrix along the tangential direction of the tooth meshing line. The cross-sectional profile of the grinding wheel is consistent with the shape of the tooth profile of the wire gear. At the same time, the height of the effective part of the profile of the shaped grinding wheel should be greater than the maximum tooth height of the processed wire gear, and the width of the grinding wheel should be smaller than the minimum tooth groove width of the processed wire gear, so as to avoid grinding wheel The non-working side interferes with the gear tooth surface of the processed line;
S3:确定线齿轮的装夹方式:圆柱线齿轮在装夹时,利用卡盘和顶尖尾座将待加工的圆柱线齿轮装夹固定,根据圆柱线齿轮轮齿啮合线参数确定旋转工作台绕B轴转过的角度γ,取
S4:确定成形砂轮和待加工线齿轮的运动形式:在磨削线齿轮的时候,使待加工的线齿轮工件和成形砂轮呈啮合状态并以规定的轴交叉角同步旋转,同时待加工的线齿轮工件以规定的方向进行相对的进给运动,从而实现成形砂轮磨削所述线齿轮工件的加工过程,待磨削线齿轮工件在磨削加工过程中绕自身轴线旋转和沿横向水平方向移动的规律是:S4: Determine the movement form of the forming grinding wheel and the wire gear to be processed: when grinding the wire gear, the wire gear workpiece to be processed and the forming grinding wheel are in a meshing state and rotate synchronously at a specified axis crossing angle, while the wire gear to be processed The gear workpiece performs relative feed motion in a specified direction, so as to realize the processing process of grinding the wire gear workpiece by the forming grinding wheel, and the wire gear workpiece to be ground rotates around its own axis and moves along the transverse horizontal direction during the grinding process The rule is:

其中,φj是磨削时线齿轮绕自身轴线旋转的角度,单位是度,Among them, φ j is the angle that the wire gear rotates around its own axis during grinding, and the unit is degree,
xj时磨削加工时线齿轮沿x轴方向移动的距离,单位是毫米, xj is the distance that the linear gear moves along the x-axis during grinding, in millimeters,
nj是线齿轮啮合线的螺旋参数,n j is the helical parameter of the wire gear meshing line,
tj是参变量。t j is the parameter variable.
进一步地,在磨削加工齿廓半径相同的线齿轮时,使用相同的成形砂轮进行磨削加工,大大的提高了成形砂轮的通用性。Furthermore, when grinding wire gears with the same tooth profile radius, the same shaped grinding wheel is used for grinding, which greatly improves the versatility of the shaped grinding wheel.
相比现有技术,本发明的线齿轮数控磨齿机及线齿轮磨削加工方法,简化了线齿轮的磨削加工工艺过程,提高了线齿轮磨削加工效率和加工精度,同时扩大了其适用范围,可用于磨削加工圆柱线齿轮、圆锥线齿轮及其它类型的螺旋齿轮。Compared with the prior art, the wire gear CNC gear grinding machine and the wire gear grinding method of the present invention simplify the wire gear grinding process, improve the wire gear grinding efficiency and processing accuracy, and expand its Scope of application, it can be used for grinding cylindrical wire gears, conical wire gears and other types of helical gears.
附图说明Description of drawings
图1是本发明实施例的一种用于加工硬齿面线齿轮的数控磨齿机结构示意图。Fig. 1 is a schematic structural diagram of a numerically controlled gear grinding machine for machining hard-tooth surface gears according to an embodiment of the present invention.
图2是本发明实施例的磨削加工方法流程图。Fig. 2 is a flow chart of the grinding method of the embodiment of the present invention.
图3是本发明实施例的磨削加工圆柱线齿轮的加工示意图。Fig. 3 is a schematic diagram of the grinding process of the cylindrical wire gear according to the embodiment of the present invention.
图4是本发明实施例的磨削加工圆柱线齿轮的另一方向加工示意图。Fig. 4 is a schematic diagram of another direction of grinding and processing a cylindrical linear gear according to an embodiment of the present invention.
图5是本发明实施例的磨削加工圆锥线齿轮的加工示意图。Fig. 5 is a schematic diagram of the grinding process of the conical gear according to the embodiment of the present invention.
图6是本发明实施例的磨削加工圆锥线齿轮的另一方向加工示意图。Fig. 6 is a schematic diagram of another direction of grinding and machining of a conical gear according to an embodiment of the present invention.
图中:In the picture:
1.立柱,2.对刀测头机构,3.顶尖尾座,4.Z轴导轨,5.砂轮修整装置,6.X轴导轨,7.床身,8.Y轴导轨,9.旋转工作台,10.分度盘,11.卡盘,12.砂轮握把,13.砂轮主轴箱,14.圆柱线齿轮,15.圆柱线齿轮加工砂轮,16.圆锥线齿轮,17.圆锥线齿轮加工砂轮。1. Column, 2. Tool setting probe mechanism, 3. Top tailstock, 4. Z-axis guide rail, 5. Grinding wheel dressing device, 6. X-axis guide rail, 7. Bed, 8. Y-axis guide rail, 9. Rotation Workbench, 10. Indexing disc, 11. Chuck, 12. Grinding wheel grip, 13. Grinding wheel spindle box, 14. Cylindrical gear, 15. Cylindrical gear processing grinding wheel, 16. Conical gear, 17. Conical wire Grinding wheel for gear machining.
具体实施方式Detailed ways
为了更加清楚的说明本发明实施例中的技术方案,下面将结合本发明实施例中的附图,对本发明实施例中的技术方案进行清楚、完整的描述,显然,所描述的实施例仅仅是本发明的一部分实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都应当属于本发明的范围。In order to illustrate the technical solutions in the embodiments of the present invention more clearly, the technical solutions in the embodiments of the present invention will be clearly and completely described below in conjunction with the drawings in the embodiments of the present invention. Obviously, the described embodiments are only Part of the embodiments of the present invention and all other embodiments obtained by those skilled in the art without creative efforts shall fall within the scope of the present invention.
如图1所示,本实施例是一种加工硬齿面线齿轮的数控磨齿机,包括床身7、立柱1、砂轮主轴箱13、砂轮修整装置5、卡盘11、顶尖尾座3、分度盘10、旋转工作台9以及数控系统。As shown in Figure 1, this embodiment is a CNC gear grinding machine for processing hard-tooth surface gears, including a bed 7, a column 1, a
所述床身7上固定安装有立柱1,所述立柱1的竖直方向上设置有沿Z轴方向移动的Z轴导轨4和驱动装置,所述砂轮主轴箱13安装在Z轴导轨4上沿Z轴导轨4移动,所述床身7上设置有X轴导轨6、与X轴导轨6滑动配合的X向移动机座、驱动所述X向移动机座沿所述X轴导轨6往复移动的驱动装置;所述X向移动机座上设置有Y轴导轨8、与所述Y轴导轨8滑动配合的Y向移动机座、驱动所述Y向移动机座沿所述Y轴导轨8往复移动的驱动装置;所述砂轮修整装置5安装在所述Y向移动机座上;所述旋转工作台9的一端通过绕B轴旋转的转动机构与Y向移动机座相连接,旋转工作台9可以通过转动机构绕B轴转动,所述B轴平行于所述Y轴导轨8;所述分度盘10固定在所述旋转工作台9中间且可绕垂直于所述旋转工作台9所在平面的C轴转动;所述工件夹持机构安装在所述分度转盘10上,用于夹紧并驱动工件沿垂直于C轴的A轴旋转,;所述数控系统分别与所述砂轮主轴箱、各驱动装置、转动机构、分度盘、砂轮修整装置电气连接。A column 1 is fixedly installed on the bed 7, and the vertical direction of the column 1 is provided with a Z-axis guide rail 4 and a driving device moving along the Z-axis direction, and the grinding wheel headstock 13 is installed on the Z-axis guide rail 4 Move along the Z-axis guide rail 4, the bed 7 is provided with an X-axis guide rail 6, an X-direction mobile base slidingly matched with the X-axis guide rail 6, and drives the X-direction mobile base to reciprocate along the X-axis guide rail 6 A moving drive device; the X-direction mobile base is provided with a Y-axis guide rail 8, a Y-direction mobile base that slides with the Y-axis guide rail 8, and drives the Y-direction mobile base along the Y-axis guide rail 8 reciprocating driving device; the grinding wheel dressing device 5 is installed on the Y-direction mobile base; one end of the rotary table 9 is connected with the Y-direction mobile base through a rotating mechanism that rotates around the B axis, and rotates The table 9 can be rotated around the B-axis through the rotating mechanism, and the B-axis is parallel to the Y-axis guide rail 8; the index plate 10 is fixed in the middle of the rotary table 9 and can rotate around the vertical axis The C-axis of the plane where 9 is located rotates; the workpiece clamping mechanism is installed on the indexing turntable 10 for clamping and driving the workpiece to rotate along the A-axis perpendicular to the C-axis; the numerical control system is respectively connected with the The grinding wheel spindle box, each driving device, the rotating mechanism, the indexing plate, and the grinding wheel dressing device are electrically connected.
本实施例中,所述数控系统分别控制卡盘11在伺服电机的驱动下绕A轴转动、X轴导轨6在伺服电机的驱动下带动工件沿X轴方向移动、Y轴导轨8在伺服电机的驱动下带动工件沿Y轴方向移动、Z轴导轨4在伺服电机的驱动下带动砂轮主轴箱13沿Z轴方向移动,所述磨齿机能够实现A轴转动、X轴移动、Y轴移动、Z轴移动这四轴联动。In this embodiment, the numerical control system respectively controls the
本实施例中,装夹待磨削加工线齿轮的时候,调节旋转工作台9使待加工工件绕B轴转过特定的角度同时调节分度盘10使待加工线齿轮绕C轴转过特定的角度,使砂轮轴线和待磨削加工线齿轮轴线的夹角为设计值,旋转工作台绕B轴的转动以及分度盘绕C轴的转动不必与A轴转动、X轴移动、Y轴移动、Z轴移动这四轴实现联动。本实施例中,所述分度盘10上有带动带磨削加工沿径向移动的T型槽,用于完成卡盘11和顶尖尾座3的安装调整,所述砂轮修整装置安装在所述Y向移动机座上,通过控制Y向移动机座和主轴箱的相对运动实现对砂轮的修形,砂轮安装在砂轮握把12上,砂轮握把12安装在砂轮主轴上,同时立柱1上还安装有对刀测头机构2,用于磨削加工开始的定位对刀。In this embodiment, when the gear to be processed is clamped, the rotary table 9 is adjusted so that the workpiece to be processed rotates through a specific angle around the B axis, and the
14.圆柱线齿轮,15.圆柱线齿轮加工砂轮,16.圆锥线齿轮,17.圆锥线齿轮加工砂轮。14. Cylindrical wire gear, 15. Cylindrical wire gear processing grinding wheel, 16. Conical wire gear, 17. Conical wire gear processing grinding wheel.
如图2所示,一种线齿轮磨削加工方法,包括步骤:As shown in Fig. 2, a kind of wire gear grinding processing method comprises steps:
S1:确定待磨削线齿轮的参数:所述线齿轮主要包括圆柱线齿轮14和圆锥线齿轮16两种形式,其中圆柱线齿轮轮齿啮合线为圆柱螺旋线,圆锥线齿轮轮齿啮合线为圆锥螺旋线,在坐标系oj-xjyjzj中,线齿轮轮齿啮合线的通用数学表达为:S1: Determine the parameters of the wire gear to be ground: the wire gear mainly includes two forms of

式中θj为线齿轮轮齿啮合线的半圆锥顶角,当θj=0时,线齿轮轮齿啮合线是圆柱螺旋线,当
kj是旋向参数,当kj=1时,轮齿啮合线为左旋,kj=-1时,轮齿啮合线为右旋,k j is the rotation direction parameter, when k j =1, the tooth meshing line is left-handed, when k j =-1, the gear tooth meshing line is right-handed,
nj为线齿轮啮合线的螺旋参数,tj为线齿轮啮合线方程的参变量,tjs≤tj≤tje;tjs为初始啮合点,tje为终端啮合点。n j is the helical parameter of the wire gear meshing line, t j is the parameter variable of the wire gear meshing line equation, t js ≤t j ≤t je ; t js is the initial meshing point, t je is the terminal meshing point.
S2:确定成形砂轮的参数:线齿轮的齿面可以看作是一条圆弧母线沿轮齿啮合线切线方向扫掠得到,成形砂轮在磨削线齿轮时,在线齿轮轮齿啮合线法向截面上,成形砂轮截面廓形与线齿轮齿廓形状一致,同时所述成形砂轮截面廓形有效部分高度应该大于被加工线齿轮的最大齿全高,砂轮宽度应该小于被加工线齿轮的最小齿槽宽度,避免砂轮的非工作侧与被加工线齿轮齿面干涉。S2: Determine the parameters of the forming grinding wheel: the tooth surface of the wire gear can be regarded as a circular arc generatrix swept along the tangential direction of the tooth meshing line. Above, the cross-sectional profile of the formed grinding wheel is consistent with the shape of the tooth profile of the wire gear, and at the same time, the height of the effective part of the cross-sectional profile of the formed grinding wheel should be greater than the maximum tooth height of the processed line gear, and the width of the grinding wheel should be smaller than the minimum tooth space width of the processed line gear , to avoid interference between the non-working side of the grinding wheel and the gear tooth surface of the processed line.
S3:确定线齿轮的装夹方式:圆柱线齿轮在装夹的时候,利用卡盘和顶尖尾座将待加工的圆柱线齿轮装夹固定,根据圆柱线齿轮轮齿啮合线参数确定旋转工作台绕B轴转过的角度γ,一般取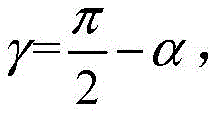
S4:确定成形砂轮和待加工线齿轮的运动形式:在磨削线齿轮的时候,使待加工的线齿轮工件和成形砂轮呈啮合状态并以规定的轴交叉角同步旋转,同时待加工的线齿轮工件以规定的方向进行相对的进给运动,从而实现成形砂轮磨削所述线齿轮工件的加工过程,待磨削线齿轮在磨削加工过程中绕自身轴线旋转和沿横向水平移动的规律是:S4: Determine the movement form of the forming grinding wheel and the wire gear to be processed: when grinding the wire gear, the wire gear workpiece to be processed and the forming grinding wheel are in a meshing state and rotate synchronously at a specified axis crossing angle, while the wire gear to be processed The gear workpiece performs relative feed motion in a specified direction, so as to realize the processing process of forming the grinding wheel to grind the wire gear workpiece, and the wire gear to be ground rotates around its own axis and moves horizontally along the horizontal direction during the grinding process yes:

其中,φj是磨削时线齿轮绕自身轴线旋转的角度,单位是度,Among them, φ j is the angle that the wire gear rotates around its own axis during grinding, and the unit is degree,
xj时磨削加工时线齿轮沿x轴方向移动的距离,单位是毫米, xj is the distance that the linear gear moves along the x-axis during grinding, in millimeters,
nj是线齿轮啮合线的螺旋参数,n j is the helical parameter of the wire gear meshing line,
tj是参变量。t j is the parameter variable.
所述线齿轮磨削加工方法使待加工的线齿轮工件和成形砂轮呈啮合状态并以规定的轴交叉角同步旋转,同时待加工的线齿轮工件以规定的方向进行相对的进给运动,从而实现成形砂轮磨削所述线齿轮工件的加工过程。The wire gear grinding method makes the wire gear workpiece to be processed and the forming grinding wheel in a meshing state and rotate synchronously at a specified axis crossing angle, and at the same time, the wire gear workpiece to be processed performs relative feed motion in a specified direction, thereby The processing process of grinding the wire gear workpiece by the forming grinding wheel is realized.
本发明针对线齿轮的齿面成形原理,提出了一种线齿轮数控磨齿机及线齿轮磨削加工方法,简化了线齿轮的加工工艺过程,可以实现圆柱线齿轮、圆锥线齿轮的磨削加工,具有磨削效率高、磨削精度高、适用范围广的优点。Aiming at the tooth surface forming principle of wire gears, the present invention proposes a wire gear CNC gear grinding machine and a wire gear grinding method, which simplifies the processing process of wire gears and can realize the grinding of cylindrical wire gears and conical wire gears It has the advantages of high grinding efficiency, high grinding precision and wide application range.
本发明的上述实施例仅仅是为清楚地说明本发明所作的举例,而并非是对本发明的实施方式的限定。对于所属领域的普通技术人员来说,在上述说明的基础上还可以做出其它不同形式的变化或变动。这里无需也无法对所有的实施方式予以穷举。凡在本发明的精神和原则之内所作的任何修改、等同替换和改进等,均应包含在本发明权利要求的保护范围之内。The above-mentioned embodiments of the present invention are only examples for clearly illustrating the present invention, rather than limiting the implementation of the present invention. For those of ordinary skill in the art, other changes or changes in different forms can be made on the basis of the above description. It is not necessary and impossible to exhaustively list all the implementation manners here. All modifications, equivalent replacements and improvements made within the spirit and principles of the present invention shall be included within the protection scope of the claims of the present invention.
Claims (9)


Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201910407772.XA CN110064799B (en) | 2019-05-15 | 2019-05-15 | A kind of wire gear numerical control gear grinding machine and wire gear grinding processing method |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201910407772.XA CN110064799B (en) | 2019-05-15 | 2019-05-15 | A kind of wire gear numerical control gear grinding machine and wire gear grinding processing method |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN110064799A CN110064799A (en) | 2019-07-30 |
| CN110064799B true CN110064799B (en) | 2023-06-16 |
Family
ID=67370862
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201910407772.XA Active CN110064799B (en) | 2019-05-15 | 2019-05-15 | A kind of wire gear numerical control gear grinding machine and wire gear grinding processing method |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN110064799B (en) |
Families Citing this family (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110328612A (en) * | 2019-08-19 | 2019-10-15 | 丹阳河工工具有限公司 | A kind of screw tap grinding attachment |
| CN110744158B (en) * | 2019-10-31 | 2021-02-12 | 华南理工大学 | Electrolytic finish machining method for micro-wire gear |
| CN111992818A (en) * | 2020-07-31 | 2020-11-27 | 江麓机电集团有限公司 | Gear machining method of linkage rotary working platform |
| CN112059322A (en) * | 2020-09-04 | 2020-12-11 | 河南科技大学 | A helical gear grinding machine |
| CN113245638A (en) * | 2021-05-24 | 2021-08-13 | 哈尔滨理工大学 | Clamp for vertical milling machine to process spiral bevel gear |
| CN115592209A (en) * | 2021-07-08 | 2023-01-13 | 佛山市二轴半科技有限公司(Cn) | A kind of wire gear forming milling processing method |
| CN113878180A (en) * | 2021-09-16 | 2022-01-04 | 重庆首业齿轮研究院有限公司 | Seven-shaft four-linkage multifunctional gear grinding machine |
| CN114473075A (en) * | 2022-03-08 | 2022-05-13 | 重庆大学 | Complex shaping grinding method and machine tool for tooth surface of precision roller enveloping worm |
| CN114769737A (en) * | 2022-05-09 | 2022-07-22 | 陕西理工大学 | Forming and grinding processing method for gear with small number of teeth |
| CN115194533A (en) * | 2022-07-29 | 2022-10-18 | 中国电子科技集团公司第三十八研究所 | Horizontal machining center |
| CN115351359B (en) * | 2022-08-17 | 2025-06-20 | 中南林业科技大学 | Gear grinding machine tool for grinding spiral bevel gears |
| CN116475503A (en) * | 2023-05-05 | 2023-07-25 | 上海星合机电有限公司 | Multi-Axis CNC Form Grinding Machine Tool |
| CN117484357B (en) * | 2023-12-19 | 2024-06-04 | 柳州瑞东机械制造有限公司 | Mechanical steel ring grinding machine capable of improving grinding precision |
| CN117620327A (en) * | 2023-12-29 | 2024-03-01 | 南京工业大学 | A large-scale gear grinding and backlash elimination device and method thereof |
| CN120243790B (en) * | 2025-04-02 | 2025-12-02 | 华南理工大学 | An automatic feeding device and method for bidirectional rolling of linear gears |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20060091212A (en) * | 2005-02-14 | 2006-08-18 | 김재복 | Polishing heads for stone processing |
| CN102528171A (en) * | 2012-02-17 | 2012-07-04 | 浙江顺天减速机制造有限公司 | Numerical-control efficient cycloid tooth-shaped grinding machine |
| CN104139219A (en) * | 2013-11-26 | 2014-11-12 | 上海拓璞数控科技有限公司 | Five-axis grinding wheel grinding processing method for planar enveloping hourglass worm |
| CN208357946U (en) * | 2018-02-07 | 2019-01-11 | 华南理工大学 | It is a kind of for processing the special horizontal milling machine of line gear |
| CN108500396A (en) * | 2018-04-17 | 2018-09-07 | 佛山市二轴半科技有限公司 | A kind of special vertical CNC milling machine for line gear processing |
-
2019
- 2019-05-15 CN CN201910407772.XA patent/CN110064799B/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| CN110064799A (en) | 2019-07-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110064799A (en) | A kind of line gear numerically controlled tooth grinding machine and line gear grinding processing method | |
| JP4202306B2 (en) | Gear grinding machine | |
| US9399279B2 (en) | Double-side dresser | |
| CN114226868B (en) | Gear grinding machine tool for forming grinding wheel | |
| CN201685166U (en) | Numerically-controlled composite grinding center | |
| CN105921823B (en) | A kind of numerical control worm wheel grinding method of cycloid gear | |
| CN202716139U (en) | Multifunctional molding grinding machine tool | |
| CN113400197B (en) | Method for shaping and trimming drum-shaped worm grinding wheel for grinding face gear | |
| CN112059327B (en) | Internal and external thread grinder with grinding wheel capable of being shaped in situ | |
| CN102107300A (en) | CNC (computerized numerical control) combined turning and grinding machine tool for four-linkage enveloping worms and processing method thereof | |
| CN213672273U (en) | Internal and external thread grinding machine with grinding wheel capable of being subjected to in-situ shape correction | |
| CN108311963A (en) | A kind of six axis knife sharpeners | |
| CN103418852A (en) | Novel efficient numerical control gear grinding machine | |
| CN116372281A (en) | Single-process numerical control worm grinding wheel gear grinding machine | |
| CN115008266B (en) | a tool grinder | |
| CN105710454B (en) | Small-sized spiral bevel gear digital control snail disk grinding wheel gear lapping machine and its procedure of processing | |
| CN115351359A (en) | A gear grinding machine tool for grinding spiral bevel gears | |
| CN111958058B (en) | Multi-station numerical control gear grinding machine | |
| CN217475585U (en) | Numerical control spiral curved surface forming grinder | |
| CN101104245A (en) | Four-Axis CNC Ellipsoidal and Spherical Hob Relief Grinding Machine | |
| CN102729126A (en) | Multifunctional forming grinding machine tool | |
| CN112108722B (en) | Full-automatic gear grinding machine device | |
| CN114769739A (en) | A full-size annular enveloping worm automatic grinding machine | |
| CN114473075A (en) | Complex shaping grinding method and machine tool for tooth surface of precision roller enveloping worm | |
| CN205764276U (en) | CNC thread tooth grinding machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |