CN107932971B - Press production system for extruded products - Google Patents
Press production system for extruded products Download PDFInfo
- Publication number
- CN107932971B CN107932971B CN201711408548.XA CN201711408548A CN107932971B CN 107932971 B CN107932971 B CN 107932971B CN 201711408548 A CN201711408548 A CN 201711408548A CN 107932971 B CN107932971 B CN 107932971B
- Authority
- CN
- China
- Prior art keywords
- cylinder
- linear module
- support frame
- horizontal
- mold
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 12
- 235000012438 extruded product Nutrition 0.000 title claims description 14
- 239000000463 material Substances 0.000 claims abstract description 55
- 239000002994 raw material Substances 0.000 claims abstract description 45
- 238000003825 pressing Methods 0.000 claims abstract description 25
- 230000007246 mechanism Effects 0.000 claims abstract description 18
- 239000003638 chemical reducing agent Substances 0.000 claims abstract description 14
- 238000013016 damping Methods 0.000 claims abstract description 8
- 238000005303 weighing Methods 0.000 claims abstract description 3
- 238000004140 cleaning Methods 0.000 claims description 58
- 239000007921 spray Substances 0.000 claims description 5
- 230000035939 shock Effects 0.000 claims 2
- 238000000034 method Methods 0.000 abstract description 11
- 238000001125 extrusion Methods 0.000 abstract description 8
- 230000009471 action Effects 0.000 description 10
- 230000008569 process Effects 0.000 description 5
- 239000000446 fuel Substances 0.000 description 3
- 238000002347 injection Methods 0.000 description 3
- 239000007924 injection Substances 0.000 description 3
- 230000000694 effects Effects 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 239000012535 impurity Substances 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 239000002245 particle Substances 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 238000005507 spraying Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/02—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/02—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space
- B30B11/022—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space whereby the material is subjected to vibrations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/02—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space
- B30B11/04—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space co-operating with a fixed mould
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/02—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space
- B30B11/04—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space co-operating with a fixed mould
- B30B11/06—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space co-operating with a fixed mould each charge of the material being compressed against the previously formed body
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/0005—Details of, or accessories for, presses; Auxiliary measures in connection with pressing for briquetting presses
- B30B15/0011—Details of, or accessories for, presses; Auxiliary measures in connection with pressing for briquetting presses lubricating means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/0076—Noise or vibration isolation means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/0082—Dust eliminating means; Mould or press ram cleaning means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/02—Dies; Inserts therefor; Mounting thereof; Moulds
- B30B15/022—Moulds for compacting material in powder, granular of pasta form
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/30—Feeding material to presses
- B30B15/302—Feeding material in particulate or plastic state to moulding presses
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/32—Discharging presses
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Press-Shaping Or Shaping Using Conveyers (AREA)
Abstract
本发明提供一种挤压成型产品的压制生产系统,属于挤压成型设备领域,以解决目前方式人力成本较高及输送效率较低的问题。包括:原料输送装置、压制装置和模具及成品抓取装置;原料输送装置包括第一进料斗、螺旋送料机、加料伺服电机、减速器、称重传感器、第一支撑架、料箕、顶升气缸、第二支撑架、送料斗、送料伺服电机、送料线性模组、滑台、第三支撑架、出料挡板和第一开闭气缸;压制装置包括底座、四个减震弹簧、下模具、物料支撑板、顶升缸、两个限位装置、第一压头和升降机构;模具及成品抓取装置包括支撑台、输送带装置、动力机构、水平输送装置、垂直输送装置和两个模具输送装置。
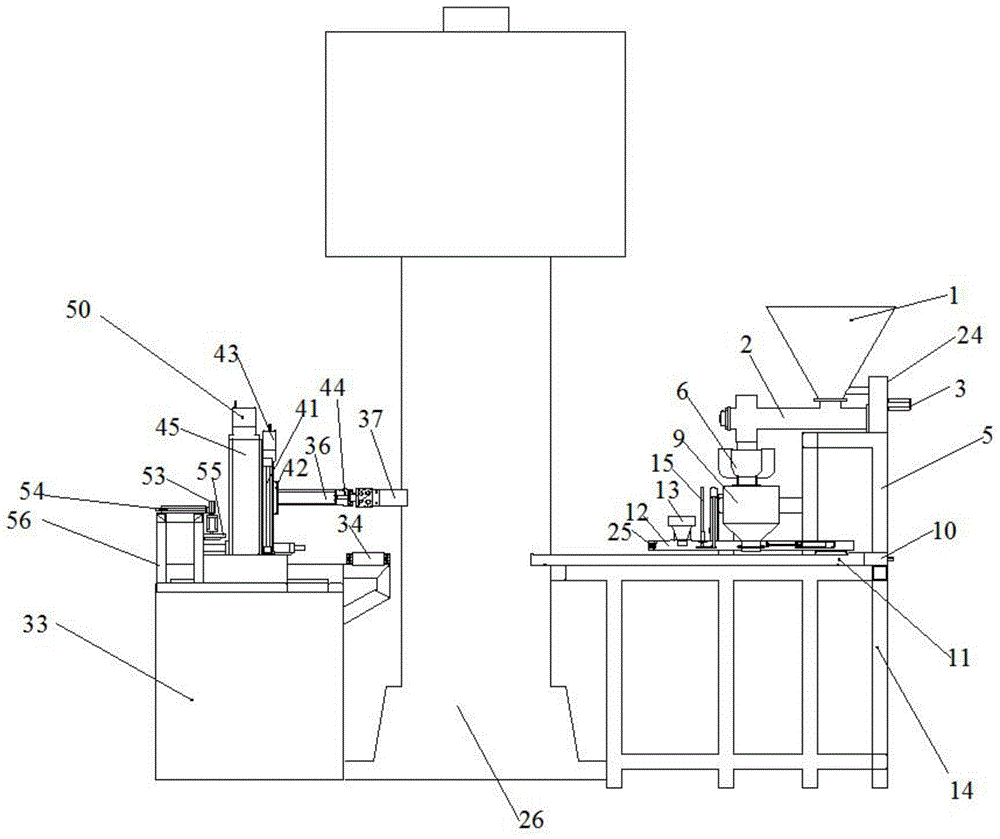
The invention provides a pressing production system for extrusion molding products, which belongs to the field of extrusion molding equipment, and aims to solve the problems of high labor cost and low conveying efficiency in the current method. Including: raw material conveying device, pressing device, mold and finished product grabbing device; raw material conveying device includes the first feeding hopper, screw feeder, feeding servo motor, reducer, weighing sensor, first support frame, material skip, top Lifting cylinder, second support frame, feeding hopper, feeding servo motor, feeding linear module, slide table, third supporting frame, discharge baffle and first opening and closing cylinder; the pressing device includes a base, four damping springs, Lower mold, material support plate, jacking cylinder, two limit devices, first pressure head and lifting mechanism; mold and finished product grabbing device includes support table, conveyor belt device, power mechanism, horizontal conveying device, vertical conveying device and Two mold transfer units.
Description
技术领域technical field
本发明涉及挤压成型设备技术领域,尤其涉及一种挤压成型产品的压制生产系统。The invention relates to the technical field of extrusion molding equipment, in particular to a press production system for extrusion molding products.
背景技术Background technique
在实际的生产过程中,经常需要对颗粒物原料、粉末原料等进行挤压而形成具有一定形状的产品,这样形成的产品即为挤压成型产品。目前在生产挤压成型产品时,经常是人工将原料放入模型腔中,然后通过一定的挤压设备对模型腔中的原料进行挤压得到产品。在挤压成型后,通过人工运输产品或人工将产品运输至输送设备上。然而,人工向模型腔中填料或者人工运输产品,不仅人力成本比较高,而且输送效率比较低。In the actual production process, it is often necessary to extrude granular raw materials, powder raw materials, etc. to form products with a certain shape, and the products formed in this way are extruded products. At present, when producing extruded products, the raw materials are often put into the mold cavity manually, and then the raw materials in the mold cavity are extruded by certain extrusion equipment to obtain the product. After extrusion, the product is transported manually or onto conveyor equipment. However, manually filling the mold cavity or manually transporting the product not only has a relatively high labor cost, but also has a relatively low delivery efficiency.
发明内容Contents of the invention
本发明的目的是解决目前生产挤压成型产品的人力成本比较高及输送效率比较低的技术问题,提供一种挤压成型产品的压制生产系统。The purpose of the present invention is to solve the technical problems of relatively high labor cost and relatively low conveying efficiency in the current production of extruded products, and provide a press production system for extruded products.
为解决上述技术问题,本发明采用的技术方案是:In order to solve the problems of the technologies described above, the technical solution adopted in the present invention is:
一种挤压成型产品的压制生产系统,包括原料输送装置、压制装置和模具及成品抓取装置;A pressing production system for extruded products, including a raw material conveying device, a pressing device, a mold and a finished product grabbing device;
所述原料输送装置包括第一进料斗、螺旋送料机、加料伺服电机、减速器、称重传感器、第一支撑架、料箕、顶升气缸、第二支撑架、送料斗、送料伺服电机、送料线性模组、滑台、第三支撑架、出料挡板和第一开闭气缸,其中:第二支撑架设在第一支撑架的一侧且其顶面位于第一支撑架的中上部;第三支撑架设在第一支撑架和第二支撑架的前面且其顶面位于第一支撑架的中部;减速器设置于第一支撑架顶面的一边,加料伺服电机的动力输出轴与减速器输入轴联接,螺旋送料机的螺旋杆与减速器的输出轴连接;第一进料斗的出料口与螺旋送料机的进料口连接;料箕设置于螺旋送料机的出料口下方;称重传感器设置于第二支撑架上面并与料箕的底面相接触;顶升气缸的缸体与第二支撑架的顶面连接,顶升气缸的活塞杆与料箕的后部连接;送料线性模组设置于第三支撑架的顶面上;送料伺服电机设置于送料线性模组的一侧并与送料线性模组连接;滑台设置于送料线性模组上面;送料斗装在滑台设置的出料口上;出料挡板设置于送料斗的出料口处;第一开闭气缸设置于滑台下面,出料挡板与第一开闭气缸的活塞杆连接;The raw material conveying device includes a first feeding hopper, a screw feeder, a feeding servo motor, a reducer, a load cell, a first support frame, a material skip, a jacking cylinder, a second support frame, a feeding hopper, and a feeding servo motor , a feeding linear module, a sliding table, a third support frame, a discharge baffle and a first opening and closing cylinder, wherein: the second support frame is set on one side of the first support frame and its top surface is located in the middle of the first support frame The upper part; the third support frame is arranged in front of the first support frame and the second support frame and its top surface is located in the middle of the first support frame; the speed reducer is arranged on one side of the top surface of the first support frame, and the power output shaft of the feeding servo motor It is connected with the input shaft of the reducer, and the screw rod of the screw feeder is connected with the output shaft of the reducer; the outlet of the first feeding hopper is connected with the inlet of the screw feeder; the dustpan is set at the outlet of the screw feeder Below the opening; the load cell is set on the second support frame and is in contact with the bottom surface of the material skip; the cylinder body of the jacking cylinder is connected with the top surface of the second support frame, and the piston rod of the jacking cylinder is connected to the rear of the material skip. Connection; the feeding linear module is set on the top surface of the third support frame; the feeding servo motor is set on one side of the feeding linear module and connected with the feeding linear module; the slide table is set on the feeding linear module; the feeding hopper is installed On the outlet of the sliding table; the outlet baffle is arranged at the outlet of the feeding hopper; the first opening and closing cylinder is arranged under the sliding table, and the outlet baffle is connected with the piston rod of the first opening and closing cylinder;
所述压制装置包括底座、四个减震弹簧、下模具、物料支撑板、顶升缸、两个限位装置、第一压头和升降机构;四个减震弹簧分别设置于底座的四个角上,所述下模具设置于四个减震弹簧上,顶升缸的缸体设置于底座中,顶升缸的活塞杆与物料支撑板连接使物料支撑板位于下模具中间的型腔中;第一压头设置于下模具上方且其与升降机构连接,两个限位装置分别设置于第一压头底面的两侧;The pressing device includes a base, four damping springs, a lower mold, a material support plate, a jacking cylinder, two limit devices, a first pressure head and a lifting mechanism; the four damping springs are respectively arranged on four In the corner, the lower mold is set on four damping springs, the cylinder body of the jacking cylinder is set in the base, the piston rod of the jacking cylinder is connected with the material support plate so that the material support plate is located in the cavity in the middle of the lower mold ; The first indenter is arranged above the lower mold and connected to the lifting mechanism, and the two limit devices are respectively arranged on both sides of the bottom surface of the first indenter;
所述模具及成品抓取装置包括支撑台、输送带装置、动力机构、水平输送装置、垂直输送装置和两个模具输送装置;水平输送装置包括水平线性模组、水平滑块和水平伺服电机,水平线性模组设置于支撑台顶面的中间位置,水平滑块设置在水平线性模组上,水平伺服电机设置于水平线性模组的一端且其与水平线性模组连接;垂直输送装置包括垂直线性模组、垂直滑块、垂直伺服电机、第一抓臂、第一气动夹爪和旋转气缸,垂直线性模组设置于水平滑块前端的上面,垂直伺服电机设置于垂直线性模组的上端并与垂直线性模组连接,垂直滑块设置于垂直线性模组上,第一抓臂的一端与垂直滑块连接,第一抓臂的另一端与旋转气缸的缸体连接,旋转气缸的阀体与第一气动夹爪的缸体连接;输送带装置设置于支撑台的一侧并位于第一气动夹爪的下方;动力机构的动力输出轴与输送带装置中的主动辊连接;两个模具输送装置设在水平滑块顶面后端的两边。The mold and finished product grabbing device includes a support platform, a conveyor belt device, a power mechanism, a horizontal conveying device, a vertical conveying device and two mold conveying devices; the horizontal conveying device includes a horizontal linear module, a horizontal slider and a horizontal servo motor, The horizontal linear module is set in the middle of the top surface of the support table, the horizontal slider is set on the horizontal linear module, the horizontal servo motor is set at one end of the horizontal linear module and connected with the horizontal linear module; the vertical conveying device includes a vertical Linear module, vertical slider, vertical servo motor, first grabbing arm, first pneumatic gripper and rotary cylinder, the vertical linear module is set above the front end of the horizontal slider, and the vertical servo motor is set on the upper end of the vertical linear module And connected with the vertical linear module, the vertical slider is set on the vertical linear module, one end of the first grabbing arm is connected with the vertical slider, the other end of the first grabbing arm is connected with the cylinder body of the rotary cylinder, and the valve of the rotary cylinder The body is connected with the cylinder body of the first pneumatic gripper; the conveyor belt device is arranged on one side of the support platform and below the first pneumatic gripper; the power output shaft of the power mechanism is connected with the driving roller in the conveyor belt device; two The mold conveying device is arranged on both sides of the rear end of the top surface of the horizontal slide block.
可选地,所述原料输送装置还包括振动加料器,所述振动加料器包括壳体、第二进料斗、振动器、细料斗、粗料斗、筛网、细料挡板和第二开闭气缸;所述壳体的底面设有细料口和粗料口,所述细料斗的进口与壳体设置的细料口连接,所述细料斗的出口与滑台设置的细料口连接,细料挡板设置于滑台的细料口处,第二开闭气缸设置于滑台下面且其活塞杆与细料挡板连接;筛网设置于细料斗的进口处;振动器设置于壳体底面的一边;第二进料斗与壳体的一侧上端连接。Optionally, the raw material conveying device further includes a vibrating feeder, and the vibrating feeder includes a housing, a second feeding hopper, a vibrator, a fine hopper, a coarse hopper, a screen, a fine material baffle and a second opening Close the cylinder; the bottom surface of the housing is provided with a fine material port and a coarse material port, the inlet of the fine hopper is connected to the fine material port provided on the housing, and the outlet of the fine hopper is connected to the fine material port provided on the slide table , the fine material baffle is set at the fine material port of the slide table, the second opening and closing cylinder is set under the slide table and its piston rod is connected with the fine material baffle; the screen is set at the entrance of the fine material hopper; the vibrator is set at the One side of the bottom surface of the shell; the second feeding hopper is connected with the upper end of one side of the shell.
可选地,所述原料输送装置还包括压料气缸和第二压头,压料气缸设置于滑台上面且其缸体与滑台连接;第二压头设置于滑台下面并与压料气缸的活塞杆连接。Optionally, the raw material conveying device also includes a pressing cylinder and a second press head, the pressing cylinder is arranged on the slide table and its cylinder body is connected with the slide table; the second press head is arranged under the slide table and connected with the press material The piston rod connection of the cylinder.
可选地,所述原料输送装置还包括喷油嘴,所述喷油嘴设置于滑台的一侧下面。Optionally, the raw material conveying device further includes an oil spray nozzle, and the oil spray nozzle is arranged under one side of the slide table.
可选地,所述模具输送装置包括滑动线性模组、第二抓臂、第二气动夹爪、摆动气缸、滑动块、伺服电机和旋转支座;滑动线性模组的下端与水平滑块顶面的后端连接,滑动块设置于滑动线性模组上;旋转支座设在滑动块上,第二抓臂的一端与旋转支座的一端铰接,第二抓臂的另一端与第二气动夹爪的缸体连接;摆动气缸的缸体与旋转支座的另一端铰接,摆动气缸的活塞杆与第二抓臂一侧的后部铰接;伺服电机设置于滑动线性模组的上端并与滑动线性模组连接。Optionally, the mold conveying device includes a sliding linear module, a second gripping arm, a second pneumatic gripper, a swing cylinder, a sliding block, a servo motor, and a rotary support; the lower end of the sliding linear module is connected to the top of the horizontal slider The rear end of the surface is connected, the sliding block is set on the sliding linear module; the rotating support is set on the sliding block, one end of the second grasping arm is hinged to one end of the rotating support, and the other end of the second grasping arm is connected to the second pneumatic The cylinder body of the gripper is connected; the cylinder body of the swing cylinder is hinged to the other end of the rotary support, and the piston rod of the swing cylinder is hinged to the rear of one side of the second gripping arm; the servo motor is arranged on the upper end of the sliding linear module and connected to the Sliding linear module connection.
可选地,所述模具及成品抓取装置还包括模具清理装置,所述模具清理装置包括左竖直清理气缸、左清洗刷、右竖直清理气缸、右水平清理气缸、右清理刷和气缸支撑架;左竖直清理气缸的缸体嵌入支撑台左侧的机体中,左竖直清理气缸的活塞杆与左清洗刷连接并使左清洗刷位于支撑台的上面;气缸支撑架设置于支撑台右侧的台面上;右水平清理气缸的缸体与气缸支撑架连接,右水平清理气缸的活塞杆与右竖直清理气缸的缸体连接,右竖直清理气缸的活塞杆与右清理刷连接。Optionally, the mold and finished product grabbing device also includes a mold cleaning device, and the mold cleaning device includes a left vertical cleaning cylinder, a left cleaning brush, a right vertical cleaning cylinder, a right horizontal cleaning cylinder, a right cleaning brush and a cylinder Support frame; the cylinder body of the left vertical cleaning cylinder is embedded in the body on the left side of the support platform, the piston rod of the left vertical cleaning cylinder is connected with the left cleaning brush and the left cleaning brush is positioned on the support platform; the cylinder support frame is arranged on the support The table on the right side of the table; the cylinder body of the right horizontal cleaning cylinder is connected with the cylinder support frame, the piston rod of the right horizontal cleaning cylinder is connected with the cylinder body of the right vertical cleaning cylinder, and the piston rod of the right vertical cleaning cylinder is connected with the right cleaning brush connect.
本发明的有益效果是:The beneficial effects of the present invention are:
通过设置螺旋送料机、加料伺服电机、送料斗、送料伺服电机、送料线性模组、滑台、出料挡板和第一开闭气缸等部件,实现原料的自动化输送,使得挤压成型产品时,原料自动填入产品的模型腔中。通过设置输送带装置、动力机构、水平输送装置、垂直输送装置和两个模具输送装置等,提供一种自动抓取模具及产品的装置。因而通过本发明压制产品时,不仅节省人力成本,而且效率比较高。因此,与背景技术相比,本发明具有能够节省人力成本并提高效率等优点。By setting the screw feeder, feeding servo motor, feeding hopper, feeding servo motor, feeding linear module, slide table, discharge baffle and first opening and closing cylinder and other components, the automatic transportation of raw materials is realized, so that when extrusion molding products , the raw material is automatically filled into the mold cavity of the product. By setting a conveyor belt device, a power mechanism, a horizontal conveying device, a vertical conveying device, two mold conveying devices, etc., a device for automatically grabbing molds and products is provided. Therefore, when the product is pressed by the present invention, not only the labor cost is saved, but also the efficiency is relatively high. Therefore, compared with the background technology, the present invention has the advantages of saving labor costs and improving efficiency.
附图说明Description of drawings
图1是本发明的结构示意图。Fig. 1 is a structural schematic diagram of the present invention.
图2是图1中的原料输送装置的主视图。Fig. 2 is a front view of the material conveying device in Fig. 1 .
图3是图2的后视图。FIG. 3 is a rear view of FIG. 2 .
图4是图2的俯视图。FIG. 4 is a top view of FIG. 2 .
图5是图1中压制装置的剖视图。Fig. 5 is a sectional view of the pressing device in Fig. 1 .
图6是图1中模具及成品抓取装置的主视图。Fig. 6 is a front view of the mold and the finished product grasping device in Fig. 1 .
图7是图6的俯视图。FIG. 7 is a top view of FIG. 6 .
图8是图2中振动加料器的主视图。Fig. 8 is a front view of the vibrating feeder in Fig. 2 .
图9是图8的俯视图。FIG. 9 is a top view of FIG. 8 .
实施方式Implementation
下面将结合附图和实施例对本发明作进一步地详细描述。The present invention will be further described in detail with reference to the accompanying drawings and embodiments.
如图1至图7所示,本实施例中的挤压成型产品的压制生产系统包括原料输送装置、压制装置和模具及成品抓取装置;As shown in Figures 1 to 7, the press production system for extruded products in this embodiment includes a raw material conveying device, a pressing device, a mold and a finished product grabbing device;
所述原料输送装置包括第一进料斗1、螺旋送料机2、加料伺服电机3、减速器24、称重传感器4、第一支撑架5、料箕6、顶升气缸7、第二支撑架8、送料斗9、送料伺服电机10、送料线性模组11、滑台12、第三支撑架14、出料挡板16和第一开闭气缸,其中:第二支撑架8设在第一支撑架5的一侧且其顶面位于第一支撑架5的中上部;第三支撑架14设在第一支撑架5和第二支撑架8的前面且其顶面位于第一支撑架5的中部;减速器24设置于第一支撑架5顶面的一边,加料伺服电机3的动力输出轴与减速器24输入轴联接,螺旋送料机2的螺旋杆与减速器24的输出轴连接;第一进料斗1的出料口与螺旋送料机2的进料口连接;料箕6设置于螺旋送料机2的出料口下方;称重传感器4设置于第二支撑架8上面并与料箕6的底面相接触;顶升气缸7的缸体与第二支撑架8的顶面连接,顶升气缸7的活塞杆与料箕6的后部连接;送料线性模组11设置于第三支撑架14的顶面上;送料伺服电机10设置于送料线性模组11的一侧并与送料线性模组11连接;滑台12设置于送料线性模组11上面;送料斗9装在滑台12设置的出料口上;出料挡板16设置于送料斗9的出料口处;第一开闭气缸设置于滑台12下面,出料挡板16与第一开闭气缸的活塞杆连接;The raw material conveying device includes a
所述压制装置包括底座26、四个减震弹簧27、下模具28、物料支撑板32、顶升缸29、两个限位装置30、第一压头31和升降机构;四个减震弹簧27分别设置于底座26的四个角上,所述下模具28设置于四个减震弹簧27上,顶升缸29的缸体设置于底座26中,顶升缸29的活塞杆与物料支撑板32连接使物料支撑板32位于下模具28中间的型腔中;第一压头31设置于下模具28上方且其与升降机构连接,两个限位装置30分别设置于第一压头31底面的两侧;The pressing device comprises a
所述模具及成品抓取装置包括支撑台33、输送带装置34、动力机构35、水平输送装置、垂直输送装置和两个模具输送装置;水平输送装置包括水平线性模组38、水平滑块39和水平伺服电机40,水平线性模组38设置于支撑台33顶面的中间位置,水平滑块39设置在水平线性模组38上,水平伺服电机40设置于水平线性模组38的一端且其与水平线性模组38连接;垂直输送装置包括垂直线性模组41、垂直滑块42、垂直伺服电机43、第一抓臂36、第一气动夹爪37和旋转气缸44,垂直线性模组41设置于水平滑块39前端的上面,垂直伺服电机43设置于垂直线性模组41的上端并与垂直线性模组41连接,垂直滑块42设置于垂直线性模组41上;第一抓臂36的一端与垂直滑块42连接,第一抓臂36的另一端与旋转气缸44的缸体连接,旋转气缸44的阀体与第一气动夹爪37的缸体连接;输送带装置34设置于支撑台33的一侧并位于第一气动夹爪37的下方;动力机构35的动力输出轴与输送带装置34中的主动辊连接;两个模具输送装置设在水平滑块39顶面后端的两边。Described mold and finished product grasping device comprise support table 33,
如图8和图9所示,所述原料输送装置还包括振动加料器13,所述振动加料器13包括壳体23、第二进料斗22、振动器18、细料斗19、粗料斗20、筛网21、细料挡板17和第二开闭气缸;所述壳体23的底面设有细料口和粗料口,所述细料斗19的进口与壳体23设置的细料口连接,所述细料斗19的出口与滑台12设置的细料口连接,细料挡板17设置于滑台12的细料口处,第二开闭气缸设置于滑台12下面且其活塞杆与细料挡板17连接;筛网21设置于细料斗19的进口处;振动器18设置于壳体23底面的一边;第二进料斗22与壳体23的一侧上端连接。As shown in Figures 8 and 9, the raw material conveying device also includes a
可选地,所述原料输送装置还包括压料气缸15和第二压头,压料气缸15设置于滑台12上面且其缸体与滑台12连接;第二压头设置于滑台12下面并与压料气缸15的活塞杆连接。Optionally, the raw material conveying device also includes a pressing
可选地,所述原料输送装置还包括喷油嘴25,所述喷油嘴25设置于滑台12的一侧下面。喷油嘴25与输油泵连接。喷油嘴25用于向模型腔中喷油。通过设置喷油嘴25,使得可以根据需要向产品的下模具28中喷油。Optionally, the raw material conveying device further includes an
可选地,所述模具输送装置包括滑动线性模组45、第二抓臂46、第二气动夹爪47、摆动气缸48、滑动块49、伺服电机50和旋转支座57;滑动线性模组45的下端与水平滑块39顶面的后端连接,滑动块49设置于滑动线性模组45上;旋转支座57设在滑动块49上,第二抓臂46的一端与旋转支座57的一端铰接,第二抓臂46的另一端与第二气动夹爪47的缸体连接;摆动气缸48的缸体与旋转支座57的另一端铰接,摆动气缸48的活塞杆与第二抓臂46一侧的后部铰接;伺服电机50设置于滑动线性模组45的上端并与滑动线性模组45连接。Optionally, the mold conveying device includes a sliding
可选地,模具及成品抓取装置还包括模具清理装置,所述模具清理装置包括左竖直清理气缸51、左清洗刷52、右竖直清理气缸53、右水平清理气缸54、右清理刷55和气缸支撑架56;左竖直清理气缸51的缸体嵌入支撑台33左侧的机体中,左竖直清理气缸51的活塞杆与左清洗刷52连接并使左清洗刷52位于支撑台33的上面;气缸支撑架56设置于支撑台33右侧的台面上;右水平清理气缸54的缸体与气缸支撑架56连接,右水平清理气缸54的活塞杆与右竖直清理气缸53的缸体连接,右竖直清理气缸53的活塞杆与右清理刷55连接。Optionally, the mold and finished product grabbing device also includes a mold cleaning device, and the mold cleaning device includes a left
本发明在使用时,原料输送装置用于向压制装置的下模具28型腔中填入原料。模具及成品抓取装置用于向下模具28型腔中放入模具以及在挤压完成后将成品输送走。挤压装置用于对下模具28型腔中的原料进行挤压形成挤压成型产品。原料输送装置中,滑台12可以在送料伺服电机10的作用下在送料线性模组11上滑动,从而使得进料斗9和振动加料器13中的原料进入下模具28型腔中。压制装置中的升降机构带动第一压头31上下移动,从而进行产品的压制。模具及成品抓取装置中,水平输送装置中的水平滑块39可以在水平伺服电机40的作用下在水平线性模组38上水平滑动,垂直输送装置和两个模具输送装置设置在水平滑块39上,因而它们可以随水平滑块39的运动而在水平线性模组38上水平滑动;垂直滑块42可以在垂直伺服电机43的作用下在垂直线性模组41上上下滑动,第一抓臂36可以随垂直滑块42在垂直线性模组41上上下滑动;两个模具输送装置中,滑动块49可以在伺服电机50的作用下在滑动线性模组45上上下滑动,第二抓臂46可以随滑动块49在滑动线性模组45上上下滑动,第二抓臂46也可以在摆动气缸48的作用下水平摆动。When the present invention is in use, the material conveying device is used to fill the material into the cavity of the
以制备挤压成型产品需要上模和下模为例,本发明使用的步骤为:步骤(1)通过模具及成品抓取装置中的第二气动夹爪47抓取下模并将下模放入下模具28型腔下面的物料支撑板32上,该过程的具体实现方式为:水平伺服电机40控制水平滑块39在水平线性模组38上水平滑动;与此同时,第二抓臂46随滑动块49在伺服电机50的作用下在滑动线性模组45上上下滑动,且第二抓臂46在摆动气缸48的作用下水平摆动,使得第二气动夹爪47到达能够抓取下模的位置后抓取下模;然后,第二气动夹爪47继续运动至下模具28型腔上方后将下模放入下模具28型腔中。步骤(2)通过原料输送装置向下模具28型腔中填入原料,向下模具28中填入原料的方式为:料仓准备好原料后,从第一进料斗1加入,在加料伺服电机3和减速器24的作用下原料经过螺旋送料机2送入料箕6,并经称重传感器4称重;然后,送料伺服电机10控制滑台12在送料线性模组11上行走,使得送料斗9位于料箕6的下方,顶升气缸7的活塞杆顶起料箕6的后部,原料从料箕6倒入送料斗9中;接下来,送料伺服电机10控制滑台12将送料斗9送至下模具28型腔上方,第一开闭气缸控制出料挡板16打开,原料倒入下模具28型腔中。步骤(3)通过模具及成品抓取装置中的第二气动夹爪47抓取下模并将上模放至下模具28型腔中原料的上面,该步骤的具体实现过程可以参见步骤(1)。步骤(4)通过压制装置压制产品,该步骤的具体实现方式为:升降机构控制压头31向下运动挤压下模具28型腔中的原料,直至压缩成型,顶升缸29将物料支撑板32、下模、产品及上模顶起。步骤(5)通过模具及成品抓取装置抓取并运输上模、下模和成品,该过程的具体实现方式为:水平伺服电机40控制水平滑块39在水平线性模组38上运动,第一抓臂36在垂直线性模组41上滑动,从而使第一气动夹爪37移动至能够抓取成品的位置后,通过第一气动夹爪37抓取成品;与此同时,控制两个模具运输装置中的第二抓臂46在滑动线性模组45上移动以及控制摆动气缸47摆动第二抓臂46,使得两个第二抓臂46移动至使两个第二气动夹爪47能够抓取上模和下模的位置,然后通过两个第二气动夹爪47分别抓取上模和下模;然后第一气动夹爪37将成品放置在输送带装置34上,输送带装置34在动力机构35的作用下将成品运到指定地方;两个第二气动夹爪47在摆动气缸48、滑动块49和伺服电机50的作用下分别将上模和下模放置在支撑台33的相应位置。进一步地,当模具及成品抓取装置还包括模具清理装置时,还可以包括步骤(6),通过模具清理装置清洗上模和下模,该过程的具体实现方式为:在清洗上模时,左清洗刷42在左竖直清理气缸51的作用下进行清洗;在清洗下模时,右清理刷55在右水平清理气缸54和右竖直清理气缸53的作用下进行清洗。Taking the upper mold and lower mold required to prepare extruded products as an example, the steps used in the present invention are: step (1) grab the lower mold through the mold and the second
另外,当原料输送装置还包括振动加料器13时,本发明适用于两种原料的挤压成型产品,即一种原料经过送料斗9进入下模具28型腔中时,另一种原料经过第二进料斗22添加至壳体23中,此时启动振动器18对另一种原料进行筛选,以去除另一种原料中的颗粒大的杂质。另一种原料经过筛选后,细料从筛网21进入细料斗19,杂质进入粗料斗20。送料伺服电机10控制滑台12在送料线性模组11上行走,将细料斗19送至下模具28型腔上方,第二开闭气缸控制细料挡板17打开,细料进入下模具28型腔中。当下模具28型腔中加入原料后,可以通过压料气缸15的活塞杆来控制压头挤压原料,从而能够实现在向下模具28型腔填入原料的过程中对原料进行预压,确保制得的产品比较密实。In addition, when the raw material conveying device also includes a vibrating
可以理解的是,以上实施方式仅仅是为了说明本发明的原理而采用的示例性实施方式,然而本发明并不局限于此。对于本领域内的普通技术人员而言,在不脱离本发明的精神和实质的情况下,可以做出各种变型和改进,这些变型和改进也视为本发明的保护范围。It can be understood that, the above embodiments are only exemplary embodiments adopted for illustrating the principle of the present invention, but the present invention is not limited thereto. For those skilled in the art, various modifications and improvements can be made without departing from the spirit and essence of the present invention, and these modifications and improvements are also regarded as the protection scope of the present invention.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201711408548.XA CN107932971B (en) | 2017-12-22 | 2017-12-22 | Press production system for extruded products |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201711408548.XA CN107932971B (en) | 2017-12-22 | 2017-12-22 | Press production system for extruded products |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN107932971A CN107932971A (en) | 2018-04-20 |
| CN107932971B true CN107932971B (en) | 2023-05-26 |
Family
ID=61939725
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201711408548.XA Expired - Fee Related CN107932971B (en) | 2017-12-22 | 2017-12-22 | Press production system for extruded products |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN107932971B (en) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108656613B (en) * | 2018-07-24 | 2023-05-16 | 扬州市职业大学 | A kind of automatic discharge tablet press machine and tablet press method |
| CN108656614B (en) * | 2018-07-24 | 2023-10-13 | 扬州市职业大学 | Tablet pressing method of tablet press |
| CN109747209B (en) * | 2019-01-29 | 2021-01-19 | 安徽沃福机械科技有限公司 | High-speed multifunctional forming device and high-speed multifunctional forming equipment with same |
| CN112810222B (en) * | 2020-12-28 | 2022-11-25 | 杭州波普电器有限公司 | Die stamping device and using method thereof |
| CN118253774A (en) * | 2024-04-15 | 2024-06-28 | 中山市万达机械自动化科技有限公司 | A hydraulic press with a feeding device and a feeding device |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20100120069A (en) * | 2009-05-04 | 2010-11-12 | 김현배 | A fixed capacity supply device for combustibility waste |
| CN103639410A (en) * | 2013-11-28 | 2014-03-19 | 山西中泰源工业自动化设备有限公司 | Mould arrangement worktable for robot system formed by die-casting magnetic materials |
| WO2015159300A1 (en) * | 2014-04-19 | 2015-10-22 | Mahidadia Dhirendra Himatlal | Dosing system with accurate weight |
| CN205464321U (en) * | 2016-04-05 | 2016-08-17 | 营口市双龙射孔器材有限公司 | Automatic suppression production system of metal powder types of medicine cover |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102005027032B4 (en) * | 2005-06-11 | 2007-06-28 | Sms Meer Gmbh | Device for producing a molded part |
-
2017
- 2017-12-22 CN CN201711408548.XA patent/CN107932971B/en not_active Expired - Fee Related
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20100120069A (en) * | 2009-05-04 | 2010-11-12 | 김현배 | A fixed capacity supply device for combustibility waste |
| CN103639410A (en) * | 2013-11-28 | 2014-03-19 | 山西中泰源工业自动化设备有限公司 | Mould arrangement worktable for robot system formed by die-casting magnetic materials |
| WO2015159300A1 (en) * | 2014-04-19 | 2015-10-22 | Mahidadia Dhirendra Himatlal | Dosing system with accurate weight |
| CN205464321U (en) * | 2016-04-05 | 2016-08-17 | 营口市双龙射孔器材有限公司 | Automatic suppression production system of metal powder types of medicine cover |
Also Published As
| Publication number | Publication date |
|---|---|
| CN107932971A (en) | 2018-04-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN107932971A (en) | The compacting production system of extrusion forming product | |
| CN108995017A (en) | One kind exempting from supporting plate static pressure block machine | |
| CN109664544B (en) | Automatic pressing device for powder materials | |
| CN211492534U (en) | Automatic compensation filling device for isostatic compaction of energetic material | |
| CN111573184B (en) | Loading and unloading conveyor | |
| CN115556226A (en) | Concrete prefabricated part pouring forming equipment and forming method | |
| CN106272904A (en) | A kind of convertible forming machine for concrete building unit | |
| CN204278214U (en) | A kind of heat insulation building block automatic assembly line | |
| CN105690550A (en) | Automatic pressing machine mold for cylindrical refractory bricks, fully-automatic hydraulic brick pressing machine and brick pressing process | |
| CN205114549U (en) | Automatic powder pouring equipment | |
| CN204725654U (en) | A kind of brick machine and feeding thereof go out brick device, feed mechanism | |
| CN119175362A (en) | Lost foam casting production line | |
| CN201357476Y (en) | Reciprocating plate supply automatic block making machine | |
| CN105619573B (en) | Tubular refractory brick automatic hydraulic press and pressure brickwork skill | |
| CN207808579U (en) | The compacting production system of extrusion forming product | |
| CN202985726U (en) | Block molding machine | |
| CN105834377A (en) | Full-automatic box molding equipment and casting production line based on equipment | |
| CN111038795B (en) | A capacitor intelligent counting, transfer, discharge, packaging and output system | |
| CN103089874B (en) | Full-automatic motor vehicle friction plate production device | |
| CN211221297U (en) | Brick making machine for making small-sized reinforced concrete products | |
| CN206154480U (en) | Convertible concrete member make -up machine | |
| CN118358969A (en) | Automatic demoulding and conveying equipment and method for sleeper production line | |
| CN106738193B (en) | Concrete formwork block manufacturing machine | |
| CN100480011C (en) | Method for mould pressing preparing artistic handicraft using plant waste material | |
| CN115534091A (en) | A prefabricated component forming production line and its production method |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20230526 |