CN104669993B - A kind of automobile rear door assembly and automobile - Google Patents
A kind of automobile rear door assembly and automobile Download PDFInfo
- Publication number
- CN104669993B CN104669993B CN201510076123.8A CN201510076123A CN104669993B CN 104669993 B CN104669993 B CN 104669993B CN 201510076123 A CN201510076123 A CN 201510076123A CN 104669993 B CN104669993 B CN 104669993B
- Authority
- CN
- China
- Prior art keywords
- back door
- inner panel
- reinforcement plate
- automobile
- plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 230000003014 reinforcing effect Effects 0.000 claims abstract description 19
- 239000000463 material Substances 0.000 claims abstract description 14
- 229920000049 Carbon (fiber) Polymers 0.000 claims abstract description 11
- 239000004917 carbon fiber Substances 0.000 claims abstract description 11
- VNWKTOKETHGBQD-UHFFFAOYSA-N methane Chemical compound C VNWKTOKETHGBQD-UHFFFAOYSA-N 0.000 claims abstract description 11
- 230000002787 reinforcement Effects 0.000 claims description 57
- 238000000034 method Methods 0.000 abstract description 15
- 238000004519 manufacturing process Methods 0.000 abstract description 9
- 238000003466 welding Methods 0.000 abstract description 8
- 239000000853 adhesive Substances 0.000 abstract 1
- 230000001070 adhesive effect Effects 0.000 abstract 1
- 239000002184 metal Substances 0.000 description 6
- 239000000446 fuel Substances 0.000 description 4
- 238000009957 hemming Methods 0.000 description 3
- 238000002347 injection Methods 0.000 description 3
- 239000007924 injection Substances 0.000 description 3
- 238000001746 injection moulding Methods 0.000 description 2
- 238000009434 installation Methods 0.000 description 2
- 238000012423 maintenance Methods 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 238000007789 sealing Methods 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images

Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02T—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO TRANSPORTATION
- Y02T10/00—Road transport of goods or passengers
- Y02T10/10—Internal combustion engine [ICE] based vehicles
- Y02T10/40—Engine management systems
Landscapes
- Body Structure For Vehicles (AREA)
- Superstructure Of Vehicle (AREA)
Abstract
Description
技术领域technical field
本发明涉及汽车工程技术领域,具体涉及一种汽车后背门总成及汽车。The invention relates to the technical field of automobile engineering, in particular to an automobile back door assembly and an automobile.
背景技术Background technique
汽车后背门多指两厢车、SUV车型的后备箱开启门,大多采用上翻式结构,是车身中最重要的开启件,在车辆开启、行李存放、装饰、零件维修等方面具有非常重要的作用。后背门的好坏,主要体现在后背门的防撞性能、密封性能、开合便利性以及其他性能指标上。The back door of a car mostly refers to the trunk opening door of hatchback cars and SUV models. Most of them adopt an upturned structure. It is the most important opening part in the car body. effect. The quality of the back door is mainly reflected in the anti-collision performance, sealing performance, opening and closing convenience and other performance indicators of the back door.
传统的汽车后背门总成的结构与制造工艺为:后背门外板总成和后背门内板总成包边、焊接后构成后背门钣金总成,然后后背门装饰板通过卡扣卡接在后背门钣金总成上形成汽车后背门总成。其中,后背门内板总成由后背门内板、铰链加强板、气动支撑杆加强板、锁扣安装板焊接而成。中国发明专利CN203188829U和CN203186048U均有铰链加强板与后背门内板是焊接连接的描述。后背门外板总成包括后背门外板。上述的后背门内板、后背门外板、铰链加强板、气动支撑杆加强杆、锁扣安装板均由钢板冲压而成,后背门装饰板和卡扣注塑成型,所以汽车后背门总成制造过程中需要借助于大量的钣金冲压模具、注塑模具,模具成本投入大,夹具数量多,零件数量也多,零件装配时间较长,工作效率低,成本高。The structure and manufacturing process of the traditional automobile back door assembly are: the back door outer panel assembly and the back door inner panel assembly are hemmed, welded to form a back door sheet metal assembly, and then the back door decorative panel The automobile rear door assembly is formed by snapping on the back door sheet metal assembly. Among them, the back door inner panel assembly is welded by the back door inner panel, the hinge reinforcement plate, the pneumatic support rod reinforcement plate, and the lock installation plate. Chinese invention patents CN203188829U and CN203186048U all have the description that the hinge reinforcement plate and the inner panel of the back door are welded. The back door outer panel assembly includes the back door outer panel. The above-mentioned rear door inner panel, rear door outer panel, hinge reinforcement plate, pneumatic support rod reinforcement rod, and lock installation plate are all stamped from steel plates, and the rear door decorative panel and buckle are injection molded, so the back of the car The manufacturing process of the door assembly requires a large number of sheet metal stamping dies and injection molds. The cost of the molds is large, the number of fixtures is large, the number of parts is also large, the assembly time of parts is long, the work efficiency is low, and the cost is high.
后背门内板和后背门外板冲压成型后包边、焊接,如中国发明专利CN202320523U公开的一种汽车后背门结构,后背门内板的一侧边与后背门外板的一端焊接,所述后背门外板上具有一向外隆起部,后背门外板的另一端弯折成断面为“L”型的包边,将后背门内板的另一侧边置于包边内。存在的问题是:包边工艺复杂,加工效率低。The inner panel of the back door and the outer panel of the back door are stamped and formed and then hemmed and welded. For example, in the structure of the back door of an automobile disclosed in Chinese invention patent CN202320523U, one side of the inner panel of the back door is connected to the outer panel of the back door. One end is welded, the outer panel of the back door has an outward bulge, the other end of the outer panel of the back door is bent into an "L"-shaped hemming section, and the other side of the inner panel of the back door is placed inside the edge. The existing problems are: the hemming process is complex and the processing efficiency is low.
另外,后背门内板、后背门外板均采用金属材料制造,增加了汽车重量,增加油耗。In addition, the inner panel of the back door and the outer panel of the back door are all made of metal materials, which increases the weight of the vehicle and increases fuel consumption.
发明内容Contents of the invention
本发明要解决的技术问题是提供一种汽车后背门总成及汽车,减少冲压模具和注塑模具数量,降低模具成本投入;取消后背门内、外板的包边工艺,提高加工效率。The technical problem to be solved by the present invention is to provide an automobile back door assembly and an automobile, reduce the number of stamping dies and injection molds, reduce mold cost investment; cancel the hemming process of the inner and outer panels of the back door, and improve processing efficiency.
为解决上述技术问题,本发明的实施例提供一种汽车后背门总成,包括后背门外板总成和后背门内板总成,所述后背门外板总成包括由碳纤维材料模压、拉挤成型的后背门外板,所述后背门内板总成包括由碳纤维材料模压、拉挤成型的后背门内板、以及铰链加强板、气动支撑杆加强板和锁扣加强板;In order to solve the above technical problems, an embodiment of the present invention provides an automobile back door assembly, including a back door outer panel assembly and a back door inner panel assembly, the back door outer panel assembly is made of carbon fiber Material molded, pultruded rear door outer panel, the rear door inner panel assembly includes molded carbon fiber material, pultruded rear door inner panel, hinge reinforcement plate, pneumatic support rod reinforcement plate and lock buckle reinforcement plate;
所述铰链加强板、气动支撑杆加强板和锁扣加强板在所述后背门内板成型时预埋于模具内,采用粘接的方式固设于后背门内板上;The hinge reinforcement plate, pneumatic support rod reinforcement plate and lock buckle reinforcement plate are pre-buried in the mold when the back door inner panel is formed, and are fixed on the back door inner panel by bonding;
所述后背门外板粘接于后背门内板的外侧。The outer panel of the rear door is bonded to the outer side of the inner panel of the rear door.
上述结构中,后背门内板和后背门外板均采用碳纤维材料,材料轻,强度高,可以根据后背门的强度要求进行适当的调整后背门内板和后背门外板的料厚。后背门内板和后背门外板不再采用钣金件,取消传统的后背门内板和后背门外板的冲压模具,模具数量减少,成本降低;汽车重量减轻,降低油耗。In the above structure, both the inner panel of the back door and the outer panel of the back door are made of carbon fiber material, which is light in weight and high in strength, and can be properly adjusted according to the strength requirements of the back door. The material is thick. The inner panel of the back door and the outer panel of the back door no longer use sheet metal parts, and the traditional stamping dies for the inner panel of the back door and the outer panel of the back door are cancelled, the number of molds is reduced, and the cost is reduced; the weight of the car is reduced, and the fuel consumption is reduced.
铰链加强板、气动支撑杆加强板和锁扣加强板在所述后背门内板成型时预埋于模具内,采用粘接的方式固设于后背门内板上,取消传统的焊接工艺,提高生产效率。The hinge reinforcement plate, the pneumatic support rod reinforcement plate and the lock buckle reinforcement plate are pre-buried in the mold when the inner panel of the back door is formed, and fixed on the inner panel of the back door by bonding, eliminating the traditional welding process ,Increase productivity.
后背门外板粘接于后背门内板的外侧,取消传统的包边、焊接工艺,工艺简化,提高生产效率。The outer panel of the back door is bonded to the outer side of the inner panel of the back door, canceling the traditional wrapping and welding process, simplifying the process and improving production efficiency.
其中,所述后背门内板总成还包括通过螺栓与所述后背门内板固定连接的后背门扣手装饰板。上述结构中,后背门扣手装饰板由传统的通过卡扣与后背门内板卡接变更为通过螺栓固定连接,方便拆卸、检修线束等其他附件;同时取消卡扣这个零件及其注塑模具,零件和模具数量减少,降低成本。Wherein, the back door inner panel assembly further includes a back door buckle handle decorative plate fixedly connected to the back door inner panel by bolts. In the above structure, the decorative panel of the back door buckle is changed from the traditional snap connection with the inner panel of the back door through a buckle to a fixed connection through bolts, which is convenient for disassembly and maintenance of wiring harness and other accessories; at the same time, the snap part and its injection molding are cancelled. Tooling, parts and tooling counts are reduced, reducing costs.
其中,所述后背门外板总成还包括设于后背门外板外侧上部的高位制动灯紧固件。Wherein, the rear door outer panel assembly further includes a high-mounted brake lamp fastener provided on the outer upper part of the rear door outer panel.
其中,所述后背门内板总成还包括缓冲块加强板,于所述后背门内板成型时预埋于模具内,采用粘接的方式固设于后背门内板上。Wherein, the rear door inner panel assembly also includes a buffer block reinforcement plate, which is pre-embedded in the mold when the rear door inner panel is formed, and fixed on the rear door inner panel by bonding.
进一步,所述铰链加强板包括左铰链加强板和右铰链加强板,分别固设于后背门内板上部的左、右侧。所述气动支撑杆加强板包括左气动支撑杆加强板和右气动支撑杆加强板,分别固设于后背门内板中部的左、右侧。所述缓冲块加强板包括左缓冲块加强板和右缓冲块加强板,分别固设于后背门内板下部的左、右侧。Further, the hinge reinforcement plate includes a left hinge reinforcement plate and a right hinge reinforcement plate, which are respectively fixed on the left and right sides of the inner panel of the back door. The pneumatic support rod reinforcement plate includes a left pneumatic support rod reinforcement plate and a right pneumatic support rod reinforcement plate, which are respectively fixed on the left and right sides of the middle part of the back door inner panel. The buffer block reinforcing plate includes a left buffer block reinforcing plate and a right buffer block reinforcing plate, which are respectively fixed on the left and right sides of the lower part of the back door inner panel.
本发明实施例还提供一种汽车,该汽车包括上述的汽车后背门总成。An embodiment of the present invention also provides an automobile, which includes the above-mentioned automobile rear door assembly.
本发明的上述技术方案的有益效果如下:The beneficial effects of above-mentioned technical scheme of the present invention are as follows:
上述方案中,后背门内板和后背门外板均采用碳纤维材料,材料轻,强度高,可以根据后背门的强度要求进行适当的调整后背门内板和后背门外板的料厚。后背门内板和后背门外板不再采用钣金件,取消传统的后背门内板和后背门外板的冲压模具,模具数量减少,成本降低;汽车重量减轻,降低油耗。铰链加强板、气动支撑杆加强板和锁扣加强板在所述后背门内板成型时预埋于模具内,采用粘接的方式固设于后背门内板上,取消传统的焊接工艺,提高生产效率。后背门外板粘接于后背门内板的外侧,取消传统的包边、焊接工艺,工艺简化,提高生产效率。In the above scheme, both the inner panel of the back door and the outer panel of the back door are made of carbon fiber material, which is light in weight and high in strength, and can be properly adjusted according to the strength requirements of the back door. The material is thick. The inner panel of the back door and the outer panel of the back door no longer use sheet metal parts, and the traditional stamping dies for the inner panel of the back door and the outer panel of the back door are cancelled, the number of molds is reduced, and the cost is reduced; the weight of the car is reduced, and the fuel consumption is reduced. The hinge reinforcement plate, the pneumatic support rod reinforcement plate and the lock buckle reinforcement plate are pre-buried in the mold when the inner panel of the back door is formed, and fixed on the inner panel of the back door by bonding, eliminating the traditional welding process ,Increase productivity. The outer panel of the back door is bonded to the outer side of the inner panel of the back door, canceling the traditional wrapping and welding process, simplifying the process and improving production efficiency.
附图说明Description of drawings
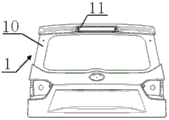
图1为本发明实施例一中后背门外板总成的结构示意图;Fig. 1 is a schematic structural view of the rear door outer panel assembly in
图2为实施例一中后背门内板总成的结构示意图。Fig. 2 is a schematic structural view of the rear door inner panel assembly in the first embodiment.
附图标记说明:Explanation of reference signs:
1、后背门外板总成;1. Back door outer panel assembly;
10、后背门外板;10. Back door outer panel;
11、高位制动灯紧固件;11. Fasteners for high position brake lights;
2、后背门内板总成;2. Back door inner panel assembly;
20、后背门内板;20. The inner panel of the back door;
21、铰链加强板;21. Hinge reinforcement plate;
22、气动支撑杆加强板;22. Pneumatic support rod reinforcement plate;
23、锁扣加强板;23. Lock reinforcement plate;
24、缓冲块加强板;24. Buffer block reinforcement plate;
25、后背门扣手装饰板。25. Decorative panel for the back door button handle.
具体实施方式Detailed ways
为使本发明要解决的技术问题、技术方案和优点更加清楚,下面将结合附图及具体实施例进行详细描述。In order to make the technical problems, technical solutions and advantages to be solved by the present invention clearer, the following will describe in detail with reference to the drawings and specific embodiments.
本发明针对现有的汽车后背门总成零件和模具数量多、生产工艺复杂、生产成本高等问题,提供一种汽车后背门总成以及汽车。The invention aims at the problems of large number of parts and moulds, complicated production process and high production cost in the existing automobile rear door assembly, and provides an automobile rear door assembly and an automobile.
本发明的实施例提供一种汽车后背门总成,包括后背门外板总成和后背门内板总成。如图1所示,所述后背门外板总成1包括由碳纤维材料模压、拉挤成型的后背门外板10,所述后背门外板10的外侧上部设有高位制动灯紧固件11。An embodiment of the present invention provides an automobile back door assembly, including a back door outer panel assembly and a back door inner panel assembly. As shown in Figure 1, the rear door
如图2所示,所述后背门内板总成2包括由碳纤维材料模压、拉挤成型的后背门内板20、以及铰链加强板21、气动支撑杆加强板22、锁扣加强板23和缓冲块加强板24。As shown in Figure 2, the back door
所述铰链加强板21、气动支撑杆加强板22、锁扣加强板23和缓冲块加强板24在所述后背门内板20成型时预埋于模具内,采用粘接的方式固设于后背门内板20上。The
所述后背门外板10粘接于后背门内板20的外侧。The rear door
所述后背门内板总成2还包括通过螺栓与所述后背门内板20固定连接的后背门扣手装饰板25。上述结构中,后背门扣手装饰板由传统的通过卡扣与后背门内板卡接变更为通过螺栓固定连接,方便拆卸、检修线束等其他附件;同时取消卡扣这个零件及其注塑模具,零件和模具数量减少,降低成本。The back door
本实施例中,所述铰链加强板21包括左铰链加强板和右铰链加强板,分别固设于后背门内板20上部的左、右侧。In this embodiment, the
所述气动支撑杆加强板22包括左气动支撑杆加强板和右气动支撑杆加强板,分别固设于后背门内板20中部的左、右侧。The pneumatic support
所述缓冲块加强板24包括左缓冲块加强板和右缓冲块加强板,分别固设于后背门内板下部的左、右侧。The buffer
本发明实施例一还提供一种汽车,该汽车包括上述的汽车后背门总成。
本发明中,后背门内板和后背门外板均采用碳纤维材料,材料轻,强度高,可以根据后背门的强度要求进行适当的调整后背门内板和后背门外板的料厚。后背门内板和后背门外板不再采用钣金件,取消传统的后背门内板和后背门外板的冲压模具,模具数量减少,成本降低;汽车重量减轻,降低油耗。铰链加强板、气动支撑杆加强板和锁扣加强板在所述后背门内板成型时预埋于模具内,采用粘接的方式固设于后背门内板上,取消传统的焊接工艺,提高生产效率。后背门外板粘接于后背门内板的外侧,取消传统的包边、焊接工艺,工艺简化,提高生产效率。In the present invention, both the inner panel of the back door and the outer panel of the back door are made of carbon fiber material, which is light in weight and high in strength, and the inner panel of the back door and the outer panel of the back door can be properly adjusted according to the strength requirements of the back door. The material is thick. The inner panel of the back door and the outer panel of the back door no longer use sheet metal parts, and the traditional stamping dies for the inner panel of the back door and the outer panel of the back door are cancelled, the number of molds is reduced, and the cost is reduced; the weight of the car is reduced, and the fuel consumption is reduced. The hinge reinforcement plate, the pneumatic support rod reinforcement plate and the lock buckle reinforcement plate are pre-buried in the mold when the inner panel of the back door is formed, and fixed on the inner panel of the back door by bonding, eliminating the traditional welding process ,Increase productivity. The outer panel of the back door is bonded to the outer side of the inner panel of the back door, canceling the traditional wrapping and welding process, simplifying the process and improving production efficiency.
以上所述是本发明的优选实施方式,应当指出,对于本技术领域的普通技术人员来说,在不脱离本发明所述原理的前提下,还可以作出若干改进和润饰,这些改进和润饰也应视为本发明的保护范围。The above description is a preferred embodiment of the present invention, it should be pointed out that for those of ordinary skill in the art, without departing from the principle of the present invention, some improvements and modifications can also be made, and these improvements and modifications can also be made. It should be regarded as the protection scope of the present invention.
Claims (5)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201510076123.8A CN104669993B (en) | 2015-02-12 | 2015-02-12 | A kind of automobile rear door assembly and automobile |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201510076123.8A CN104669993B (en) | 2015-02-12 | 2015-02-12 | A kind of automobile rear door assembly and automobile |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN104669993A CN104669993A (en) | 2015-06-03 |
| CN104669993B true CN104669993B (en) | 2023-05-16 |
Family
ID=53305792
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201510076123.8A Expired - Fee Related CN104669993B (en) | 2015-02-12 | 2015-02-12 | A kind of automobile rear door assembly and automobile |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN104669993B (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR3038575B1 (en) * | 2015-07-09 | 2018-11-09 | Renault Sas | STRUCTURAL ELEMENT OF A CASE OF A MOTOR VEHICLE COMPRISING AN INTERCHANGEABLE MODULE |
| CN111994171B (en) * | 2020-09-02 | 2022-10-21 | 奇瑞商用车(安徽)有限公司 | Frame type tail door frame structure and installation steps thereof |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN201784432U (en) * | 2010-06-02 | 2011-04-06 | 奇瑞汽车股份有限公司 | Automobile back door reinforcement structure |
| CN202624394U (en) * | 2012-06-29 | 2012-12-26 | 无锡同捷汽车设计有限公司 | Back door assembly of two-carriage vehicle, and two-carriage vehicle |
| CN103057453A (en) * | 2013-01-21 | 2013-04-24 | 内蒙古第一机械集团有限公司 | Dumper carriage made of aluminum alloy honeycomb plates |
| CN203046844U (en) * | 2012-12-19 | 2013-07-10 | 杭州华聚复合材料有限公司 | Door structure of refrigerated truck carriage body |
| CN203713981U (en) * | 2013-12-19 | 2014-07-16 | 全耐塑料公司 | Structural component of motor vehicle closure member and motor vehicle closure member containing same |
-
2015
- 2015-02-12 CN CN201510076123.8A patent/CN104669993B/en not_active Expired - Fee Related
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN201784432U (en) * | 2010-06-02 | 2011-04-06 | 奇瑞汽车股份有限公司 | Automobile back door reinforcement structure |
| CN202624394U (en) * | 2012-06-29 | 2012-12-26 | 无锡同捷汽车设计有限公司 | Back door assembly of two-carriage vehicle, and two-carriage vehicle |
| CN203046844U (en) * | 2012-12-19 | 2013-07-10 | 杭州华聚复合材料有限公司 | Door structure of refrigerated truck carriage body |
| CN103057453A (en) * | 2013-01-21 | 2013-04-24 | 内蒙古第一机械集团有限公司 | Dumper carriage made of aluminum alloy honeycomb plates |
| CN203713981U (en) * | 2013-12-19 | 2014-07-16 | 全耐塑料公司 | Structural component of motor vehicle closure member and motor vehicle closure member containing same |
Also Published As
| Publication number | Publication date |
|---|---|
| CN104669993A (en) | 2015-06-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105980180B (en) | Composite material lever gear door | |
| CN113846924B (en) | Hinge mounting structure for C-shaped column of split door | |
| JP2017508656A (en) | Combined lift gate | |
| CN103587390A (en) | Modularized vehicle door with steel, aluminum and plastic mixed | |
| CN201769903U (en) | Automotive wheel fender | |
| CN201390292Y (en) | Car front fender assembly | |
| CN104669993A (en) | Automobile rear back door assembly and automobile | |
| CN205498569U (en) | Light car back door | |
| CN205836477U (en) | A kind of exit structure of PDCPD material | |
| CN207015438U (en) | A kind of vehicle side-wall outer-plate | |
| CN203806014U (en) | Side beam structure shared by front floor assemblies of old and new vehicle models | |
| CN206012298U (en) | Automotive back door assembly | |
| CN217320278U (en) | Lightweight truck front bumper | |
| CN210592144U (en) | Bearing type vehicle body structure and prowl car | |
| CN205971517U (en) | Electric automobile houding beam assembly | |
| CN204871221U (en) | Car A post and car | |
| CN116238600A (en) | A vehicle side wall assembly and vehicle | |
| CN207579816U (en) | A kind of heavy truck metal front bumper assembly based on lightweight structure | |
| CN207416740U (en) | A kind of automobile back door balustrade exterior panelling | |
| CN201833965U (en) | Structure of outer plate and decoration strip of luggage compartment door | |
| CN207078203U (en) | For the maximized new body side wall rear end structure of rear triangle window clear field | |
| CN217532722U (en) | car luggage rack | |
| CN205256254U (en) | Truck front bumper | |
| CN219236426U (en) | Vacuum activated cladding | |
| CN209921013U (en) | Installing support and car of door handrail box |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20230516 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |