CN103357766A - Complex spin-riveting head, spin-riveting machine, and press-fitting and spin-riveting complex assembly process for automotive ball pins - Google Patents
Complex spin-riveting head, spin-riveting machine, and press-fitting and spin-riveting complex assembly process for automotive ball pins Download PDFInfo
- Publication number
- CN103357766A CN103357766A CN2012100872167A CN201210087216A CN103357766A CN 103357766 A CN103357766 A CN 103357766A CN 2012100872167 A CN2012100872167 A CN 2012100872167A CN 201210087216 A CN201210087216 A CN 201210087216A CN 103357766 A CN103357766 A CN 103357766A
- Authority
- CN
- China
- Prior art keywords
- ball
- push rod
- spin
- riveting
- press
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title abstract description 10
- 230000008569 process Effects 0.000 title abstract description 7
- 150000001875 compounds Chemical class 0.000 claims description 25
- 238000005516 engineering process Methods 0.000 claims description 11
- 230000000694 effects Effects 0.000 claims description 7
- 238000007789 sealing Methods 0.000 claims description 7
- 238000006073 displacement reaction Methods 0.000 claims description 6
- 241001133184 Colletotrichum agaves Species 0.000 claims description 5
- 238000004519 manufacturing process Methods 0.000 abstract description 6
- 238000003754 machining Methods 0.000 description 5
- 230000010354 integration Effects 0.000 description 3
- 230000007246 mechanism Effects 0.000 description 2
- 230000003068 static effect Effects 0.000 description 2
- 238000010009 beating Methods 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 230000008878 coupling Effects 0.000 description 1
- 238000010168 coupling process Methods 0.000 description 1
- 238000005859 coupling reaction Methods 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 238000005538 encapsulation Methods 0.000 description 1
- 239000012467 final product Substances 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 239000000725 suspension Substances 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
- 230000001131 transforming effect Effects 0.000 description 1
- 238000007514 turning Methods 0.000 description 1
Images


Landscapes
- Automatic Assembly (AREA)
Abstract
The invention aims to provide a complex spin-riveting head, a spin-riveting machine, and a press-fitting and spin-riveting complex assembly process for automotive ball pins in order to improve production efficiency and reduce production cost. An ejector rod is added to the middle of the complex spin-riveting head of the spin-riveting machine. An elastic module is fitted the base end of the ejector rod. A circular ball guide is disposed on the upper end surface of the elastic module. A ball pin, a ball bowl and an end cover are sequentially placed in a ball seat; the ejector rod is powered by a spindle of the spin-riveting machine to descend; when the spindle of the spin-riveting machine descends, the ejector rod also descends and contacts with the end cover to stress and deform a rubber block; with descent increasing, pressure of the ejector rod forces the end cover and the ball bowl which are slowly pressed into the ball seat; the spindle of the spin-riveting machine continues descending; the ball bowl is tightly pressed in the ball seat so that the ejector rod is fully tightly ejected; under the action of continuous deformation of the elastic module, a roller of the spin-riveting machine successfully contacts with a turned edge of the ball seat, while the ejector rod is kept unchanged; a ball on the circular ball guide auto-rotates to immobilize the ejector rod; finally, the ball pin is sealed.
Description
Technical field
The present invention relates to revolve die, riveter and car ball stud and press-fit, revolve the riveting assembly technology.
Background technology
For satisfying automobile lateral rotation in the process of moving and vertically beating, ball stud often applies among the chain connection of motor turning, suspension, is vitals and the safety member of automobile.Ball stud mainly is comprised of ball seat, ball bowl, ball pin, end cap, dust cover, jump ring etc., wherein ball bowl, ball pin need to utilize press-loading device that it is pressed among the ball seat together, the ball seat turn-up portion is divided carry out machining deformation by revolving riveting equipment again, finish the final encapsulation of ball stud.
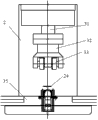
Now, most auto parts and components manufacturing enterprise all adopts above-mentioned technique when making the ball stud associated components.Among Fig. 1, Reference numeral 1,21,20,23,22,10 indicates respectively forcing press, ball bowl, workbench, ball seat, ball stud, pressure head.Among Fig. 2, Reference numeral 2,31,32,33,35,24 respectively mark riveter, main shaft, revolve die, roller, workbench, end cap.As shown in Figure 1 and Figure 2, at first ball stud 22 is put into ball seat 23, utilize press 1 that ball bowl 21 is pressed into ball seat 23, make ball bowl 21 that deformation occur and cooperate with the ball stud bulb.Then place end cap 24, and divide by 2 pairs of ball seat turn-up portion of riveter and to carry out machining deformation, finally reach the effect of ball stud sealing.
Can find out that the assembling of ball stud need to use press and two equipment of riveter to finish smoothly usually.The input of lathe and frock clamp just becomes a large problem of relevant processing enterprise, and personnel's outfit also can correspondingly increase, and production efficiency is difficult to promote.
Summary of the invention
The object of the present invention is to provide compound die, riveter and the car ball stud of revolving to press-fit and revolve the riveting Applying Compound Assembling Technology, so that production efficiency improves, reduces production costs.
For realizing that having of described purpose press-fits the compound die that revolves of function, comprise and revolve die, be characterized in, also comprise push rod and pressure-bearing module, revolve die and establish axial center hole, establish this push rod and pressure-bearing module in this axial center hole, expose outside revolving die on the top of push rod, the pressure-bearing module is attached to the cardinal extremity of push rod, and this pressure-bearing module produces axial displacement so that this push rod shrinks in this axial center hole in this axial center hole after bearing pressure.
Described have a compound die that revolves that press-fits function, and its further characteristics are, this pressure-bearing module is elastic module, and this axial displacement is the axial elasticity deflection of elastic module.
Described have a compound die that revolves that press-fits function, and its further characteristics are that this pressure-bearing module is the executing agency of hydraulic system.
Described have a compound die that revolves that press-fits function, and its further characteristics are that the end in contrast to this push rod of this pressure-bearing module is equipped with plane bearing.
Described have a compound die that revolves that press-fits function, and its further characteristics are that this plane bearing is spherical guide.
For realizing the riveter of described purpose, be characterized in, comprise aforementioned arbitrary compound die that revolves, described revolving on the main shaft that die is connected to riveter.
Revolve the riveting Applying Compound Assembling Technology for the car ball stud of realizing described purpose press-fits, be characterized in, add push rod in the middle of the anchor head revolving of riveter, set elastic module at the cardinal extremity of push rod, place a pair of annular spherical guide in the upper surface of elastic module; At first with ball pin and ball bowl, end cap is successively placed in the ball seat, utilize the riveter main shaft that power source is provided so that push rod descends, when the riveter main shaft descends, push rod descends and simultaneously with after end cap contacts, make the block rubber compressive deformation, continuous increase along with slippage, the pressure of push rod forces end cap and ball bowl slowly to be pressed in the ball seat, the riveter main shaft continues to walk downward afterwards, thereby in ball seat make push rod complete dieback owing to the ball bowl kills this moment, under the effect that elastic module constantly is out of shape, the roller of riveter divides with the ball seat turn-up portion smoothly and contacts and the push rod holding position is constant, the ball rotation of annular spherical guide makes the push rod transfixion, finally realizes the ball stud sealing.
Described car ball stud press-fits and revolves the riveting Applying Compound Assembling Technology, and its further characteristics are that described elastic module is block rubber.
When push rod with after the workpiece end cap contacts, the ball bowl is pressed into ball seat, the pressure-bearing module has backward displacement simultaneously, push rod with ball bowl, end cap dieback after, the pressure-bearing module remains unchanged the push rod position and the main shaft of riveter can drive roller rotation and walk downward, finally revolve die and the ball seat turn-up portion is divided carry out machining deformation, finish the ball stud sealing.Therefore can realize ball stud is press-fited and these two kinds of process integrations of roll riveting are finished continuously to a technique.
If revolve on the main shaft that die appends to riveter compound, then ball stud is press-fited and these two kinds of process integration to machines of roll riveting are finished continuously.
For avoiding push rod also to rotate, above the pressure-bearing module, add a plane bearing, make push rod remain static.
Need a large amount of connectors between automotive wheel and chassis, in order to satisfy the requirement of rotation in the Vehicle Driving Cycle process and bob, vibration, ball stud becomes a part indispensable in the Automobile Chassis Parts.Along with constantly popularizing that human automobile uses, the demand of ball stud also will improve constantly.Obviously, pressure and these two kinds of techniques of riveting are integrated in the ball stud assembly technology will further be promoted.
Description of drawings
Fig. 1, Fig. 2 are respectively the schematic diagram that existing car ball stud press-fits, revolves the riveting assembly technology.
Fig. 3 is riveter overall schematic of the present invention.
Fig. 4 is the compound structural representation that revolves die of the present invention.
The specific embodiment
The shaft portion that revolves die among Fig. 4 has carried out partly cuing open, so that show its internal structure.As shown in Figure 3 and Figure 4, in one embodiment of this invention, the compound die 4 that revolves comprises and revolves die 41, push rod 42, pressure-bearing module 43 and plane bearing 44.Revolve die 41 and can select the die that revolves of existing riveter, it is used for ball stud is revolved the riveting assembling, the ball seat turn-up portion is divided carry out machining deformation, reaches the effect of ball stud sealing.The axial region that revolves die 41 has axial centre bore 412, and push rod 42 is inserted in the centre bore 412, and its top (lower end) is outer to be exposed at outside the centre bore 412, and its cardinal extremity (upper end) and pressure-bearing module 43 are joined.Pressure-bearing module 43 is elastic module in embodiment as shown in the figure, can directly adopt block rubber.End in contrast to push rod 42 of pressure-bearing module 43 is equipped with plane bearing 44, and plane bearing 44 plays the effect of transmitting axial force on the one hand, cuts off on the one hand transfer of torque.Wholely compoundly revolve the upper end of die 4 and the main shaft of riveter joins, the two can connect by flange, and main shaft contacts with plane bearing 44, plane bearing 44 is played the effect of supporting.Plane bearing 44 can adopt annular spherical guide, but the implication of plane bearing 44 is not limited to the spherical guide of annular, and it refers to transmit axial force but the bearing that can cut off moment of torsion.
Embodiment as shown in the figure compound revolved die when work, drives push rod 42 when axis feeding, when push rod 42 with after the workpiece end cap contact, by main shaft pressure the ball bowl is pressed into ball seat, this moment pressure-bearing module 43 to be that block rubber is existing partly be out of shape.Push rod 42 with ball bowl, end cap dieback after, block rubber continues distortion, push rod 42 positions remain unchanged and main shaft continues to drive roller 410 rotations and walks downward.This moment, plane bearing 44 was that the ball rotation of annular spherical guide makes push rod remain static in order to avoid push rod also to rotate.Finally revolve die and the ball seat turn-up portion is divided carry out machining deformation, finish the ball stud sealing.
In another embodiment of the present invention, the mainshaft mechanism of push rod 42 and riveter can separate and moves, and also can reach purpose of the present invention.Be executing agency at axis hole 412 or push rod 42 inner annex solution pressing systems such as pressure-bearing module 43, the dynamic change of the hydraulic coupling that provides by hydraulic pressure, pressure-bearing module 43 drives push rod 42 axially having certain displacement thereupon.
Car ball stud of the present invention press-fits and revolves the riveting Applying Compound Assembling Technology and can understand in conjunction with embodiment as shown in the figure, at first ball pin and ball bowl, end cap is successively placed in the ball seat, and the decline power source of push rod 42 is exactly the riveter main shaft.The inner flexible member (for example block rubber) 43 that adds of push rod, a pair of annular spherical guide 44 is placed in block rubber 43 upper surfaces.When the riveter main shaft descended, push rod 42 descended and simultaneously with after the end cap of workpiece contacts, block rubber 43 compressive deformations.Along with the continuous increase of slippage, push rod 42 pressure force end cap and ball bowl slowly to be pressed in the ball seat.Main shaft continues to walk downward afterwards, thereby makes push rod 43 complete diebacks owing to the ball bowl kills in ball seat this moment.At block rubber constantly under the effect of distortion, roller 410 divides with the ball seat turn-up portion smoothly and contacts and push rod 42 holding positions are constant.Roller 410 may drive push rod block rubber base and rotate together in rotary course, so add annular spherical guide 44, the ball rotation makes the push rod transfixion, finally realizes the ball stud sealing.
By transforming the existing riveting equipment that revolves, can be by the feeding of main shaft, ball stud is press-fited and these two kinds of process integration to machines of roll riveting are finished continuously, greatly reduce the consumption of the expense of equipment investment and manpower, the energy.
Claims (8)
1. one kind has the compound die that revolves that press-fits function, comprise and revolve die, it is characterized in that, also comprise push rod and pressure-bearing module, revolve die and establish axial center hole, establish this push rod and pressure-bearing module in this axial center hole, expose outside revolving die on the top of push rod, the pressure-bearing module is attached to the cardinal extremity of push rod, and this pressure-bearing module produces axial displacement so that this push rod shrinks in this axial center hole in this axial center hole after bearing pressure.
2. as claimed in claim 1 have a compound die that revolves that press-fits function, it is characterized in that this pressure-bearing module is elastic module, and this axial displacement is the axial elasticity deflection of elastic module.
3. as claimed in claim 1 have a compound die that revolves that press-fits function, it is characterized in that this pressure-bearing module is the executing agency of hydraulic system.
4. as claimed in claim 1 have a compound die that revolves that press-fits function, it is characterized in that the end in contrast to this push rod of this pressure-bearing module is equipped with plane bearing.
5. as claimed in claim 1 have a compound die that revolves that press-fits function, it is characterized in that this plane bearing is spherical guide.
6. a riveter is characterized in that, comprises such as each described compound die that revolves in the claim 1 to 5, described revolving on the main shaft that die is connected to riveter.
7. a car ball stud press-fits and revolves the riveting Applying Compound Assembling Technology, it is characterized in that, riveter revolve anchor head in the middle of add push rod, set elastic module at the cardinal extremity of push rod, place a pair of annular spherical guide in the upper surface of elastic module; At first with ball pin and ball bowl, end cap is successively placed in the ball seat, utilize the riveter main shaft that power source is provided so that push rod descends, when the riveter main shaft descends, push rod descends and simultaneously with after end cap contacts, make the block rubber compressive deformation, continuous increase along with slippage, the pressure of push rod forces end cap and ball bowl slowly to be pressed in the ball seat, the riveter main shaft continues to walk downward afterwards, thereby in ball seat make push rod complete dieback owing to the ball bowl kills this moment, under the effect that elastic module constantly is out of shape, the roller of riveter divides with the ball seat turn-up portion smoothly and contacts and the push rod holding position is constant, the ball rotation of annular spherical guide makes the push rod transfixion, finally realizes the ball stud sealing.
8. car ball stud as claimed in claim 7 press-fits and revolves the riveting Applying Compound Assembling Technology, it is characterized in that described elastic module is block rubber.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210087216.7A CN103357766B (en) | 2012-03-29 | 2012-03-29 | Compound is revolved die, riveter and car ball stud and is press-fited and revolve riveting Applying Compound Assembling Technology |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210087216.7A CN103357766B (en) | 2012-03-29 | 2012-03-29 | Compound is revolved die, riveter and car ball stud and is press-fited and revolve riveting Applying Compound Assembling Technology |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN103357766A true CN103357766A (en) | 2013-10-23 |
| CN103357766B CN103357766B (en) | 2016-01-13 |
Family
ID=49360505
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201210087216.7A Active CN103357766B (en) | 2012-03-29 | 2012-03-29 | Compound is revolved die, riveter and car ball stud and is press-fited and revolve riveting Applying Compound Assembling Technology |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN103357766B (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103706721B (en) * | 2013-12-18 | 2015-12-09 | 上海第二工业大学 | Ball stud riveting device and riveting method |
| CN115647164A (en) * | 2022-10-20 | 2023-01-31 | 重庆铁马工业集团有限公司 | Hydraulic sealing device and method for steering ball head |
| CN115945592A (en) * | 2021-10-09 | 2023-04-11 | 温州瑞立科密汽车电子有限公司 | EBS solenoid valve iron core roll riveting tooling and roll riveting process |
| CN117444580A (en) * | 2023-11-02 | 2024-01-26 | 建新赵氏科技股份有限公司 | A support assembly and its riveting head |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1318307A (en) * | 1969-08-12 | 1973-05-31 | Rau Swf Autozubehoer | Device for mounting a ball pin in a crank |
| US20040165941A1 (en) * | 2003-02-21 | 2004-08-26 | Nippon Thompson Co., Ltd. | Joint |
| CN101607602A (en) * | 2008-06-18 | 2009-12-23 | 上海奇谋能源技术开发有限公司 | A kind of launching power method and device |
| CN201693120U (en) * | 2010-06-14 | 2011-01-05 | 玉环县锐利机械有限公司 | Pincers fixed plate for rotary riveting machine |
| CN201950127U (en) * | 2010-12-21 | 2011-08-31 | 何金魁 | Spin riveting head for hydraulic pressure spin riveting machine |
| CN201950125U (en) * | 2010-12-16 | 2011-08-31 | 何金魁 | Hydraulic revolving-riveting machine |
| CN202048178U (en) * | 2010-07-23 | 2011-11-23 | 中国第一汽车集团公司 | Fixed type single-lever speed changing control lever assembly for truck |
| CN102267051A (en) * | 2011-07-18 | 2011-12-07 | 湖北唯思凌科装备制造有限公司 | Automatic assembling platform for external ball joint assembly of automobile pull rod |
-
2012
- 2012-03-29 CN CN201210087216.7A patent/CN103357766B/en active Active
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1318307A (en) * | 1969-08-12 | 1973-05-31 | Rau Swf Autozubehoer | Device for mounting a ball pin in a crank |
| US20040165941A1 (en) * | 2003-02-21 | 2004-08-26 | Nippon Thompson Co., Ltd. | Joint |
| CN101607602A (en) * | 2008-06-18 | 2009-12-23 | 上海奇谋能源技术开发有限公司 | A kind of launching power method and device |
| CN201693120U (en) * | 2010-06-14 | 2011-01-05 | 玉环县锐利机械有限公司 | Pincers fixed plate for rotary riveting machine |
| CN202048178U (en) * | 2010-07-23 | 2011-11-23 | 中国第一汽车集团公司 | Fixed type single-lever speed changing control lever assembly for truck |
| CN201950125U (en) * | 2010-12-16 | 2011-08-31 | 何金魁 | Hydraulic revolving-riveting machine |
| CN201950127U (en) * | 2010-12-21 | 2011-08-31 | 何金魁 | Spin riveting head for hydraulic pressure spin riveting machine |
| CN102267051A (en) * | 2011-07-18 | 2011-12-07 | 湖北唯思凌科装备制造有限公司 | Automatic assembling platform for external ball joint assembly of automobile pull rod |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103706721B (en) * | 2013-12-18 | 2015-12-09 | 上海第二工业大学 | Ball stud riveting device and riveting method |
| CN115945592A (en) * | 2021-10-09 | 2023-04-11 | 温州瑞立科密汽车电子有限公司 | EBS solenoid valve iron core roll riveting tooling and roll riveting process |
| CN115647164A (en) * | 2022-10-20 | 2023-01-31 | 重庆铁马工业集团有限公司 | Hydraulic sealing device and method for steering ball head |
| CN117444580A (en) * | 2023-11-02 | 2024-01-26 | 建新赵氏科技股份有限公司 | A support assembly and its riveting head |
Also Published As
| Publication number | Publication date |
|---|---|
| CN103357766B (en) | 2016-01-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204035967U (en) | A kind of gear ring pressing machine | |
| CN103357766B (en) | Compound is revolved die, riveter and car ball stud and is press-fited and revolve riveting Applying Compound Assembling Technology | |
| CN101881304B (en) | Assembly structure, method and fixture of pulley and bearing | |
| CN202208113U (en) | Dynamic balance system of high-speed precision press | |
| CN104308198B (en) | A kind of main shaft device for direct-drive type numerical control hobbing knife rest | |
| CN109261842A (en) | Stamping device for production of C-type sealing ring | |
| CN204234820U (en) | Half shaft flange one time boring grab | |
| CN201687920U (en) | Assembly structure for belt wheel and bearing and clamp | |
| CN204381220U (en) | The press-in riveting tool of shifting vehicle gearbox lever | |
| CN206296832U (en) | Motor positioning tool | |
| CN205571131U (en) | Bearing holder punching device | |
| CN201124251Y (en) | Multi-hole drilling transmission mechanism | |
| JP2015224682A (en) | Cross shaft type universal joint assembly method | |
| CN210967751U (en) | Expanded wheel synthesis assembly die | |
| CN204018557U (en) | Limit fixed sleeve riveting set | |
| CN203484895U (en) | Gear ring positioning and press fitting device | |
| CN203281905U (en) | Jig for installing conical roller bearing outer rings of vehicle axle hub | |
| CN107283178A (en) | A kind of wheel two-shot clamping device | |
| CN207255143U (en) | A kind of automobile axle shaft forge die | |
| CN206925582U (en) | A kind of wheel two-shot clamping device | |
| CN104056970A (en) | Limiting and fixing sleeve riveting device | |
| CN203526454U (en) | Servo pressing-riveting device with automatically gyratory riveting head | |
| CN222471411U (en) | Sleeve inner hole bidirectional bearing pressing tool | |
| CN204320989U (en) | The horizontal riveting set of universal joint assembly | |
| CN202910642U (en) | Transferring and positioning device of wheel processing center |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant |