CN102990728A - Highly shearing-resistant container bottom board and manufacturing method thereof - Google Patents
Highly shearing-resistant container bottom board and manufacturing method thereof Download PDFInfo
- Publication number
- CN102990728A CN102990728A CN2012105093713A CN201210509371A CN102990728A CN 102990728 A CN102990728 A CN 102990728A CN 2012105093713 A CN2012105093713 A CN 2012105093713A CN 201210509371 A CN201210509371 A CN 201210509371A CN 102990728 A CN102990728 A CN 102990728A
- Authority
- CN
- China
- Prior art keywords
- veneer
- wooden veneer
- vertical texture
- bottom board
- layer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000010008 shearing Methods 0.000 title claims abstract description 32
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 16
- 239000000463 material Substances 0.000 claims abstract description 12
- 239000003292 glue Substances 0.000 claims description 21
- 235000013339 cereals Nutrition 0.000 claims description 14
- 238000000034 method Methods 0.000 claims description 11
- ISWSIDIOOBJBQZ-UHFFFAOYSA-N phenol group Chemical group C1(=CC=CC=C1)O ISWSIDIOOBJBQZ-UHFFFAOYSA-N 0.000 claims description 9
- 230000032683 aging Effects 0.000 claims description 7
- 238000007731 hot pressing Methods 0.000 claims description 7
- 239000000575 pesticide Substances 0.000 claims description 7
- 230000007547 defect Effects 0.000 claims description 6
- 239000000945 filler Substances 0.000 claims description 6
- 235000013312 flour Nutrition 0.000 claims description 6
- 238000001035 drying Methods 0.000 claims description 5
- 238000007654 immersion Methods 0.000 claims description 2
- 239000004745 nonwoven fabric Substances 0.000 claims description 2
- 238000007598 dipping method Methods 0.000 claims 1
- 239000004744 fabric Substances 0.000 claims 1
- 239000010410 layer Substances 0.000 abstract description 61
- 239000002344 surface layer Substances 0.000 abstract description 2
- -1 phenolic aldehyde Chemical class 0.000 abstract 1
- 241000219502 Casuarina glauca Species 0.000 description 6
- 235000016421 Pinus nigra Nutrition 0.000 description 6
- 244000166124 Eucalyptus globulus Species 0.000 description 5
- 230000006378 damage Effects 0.000 description 5
- 239000007787 solid Substances 0.000 description 4
- 239000002023 wood Substances 0.000 description 4
- 239000011121 hardwood Substances 0.000 description 3
- 239000002932 luster Substances 0.000 description 3
- 235000018185 Betula X alpestris Nutrition 0.000 description 2
- 235000018212 Betula X uliginosa Nutrition 0.000 description 2
- 240000000731 Fagus sylvatica Species 0.000 description 2
- 235000010099 Fagus sylvatica Nutrition 0.000 description 2
- 241001484029 Dipterocarpus grandiflorus Species 0.000 description 1
- 241000238631 Hexapoda Species 0.000 description 1
- 238000004026 adhesive bonding Methods 0.000 description 1
- 230000004888 barrier function Effects 0.000 description 1
- 238000005253 cladding Methods 0.000 description 1
- 239000011162 core material Substances 0.000 description 1
- 230000010354 integration Effects 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
- 239000002994 raw material Substances 0.000 description 1
- 239000011122 softwood Substances 0.000 description 1
- 230000007306 turnover Effects 0.000 description 1
Images


Landscapes
- Laminated Bodies (AREA)
Abstract
The invention discloses a highly shearing-resistant container bottom board with a special structural design, and a manufacturing method thereof. The maximal collapsing force of 254mm short span is more than 9300N. The highly shearing-resistant container bottom board is structured in that the upper and lower layers are made of longitudinal single boards with attractive color and textures; 2-4 layers of longitudinal texture signal boards with high mechanical properties are symmetrically arranged towards the inside; transverse texture single boards and longitudinal texture single boards are paved at intervals towards the inside; and 5-9 layers of longitudinal texture single boards are arranged on the middlemost part; and a layer of phenolic aldehyde impregnated materials is arranged on the outermost layer. The highly shearing-resistant container bottom board has the advantages of high shearing resistance, and attractive surface layer color, material resources are sustainable, and various performance indexes of the highly shearing-resistant container bottom board satisfy the technical requirements of the international container industry.
Description
Technical field
What the present invention relates to is a kind of high shearing resistance container bottom board and manufacture method thereof, with raw material such as Australian pine, Eucalyptus and hardwood, makes container bottom board, belongs to the wood-based plate manufacturing technology field in the timber industry.
Background technology
In the modern logistics container with load and unload fast, turnover, convenient transportation safety and being used by more and more, accelerate along with the process of global economic integration, Container Transport already develops very fast, the demand of container also increases severely with day.The main loaded area of container is wooden base plate, requires its base plate to have higher mechanical property, presentation quality, impact resistance and ageing-resistant performance.For a long time, almost all rely on the thick multiplyplywood that the hard broadleaf clone (Keruing) that grows in the tropical rain forest and A Bidong (Apitong) make and make base plate.Because the growth cycle of such seeds is very long, generally all need more than 50 years, the alternative materials of seeking clone and A Bidong is very urgent, and timber and the quick-growing plantation material through Forest Certification becomes first-selection for this reason.
During existing container bottom board is produced, the crisscross arrangement of the normal employing of intermediate layer Wooden veneer; Or middle three layers of longitudinal arrangement, outwards be again criss-cross arrangement, these arrange to container bottom board stressed large, span is short not too suitable, because container bottom board is under the stressing conditions of short span, the intermediate layer can be subject to larger shearing force, and it also is the reliability of judging accordingly container bottom board that the world rents case association (IICL) 7.26 tons of dolly van tests commonly used.This patent is exactly for this, improves the short span shear strength of container bottom board, guarantees to produce the container bottom board reliable in quality.
Summary of the invention
The purpose of this invention is to provide a kind of high shearing resistance container bottom board and manufacture method.Its objective is that Wooden veneers such as utilizing beech, birch, clone is the table backing layer, the sandwich layer veneer mostly is the quick-growing plantation materials such as Eucalyptus, Australian pine, add the tropical hard wood veneer that a small amount of intensity is high, make the surface layer with color and luster and beautiful texture, and satisfy the base plate of container bottom board performance requirement.
The present invention adopts some color and lusters and beautiful texture and flawless Wooden veneer as surface material, sandwich layer adopts the artificial forest wood that can fell in a large number, adopting middle five layers of Wooden veneer above is full longitudinal arrangement, and the high Australian pine of employing longitudinal shear resistance performance, the shear strength of base plate is improved greatly, and 254mm is short to stride maximal destruction power greater than 9300N.The container bottom board that makes like this has beautiful texture and color and luster, and the shear strength of base plate is higher than traditional clone or A Bidong base plate, can satisfy the permanent needs that use of container bottom board.
Technical solution of the present invention: its structure be from outside to inside up and down symmetry establish: one deck table backing layer is with vertical texture high-quality veneer, inwardly be two-layer vertical texture Wooden veneer (or two-layer vertical texture Wooden veneer, inside again is two-layer vertical texture Wooden veneer); Again inwardly for the cross grain Wooden veneer and vertically the texture Wooden veneer be staggered, middlely be vertical texture Wooden veneer more than five layers.
A kind of manufacture method of high shearing resistance container bottom board, its processing step divides:
A, Wooden veneer sorting and arrangement, Wooden veneer moisture content≤10% is selected without the veneer of joint, zero defect, beautiful texture as the table backing layer, according to the required two-sided phenol glue that is coated with, glue-spread 300~400g/m
2, add 10~15% filler and a small amount of pesticides such as flour in the glue, then 70 ℃ of dry 10min of ageing 40~70min or low temperature;
B, assembly with multiple veneer assembly, are 130~150 ℃ in temperature, and maximum pressure is to carry out hot pressing under the condition of 1.8~2.5MPa, keeps 30~40 minutes, then divides three sections step-downs, steam discharge, release.
Advantage of the present invention: can effectively utilize China and timber all over the world, various softwoods, broadleaf timber such as wildwood and artificial fast-growing woods, these Material claddings are used, through science design and reasonable combination, both can solve tropical hard wood difficulty in short supply in the world wide, can solve again the technical barrier of the high shearing resistance Novel bottom plate of producing to meet the requirement of trans-container industrial technology in enormous quantities.
The present invention as the table backing layer, is composited beautiful texture, flawless high-quality veneer again by the Wooden veneer with fast-growing.All should add pesticide in the used glue, uniformly penetrating is in the layers of material of container bottom board when hot pressing to make it, and base plate has long-acting insect protected performance like this; Core material and surface material are combined into slab, make container bottom board through hot-press gluing again, the property indices such as its intensity, elastic modelling quantity, surface quality and short span are anti-shearing can both meet the specification requirement of trans-container industry fully.
Description of drawings
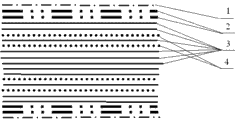
Accompanying drawing 1 is the high shearing resistance container bottom board of the first structural representation.
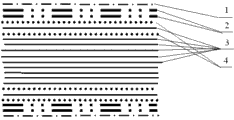
Accompanying drawing 2 is the high shearing resistance container bottom board of the second structural representations.
Accompanying drawing 3 is the third high shearing resistance container bottom board structural representations.
Accompanying drawing 4 is the 4th kind high shearing resistance container bottom board structural representations.
Among the figure: the 1st, the table backing layer needs color and luster and beautiful texture and flawless Wooden veneer with vertical texture high-quality veneer, and assortment can be selected beech, birch and clone etc.; The 2nd, vertical texture Wooden veneer requires mechanical property higher, and assortment can be selected horse traction silk (Malas), or the clone, or Australian pine and Eucalyptus etc.; The 3rd, vertical texture Wooden veneer is Australian pine, or China's artificial forest fast growing wood Eucalyptus; The 4th, cross grain Wooden veneer, available China artificial forest fast growing wood Eucalyptus or Australian pine; The 5th, one deck phenolic impregnated material can be impregnated paper, also can be immersion non-woven fabrics.
The specific embodiment
Embodiment 1:
The structure of high shearing resistance container bottom board such as Fig. 1,
The manufacture method of high shearing resistance container bottom board is as follows:
A, Wooden veneer sorting and arrangement, Wooden veneer moisture content≤9% is selected without the veneer of joint, zero defect, beautiful texture as the table backing layer, according to the required two-sided phenol glue that is coated with, glue-spread 350g/m
2, the flour filler of adding 15% in the glue adds 4.6 pesticide that restrains, then ageing or 70 ℃ of low temperature drying 10min by 1 kilogram of glue (solid content 48%) in the glue simultaneously;
B, assembly, from outside to inside symmetrical each: one deck table backing layer is with vertical texture high-quality veneer 1, two-layer vertical texture Wooden veneer 2, two-layer vertical texture Wooden veneer 3; Be the vertical texture veneers 3 of two-layer cross grain veneer 4 therebetween one decks inwardly again, middle five layers are vertical texture Wooden veneer 3.Then be 140 ℃ in temperature, maximum pressure is to carry out hot pressing under the condition of 2.3MPa, keeps then pressure drop stage, steam discharge, release 38 minutes.
After conventional post-production, can obtain the finished container base plate, its physical and mechanical property is as follows:
MOR∥: ≥ 100 MPa
MOR⊥: ≥ 35 MPa
MOE∥: ≥ 12000 MPa
MOE⊥: ≥ 3500 MPa
The short maximal destruction power of striding of 254mm: 〉=9300 N
Density: 0.70~0.85 g/cm
3
The structure of high shearing resistance container bottom board such as Fig. 2,
The manufacture method of high shearing resistance container bottom board is as follows:
A, Wooden veneer sorting and arrangement, Wooden veneer moisture content≤9% is selected without the veneer of joint, zero defect, beautiful texture as the table backing layer, according to the required two-sided phenol glue that is coated with, glue-spread 350g/m
2, the flour filler of adding 15% in the glue adds 4.6 pesticides that restrain, ageing or 70 ℃ of low temperature drying 10min by 1 kilogram of glue (solid content 48%) in the glue;
B, assembly, from outside to inside symmetrical each: one deck table backing layer is with vertical texture high-quality veneer 1, two-layer vertical texture Wooden veneer 2; Inwardly be three layers of cross grain veneer 4 and two-layer vertical texture veneer 3 alternate layings again, middle five layers are vertical texture Wooden veneer 3.Then be 140 ℃ in temperature, maximum pressure is to carry out hot pressing under the condition of 2.5MPa, keeps then pressure drop stage, steam discharge, release 38 minutes.
After conventional post-production, can obtain the finished container base plate, its physical and mechanical property is as follows:
MOR∥: ≥ 95 MPa
MOR⊥: ≥ 35 MPa
MOE∥: ≥ 10500 MPa
MOE⊥: ≥ 3500 MPa
The short maximal destruction power of striding of 254mm: 〉=9300 N
Density: 0.70~0.85 g/cm
3
The structure of high shearing resistance container bottom board such as Fig. 3,
The manufacture method of high shearing resistance container bottom board is as follows:
A, Wooden veneer sorting and arrangement, Wooden veneer moisture content≤10% is selected without the veneer of joint, zero defect, beautiful texture as the table backing layer, according to the required two-sided phenol glue that is coated with, glue-spread 380g/m
2, the flour filler of adding 15% in the glue adds 4.6 pesticide that restrains, then ageing or 70 ℃ of low temperature drying 10min by 1 kilogram of glue (solid content 48%) in the glue;
B, assembly, respectively symmetrical from outside to inside: one deck hard paper 5, one deck table backing layer is the vertical texture veneers 3 of two-layer cross grain veneer 4 therebetween one decks inwardly with vertical texture high-quality veneer 1, two-layer vertical texture Wooden veneer 2 again, and middle seven layers are vertical texture Wooden veneer 3.Then be 140 ℃ in temperature, maximum pressure is to carry out hot pressing under the condition of 2.1MPa, keeps then pressure drop stage, steam discharge, release 36 minutes;
After conventional post-production, can obtain the finished container base plate, its physical and mechanical property is as follows:
MOR∥: ≥ 90 MPa
MOR⊥: ≥ 35 MPa
MOE∥: ≥ 10000 MPa
MOE⊥: ≥ 3500 MPa
The short maximal destruction power of striding of 254mm: 〉=9300 N
Density: 0.70~0.85 g/cm
3
The structure of high shearing resistance container bottom board such as Fig. 4,
The manufacture method of high shearing resistance container bottom board is as follows:
A, Wooden veneer sorting and arrangement, Wooden veneer moisture content≤10% is selected without the veneer of joint, zero defect, beautiful texture as the table backing layer, according to the required two-sided phenol glue that is coated with, glue-spread 400g/m
2, the flour filler of adding 15% in the glue adds 4.6 pesticide that restrains, then ageing or 70 ℃ of low temperature drying 10min by 1 kilogram of glue (solid content 48%) in the glue;
B, assembly, respectively symmetrical from outside to inside: one deck table backing layer is the vertical texture veneers 3 of two-layer cross grain veneer 4 therebetween one decks inwardly with vertical texture high-quality veneer 1, two-layer vertical texture Wooden veneer 2 again, and middle nine layers are vertical texture Wooden veneer 3.Then be 140 ℃ in temperature, maximum pressure is to carry out hot pressing under the condition of 2.4MPa, keeps then pressure drop stage, steam discharge, release 39 minutes;
After conventional post-production, can obtain the finished container base plate, its physical and mechanical property is as follows:
MOR∥: ≥ 95 MPa
MOR⊥: ≥ 35 MPa
MOE∥: ≥ 10000 MPa
MOE⊥: ≥ 3500 MPa
The short maximal destruction power of striding of 254mm: 〉=9300 N
Density: 0.70~0.85 g/cm
3
Claims (7)
1. one kind high shearing resistance container bottom board is characterized in that from outside to inside symmetry is established up and down: one deck table backing layer is with vertical texture high-quality veneer, two-layer vertical texture Wooden veneer, two-layer vertical texture Wooden veneer; Be the vertical texture Wooden veneer of therebetween one deck of two-layer cross grain Wooden veneer inwardly again, middle five layers are vertical texture Wooden veneer.
2. a kind of high shearing resistance container bottom board according to claim 1 is characterized in that from outside to inside to being called: one deck table backing layer is with vertical texture high-quality veneer, two-layer vertical texture Wooden veneer; Inwardly be three layers of cross grain Wooden veneer and the alternate laying of two-layer vertical texture Wooden veneer again, middle five layers are vertical texture Wooden veneer.
3. a kind of high shearing resistance container bottom board according to claim 1, it is characterized in that from outside to inside to being called: one deck table backing layer is with vertical texture high-quality veneer, two-layer vertical texture Wooden veneer, be the vertical texture Wooden veneer of therebetween one deck of two-layer cross grain Wooden veneer inwardly again, middle seven layers are vertical texture Wooden veneer.
4. a kind of high shearing resistance container bottom board according to claim 1, it is characterized in that from outside to inside to being called: one deck table backing layer is with vertical texture high-quality veneer, two-layer vertical texture Wooden veneer, be the vertical texture Wooden veneer of two-layer cross grain Wooden veneer therebetween one deck inwardly again, middle nine layers are vertical texture Wooden veneer.
5. a kind of high shearing resistance container bottom board according to claim 1, middle at least five layers are vertical texture Wooden veneer.
6. a kind of high shearing resistance container bottom board according to claim 1 is characterized in that adopting one deck phenolic impregnated material at outermost layer, and this phenolic impregnated material is impregnated paper, or immersion non-woven fabrics, or the dipping glass-fiber-fabric.
7. the manufacture method of a high shearing resistance container bottom board is characterized in that the method comprises following processing step:
A, Wooden veneer sorting and arrangement, Wooden veneer moisture content≤10% is selected without the veneer of joint, zero defect, beautiful texture as the table backing layer, according to the required two-sided phenol glue that is coated with, glue-spread 300~400g/m
2, add flour filler and a small amount of pesticide, then ageing 40~70min or 70 ℃ of low temperature drying 10min of 10~15% in the glue;
B, assembly with multiple veneer assembly, are 130~150 ℃ in temperature, and maximum pressure is to carry out hot pressing under the condition of 1.8~2.5MPa, keeps 30~40 minutes, then divides three sections step-downs, steam discharge, release.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012105093713A CN102990728A (en) | 2012-12-04 | 2012-12-04 | Highly shearing-resistant container bottom board and manufacturing method thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012105093713A CN102990728A (en) | 2012-12-04 | 2012-12-04 | Highly shearing-resistant container bottom board and manufacturing method thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN102990728A true CN102990728A (en) | 2013-03-27 |
Family
ID=47920101
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012105093713A Pending CN102990728A (en) | 2012-12-04 | 2012-12-04 | Highly shearing-resistant container bottom board and manufacturing method thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102990728A (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104669370A (en) * | 2013-11-27 | 2015-06-03 | 上海杰事杰新材料(集团)股份有限公司 | Reinforced container bottom plate and manufacturing method thereof |
| CN104802231A (en) * | 2014-01-27 | 2015-07-29 | 上海杰事杰新材料(集团)股份有限公司 | Reinforced container soleplate and preparation method thereof |
| CN104802235A (en) * | 2014-01-27 | 2015-07-29 | 上海杰事杰新材料(集团)股份有限公司 | Composite board, preparation method and application thereof |
| CN105014753A (en) * | 2015-07-14 | 2015-11-04 | 王伟宏 | Fast-growing wood flame-retardant laminated plate and production method thereof |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH08197507A (en) * | 1994-08-18 | 1996-08-06 | Qingdao Jinyuan Co | Strong bamboo plywood and manufacturing method thereof |
| CN2663356Y (en) * | 2003-07-25 | 2004-12-15 | 中国国际海运集装箱(集团)股份有限公司 | Container floor |
| CN201361916Y (en) * | 2009-03-12 | 2009-12-16 | 嘉善新华昌木业有限公司 | Plywood used for container flooring |
| CN101712167A (en) * | 2008-10-08 | 2010-05-26 | 胜狮货柜技术研发(上海)有限公司 | Composite bottom board for container |
| CN101948037A (en) * | 2010-09-02 | 2011-01-19 | 佛山市顺德区东顺木业有限公司 | Wood-bamboo composite container bottom plate produced by adopting hot-in and hot-out process and producing method thereof |
| CN202192652U (en) * | 2011-07-18 | 2012-04-18 | 佛山市顺德区东顺木业有限公司 | A non-cloning panel container floor |
-
2012
- 2012-12-04 CN CN2012105093713A patent/CN102990728A/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH08197507A (en) * | 1994-08-18 | 1996-08-06 | Qingdao Jinyuan Co | Strong bamboo plywood and manufacturing method thereof |
| CN2663356Y (en) * | 2003-07-25 | 2004-12-15 | 中国国际海运集装箱(集团)股份有限公司 | Container floor |
| CN101712167A (en) * | 2008-10-08 | 2010-05-26 | 胜狮货柜技术研发(上海)有限公司 | Composite bottom board for container |
| CN201361916Y (en) * | 2009-03-12 | 2009-12-16 | 嘉善新华昌木业有限公司 | Plywood used for container flooring |
| CN101948037A (en) * | 2010-09-02 | 2011-01-19 | 佛山市顺德区东顺木业有限公司 | Wood-bamboo composite container bottom plate produced by adopting hot-in and hot-out process and producing method thereof |
| CN202192652U (en) * | 2011-07-18 | 2012-04-18 | 佛山市顺德区东顺木业有限公司 | A non-cloning panel container floor |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104669370A (en) * | 2013-11-27 | 2015-06-03 | 上海杰事杰新材料(集团)股份有限公司 | Reinforced container bottom plate and manufacturing method thereof |
| CN104802231A (en) * | 2014-01-27 | 2015-07-29 | 上海杰事杰新材料(集团)股份有限公司 | Reinforced container soleplate and preparation method thereof |
| CN104802235A (en) * | 2014-01-27 | 2015-07-29 | 上海杰事杰新材料(集团)股份有限公司 | Composite board, preparation method and application thereof |
| CN104802235B (en) * | 2014-01-27 | 2017-09-15 | 上海杰事杰新材料(集团)股份有限公司 | A kind of composite board, preparation method and applications |
| CN105014753A (en) * | 2015-07-14 | 2015-11-04 | 王伟宏 | Fast-growing wood flame-retardant laminated plate and production method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN100999086B (en) | Internally reinforced bamboo-wood composite container bottom plate and manufacturing method thereof | |
| CN100491086C (en) | Composite container floor with particleboard for structure as core material and manufacturing method thereof | |
| CN101012701A (en) | Four-layer solid wood composite floor with skin layer having horizontal-longitudinal split joint structure and method for making same | |
| CN102717408B (en) | Bamboo and wood composite container bottom plate manufactured by one-step hot pressing and having high elastic modulus and manufacture method thereof | |
| CN104191471A (en) | High-strength poplar laminated veneer lumber and manufacturing method thereof | |
| CN102717409A (en) | Bamboo-wood composite board with high-strength bamboo plywood coated on the surface and manufacturing method thereof | |
| CN101549505A (en) | Veneer for container base plate | |
| CN203156875U (en) | Plywood for container soleplate | |
| CN102773887B (en) | Recombined bamboo wood and oriented strand board composite structural board and manufacturing method thereof | |
| CN203110061U (en) | Highly shearing-resistant container bottom board | |
| CN102398396B (en) | Bamboo-wood composite container base plate with improved bamboo curtain splint surface layers, and manufacturing method thereof | |
| CN203266833U (en) | OSB high-strength composite wood veneer | |
| CN202106432U (en) | Bamboo-wood composite board | |
| CN201914627U (en) | Wood-bamboo-composite container bottom board adopting hot-in hot-out process | |
| CN102581890A (en) | Method for manufacturing bamboo and wood composite container bottom plate by using rolled sympodial bamboo as raw material | |
| CN104128971B (en) | Bottom plate for bamboo-wood composite container and production method thereof | |
| CN102528858A (en) | Plywood for composite bamboo and wood container flooring | |
| CN203198012U (en) | Plywood for shipbuilding | |
| CN201511420U (en) | Bamboo wood composite board | |
| CN202192652U (en) | A non-cloning panel container floor | |
| CN202556510U (en) | Bamboo and wood composite plywood used in container bottom plate | |
| CN102581892A (en) | Method for manufacturing bamboo and wood composite container bottom plate by using thick bamboo curtain substrate as core | |
| CN211686632U (en) | Bamboo-wood laminated container bottom plate | |
| CN202640503U (en) | Bamboo-wood composite plate with high-intensity bamboo plywood coated on surface | |
| CN202572540U (en) | Automobile platform floor |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C12 | Rejection of a patent application after its publication | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20130327 |