CN102983445A - Seamless metal shell of data transmission interface and production method of same - Google Patents

Seamless metal shell of data transmission interface and production method of same Download PDF

Info

Publication number
CN102983445A
CN102983445A CN2012105152887A CN201210515288A CN102983445A CN 102983445 A CN102983445 A CN 102983445A CN 2012105152887 A CN2012105152887 A CN 2012105152887A CN 201210515288 A CN201210515288 A CN 201210515288A CN 102983445 A CN102983445 A CN 102983445A
Authority
CN
China
Prior art keywords
metal shell
data transmission
transmission interface
seamless metal
tubing
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Granted
Application number
CN2012105152887A
Other languages
Chinese (zh)
Other versions
CN102983445B (en
Inventor
谢二文
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
Nanchang Liqi Machinery Manufacturing Co.,Ltd.
Original Assignee
FOSHAN DEXINGYE METAL TECHNOLOGY CO LTD
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by FOSHAN DEXINGYE METAL TECHNOLOGY CO LTD filed Critical FOSHAN DEXINGYE METAL TECHNOLOGY CO LTD
Priority to CN201210515288.7A priority Critical patent/CN102983445B/en
Publication of CN102983445A publication Critical patent/CN102983445A/en
Application granted granted Critical
Publication of CN102983445B publication Critical patent/CN102983445B/en
Active legal-status Critical Current
Anticipated expiration legal-status Critical

Links

Images

Landscapes

  • Metal Extraction Processes (AREA)
  • Bending Of Plates, Rods, And Pipes (AREA)
  • Shaping Metal By Deep-Drawing, Or The Like (AREA)

Abstract

The invention discloses a seamless metal shell of a data transmission interface and a production method of the seamless metal shell, wherein the metal pipe of the seamless metal shell is formed by cold deformation, and the seamless metal shell is not provided with a connecting seam which is arranged on the metal shell of a present data transmission interface. The production method for the seamless metal shell of the data transmission interface, provided by the invention, can be applied to production of different shapes of seamless metal shells of the data transmission interface, has simple production procedures, is high in production efficiency, does not cause leftover bits and pieces, and facilitates conservation of raw materials. The seamless metal shell of the data transmission interface, which is produced with the production method, does not have a connecting seam, has a beautiful appearance, and is integrally arranged; and the mechanical properties are greatly improved.

Description

A kind of seamless metal shell and production method thereof of data transmission interface
Technical field
The present invention relates to a kind of data transmission interface, in particular a kind of seamless metal shell and production method thereof of data transmission interface.
Background technology
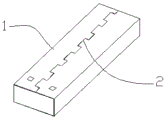
The metal shell of existing data transmission interface all is to produce the required form structure by the mode of bending-riveted, shown in the structural representation of Fig. 1 available data coffret metal shell, there is a connecting sewing 2 on the metal shell 1 of existing data transmission interface.Shown in the expansion schematic diagram of Fig. 2 available data coffret metal shell, metal shell 1 is metallic plate 3 after connecting sewing 2 launches, be provided with link slot 4 and connecting portion 5 on the metallic plate 3, metal shell 1 among Fig. 1 is namely formed by metallic plate 3 bendings, and connecting sewing 2 is namely formed by link slot 4 and connecting portion 5 riveteds.There is following technical problem in the metal shell of this structure of available data coffret: one, production efficient is low, scrappage is high.Because the making of each metal shell needs sheet metal is processed into first shape shown in Figure 2, again its bending-riveted is become structure shown in Figure 1.So that the production process of existing metal shell is very complicated, and the required precision of bending-riveted course of processing is very high, is very easy to produce substandard products, thereby causes the production efficiency of existing this metal shell to be difficult to improve, and the scrappage of product is also very high.Two, waste of raw materials is serious in the process of producing product.From original material, cut out the sheet metal shown in Fig. 2, can cause the waste of a large amount of leftover pieces, be unfavorable for the saving of production cost.Three, the product mechanics effect is poor.Because the existence of connecting sewing so that existing metal shell is not to be wholely set, when product is subject to clashing into, the problems such as bending, distortion occur easily at the connecting sewing place in transportation, use procedure.
Therefore, prior art has yet to be improved and developed.
Summary of the invention
The object of the present invention is to provide a kind of seamless metal shell and production method thereof of data transmission interface, the technical problem that exists with the metal shell that solves above-mentioned available data coffret.
Technical scheme of the present invention is as follows:
A kind of seamless metal shell of data transmission interface, wherein, described seamless metal outer cover metal tubing is made through cold deformation is one-body molded.
The seamless metal shell of described data transmission interface, wherein, that the cross section of described seamless metal shell can be set to is square, circular, stairstepping or U-shaped.
A kind of production method of seamless metal shell of data transmission interface wherein, specifically may further comprise the steps:
S1, planar metal sheet material is welded into tubing for the seamless metal shell of making data transmission interface;
S2, removing are for the projection on the inside and outside weld seam of tubing of the seamless metal shell of making data transmission interface;
S3, utilize pipe mold that the tubing of seamless metal shell that be used for to make data transmission interface is carried out cold deformation processing, obtain the high accuracy tubing with required metal shell cross sectional shape, consistent size;
S4, by the length of required metal shell, the tubing of high-precision seamless metal shell for making data transmission interface is cut;
The production method of the seamless metal shell of described data transmission interface, wherein, described seamless metal shell is that the cross section is circular, described pipe mold is the circular pipe mould.
The production method of the seamless metal shell of described data transmission interface, wherein, described seamless metal shell is that the cross section is square, described pipe mold is the square pipe mould.
The production method of the seamless metal shell of described data transmission interface, wherein, described seamless metal shell is that the cross section is stairstepping, described pipe mold is the stairstepping pipe mold.
The production method of the seamless metal shell of described data transmission interface is characterized in that, described seamless metal shell is that the cross section is U-shaped, and described pipe mold is the U-shaped pipe mold.
The production method of the seamless metal shell of described data transmission interface, wherein, described step S3 specifically may further comprise the steps:
A: the cross sectional shape according to required metal shell carries out preliminary stretcher strain to the tubing for the seamless metal shell of making data transmission interface;
B: the shape of corresponding required metal shell, utilize plane mould that the tubing for the seamless metal shell of making data transmission interface is carried out the face shaping;
C: the shape of corresponding required metal shell, utilize angle mold that the tubing for the seamless metal shell of making data transmission interface is carried out the angle shaping.
Beneficial effect of the present invention: the invention provides a kind of seamless metal shell and production method thereof of data transmission interface, this production method can be applied to the production of seamless metal shell of the various shapes of data transmission interface.Its production process is simple, and production efficiency is high, but also can not produce leftover pieces, is conducive to raw-material saving.Utilize the seamless metal shell of the next data transmission interface of the method production department, no longer include the existence of connecting sewing, good looking appearance, and be wholely set, mechanical property also is improved greatly.
Description of drawings
Fig. 1 is the structural representation of available data coffret metal shell.
Fig. 2 is the expansion schematic diagram of available data coffret metal shell.
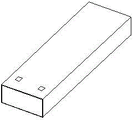
Fig. 3 is the structural representation of the square seamless metal shell of data transmission interface among the present invention.
Fig. 4 is the structural representation of the circular seamless metal shell of data transmission interface among the present invention.
Fig. 5 is the structural representation of the ladder seamless metal shell of data transmission interface among the present invention.
Fig. 6 is the structural representation of the U-shaped seamless metal shell of data transmission interface among the present invention.
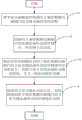
Fig. 7 is the square seamless metal shell production method flow chart of data transmission interface among the present invention.
Fig. 8 is the particular flow sheet of tubing cooling strain in the square seamless metal shell production method of data transmission interface among the present invention.
Fig. 9 is the circular seamless metal shell production method flow chart of data transmission interface among the present invention.
Figure 10 is the ladder seamless metal shell production method flow chart of data transmission interface among the present invention.
Figure 11 is the U-shaped seamless metal shell production method flow chart of data transmission interface among the present invention.
Embodiment
For making purpose of the present invention, technical scheme and advantage clearer, clear and definite, developing simultaneously referring to accompanying drawing, the present invention is described in more detail for embodiment.
Embodiment one, the invention provides a kind of seamless metal shell of data transmission interface.The structural representation of data transmission interface seamless metal shell among the present invention as shown in Figure 3.There is not the connecting sewing 2 on the metal shell 1 of the existing data transmission interface shown in Fig. 1 on the seamless metal shell of data transmission interface provided by the invention.Seamless metal shell provided by the invention is integrated setting, directly is made through cold deformation by metal pipe material.The cross section of the seamless metal shell shown in Fig. 3 is square, and such as Fig. 4, Fig. 5 and shown in Figure 6, in fact the seamless metal shell of data transmission interface provided by the invention can also be arranged to the cross section and be the various shapes such as circle, ladder, U-shaped.
Embodiment two, and the present invention also provides a kind of production method of square seamless metal shell of data transmission interface.Shown in the square seamless metal shell of data transmission interface production method flow chart among Fig. 7 the present invention, this production method comprises the steps: beginning; S1, planar metal sheet material is welded into tubing for the seamless metal shell of making data transmission interface; S2, removing are for the projection on the inside and outside weld seam of tubing of the seamless metal shell of making data transmission interface; S3, utilize the square pipe mould that the tubing of seamless metal shell that be used for to make data transmission interface is carried out cold deformation processing, obtain the high accuracy tubing with required square metal shell cross sectional shape, consistent size; Described direction tubing is that the cross section is square tubing; S4, by the length of required square metal shell, the tubing of high-precision square seamless metal shell for making data transmission interface is cut; The length of required square metal shell can specifically arrange according to different application needs; Finish.After cutting is finished, also can carry out following process to described square metal shell, following process mainly is for the seamless metal shell being applied to needed other making processing on the transfer of data holder, for example, at described metal shell Ka Tai etc. being set.
Shown in the particular flow sheet of tubing cooling strain in the square seamless metal shell production method of data transmission interface among Fig. 8 the present invention, above-mentioned steps 4 specifically may further comprise the steps well: beginning; A: the cross sectional shape according to required square metal shell carries out preliminary stretcher strain to the tubing for the square seamless metal shell of making data transmission interface, obtains the blank of required tubing through preliminary stretcher strain; B: the shape of corresponding required square metal shell, utilize plane mould that the tubing for the seamless metal shell of making data transmission interface is carried out the face shaping; C: the shape of corresponding required square metal shell, utilize angle mold that the tubing for the seamless metal shell of making data transmission interface is carried out the angle shaping; Finish.
Embodiment three, and the present invention also provides a kind of production method of circular seamless metal shell of data transmission interface.Shown in the circular seamless metal shell production method flow chart of data transmission interface among Fig. 9 the present invention, this production method may further comprise the steps: beginning; A, planar metal sheet material is welded into tubing for the seamless metal shell of making data transmission interface; B, removing are for the projection on the inside and outside weld seam of tubing of the seamless metal shell of making data transmission interface; C, utilize the pipe mould that the tubing of seamless metal shell that be used for to make data transmission interface is carried out cold deformation processing, obtain the high accuracy tubing with required circular metal shell cross sectional shape, consistent size, described pipe is that the cross section is circular tubing; D, by the length of required circular metal shell, the tubing of high-precision seamless metal shell for making data transmission interface is cut, the length of required circular metal shell can be according to different application needs and concrete the setting; Finish.In the present embodiment, there are not concrete steps such as the step 3 among the embodiment two among the step c.
Embodiment four, and the present invention also provides a kind of production method of ladder seamless metal shell of data transmission interface.Shown in the ladder seamless metal shell production method flow chart of data transmission interface among Figure 10 the present invention, this production method may further comprise the steps: beginning; 1., planar metal sheet material is welded into tubing for the seamless metal shell of making data transmission interface; 2., remove for the projection on the inside and outside weld seam of tubing of the seamless metal shell of making data transmission interface; 3., utilize the ladder pipe mold that the tubing for the seamless metal shell of making data transmission interface is carried out cold deformation processing, obtain the high accuracy tubing with required ladder metal shell cross sectional shape, consistent size, described ladder pipe is that the cross section is step-like tubing; 4., by the length of required ladder metal shell, the tubing of high-precision seamless metal shell for making data transmission interface is cut, the length of required ladder metal shell can be according to different application needs and concrete the setting; Finish.In the present embodiment, step concrete steps and the concrete steps of the step S3 among the embodiment two 3. are unanimous on the whole, be the mould that adopts for making the mould of ladder tubing, no longer repeat herein.
Embodiment five, and the present invention also provides a kind of production method of U-shaped seamless metal shell of data transmission interface.Shown in the U-shaped seamless metal shell production method flow chart of data transmission interface among Figure 11 the present invention, this production method may further comprise the steps: beginning; (1), planar metal sheet material is welded into tubing for the seamless metal shell of making data transmission interface; (2), remove for the projection on the inside and outside weld seam of tubing of the seamless metal shell of making data transmission interface; (3), utilize the U-shaped pipe mold that the tubing for the seamless metal shell of making data transmission interface is carried out cold deformation processing, obtain the high accuracy tubing with required U-shaped metal shell cross sectional shape, consistent size, described ladder pipe is that the cross section is step-like tubing; (4), by the length of required U-shaped metal shell, the tubing of high-precision seamless metal shell for making data transmission interface is cut, the length of required ladder metal shell can be according to different application needs and concrete the setting; Finish.In the present embodiment, the concrete steps of step (3) and the concrete steps of the step S3 among the embodiment two are unanimous on the whole, be the mould that adopts for making the mould of U-shaped tubing, no longer repeat herein.
Can find out that from above-described embodiment the production method of the seamless metal shell of data transmission interface provided by the invention can be applied to the production of seamless metal shell of the various shapes of data transmission interface.Its production process is simple, and production efficiency is high, but also can not produce leftover pieces, is conducive to raw-material saving.Utilize the seamless metal shell of the next data transmission interface of the method production department, no longer include the existence of connecting sewing, good looking appearance, and be wholely set, mechanical property also is improved greatly.
Should be understood that application of the present invention is not limited to above-mentioned giving an example, for those of ordinary skills, can be improved according to the above description or conversion that all these improvement and conversion all should belong to the protection range of claims of the present invention.

Claims (8)

1. the seamless metal shell of a data transmission interface is characterized in that, described seamless metal outer cover metal tubing is made through cold deformation is one-body molded.
2. the seamless metal shell of data transmission interface according to claim 1 is characterized in that, that the cross section of described seamless metal shell can be set to is square, circular, stairstepping or U-shaped.
3. the production method of the seamless metal shell of a data transmission interface is characterized in that, specifically may further comprise the steps:
S1, planar metal sheet material is welded into tubing for the seamless metal shell of making data transmission interface;
S2, removing are for the projection on the inside and outside weld seam of tubing of the seamless metal shell of making data transmission interface;
S3, utilize pipe mold that the tubing of seamless metal shell that be used for to make data transmission interface is carried out cold deformation processing, obtain the high accuracy tubing with required metal shell cross sectional shape, consistent size;
S4, by the length of required metal shell, the tubing of high-precision seamless metal shell for making data transmission interface is cut.
4. the production method of the seamless metal shell of data transmission interface according to claim 3 is characterized in that, described seamless metal shell is that the cross section is circular, and described pipe mold is the circular pipe mould.
5. the production method of the seamless metal shell of data transmission interface according to claim 3 is characterized in that, described seamless metal shell is that the cross section is square, and described pipe mold is the square pipe mould.
6. the production method of the seamless metal shell of data transmission interface according to claim 3 is characterized in that, described seamless metal shell is that the cross section is stairstepping, and described pipe mold is the stairstepping pipe mold.
7. the production method of the seamless metal shell of data transmission interface according to claim 3 is characterized in that, described seamless metal shell is that the cross section is U-shaped, and described pipe mold is the U-shaped pipe mold.
8. according to claim 5, the production method of the seamless metal shell of 6 or 7 described data transmission interfaces, it is characterized in that described step S3 specifically may further comprise the steps:
A: the cross sectional shape according to required metal shell carries out preliminary stretcher strain to the tubing for the seamless metal shell of making data transmission interface;
B: the shape of corresponding required metal shell, utilize plane mould that the tubing for the seamless metal shell of making data transmission interface is carried out the face shaping;
C: the shape of corresponding required metal shell, utilize angle mold that the tubing for the seamless metal shell of making data transmission interface is carried out the angle shaping.
CN201210515288.7A 2012-12-05 2012-12-05 Seamless metal shell of data transmission interface and production method of same Active CN102983445B (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN201210515288.7A CN102983445B (en) 2012-12-05 2012-12-05 Seamless metal shell of data transmission interface and production method of same

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN201210515288.7A CN102983445B (en) 2012-12-05 2012-12-05 Seamless metal shell of data transmission interface and production method of same

Publications (2)

Publication Number Publication Date
CN102983445A true CN102983445A (en) 2013-03-20
CN102983445B CN102983445B (en) 2015-07-01

Family

ID=47857275

Family Applications (1)

Application Number Title Priority Date Filing Date
CN201210515288.7A Active CN102983445B (en) 2012-12-05 2012-12-05 Seamless metal shell of data transmission interface and production method of same

Country Status (1)

Country Link
CN (1) CN102983445B (en)

Cited By (5)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN104577637A (en) * 2015-01-08 2015-04-29 番禺得意精密电子工业有限公司 Manufacturing method for metal shell and electric coupler thereof
WO2016037341A1 (en) * 2014-09-11 2016-03-17 深圳市大富精工有限公司 Data interface metal housing, machining method thereof and machining device
CN106099616A (en) * 2016-07-07 2016-11-09 东莞市博艾德通信器材有限公司 A kind of USB TYPE C metal shell processing method
CN106329292A (en) * 2016-10-28 2017-01-11 李良浩 Method for preparing metal enclosure of seamless USB connector
WO2018023211A1 (en) * 2016-07-30 2018-02-08 东莞市博艾德通信器材有限公司 Processing method for usb type-c metal housing

Citations (5)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN2634734Y (en) * 2003-02-10 2004-08-18 恒享实业有限公司 The structure of the universal serial bus plug housing and the memory card housing are integrally formed
CN201489816U (en) * 2009-08-18 2010-05-26 合谥螺丝五金股份有限公司 Retractable USB flash drive
CN201515050U (en) * 2009-10-13 2010-06-23 陈伟镇 USB equipment
US20110299246A1 (en) * 2009-02-23 2011-12-08 Weidmueller Interface Gmbh & Co., Kg Modular electronics housing
CN202076535U (en) * 2011-05-03 2011-12-14 东莞宇球电子有限公司 Metal shell of connector

Patent Citations (5)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN2634734Y (en) * 2003-02-10 2004-08-18 恒享实业有限公司 The structure of the universal serial bus plug housing and the memory card housing are integrally formed
US20110299246A1 (en) * 2009-02-23 2011-12-08 Weidmueller Interface Gmbh & Co., Kg Modular electronics housing
CN201489816U (en) * 2009-08-18 2010-05-26 合谥螺丝五金股份有限公司 Retractable USB flash drive
CN201515050U (en) * 2009-10-13 2010-06-23 陈伟镇 USB equipment
CN202076535U (en) * 2011-05-03 2011-12-14 东莞宇球电子有限公司 Metal shell of connector

Cited By (10)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
WO2016037341A1 (en) * 2014-09-11 2016-03-17 深圳市大富精工有限公司 Data interface metal housing, machining method thereof and machining device
CN106716731A (en) * 2014-09-11 2017-05-24 深圳市大富精工有限公司 Data interface metal housing, machining method thereof and machining device
CN106716731B (en) * 2014-09-11 2019-08-13 深圳市大富精工有限公司 Metal shell for data interface, its processing method and processing equipment
CN104577637A (en) * 2015-01-08 2015-04-29 番禺得意精密电子工业有限公司 Manufacturing method for metal shell and electric coupler thereof
CN104577637B (en) * 2015-01-08 2017-05-10 番禺得意精密电子工业有限公司 Manufacturing method for electric coupler
CN106099616A (en) * 2016-07-07 2016-11-09 东莞市博艾德通信器材有限公司 A kind of USB TYPE C metal shell processing method
CN106099616B (en) * 2016-07-07 2018-09-11 东莞市博艾德通信器材有限公司 A kind of USB TYPE C metal shell processing methods
WO2018023211A1 (en) * 2016-07-30 2018-02-08 东莞市博艾德通信器材有限公司 Processing method for usb type-c metal housing
CN106329292A (en) * 2016-10-28 2017-01-11 李良浩 Method for preparing metal enclosure of seamless USB connector
CN106329292B (en) * 2016-10-28 2018-09-11 广州市康超信息科技有限公司 A kind of preparation method of the metal shell of gapless USB connector

Also Published As

Publication number Publication date
CN102983445B (en) 2015-07-01

Similar Documents

Publication Publication Date Title
CN102983445B (en) Seamless metal shell of data transmission interface and production method of same
CN102430642A (en) Progressive die forming process of high-temperature alloy sheet metal part with high flanging hole
CN204093928U (en) One-time formed circle_curling die tool
CN103521674A (en) Method for manufacturing box shell of large special-shaped low-pressure turbine used for aircraft engine
CN108326226B (en) Cold heading process and cold heading module for forming adjusting screw
CN107774796A (en) The stretch forming process of copper alloy shock-absorbing sleeve
CN103350136A (en) Method using standard die to processing any circular arc
CN101823106A (en) Manufacturing method of metal frame for flat panel display
CN203470672U (en) Split-type oil drill pipe joint forming die
CN103350323B (en) The manufacture method of torsional deformation metal finishing band
CN102179680A (en) Method for manufacturing sole mold
CN103394547B (en) A kind of bend forming method
CN202447531U (en) Drawing mold
CN103128174A (en) Assembly die for cold stamping and forming of auto-body panels and design method of assembly die
CN103552151B (en) Concrete reinforced pipe high accuracy punching block and preparation method thereof
CN104525807A (en) Method for forming corners of frame forging piece
CN105184009B (en) A kind of computational methods of large size Z-shaped section crimp frame rib hydroforming rebound
CN204087691U (en) A kind of date of manufacture and production batch mark template
CN202539244U (en) Cold extrusion pipe bending die
CN202683775U (en) Bending die for laminated spring plates of switches
CN202667304U (en) Metal bend extrusion forming device
CN103042215B (en) Combination method of tool for compacting of magnetic materials
CN106392482A (en) Method for manufacturing simple tool
CN202037549U (en) Sand spraying fixture adopting crystal face glue
CN203494970U (en) Structure of dual-boss pipe end molding and clamping die

Legal Events

Date Code Title Description
C06 Publication
PB01 Publication
C10 Entry into substantive examination
SE01 Entry into force of request for substantive examination
C14 Grant of patent or utility model
GR01 Patent grant
C41 Transfer of patent application or patent right or utility model
TR01 Transfer of patent right

Effective date of registration: 20151222

Address after: 528041, Foshan District, Guangdong city Chancheng District Lanshi (International) metal trading center fourteenth, two, 5 shop

Patentee after: Foshan City Cheung Tyrone Pioneer Metals Corporation

Address before: 528500, Ming 99, Ming two road, Gaoming Town, Gaoming District, Guangdong, Foshan

Patentee before: Foshan Dexingye Metal Technology Co.,Ltd.

TR01 Transfer of patent right

Effective date of registration: 20180928

Address after: 528313 107A No. C, Liyuan Logistics City No. 38, No. three industrial road, Tan Chau Industrial Zone, Shunde District, Foshan, Guangdong

Patentee after: Foshan huchengxin Pioneer Metals Corporation

Address before: 528041 Chancheng Lanshi (International) metal trading center, fourteenth, two, 5, Guangdong, Foshan.

Patentee before: Foshan City Cheung Tyrone Pioneer Metals Corporation

TR01 Transfer of patent right

Effective date of registration: 20210204

Address after: 330000 workshop 3 (1st floor), north of Meilin Avenue and west of Rixiu Road, Nanchang Economic and Technological Development Zone, Nanchang City, Jiangxi Province

Patentee after: Nanchang Liqi Machinery Manufacturing Co.,Ltd.

Address before: 528313 107A No. C, Liyuan Logistics City No. 38, No. three industrial road, Tan Chau Industrial Zone, Shunde District, Foshan, Guangdong

Patentee before: Foshan huchengxin Pioneer Metals Corp.

TR01 Transfer of patent right