CN102909612A - Method for grinding self-centering drill bit - Google Patents
Method for grinding self-centering drill bit Download PDFInfo
- Publication number
- CN102909612A CN102909612A CN2011102161786A CN201110216178A CN102909612A CN 102909612 A CN102909612 A CN 102909612A CN 2011102161786 A CN2011102161786 A CN 2011102161786A CN 201110216178 A CN201110216178 A CN 201110216178A CN 102909612 A CN102909612 A CN 102909612A
- Authority
- CN
- China
- Prior art keywords
- grinding
- flank
- tool
- drill
- tip
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Landscapes
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
Abstract
本发明属于对钻头的切削刃进行刃磨的技术领域,尤其涉及一种修磨自定心钻头的方法。该方法通过将定心钻头固定后,采用砂轮对定心钻头进行修磨,具体来讲,该方法通过调整定心钻头的各修磨面与具有尖角的砂轮之间的角度,顺次对定心钻头的刀尖第一后刀面、钻尖第一后刀面、刀尖第二后刀面、钻尖第二后刀面进行磨削。该方法通过现有的普通修磨设备实现了对钻头的研磨,实用性高,降低了使用成本。
The invention belongs to the technical field of sharpening the cutting edge of a drill bit, in particular to a method for grinding a self-centering drill bit. In this method, after the centering bit is fixed, the centering bit is ground with a grinding wheel. Specifically, the method adjusts the angle between each grinding surface of the centering bit and the grinding wheel with a sharp angle, and sequentially The first flank of the centering drill, the first flank of the drill point, the second flank of the tool point, and the second flank of the drill point are ground. The method realizes the grinding of the drill bit through the existing common grinding equipment, has high practicability and reduces the use cost.
Description
技术领域 technical field
本发明属于对钻头的切削刃进行刃磨的技术领域,尤其涉及一种修磨自定心钻头的方法。 The invention belongs to the technical field of sharpening the cutting edge of a drill bit, in particular to a method for grinding a self-centering drill bit.
背景技术 Background technique
钻头按槽型来分可分为直槽和螺旋槽两种,按螺旋角方向来分可分为正螺旋角和反螺旋角,根据实际需要螺旋角可以有大有小。从刀具材质来分有硬质合金、高速钢、还有焊接PCD钻头。刀柄有直柄和锥柄两种。现在的钻头大部分都是硬质合金直柄钻头,因为现在的刀柄都是液压、热涨还有侧固的固定形式。只有很少的专机还在使用锥柄钻头。按照钻头的顶角来看也摒弃以往钻头顶角118度的传统理念,开始有更多的钻头顶角有130度、135度、140度、150度根据要求不同可以有更多的钻头角度存在。按钻尖的形式来看有普通的钻尖和本方案所说的自定心钻尖,还有一种特殊的薄壁钻尖。在现在高速切削时代大多采用普通钻尖和自定心钻尖,普通钻尖使用最为广泛。因为自定心钻头修磨维护困难,即使数控磨床有时编程也十分困难,不能像刀具厂家批量生产一样统一。所以普通钻尖应用广泛,但是为了能够迅速准确的定位提高生产节拍,还是很多公司使用这种自定心钻头来实现快速准确定位实现高数切削。 According to the groove type, the drill bit can be divided into two types: straight groove and spiral groove. According to the direction of the helix angle, it can be divided into positive helix angle and reverse helix angle. The helix angle can be large or small according to actual needs. From the tool material, there are cemented carbide, high-speed steel, and welded PCD drills. There are two kinds of handles: straight handle and tapered handle. Most of the current drill bits are cemented carbide straight shank drill bits, because the current tool holders are all fixed in the form of hydraulic pressure, heat expansion and lateral solidification. Only a few special machines still use tapered shank drill bits. According to the top angle of the drill bit, the traditional concept of 118 degrees for the top angle of the drill bit is also abandoned. There are more drills with top angles of 130 degrees, 135 degrees, 140 degrees, and 150 degrees. According to different requirements, there can be more drill angles. . According to the form of the drill point, there are common drill points and the self-centering drill point mentioned in this program, as well as a special thin-walled drill point. In the current high-speed cutting era, ordinary drill points and self-centering drill points are mostly used, and ordinary drill points are the most widely used. Because of the difficulty in grinding and maintaining self-centering drills, even the programming of CNC grinding machines is sometimes very difficult, and cannot be as unified as mass production by tool manufacturers. Therefore, ordinary drill bits are widely used, but in order to quickly and accurately locate and improve production beats, many companies still use this self-centering drill to achieve fast and accurate positioning to achieve high-number cutting.
随着制造业的日益进步,对工件的精度和加工效率要求越来越高。自定心钻尖正逐渐代替普通钻尖。从而实现高速切削快速定位提高生产效率,但此类修磨维护十分困难。因为此类钻头钻尖由两部分构成,一是快速定位的钻尖,二是高速切削的刀尖。利用普通设备在修磨时,由于普通修磨设备只可以完成普通的直线运动,不能实现像数控磨床编程走差补的功能,修磨钻尖时刀尖干涉,修磨刀尖时钻尖干涉。即使用高精度五轴磨床对编程人员技能要求特别高。对刀具的修磨和重复利用带来极大的不便。造成刀具成本高,因刀具磨损后无法自行修复,需委派到外单位或返厂进行修磨,费用一般为新刀的30%或者更多。需支付高额的修磨费用,造成企业刀具成本高;同时因刀具修磨周期长,需要增加刀具的周转量才可以不影响正常的使用,给企业造成资金占用,给企业带来经济上的损失。 With the increasing progress of the manufacturing industry, the requirements for the precision and processing efficiency of the workpiece are getting higher and higher. Self-centering drill points are gradually replacing ordinary drill points. In this way, high-speed cutting and rapid positioning can be realized to improve production efficiency, but this type of grinding and maintenance is very difficult. Because the drill tip of this type of drill bit is composed of two parts, one is the drill tip for rapid positioning, and the other is the tool tip for high-speed cutting. When using ordinary equipment for grinding, because ordinary grinding equipment can only complete ordinary linear motion, it cannot realize the function of compensating for deviations in programming like a CNC grinder. The tool tip interferes when grinding the drill tip, and the drill tip interferes when grinding the tool tip. . Even the use of high-precision five-axis grinding machines requires particularly high skills for programmers. It brings great inconvenience to the sharpening and repeated utilization of the cutting tool. The cost of the tool is high, because the tool cannot be repaired by itself after it is worn out, it needs to be assigned to an external unit or returned to the factory for regrinding, and the cost is generally 30% or more of the new knife. It is necessary to pay a high amount of grinding costs, resulting in high tool costs for the enterprise; at the same time, due to the long tool grinding cycle, it is necessary to increase the turnover of the tools so as not to affect the normal use, causing capital occupation for the enterprise and bringing economic losses to the enterprise. loss.
发明内容 Contents of the invention
为解决现有技术中存在的不足,本发明提供了一种修磨自定心钻头的方法,其通过现有的普通修磨设备实现了对钻头的研磨,实用性高,降低了使用成本。 In order to solve the deficiencies in the prior art, the present invention provides a method for grinding self-centering drill bits, which realizes the grinding of drill bits through existing common grinding equipment, has high practicability, and reduces the use cost.
为实现上述目的,本发明的修磨自定心钻头的方法,通过将定心钻头固定后,采用较尖的碗型或蝶形砂轮对定心钻头进行修磨,该方法通过调整定心钻头的各修磨面与具有尖角的砂轮之间的角度,顺次对定心钻头的刀尖第一后刀面、钻尖第一后刀面、刀尖第二后刀面、钻尖第二后刀面进行磨削。 In order to achieve the above object, the method for grinding the self-centering drill bit of the present invention, after the centering drill bit is fixed, adopts a sharper bowl-shaped or butterfly-shaped emery wheel to grind the centering drill bit, the method adjusts the centering drill bit The angle between each grinding surface of the centering drill bit and the grinding wheel with sharp corners, the first flank of the centering drill bit, the first flank of the drill point, the second flank of the tool point, the second flank of the drill point The second flank is ground.
作为对上述方式的限定,所述的砂轮为碗型砂轮或蝶形砂轮。 As a limitation to the above manner, the grinding wheel is a bowl-shaped grinding wheel or a butterfly-shaped grinding wheel.
具体来讲,本发明的修磨自定心钻头的方法包括如下步骤: Specifically, the method for grinding self-centering drill bit of the present invention comprises the following steps:
步骤一,自定心钻头的固定,将定心钻头装夹在刀具装夹轴上,使定心钻头的中心线与刀具装夹轴的轴线平行; Step 1, fixing the self-centering drill bit, clamping the centering drill bit on the tool clamping shaft, so that the center line of the centering drill bit is parallel to the axis of the tool clamping shaft;
步骤二,刀尖第一后刀面修磨,调整砂轮角度,使砂轮上翘,砂轮相对刀尖第一后刀面形成7~10度的第一后角;进给修磨定心钻头,通过砂轮将定心钻头的第一后刀面修磨至刀尖处,对其中一个刀尖第一后刀面修磨到位;将自定心钻头旋转180度后,对另一个刀尖第一后刀面修磨位; Step 2: Grinding the first flank of the tool tip, adjusting the angle of the grinding wheel so that the grinding wheel is upturned, and the grinding wheel forms a first relief angle of 7 to 10 degrees relative to the first flank of the tool tip; feed and grind the centering drill bit, Use the grinding wheel to grind the first flank of the centering drill to the tool tip, and grind the first flank of one of the tool tips in place; after rotating the self-centering drill 180 degrees, grind the first flank of the other tool tip Flank grinding position;
步骤三,钻尖第一后刀面修磨,调整刀具装夹轴,使其与砂轮尖角所在端面之间具有钻尖一半的角度,通过砂轮将钻尖第一后刀面修磨到刀尖第一后刀面处,对钻尖其中一个第一后刀面修磨到位;将自定心钻头旋转180度后,对钻尖另一个第一后刀面修磨到位; Step 3: Grinding the first flank of the drill tip, adjusting the tool clamping axis so that it has half the angle of the drill tip with the end face where the sharp corner of the grinding wheel is, and grinding the first flank of the drill tip to the tool through the grinding wheel At the first flank of the drill point, grind one of the first flanks of the drill point in place; after rotating the self-centering drill 180 degrees, grind the other first flank of the drill point in place;
步骤四,刀尖第二后刀面修磨,基于步骤三,将刀具装夹轴上抬10~15度,以刃带为基准,通过控制刀尖第二后刀面研磨长度,通过砂轮将第二后刀面修磨至刀尖处,对其中一个刀尖第二后刀面修磨到位;将自定心钻头旋转180度后,对另一个刀尖第二后刀面修磨到位; Step 4: Grinding the second flank of the tool tip. Based on step 3, raise the tool clamping axis by 10~15 degrees. Taking the edge band as the reference, control the grinding length of the second flank of the tool tip, and use the grinding wheel to The second flank is ground to the tip of the tool, and the second flank of one tool tip is ground in place; after the self-centering drill is rotated 180 degrees, the second flank of the other tool tip is ground in place;
步骤五,钻尖第二后刀面修磨,调整刀具装夹轴,使其与砂轮尖角所在端面之间具有钻尖一半的角度,通过控制研磨量以形成钻尖第一后刀面宽度,使用砂轮将钻尖第二后刀面修磨到刀尖第二后刀面处,对钻尖其中一个第二后刀面修磨到位;将自定心钻头旋转180度后,对钻尖另一个第二后刀面修磨到位。 Step 5: Grinding the second flank of the drill tip, adjusting the tool clamping axis so that it has half the angle of the drill tip with the end face where the sharp corner of the grinding wheel is located, and controlling the amount of grinding to form the width of the first flank of the drill tip , use the grinding wheel to grind the second flank of the drill tip to the second flank of the tool tip, and grind one of the second flanks of the drill tip in place; after rotating the self-centering drill 180 degrees, the drill tip Another second relief ground in place.
进一步的,步骤六,开横刃,由砂轮磨出宽度为0.2mm-0.3mm的横韧。 Further, in step six, cut the chisel edge, and grind the transverse toughness with a width of 0.2mm-0.3mm by the grinding wheel.
作为对上述方式的限定,在上述各步骤对自定心钻头的各后刀面修磨到位后,均加工一个相等的研磨量。 As a limitation to the above method, after each flank of the self-centering drill is ground in place in each of the above steps, an equal amount of grinding is processed.
作为对上述方式的进一步限定,上述的研磨量为0.2mm。 As a further limitation on the above manner, the above grinding amount is 0.2mm.
作为对上述方式的改进,上述的自定心钻头通过弹簧夹套固定在刀具装夹轴上。 As an improvement to the above method, the above self-centering drill bit is fixed on the tool clamping shaft through a spring collet.
作为对上述方式的限定,在步骤一前包括跳动检查步骤,将自定心钻头用弹簧夹套夹好安装在刀具装夹轴上时,对刀具相对刀具装夹轴的轴线跳动量进行检查。 As a limitation to the above method, a runout inspection step is included before step 1. When the self-centering drill is clamped and installed on the tool clamping shaft with a spring collet, the axial runout of the tool relative to the tool clamping shaft is checked.
作为对上述方式的进一步限定,所述的刀具跳动量为0.02mm。 As a further limitation to the above manner, the said tool runout is 0.02mm.
采用上述技术方案,利用碗型砂轮或蝶形砂轮尖角的特点,通过将自定心钻头的各后刀面进行分部顺次研磨,实现了较好的研磨效果,解决了对自定心钻头的修复设备投入,使自定心钻头修磨后可再次利用,对设备和人员要求较低。 By adopting the above-mentioned technical scheme and using the characteristics of the sharp corner of the bowl-shaped grinding wheel or the butterfly-shaped grinding wheel, the flank face of the self-centering drill bit is ground sequentially in sections to achieve a better grinding effect and solve the problem of self-centering. The repair equipment of the drill bit is put into use, so that the self-centering drill bit can be used again after grinding, and the requirements for equipment and personnel are relatively low. the
附图说明 Description of drawings
下面结合附图及具体实施方式对本发明作更进一步详细说明: Below in conjunction with accompanying drawing and specific embodiment the present invention is described in further detail:
图1为本发明涉及的自定心钻头的整体结构示意图; Fig. 1 is the overall structure schematic diagram of the self-centering drill bit that the present invention relates to;
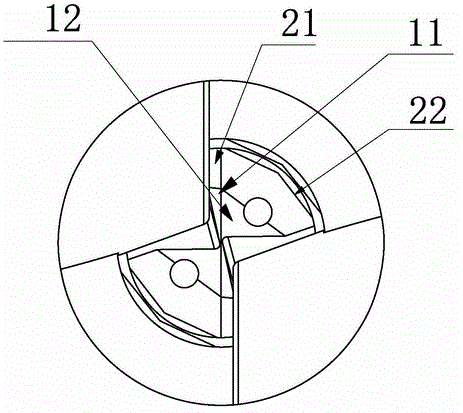
图2为图1的右视图。 Fig. 2 is the right side view of Fig. 1 .
图中: In the picture:
1、钻尖;11、钻尖第一后刀面;12、钻尖第二后刀面;2、刀尖;21、刀尖第一后刀面;22、刀尖第二后刀面。 1. Drill tip; 11. First flank of drill tip; 12. Second flank of drill tip; 2. Tool tip; 21. First flank of tool tip; 22. Second flank of tool tip.
具体实施方式 Detailed ways
下面以现有的典型硬质合金直槽自定心钻头为例,对本发明的方法详细描述如下: Taking the existing typical cemented carbide straight flute self-centering drill as an example, the method of the present invention is described in detail below:
由图1所示可知,该自定心钻头的切削部分主要由钻尖1和刀尖2两部分组成,且由图2可以看出,该自定心钻头有钻尖1和刀尖2的组合结构。其中,钻尖1钻尖第一后刀面11和钻尖第二后刀面12,刀尖2刀尖第一后刀面21和刀尖第二后刀面。
As can be seen from Figure 1, the cutting part of the self-centering drill is mainly composed of drill tip 1 and
在对上述自定心钻头进行修复时,其修复的总体思路是对钻头进行分解,通过调整定心钻头的各修磨面与具有尖角的砂轮之间的角度,顺次对定心钻头的刀尖第一后刀面21、钻尖第一后刀面11、刀尖第二后刀面22、钻尖第二后刀面12进行磨削。砂轮采用碗型砂轮(11V9)或蝶形砂轮(12V9)。
When repairing the above-mentioned self-centering drill bit, the general idea of the repair is to decompose the drill bit, adjust the angle between each grinding surface of the centering drill bit and the grinding wheel with a sharp angle, and sequentially correct the centering drill bit. The
其具体研磨的方法包括如下步骤: Its concrete grinding method comprises the steps:
步骤一,将定心钻头用弹簧套夹好后安装在具有刀具装夹轴的设备上,采用磁力表或百分表检测钻头安装的跳动,具体是将磁力表座吸附在设备上检测两个刀尖的高度,将表头接触刀尖记下百分表读数,然后刀具旋转180度测量另一刀尖的高度,若相差太大则说明刀具装夹有问题需要调整,保证刀具的跳动在0.02mm,以使定心钻头的中心线与刀具装夹轴的轴线重合; Step 1: Clamp the centering drill bit with a spring sleeve and install it on the equipment with the tool clamping shaft. Use a magnetic gauge or a dial indicator to detect the runout of the drill bit installation. Specifically, attach the magnetic gauge base to the equipment to detect two For the height of the tool tip, touch the gauge head to the tip of the tool and record the reading on the dial indicator, then rotate the tool 180 degrees to measure the height of the other tool tip. If the difference is too large, it means that there is a problem with the tool clamping and needs to be adjusted to ensure that the tool’s runout is within 0.02 mm, so that the centerline of the centering drill coincides with the axis of the tool clamping shaft;
步骤二,刀尖第一后刀面21修磨,将装有刀具的装夹轴调节到水平状态,以确保修磨的钻头主切削刃与钻头中心线垂直,此时,砂轮和刀具平行。调整砂轮角度,使砂轮轴向上抬起7~10度,使砂轮相对刀尖第一后刀面形成7~10度的第一后角,在这里要尽量使用砂轮直径最大处,以保证修磨钻尖的质量。通过手动进给定心钻头,使定心钻头的刀尖第一后刀面21和砂轮接触开始修磨,定心钻头每次的进给量为0.01mm为宜,通过砂轮将定心钻头的刀尖第一后刀面21修磨至刀尖处,对其中一个刀尖第一后刀面修磨到位,然后再进给修磨0.2mm左右的研磨量,修磨到位后记下此位置;将自定心钻头旋转180度后,对另一个刀尖第一后刀面21修磨到位后,同样在进给修磨0.2mm左右的研磨量,以将磨损部分修磨好;
步骤三,钻尖第一后刀面11修磨,以钻尖部分的角度为120度为例,调整刀具装夹轴,使刀具装夹轴与砂轮最尖部分单边形成60度夹角,通过砂轮将钻尖第一后刀面修模到刀尖第一后刀面处时停止砂轮进给,然后修磨另一边,反复研磨后让刀具向前进0.2mm左右;将自定心钻头旋转180度后,对钻尖另一个第一后刀面修磨后,让刀具向前进0.2mm左右,以实现钻尖第一后刀面11和刀尖第一后刀面21的无缝对接;
Step 3: Grinding the
步骤四,刀尖第二后刀面22修磨,这一步骤中砂轮和设备状态与步骤二基本相同,只是基于步骤三,将刀具装夹轴上抬10~15度,逐渐进给修磨。方法和修磨刀尖第一后刀面基本相同,只是要控制修磨量,以控制第一后刀面的宽度,一般第一后刀面的宽度在0.3~0.5mm左右,由于不易进行拆卸测量,所以这个宽度可以以刀具的刃带为基准,宽度与刃带宽度一样就可以使第二后刀面的长度和第一后刀面长度一致,通过控制刀尖第二后刀面研磨长度,通过砂轮将第二后刀面修磨至刀尖处,对其中一个刀尖第二后刀面修磨到位,然后进给修磨0.2mm左右的研磨量;将自定心钻头旋转180度后,对另一个刀尖第二后刀面修磨到位,再进给修磨0.2mm左右的研磨量;
Step 4: Grinding the
步骤五,钻尖第二后刀面12修磨,该步骤与步骤三基本相同,不同之处在于基于步骤四,调整刀具装夹轴,使其与砂轮尖角所在端面之间形成60度夹角。
Step 5: Grinding the
步骤六,开横刃,由砂轮磨出宽度为0.2mm-0.3mm的横韧。 Step 6, cut the chisel edge, and grind the transverse toughness with a width of 0.2mm-0.3mm by the grinding wheel.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201110216178.6A CN102909612B (en) | 2011-07-31 | 2011-07-31 | Method for grinding self-centering drill bit |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201110216178.6A CN102909612B (en) | 2011-07-31 | 2011-07-31 | Method for grinding self-centering drill bit |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN102909612A true CN102909612A (en) | 2013-02-06 |
| CN102909612B CN102909612B (en) | 2014-12-03 |
Family
ID=47608319
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201110216178.6A Expired - Fee Related CN102909612B (en) | 2011-07-31 | 2011-07-31 | Method for grinding self-centering drill bit |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102909612B (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104227093A (en) * | 2014-09-12 | 2014-12-24 | 广西玉林达业机械配件有限公司 | Drill point centering countersinking cutter |
| JP2019166591A (en) * | 2018-03-22 | 2019-10-03 | 株式会社不二越 | Drill |
| CN112643414A (en) * | 2020-12-09 | 2021-04-13 | 航天科工哈尔滨风华有限公司 | Method for processing and manufacturing hard alloy drill bit |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB932422A (en) * | 1958-12-11 | 1963-07-24 | Birmingham Small Arms Co Ltd | Improvements in or relating to the pointing of drills |
| JPS5577453A (en) * | 1978-11-29 | 1980-06-11 | Seiichi Tsunoda | Drill grinding machine |
| CN2158766Y (en) * | 1992-10-31 | 1994-03-16 | 西南石油学院 | Hand-driven cutter grinding device for group drills |
| CN1295903A (en) * | 2000-12-08 | 2001-05-23 | 王存厚 | Other axle helicoidal surface grinding method and edge-grinding machine for cutting edge of twist drill |
| CN101053940A (en) * | 2007-04-17 | 2007-10-17 | 湖南大学 | Sharpening method for drill tip back knife face of fully screw face drill |
| CN101081483A (en) * | 2007-04-17 | 2007-12-05 | 湖南大学 | Full helicoidal surface Micro-drill web thinning method |
-
2011
- 2011-07-31 CN CN201110216178.6A patent/CN102909612B/en not_active Expired - Fee Related
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB932422A (en) * | 1958-12-11 | 1963-07-24 | Birmingham Small Arms Co Ltd | Improvements in or relating to the pointing of drills |
| JPS5577453A (en) * | 1978-11-29 | 1980-06-11 | Seiichi Tsunoda | Drill grinding machine |
| CN2158766Y (en) * | 1992-10-31 | 1994-03-16 | 西南石油学院 | Hand-driven cutter grinding device for group drills |
| CN1295903A (en) * | 2000-12-08 | 2001-05-23 | 王存厚 | Other axle helicoidal surface grinding method and edge-grinding machine for cutting edge of twist drill |
| CN101053940A (en) * | 2007-04-17 | 2007-10-17 | 湖南大学 | Sharpening method for drill tip back knife face of fully screw face drill |
| CN101081483A (en) * | 2007-04-17 | 2007-12-05 | 湖南大学 | Full helicoidal surface Micro-drill web thinning method |
Non-Patent Citations (1)
| Title |
|---|
| 吕彦明等: "复杂螺旋面钻尖刃磨原理及实现", 《中国机械工程》, vol. 11, no. 3, 30 March 2000 (2000-03-30) * |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104227093A (en) * | 2014-09-12 | 2014-12-24 | 广西玉林达业机械配件有限公司 | Drill point centering countersinking cutter |
| JP2019166591A (en) * | 2018-03-22 | 2019-10-03 | 株式会社不二越 | Drill |
| JP7082750B2 (en) | 2018-03-22 | 2022-06-09 | 株式会社不二越 | Drill |
| CN112643414A (en) * | 2020-12-09 | 2021-04-13 | 航天科工哈尔滨风华有限公司 | Method for processing and manufacturing hard alloy drill bit |
Also Published As
| Publication number | Publication date |
|---|---|
| CN102909612B (en) | 2014-12-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN101407016B (en) | A machining method of a turbine shaft | |
| CN102990304B (en) | Spherical surface machining method | |
| WO2016054760A1 (en) | Fixed chuck threaded adjustable suspended sliding blade chamfering device | |
| CN104227345A (en) | Processing method for high-precision thin step shaft and grinding chuck for processing method | |
| CN107160114A (en) | The processing method of floating disc | |
| CN102962489B (en) | Large support plate elastic hole drilling machine and use method thereof | |
| CN106021796A (en) | Remaining-life predicting method for ball end mill for chrome steel blade profile | |
| CN103480862B (en) | High accuracy and roughness circular cone endoporus turning process | |
| CN102909612B (en) | Method for grinding self-centering drill bit | |
| CN103624653B (en) | Processing method for forming helical groove of twist drill | |
| CN102350646B (en) | Typical curved part milling fixture | |
| CN105538108B (en) | A processing method for NdFeB small magnetic rings with high verticality requirements | |
| CN102350657B (en) | Method for coping center drill with protecting cone | |
| CN103659519A (en) | Grinding method for machining high-precision outer spherical surface through ordinary cylindrical grinding machine | |
| CN202572027U (en) | Positioning device for hob sharpening machine | |
| CN112238331A (en) | Method for processing aluminum alloy car body long and large section notch | |
| CN206286940U (en) | A 50EF spherical milling cutter grinder assembly | |
| CN204724906U (en) | Bore boring compound tool | |
| CN202622069U (en) | Reamer provided with locator | |
| CN115430993A (en) | Main shaft for ultra-large mine crushing equipment and machining method | |
| CN104842217B (en) | Sky and space plane ceramic fibre rigidity thermal insulation tile precision machining method | |
| CN203542341U (en) | Locating device of grinding center hole | |
| CN103537723A (en) | Method for manufacturing common-rail overlapping double-hole type high-pressure fuel pipe of diesel engine | |
| CN108127353B (en) | A kind of compressor long axis processing method | |
| CN105382663A (en) | Machining method for profile detection test sheet of diamond roller |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| TR01 | Transfer of patent right | ||
| TR01 | Transfer of patent right |
Effective date of registration: 20201224 Address after: No.99 Hangzhou Road, Rizhao Economic and Technological Development Zone, Rizhao City, Shandong Province Patentee after: Rizhao Weiyi Automobile Co.,Ltd. Address before: 071000 No. 2266 Chaoyang South Street, Hebei, Baoding Patentee before: Great Wall Motor Co.,Ltd. |
|
| CP01 | Change in the name or title of a patent holder | ||
| CP01 | Change in the name or title of a patent holder |
Address after: No.99 Hangzhou Road, Rizhao Economic and Technological Development Zone, Rizhao City, Shandong Province Patentee after: Rizhao WeiPai Automobile Co.,Ltd. Address before: No.99 Hangzhou Road, Rizhao Economic and Technological Development Zone, Rizhao City, Shandong Province Patentee before: Rizhao Weiyi Automobile Co.,Ltd. |
|
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20141203 |