CN102886407A - bending and machining device for arc-shaped part - Google Patents
bending and machining device for arc-shaped part Download PDFInfo
- Publication number
- CN102886407A CN102886407A CN2012103489025A CN201210348902A CN102886407A CN 102886407 A CN102886407 A CN 102886407A CN 2012103489025 A CN2012103489025 A CN 2012103489025A CN 201210348902 A CN201210348902 A CN 201210348902A CN 102886407 A CN102886407 A CN 102886407A
- Authority
- CN
- China
- Prior art keywords
- support wheel
- installing rack
- right support
- bent
- wheel installing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Landscapes
- Transmission Devices (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
Abstract
本发明涉及一种弧形零件弯形加工装置,包括支座及其上设置的转动臂,转动臂上设置有压轮,弯形装置还包括与压轮配合使用而使相应待弯零件被滚压成形的支撑轮,所述的支座上还设置有支撑轮安装架,所述的支撑轮包括设置于所述支撑轮安装架上并在相应待加工零件被滚压成形时分布于所述压轮左、右两侧的左、右支撑轮,所述左、右支撑轮具有用于与相应待弯零件的被弯部分两端滚动撑托配合的外周面,所述压轮具有在随所述转动臂由上至下翻转时与相应待弯零件的被弯部分中部滚压配合而使待弯零件的被弯部分中部下凹变形的外周面。本发明提供了一种由待弯零件的中部进行弯形加工,以不损坏待弯零件两端结构的弧形零件弯形加工装置。
The invention relates to a bending processing device for arc-shaped parts, which includes a support and a rotating arm arranged on it, and a pressing wheel is arranged on the rotating arm. Press-formed support wheels, the support wheel is also provided with a support wheel mounting frame, the support wheel is arranged on the support wheel mounting frame and distributed in the corresponding parts to be processed when rolling forming The left and right support wheels on the left and right sides of the pressure wheel, the left and right support wheels have outer peripheral surfaces for rolling and supporting the two ends of the bent part of the corresponding part to be bent. When the turning arm is turned from top to bottom, it rolls and fits with the middle part of the bent part of the corresponding part to be bent, so that the outer peripheral surface of the middle part of the bent part of the part to be bent is concave and deformed. The invention provides a bending processing device for an arc-shaped part, which can be bent from the middle of the part to be bent so as not to damage the structures at both ends of the part to be bent.
Description
技术领域 technical field
本发明涉及用于加工弧形零件的弧形零件弯形加工装置。 The invention relates to an arc part bending processing device for processing arc parts.
背景技术 Background technique
在实际生产中,经常会用的一些弧形类零件,比如说U形管、U形螺栓、弧形管接头等,这类弧形零件需要现场利用弯形装置进行弯形制作,现有的弯形装置如中国专利CN202224485U公开的“手动弯管装置”,该手动弯管装置包括支座及与支座转动连接的转动架,转动架为“U”形,在转动架封闭的一端连接有加力杆,转动架与加力杆一起构成一个转动臂,转动架内部通过第一固定轴和第二固定轴分别连接第一滚轮和第二滚轮,第一滚轮和第二滚轮的外周面上均设有与相应待弯零件的外周弧面适配的环槽,支座上还设置有支撑件。使用时,待弯零件的前端由支撑件中穿过,进入到第一滚轮和第二滚轮之间,并探出,转动加力杆,转动架以第一固定轴为圆心,作圆周运动,第一滚轮和第二滚轮始终紧贴住待弯零件,第一滚轮相当于一个支撑轮,第二滚轮相当于一个压轮,压轮由待弯零件的后端滚向待弯零件的前端过程中将待弯零件逐渐弯形成预期的弧形结构。这种双滚轮弯形装置存在的问题在于:压轮必须由待弯零件的一端滚向待弯零件的另一端才能实现待弯零件的弧形加工,当待弯零件的两端均有工作结构时,现有的弯形装置就不能适用,比如说U形螺栓的弯制过程中,U形螺栓的两端均设有外螺纹,如果采用现有的这种弯形装置,压轮就有可能将U形螺栓两端的外螺纹挤压坏而导致U形螺栓不能使用;同时由于压轮由待弯零件的一端滚向另一端时,压轮带着待弯零件有向前窜的趋势,因此必须通过支撑件对待弯零件的后端进行限位,这就使得要想弯制成一个零件,零件制作过程中的实际用料就必须比零件的使用长度要长,从而造成材料的浪费和制作成本的增加。 In actual production, some arc-shaped parts are often used, such as U-shaped pipes, U-shaped bolts, arc-shaped pipe joints, etc. These arc-shaped parts need to be bent on site with bending devices. Bending device such as the "manual pipe bending device" disclosed in Chinese patent CN202224485U, the manual pipe bending device includes a support and a turret connected to the support in rotation. The booster rod, the turret and the booster rod together form a rotating arm, the inside of the turret is respectively connected to the first roller and the second roller through the first fixed shaft and the second fixed shaft, and the outer peripheral surfaces of the first roller and the second roller are All are provided with ring grooves adapted to the outer peripheral arc surfaces of the corresponding parts to be bent, and supports are also provided on the supports. When in use, the front end of the part to be bent passes through the support, enters between the first roller and the second roller, and protrudes out. Turning the force bar, the turret moves in a circle with the first fixed shaft as the center. The first roller and the second roller are always close to the part to be bent. The first roller is equivalent to a support wheel, and the second roller is equivalent to a pressure wheel. The pressure wheel rolls from the rear end of the part to be bent to the front end of the part to be bent. In the middle, the parts to be bent are gradually bent to form the expected arc structure. The problem with this double-roller bending device is that the pressure roller must roll from one end of the part to be bent to the other end of the part to be bent to realize the arc processing of the part to be bent. When both ends of the part to be bent have working structures , the existing bending device cannot be applied. For example, in the bending process of U-shaped bolts, both ends of the U-shaped bolts are provided with external threads. If the existing bending device is used, the pressure roller will have The external thread at both ends of the U-shaped bolt may be squeezed and the U-shaped bolt cannot be used; at the same time, when the pressure roller rolls from one end of the part to be bent to the other end, the pressure wheel will move forward with the part to be bent. Therefore, the rear end of the part to be bent must be limited by the support, which makes it necessary to bend it into a part, the actual material used in the part manufacturing process must be longer than the use length of the part, resulting in material waste and Increased production costs.
发明内容 Contents of the invention
本发明的目的在于提供一种由待弯零件的中部进行弯形加工,以不损坏待弯零件两端结构的弧形零件弯形加工装置。 The object of the present invention is to provide a bending processing device for arc-shaped parts that can be bent from the middle of the part to be bent so as not to damage the structures at both ends of the part to be bent.
为了解决上述问题,本发明的技术方案为: In order to solve the above problems, the technical solution of the present invention is:
一种弧形零件弯形加工装置,包括支座及其上设置的转动轴线沿前后方向延伸的转动臂,转动臂上设置有转动轴线沿前后延伸的压轮,弯形装置还包括与压轮配合使用而使相应待弯零件被滚压成形的支撑轮,所述的支座上还设置有支撑轮安装架,所述的支撑轮包括设置于所述支撑轮安装架上并在相应待加工零件被滚压成形时分布于所述压轮左、右两侧的左、右支撑轮,所述左、右支撑轮具有用于与相应待弯零件的被弯部分两端滚动撑托配合的外周面,所述压轮具有在随所述转动臂由上至下翻转时与相应待弯零件的被弯部分中部滚压配合而使待弯零件的被弯部分中部下凹变形的外周面。 A bending processing device for arc-shaped parts, comprising a support and a rotating arm with a rotating axis extending along the front-to-back direction; Cooperate with the supporting wheels that make the corresponding parts to be bent be rolled and formed, and the support wheel is also provided with a supporting wheel mounting frame, and the supporting wheel includes a supporting wheel that is arranged on the supporting wheel mounting The left and right support wheels are distributed on the left and right sides of the pressure wheel when the parts are rolled and formed. On the outer peripheral surface, the pressing wheel has an outer peripheral surface that rolls and fits with the middle part of the bent part of the corresponding part to be bent when the rotating arm is turned from top to bottom, so that the middle part of the bent part of the part to be bent is concavely deformed.
所述的支撑轮安装架包括左右分体设置的左支撑轮安装架和右支撑轮安装架,所述的弯形装置还包括对所述左、右支撑轮安装架之间的间距进行调节的间距调节机构。 The supporting wheel mounting frame includes a left supporting wheel mounting frame and a right supporting wheel mounting frame which are separately arranged on the left and right sides, and the bending device also includes a device for adjusting the distance between the left and right supporting wheel mounting frames. Spacing adjustment mechanism.
所述的间距调节机构包括于所述支座上设置的导向方向沿左右方向延伸的导轨,所述的左、右支撑轮安装架上均设置有与所述导轨导向滑动配合的导轨配合部,所述的间距调节机构还包括轴向沿左右方向延伸并与所述支座轴向移动限位配合的丝杠,所述丝杠的左、右端分别设置有旋向相反的左旋外螺纹和右旋外螺纹,所述左、右支撑轮安装架上分别设有与左、右旋外螺纹旋合适配的左、右旋内螺纹。 The distance adjustment mechanism includes guide rails provided on the support which extend along the left and right directions, and the left and right supporting wheel mounting frames are provided with guide rail matching parts that slide and cooperate with the guide rails. The distance adjustment mechanism also includes a lead screw axially extending along the left and right directions and cooperating with the axial movement limit of the support. The left and right ends of the lead screw are respectively provided with left-handed external threads and right The left and right support wheel mounting frames are respectively provided with left and right-handed internal threads that are suitable for the left-handed and right-handed external threads.
所述的左、右支撑轮安装架上分别设置有导向方向沿左右方向延伸的左、右支撑轮安装架导向长孔,所述的支座上分别设有与所述左、右支撑轮安装架导向长孔位置对应的左、右支撑轮安装架螺纹孔,所述的左、右支撑轮安装架导向长孔与对应左、右支撑轮安装架螺纹孔中分别连接有对左、右支撑轮安装架进行固定锁紧的左、右支撑轮安装架螺栓。 The left and right support wheel mounting frames are respectively provided with guide slots for the left and right support wheel mounting frames whose guiding direction extends along the left and right directions, and the described supports are respectively provided with mounting holes for mounting with the left and right support wheels. The left and right support wheel mounting frame threaded holes corresponding to the positions of the frame guide slots, the left and right support wheel mounting frame guide slots and the corresponding left and right support wheel mounting frame threaded holes are respectively connected with left and right support The left and right support wheel mounting frame bolts that are fixed and locked by the wheel mounting frame.
所述的转动臂上还设置有导向方向与所述转动臂延伸方向一致的转动臂导向长孔,所述压轮的转轴滚动导向装配于所述的转动臂导向长孔中,所述的支座上于所述的左、右支撑轮安装架之间固设有中心滚轮架,所述的中心滚轮架上设置有导向方向沿上下方向延伸并用于在所述压轮对相应待弯零件滚压成型时与压轮的转轴滚动导向配合的竖向导向机构。 The rotating arm is also provided with a rotating arm guiding long hole whose guiding direction is consistent with the extending direction of the rotating arm. A central roller frame is fixed between the left and right support wheel mounting brackets on the seat, and the center roller frame is provided with a guiding direction extending along the up and down direction and used for rolling the corresponding parts to be bent by the pressure rollers. A vertical guide mechanism that cooperates with the rolling guide of the rotating shaft of the press wheel during pressing.
所述的竖向导向机构包括槽深沿上下方向延伸的十字槽,所述的十字槽由沿左右方向延伸以供所述压轮由上至下通过的横槽和沿前后方向延伸的竖槽构成,所述的竖槽具有导向方向沿上下方向延伸以实现所述竖向导向机构与所述压轮的转轴滚动导向配合的槽壁。 The vertical guide mechanism includes a cross groove whose groove depth extends in the up and down direction, and the cross groove is composed of a horizontal groove extending in the left and right direction for the pressure roller to pass from top to bottom and a vertical groove extending in the front and rear direction As a configuration, the vertical groove has a groove wall whose guiding direction extends along the vertical direction to realize the rolling guiding cooperation between the vertical guiding mechanism and the rotating shaft of the pressing wheel.
所述的支座上于所述的左、右支撑轮安装架之间固设有中心滚轮架,所述的中心滚轮架上设置有槽深沿上下方向延伸的十字槽,所述的十字槽由沿左右方向延伸以供所述压轮由上至下通过的横槽和沿前后方向延伸的竖槽构成,所述的竖槽具有导向方向沿上下方向延伸并用于与所述压轮的转轴的两端导向配合的槽壁,所述丝杠上于所述左、右旋外螺纹之间设置有环形凹槽,所述的中心滚轮架上设有插装于所述环形凹槽中与所述环形凹槽的槽壁限位配合而使所述丝杠轴向移动被限位的限位板。 A central roller frame is fixed between the left and right support wheel mounting brackets on the support, and a cross groove with a groove depth extending in the up and down direction is arranged on the center roller frame, and the cross groove It is composed of a horizontal groove extending in the left and right direction for the pressure roller to pass through from top to bottom and a vertical groove extending in the front and rear direction. The two ends of the two ends are guided to match the groove wall, and the screw is provided with an annular groove between the left and right-handed external threads, and the center roller frame is provided with a groove inserted in the annular groove and The groove wall of the annular groove is limitedly fitted with the limiting plate that enables the axial movement of the screw to be limited.
所述的支座上于所述左支撑轮安装架的左侧固设有铰链支架,所述的转动臂包括与所述铰链支架铰接相连的U形的转动架,所述的转动臂还包括设置于所述转动架的封闭端上的用于手持的加力杆。 A hinge bracket is fixed on the left side of the left support wheel mounting bracket on the support, and the rotating arm includes a U-shaped turret hingedly connected with the hinge bracket, and the rotating arm also includes An afterburner rod for hand-holding is arranged on the closed end of the turret.
所述的加力杆与所述转动架通过螺纹连接固定相连或通过焊接固定相连。 The reinforcing rod is fixedly connected with the turret through threaded connection or through welding.
所述铰链支架上螺纹连接有轴向沿左右方向延伸的定位螺杆,所述定位螺杆的右端具有用于与相应待弯零件的左端端面挡止定位配合的定位端面。 The hinge bracket is threaded with a positioning screw extending axially along the left and right directions, and the right end of the positioning screw has a positioning end surface for blocking and positioning cooperation with the left end surface of the corresponding part to be bent.
本发明的有益效果为:通过压轮和分布于压轮左、右两侧的左、右支撑轮配合来使相应待弯零件滚压弯形,使用时将相应待弯零件的两端分别置于左、右支撑轮上,压轮随转动臂由上至下翻转时由待弯零件的中部向下滚压,在左、右支撑轮的滚动撑托配合下,待弯零件的中部被滚压成下凹的弧形。通过三个滚轮配合,使待弯零件由中部开始变形,不会破坏待弯零件两端的结构,可以适用于U形螺栓等其它两端有工作结构的情况;同时待弯零件由中部开始变形,待弯零件的两端直接被左、右支撑轮撑托限位,不需要对待弯零件多余部分的结构进行限位,节省了原材料,降低了生产成本。 The beneficial effects of the present invention are as follows: through the cooperation of the pressing wheel and the left and right supporting wheels distributed on the left and right sides of the pressing wheel, the corresponding parts to be bent are rolled and bent, and the two ends of the corresponding parts to be bent are respectively placed On the left and right supporting wheels, the pressing wheel rolls down from the middle of the part to be bent when the rotating arm is turned from top to bottom. With the cooperation of the rolling support of the left and right supporting wheels, the middle part of the part to be bent is rolled Press into a concave arc. Through the cooperation of three rollers, the part to be bent starts to deform from the middle, without damaging the structure at both ends of the part to be bent, and can be applied to U-shaped bolts and other situations where there are working structures at both ends; at the same time, the part to be bent starts to deform from the middle, The two ends of the part to be bent are directly supported and limited by the left and right support wheels, and there is no need to limit the structure of the redundant part of the part to be bent, which saves raw materials and reduces production costs. the
附图说明 Description of drawings
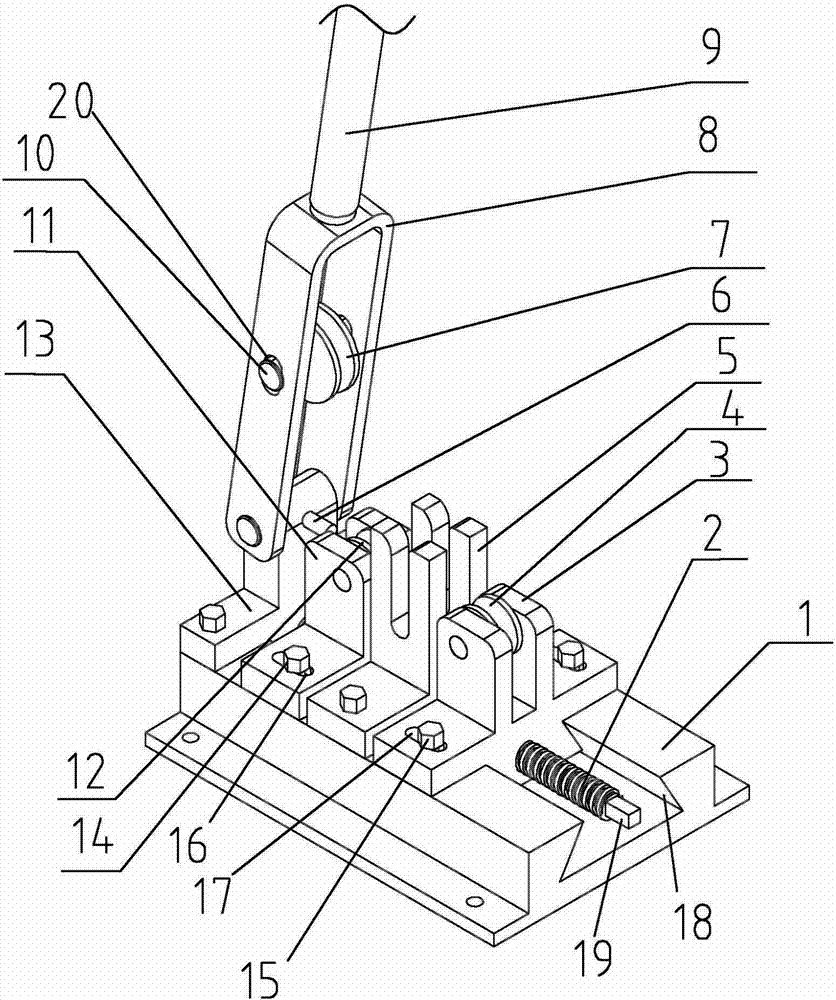
图1是本发明实施例的结构示意图; Fig. 1 is the structural representation of the embodiment of the present invention;
图2是图1中间距调节机构的结构示意图; Fig. 2 is a structural schematic diagram of the distance adjusting mechanism in Fig. 1;
图3是图1中支座的结构示意图; Fig. 3 is a schematic structural view of the support in Fig. 1;
图4是图1中左支撑轮安装架的结构示意图; Fig. 4 is a schematic structural view of the left support wheel installation frame in Fig. 1;
图5是图1中右支撑轮安装架的结构示意图; Fig. 5 is a schematic structural view of the right support wheel mounting bracket in Fig. 1;
图6是图1中铰链支架的结构示意图; Fig. 6 is a schematic structural view of the hinge bracket in Fig. 1;
图7是图1中中心滚轮架的结构示意图; Fig. 7 is a schematic structural view of the center roller frame in Fig. 1;
图8是图1中转动臂的结构示意图; Fig. 8 is a structural schematic diagram of the rotating arm in Fig. 1;
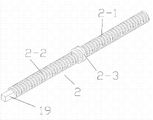
图9是图1中丝杠的结构示意图。 Fig. 9 is a schematic structural view of the lead screw in Fig. 1 . the
具体实施方式 Detailed ways
一种弧形零件弯形加工装置的实施例如图1~9所示:包括支座1,支座上设置有导向方向沿左右方向延伸的燕尾槽状的导轨18,导轨18中由左至右顺次设置有铰链支架13、左支撑轮安装架21、中心滚轮架5和右支撑轮安装架3,铰链支架13、左支撑轮安装架21、中心滚轮架5和右支撑轮安装架3的底部均设置有与导轨18适配导向配合的导轨配合部,其中铰链支架13和中心滚轮架5均通过相应的螺栓与支座1固定装配,左、右支撑轮安装架间设置有对其两者间间距进行调整的间距调节机构,间距调节机构包括设置于导轨18中的丝杠2,丝杠2的左、右两端分别设有旋向向反的左旋外螺纹2-1和右旋外螺纹2-2,左、右支撑轮安装架的导轨配合部上分别设有与左、右旋外螺纹旋合适配的左、右旋内螺纹。导轨18上于左、右旋外螺纹之间设置有用于实现丝杠2与支座1轴向限位配合的环形凹槽2-3,中心滚轮架5的导轨配合部为一板状结构5-1,中心滚轮架5的导轨配合部上设有开口朝下的U形槽5-2,U形槽5-2插装于丝杠2的环形凹槽2-3中,中心滚轮架5的板状结构的导轨配合部与环形凹槽2-3的槽壁限位配合而使丝杠2轴向移动被限位,丝杠2的右端设有用于与相应扳手配合以输入扭矩的外四方结构19,左、右支撑轮安装架上分别设置有导向方向沿左右方向延伸的左支撑轮安装架导向长孔16和右支撑轮安装架导向长孔17,支座1上分别设有与左、右支撑轮安装架导向长孔位置对应的左、右支撑轮安装架螺纹孔,左、右支撑轮安装架导向长孔与对应左、右支撑轮安装架螺纹孔中分别连接有对左、右支撑轮安装架进行固定锁紧的左支撑轮安装架螺栓14和右支撑轮安装架螺栓15。铰链支架13的导轨配合部上设有供丝杠2的左端贯穿的通孔23,中心滚轮架5的导轨配合部构成了对丝杠2轴向移动限位的限位板,这样转动丝杠2可带动左、右支撑轮安装架相对运动或相背运动,在左、右支撑轮安装架位置调整以后,可以通过左、右支撑轮安装架螺栓分别将左、右支撑轮安装架锁紧固定。铰链支架13铰接有转动轴线沿前后方向延伸的转动臂,转动臂包括与铰链支架13铰接相连的U形的转动架8和设置于转动架8的封闭端上的用于手持的加力杆9,加力杆9的左端与转动架8螺纹连接,转动架8的两侧壁上设置有导向方向与转动臂的延伸方向一致的转动臂导向长孔20,弯形装置还包括配合使用以完成对相应待弯零件滚压施工的并分别具有转轴的压轮7、左支撑轮12和右支撑轮4,压轮7的转轴10导向滚动装配于转动臂导向长孔20中,左支撑轮12转动装配于左支撑轮安装架21上,右支撑轮4转动装配于右支撑轮安装架3上,在对相应待弯零件22滚压施工时,左、右支撑轮分布于压轮7的左、右两侧,左、右支撑轮具有用于与相应待弯零件的被弯部分两端滚动撑托配合的外周面,左、右支撑轮的外周面上设有与相应待弯零件22的外周弧面适配的环形凹槽,压轮7具有在随所述转动臂由上至下翻转时与相应待弯零件的被弯部分中部滚压配合而使待弯零件的被弯部分中部下凹变形的外周面,压轮7的外周面上也设有与相应待弯零件的外周弧面适配的环形凹槽。中心滚轮架5上设置有导向方向沿上下方向延伸并用于在压轮对相应待弯零件滚压成型时与压轮的转轴导向配合的竖向导向机构,竖向导向机构包括槽深沿上下方向延伸的十字槽,十字槽由沿左右方向延伸以供所述压轮7由上至下通过的横槽5-3和沿前后方向延伸的竖槽5-4构成,所述的竖槽5-4具有导向方向沿上下方向延伸以实现竖向导向机构与压轮7的转轴10两端导向配合的槽壁,竖槽的槽口呈上端口径大、下端口径小的缩口状。铰链支架13上螺纹连接有轴向沿左右方向延伸的定位螺杆6,定位螺杆6的右端具有用于与相应待弯零件22的左端端面挡止定位配合的定位端面。
An embodiment of an arc-shaped part bending processing device is shown in Figures 1 to 9: it includes a support 1, and the support is provided with a dovetail-
使用时,先将丝杠9上的环形凹槽2-3放到中心滚轮架5上的U形槽5-2里,再将上述装配体装配到支座1的导轨18中,具体装配是通过中心滚轮架5的导轨配合部与导轨的燕尾槽配合,用螺栓将中心滚轮架5固定于支座1上,将左、右支撑轮安装架装配到丝杠2的对应端,丝杠2转动可调整左、右支撑轮安装架间的间距。将铰链支架13安装于导轨18中,并通过相应螺栓使铰链支架13与支座1固定装配,同时将定位螺杆6旋入铰链支架13上,下翻转动架,根据待弯零件尺寸旋转丝杠对左、右支撑轮安装架位置进行调整,直到左支撑轮12的外缘与压轮7的外缘接触,用左、右支撑轮安装架螺栓将对应支撑轮安装架锁紧固定。将待弯零件的两端放置在左、右支撑轮上,调整定位螺杆到所需位置,使待弯零件的左端与定位螺杆的定位端面接触。用力下压加力杆,根据杠杆原理,压轮会对待弯零件的中部产生较大压力,待弯零件在压轮和左、右支撑轮的限位施压下,按照预定轨道向下移动,最终成型。如果待弯零件的所需弯角小于180??,则可改变加力杆的下压位置,加力杆可根据待弯零件不同而选择更换,加力杆的长度越长,待弯零件越容易成形。因在对U形零件的弯形加工过程中,转动臂在由上至下的摆动过程中,转动臂与水平方向夹角在不断变化,而压轮只能上下移动,根据余弦定理,水平边不变情况下,转动臂的转轴与压轮的转轴之间的间距在不变变化,故有转动臂导向长孔20和竖向导向机构的制作,竖向以满足压轮的转轴在转动臂导向长孔20内的移动,在压轮7的转轴10与竖向导向机构滚动导向配合后,压轮只能沿上下方向移动,从而满足对标准U形零件的弯形加工;针对尺寸不同的待弯零件,压轮需要进行更换,且压轮上的环形凹槽的半径与待弯零件的半径一致,保证尺寸的准确性,即使弯制管类零件也不会使管子被压扁。
When in use, first put the annular groove 2-3 on the
在本发明的其它实施例中,当只对一个类型的待弯零件进行加工时,左、右支撑轮安装架间的间距是可以固定不变的,此时左、右支撑轮安装架可以一体设置,左、右支撑轮安装架可以与支座一体设置,当然支座上的导轨也可以不设;通过丝杠调整,保证了左、右支撑轮安装架间位置调整的连续性,当然丝杠也可以不设,可以直接通过左、右支撑轮安装架导向长孔对左、右支撑轮安装架进行位置调整;加力杆也可以与转动架焊接固连或一体设置;当使用本加工装置对一些非U形标准件进行加工时,比如说对不标准的C形零件进行弯形加工时,竖向导向机构和转动臂导向长孔均可以没有,此时将压轮直接转动装配于转动臂上。 In other embodiments of the present invention, when only one type of parts to be bent is processed, the distance between the left and right support wheel mounting frames can be fixed, and now the left and right support wheel mounting frames can be integrated Setting, the left and right support wheel mounting brackets can be integrated with the support, of course, the guide rail on the support can also be omitted; through the adjustment of the screw, the continuity of the position adjustment between the left and right support wheel mounting brackets is guaranteed. The bar can also be omitted, and the position of the left and right supporting wheel mounting frames can be adjusted directly through the guide slots of the left and right supporting wheel mounting frames; When the device processes some non-U-shaped standard parts, for example, when bending non-standard C-shaped parts, the vertical guide mechanism and the long guide hole of the rotating arm can be omitted. At this time, the pressure roller can be directly rotated and assembled on the Turn on the arm.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210348902.5A CN102886407B (en) | 2012-09-19 | 2012-09-19 | bending and machining device for arc-shaped part |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210348902.5A CN102886407B (en) | 2012-09-19 | 2012-09-19 | bending and machining device for arc-shaped part |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN102886407A true CN102886407A (en) | 2013-01-23 |
| CN102886407B CN102886407B (en) | 2014-12-10 |
Family
ID=47530200
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201210348902.5A Active CN102886407B (en) | 2012-09-19 | 2012-09-19 | bending and machining device for arc-shaped part |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102886407B (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103143866A (en) * | 2013-04-02 | 2013-06-12 | 国家电网公司 | Dedicated portable welding table for machine room |
| CN105458111A (en) * | 2016-01-25 | 2016-04-06 | 珠海格力电器股份有限公司 | Automatic material receiving device with hinge structure and method |
| CN108994227A (en) * | 2018-09-11 | 2018-12-14 | 苏州迈道纳自动化科技有限公司 | Decorative pattern spline rolls seat |
Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0910851A (en) * | 1995-06-26 | 1997-01-14 | Yuji Otsubo | Reinforcing bar bender |
| EP0990471A1 (en) * | 1998-09-30 | 2000-04-05 | FABBRICA MACCHINE CURVATUBI CRIPPA AGOSTINO S.p.A. | Bending machine |
| CN2491146Y (en) * | 2001-07-12 | 2002-05-15 | 余波 | Push-pull roller type cold bender |
| CN2590693Y (en) * | 2002-10-17 | 2003-12-10 | 张亚成 | Section bar bending machine |
| CN201455062U (en) * | 2009-07-30 | 2010-05-12 | 宝鸡石油机械有限责任公司 | Lifting ring simmering device |
| CN201768787U (en) * | 2010-08-12 | 2011-03-23 | 天津二十冶建设有限公司 | Bending device of metal section |
| CN102179435A (en) * | 2011-03-30 | 2011-09-14 | 陕西科技大学 | Device and method for bending variable-curvature pipe |
| CN202199639U (en) * | 2011-07-15 | 2012-04-25 | 天津曹氏传动机械制造有限公司 | Improve tubular product bender of extrusion effect |
| CN202199640U (en) * | 2011-07-15 | 2012-04-25 | 天津曹氏传动机械制造有限公司 | Antifriction's vertical bender |
| CN202224485U (en) * | 2011-09-05 | 2012-05-23 | 山东金宝电子股份有限公司 | Hand-operated pipe bending apparatus |
| CN202845522U (en) * | 2012-09-19 | 2013-04-03 | 河南平高电气股份有限公司 | Bending shape machining device for arc-shaped parts |
-
2012
- 2012-09-19 CN CN201210348902.5A patent/CN102886407B/en active Active
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0910851A (en) * | 1995-06-26 | 1997-01-14 | Yuji Otsubo | Reinforcing bar bender |
| EP0990471A1 (en) * | 1998-09-30 | 2000-04-05 | FABBRICA MACCHINE CURVATUBI CRIPPA AGOSTINO S.p.A. | Bending machine |
| CN2491146Y (en) * | 2001-07-12 | 2002-05-15 | 余波 | Push-pull roller type cold bender |
| CN2590693Y (en) * | 2002-10-17 | 2003-12-10 | 张亚成 | Section bar bending machine |
| CN201455062U (en) * | 2009-07-30 | 2010-05-12 | 宝鸡石油机械有限责任公司 | Lifting ring simmering device |
| CN201768787U (en) * | 2010-08-12 | 2011-03-23 | 天津二十冶建设有限公司 | Bending device of metal section |
| CN102179435A (en) * | 2011-03-30 | 2011-09-14 | 陕西科技大学 | Device and method for bending variable-curvature pipe |
| CN202199639U (en) * | 2011-07-15 | 2012-04-25 | 天津曹氏传动机械制造有限公司 | Improve tubular product bender of extrusion effect |
| CN202199640U (en) * | 2011-07-15 | 2012-04-25 | 天津曹氏传动机械制造有限公司 | Antifriction's vertical bender |
| CN202224485U (en) * | 2011-09-05 | 2012-05-23 | 山东金宝电子股份有限公司 | Hand-operated pipe bending apparatus |
| CN202845522U (en) * | 2012-09-19 | 2013-04-03 | 河南平高电气股份有限公司 | Bending shape machining device for arc-shaped parts |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103143866A (en) * | 2013-04-02 | 2013-06-12 | 国家电网公司 | Dedicated portable welding table for machine room |
| CN105458111A (en) * | 2016-01-25 | 2016-04-06 | 珠海格力电器股份有限公司 | Automatic material receiving device with hinge structure and method |
| CN108994227A (en) * | 2018-09-11 | 2018-12-14 | 苏州迈道纳自动化科技有限公司 | Decorative pattern spline rolls seat |
| CN108994227B (en) * | 2018-09-11 | 2024-05-17 | 苏州迈道纳自动化科技有限公司 | Patterned spline rolling seat |
Also Published As
| Publication number | Publication date |
|---|---|
| CN102886407B (en) | 2014-12-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103331992B (en) | A kind of tension control mechanism of printing machine cloth | |
| CN102886407B (en) | bending and machining device for arc-shaped part | |
| EP2711100B1 (en) | Rolling mill bearing chock positioning device | |
| CN101983788A (en) | Roll angle adjustable multi-roll flexible roll bending forming calibrating device | |
| CN107716628B (en) | Rebound control device for high-strength steel cold-formed product piece | |
| CN202845522U (en) | Bending shape machining device for arc-shaped parts | |
| CN112570460B (en) | An adjustable device for metal rolling | |
| CN208575122U (en) | A kind of spheronizator | |
| CN105798068A (en) | Roll axial adjustment mechanism | |
| CN110814091A (en) | Leveling machine for producing double-shaft tracking photovoltaic support | |
| KR101530820B1 (en) | The rolling device of hose-band | |
| CN212598131U (en) | I-steel cold bending machine | |
| CN210280305U (en) | A pipe bending machine with good bending effect | |
| CN222725180U (en) | Multi-angle positioning bending machine for metal plate processing | |
| CN209349315U (en) | Tuber strip center pre-profiling mechanism | |
| CN204307969U (en) | Compression roller device in a kind of Straight-weld pipe mill | |
| CN201644522U (en) | Deformed steel bar bending preventive device | |
| CN223491745U (en) | Multi-roller adjustable online shaping device for aluminum profile | |
| CN1229193C (en) | United corner jointing machine | |
| CN219840645U (en) | Side rolling prevention device for shield tunneling machine | |
| CN106914492B (en) | A kind of extruding roller arrangement and rolling machine equipment | |
| CN220687126U (en) | Bolt moving assembly | |
| CN224253930U (en) | A plate rolling machine with plate alignment function | |
| CN214348887U (en) | A kind of purification board automatic crimping equipment | |
| CN221312287U (en) | Reinforcing bar straightener |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C53 | Correction of patent of invention or patent application | ||
| CB02 | Change of applicant information |
Address after: South East of Pingdingshan city in Henan province 467001 No. 22 Applicant after: Pinggao Electric Co., Ltd., Henan Applicant after: Pinggao Group Co., Ltd. Applicant after: State Grid Corporation of China Address before: South East of Pingdingshan city in Henan province 467001 No. 23 Applicant before: Pinggao Electric Co., Ltd., Henan Applicant before: Pinggao Group Co., Ltd. Applicant before: State Grid Corporation of China |
|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant |