CN102825518A - Side polisher for rectangular workpiece - Google Patents
Side polisher for rectangular workpiece Download PDFInfo
- Publication number
- CN102825518A CN102825518A CN2012103076179A CN201210307617A CN102825518A CN 102825518 A CN102825518 A CN 102825518A CN 2012103076179 A CN2012103076179 A CN 2012103076179A CN 201210307617 A CN201210307617 A CN 201210307617A CN 102825518 A CN102825518 A CN 102825518A
- Authority
- CN
- China
- Prior art keywords
- grinding
- head
- flange
- fixed mount
- revolute pair
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 230000005540 biological transmission Effects 0.000 claims abstract description 3
- 230000000007 visual effect Effects 0.000 claims 1
- 230000006835 compression Effects 0.000 abstract description 8
- 238000007906 compression Methods 0.000 abstract description 8
- 238000004519 manufacturing process Methods 0.000 description 9
- 238000010586 diagram Methods 0.000 description 8
- 238000000034 method Methods 0.000 description 5
- 238000003825 pressing Methods 0.000 description 5
- 239000002184 metal Substances 0.000 description 2
- 238000005498 polishing Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000002347 injection Methods 0.000 description 1
- 239000007924 injection Substances 0.000 description 1
- 230000001788 irregular Effects 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 238000010422 painting Methods 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
Images


Landscapes
- Grinding And Polishing Of Tertiary Curved Surfaces And Surfaces With Complex Shapes (AREA)
Abstract
一种长方形工件侧边打磨机,包括输送装置和打磨装置,输送装置由包含机架(1)、输送带(2)的输送线一(I)、输送线二(II)以及升降转向台(12)组成,输送线一(I)通过升降转向台(12)与输送线二(II)连接;打磨装置包括固定架(4)、打磨头(5)、主臂(6)、辅杆(7)、摇杆(10)、法兰(8)、压紧头(9)、定位块(11),主臂(6)与固定架(4)以转动副一(E)连接后,又以球副(F)连接辅杆(7)的一端,辅杆(7)另一端的丝杆部分又与固定在摇杆(10)一端的螺母(G)构成丝杆螺纹传动,而摇杆(10)的另一端与固定架(4)以转动副二(D)连接,打磨头(5)通过法兰(8)连接在主臂(6)的末端;长方形工件(3)在放置于对称两侧的输送带(2)的定位块(11)上定位后,再用压紧头(9)压紧。该打磨机结构简单、易于控制,适应性好,自动化程度高,打磨质量好。
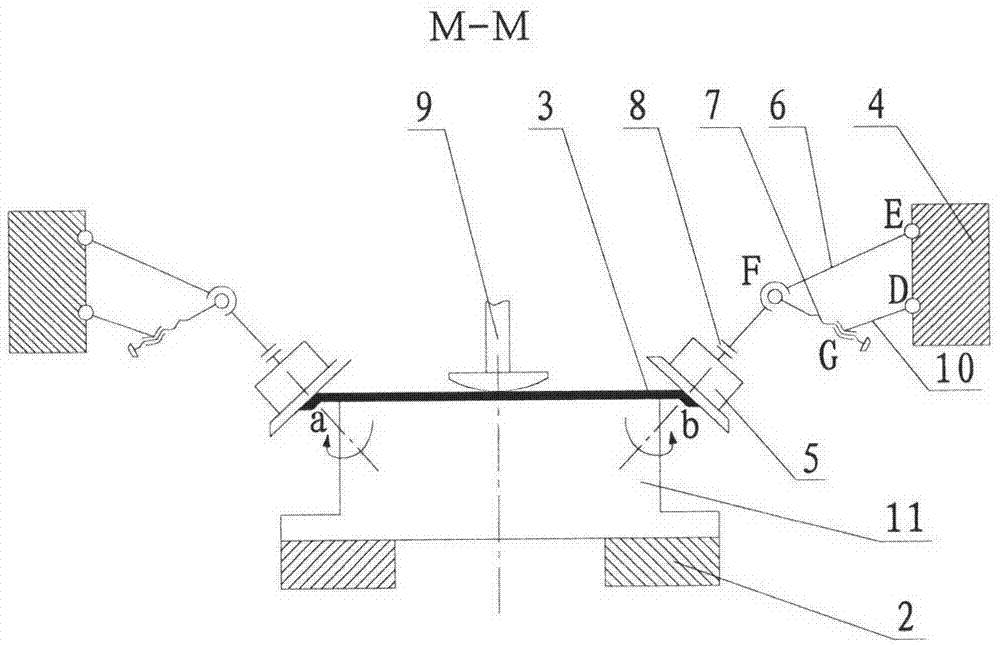
A side grinding machine for a rectangular workpiece, comprising a conveying device and a grinding device, the conveying device consists of a conveying line one (I), a conveying line two (II) comprising a frame (1), a conveying belt (2), and a lift steering platform ( 12) composition, conveying line one (I) is connected with conveying line two (II) through lifting steering table (12); grinding device comprises fixed frame (4), grinding head (5), main arm (6), auxiliary bar ( 7), the rocker (10), the flange (8), the compression head (9), the positioning block (11), the main arm (6) and the fixed frame (4) are connected by the rotation pair one (E), and then A ball pair (F) is used to connect one end of the auxiliary rod (7), and the screw part at the other end of the auxiliary rod (7) forms a screw thread transmission with the nut (G) fixed at one end of the rocker (10), and the rocker The other end of (10) is connected with fixed frame (4) with rotating pair two (D), and grinding head (5) is connected on the end of main arm (6) by flange (8); Rectangular workpiece (3) is placed on After positioning on the positioning block (11) of the conveyor belt (2) on both sides of the symmetry, use the compression head (9) to compress again. The grinding machine has simple structure, easy control, good adaptability, high degree of automation and good grinding quality.
Description
技术领域 technical field
本发明主要涉及长方形工件的侧边或倒角的打磨,具体地说是为笔记本电脑外壳等长方形工件的侧边或倒角的抛光和打磨,提供一种高效的流水线作业方式的打磨机。The invention mainly relates to the grinding of the sides or chamfers of rectangular workpieces, and in particular provides an efficient assembly line grinding machine for the polishing and grinding of the sides or chamfers of rectangular workpieces such as notebook computer casings.
背景技术 Background technique
长方形工件,例:通过注塑成型的笔记本电脑外壳、金属钣金或结构件、铸件等,制造过程中其边边角角必定会出现毛刺,这对后道工序,例:工件表面的油漆喷涂会带来一定影响。因此,打磨工序极其必要,打磨质量的好坏,直接影响到后续工序是否能够顺利进行,以及产品的最终质量。Rectangular workpieces, such as: laptop casings, metal sheet metal or structural parts, castings, etc., which are molded by injection, will inevitably have burrs on the corners and corners during the manufacturing process. have a certain impact. Therefore, the grinding process is extremely necessary, and the quality of the grinding directly affects whether the subsequent process can be carried out smoothly and the final quality of the product.
根据作业方式的不同,可将打磨分为手工打磨和机器打磨。目前,对于不规则曲面造型的表面,一般采用手工打磨,它比机器打磨效率低、质量差、劳动力消耗大;对于较为平整、面积较大的表面,一般用通用机器人来进行打磨,因此,在大批量的生产过程中,为节约生产成本,提高打磨质量,常采用自动化机器人进行打磨。但对于长方形工件的侧边或倒角的打磨,如采用通用机器人来打磨,则成本高,打磨效率也低,为此,急需一种高效的自动化打磨专用装置。According to different operation methods, grinding can be divided into manual grinding and machine grinding. At present, for surfaces with irregular curved surfaces, manual grinding is generally used, which is less efficient, poorer in quality, and more labor-intensive than machine grinding; for relatively flat and large-area surfaces, general-purpose robots are generally used for grinding. Therefore, in In the mass production process, in order to save production costs and improve the quality of grinding, automatic robots are often used for grinding. However, for the grinding of the side or chamfer of the rectangular workpiece, if a general-purpose robot is used for grinding, the cost is high and the grinding efficiency is low. Therefore, an efficient automatic grinding special device is urgently needed.
发明内容 Contents of the invention
为解决上述问题,本发明提供了一种长方形工件侧边、倒角打磨的自动化流水线作业装置,提高了工作效率和产品的质量,大大降低了劳动力生产成本。In order to solve the above problems, the present invention provides an automatic assembly line operation device for grinding the sides and chamfers of rectangular workpieces, which improves work efficiency and product quality, and greatly reduces labor production costs.
本发明所采用的技术方案是:一种长方形工件侧边打磨机,包括输送装置和打磨装置,输送装置由均包含机架(1)、输送带(2)的输送线一(I)、输送线二(II)以及升降转向台(12)组成,输送线一(I)通过升降转向台(12)与输送线二(II)连接,打磨装置(III)布置于输送线一(I)、输送线二(II)的上方;第一种打磨装置包括固定架(4)、打磨头(5)、主臂(6)、辅杆(7)、摇杆(10)、法兰(8)、压紧头(9)、定位块(11),主臂(6)与固定架(4)以转动副一(E)连接后,又以球副(F)连接辅杆(7)的一端,辅杆(7)另一端的丝杆部分又与固定在摇杆(10)一端的螺母(G)构成丝杆螺纹传动,而摇杆(10)的另一端与固定架(4)以转动副二(D)连接,打磨头(5)通过法兰(8)连接在主臂(6)的末端;长方形工件(3)在放置于对称两侧的输送带(2)的定位块(11)上定位后,再用压紧头(9)压紧。The technical scheme that the present invention adopts is: a kind of rectangular workpiece side grinding machine, comprises conveying device and grinding device, and conveying device is made of conveying line one (1) that all comprises frame (1), conveyor belt (2), conveying Line two (II) and the lifting steering platform (12), the conveying line one (I) is connected with the conveying line two (II) through the lifting and turning platform (12), and the grinding device (III) is arranged on the conveying line one (I), Above the conveyor line II (II); the first type of grinding device includes a fixed frame (4), a grinding head (5), a main arm (6), an auxiliary rod (7), a rocker (10), and a flange (8) , compression head (9), positioning block (11), after the main arm (6) is connected with the fixed frame (4) with the rotation pair one (E), connect one end of the auxiliary rod (7) with the ball pair (F) , the screw part at the other end of the auxiliary rod (7) and the nut (G) fixed at one end of the rocker (10) form a screw thread transmission, and the other end of the rocker (10) and the fixed frame (4) can rotate Secondary (D) connection, the grinding head (5) is connected to the end of the main arm (6) through the flange (8); the rectangular workpiece (3) is placed on the positioning block (11) of the conveyor belt (2) on both sides of the symmetry ) and then press it with the compression head (9).
第二种打磨装置包括固定架(4)、打磨头(5)、主臂(6)、辅杆(7)、滑块(13)、法兰(8)、压紧头(9)、定位块(11),主臂(6)与固定架(4)以转动副一(E)连接后,又以转动副二(F)连接辅杆(7)的一端,辅杆(7)的另一端以转动副三(G)连接滑块(13),而滑块(13)与固定架(4)构成移动副(P);打磨头(5)通过法兰(8)连接在主臂(6)的末端;长方形工件(3)在放置于对称两侧的输送带(2)的定位块(11)上定位后,再用压紧头(9)压紧。The second type of grinding device includes a fixed frame (4), a grinding head (5), a main arm (6), an auxiliary rod (7), a slider (13), a flange (8), a pressing head (9), a positioning Block (11), after main arm (6) and fixed mount (4) are connected with swivel pair one (E), connect an end of auxiliary rod (7) with swivel pair two (F) again, the other end of auxiliary rod (7) One end is connected with the sliding block (13) by the rotating pair three (G), and the sliding block (13) and the fixed frame (4) constitute the moving pair (P); the grinding head (5) is connected to the main arm ( 6) at the end; after the rectangular workpiece (3) is positioned on the positioning block (11) of the conveyor belt (2) placed on both sides of the symmetry, it is compressed with the compression head (9).
第三种打磨装置包括固定架(4)、打磨头(5)、主臂(6)、辅杆(7)、摇杆(14)、法兰(8)、压紧头(9)、定位块(11),主臂(6)与固定架(4)以转动副一(E)连接后,又以转动副二(F)连接辅杆(7)的一端,辅杆(7)的另一端以转动副三(G)连接摇杆(14)的一端,而摇杆(14)的另一端与固定架(4)再用转动副四(M)连接;打磨头(5)通过法兰(8)连接在主臂(6)末端;长方形工件(3)在放置于对称两侧的输送带(2)的定位块(11)上定位后,再用压紧头(9)压紧。The third grinding device includes a fixed frame (4), a grinding head (5), a main arm (6), an auxiliary rod (7), a rocker (14), a flange (8), a pressing head (9), a positioning Block (11), after main arm (6) and fixed mount (4) are connected with swivel pair one (E), connect an end of auxiliary rod (7) with swivel pair two (F) again, the other end of auxiliary rod (7) One end is connected to one end of the rocker (14) with the third rotating pair (G), and the other end of the rocker (14) is connected to the fixed frame (4) with the fourth rotating pair (M); the grinding head (5) passes through the flange (8) be connected at main arm (6) end; Rectangular workpiece (3) compresses with compression head (9) after positioning on the positioning block (11) of the conveyer belt (2) that is placed on symmetrical both sides.
进一步,上述三种长方形工件侧边打磨机中,输送线一(I)、输送线二(II)左右两侧的打磨装置结构相同,两个打磨头(5)中心点之间的距离(ab)可视长方形工件的长宽比不同而不同。Further, in the above-mentioned three kinds of side grinding machines for rectangular workpieces, the grinding devices on the left and right sides of conveyor line one (I) and conveyor line two (II) have the same structure, and the distance between the center points of the two grinding heads (5) (ab ) can vary depending on the aspect ratio of the rectangular workpiece.
本发明所起到的有益效果:本发明与现有技术相比,具有以下优点和优势:(1)经本装置打磨后,工件打磨均匀,去毛刺效果明显;(2)通过本装置的流水线生产增强了打磨作业的连续性,使得加工效率和质量大大提高。(3)可以直接把打磨流水线接到喷房进行后工序喷漆作业,真正实现自动化生产。(4)相对于手工打磨而言,可以有效地节约工人的使用量,缩短工时,降低了成本。Beneficial effects of the present invention: Compared with the prior art, the present invention has the following advantages and advantages: (1) after being polished by the device, the workpiece is polished evenly, and the deburring effect is obvious; (2) through the assembly line of the device Production enhances the continuity of grinding operations, greatly improving processing efficiency and quality. (3) The polishing line can be directly connected to the spray booth for post-process painting operations, truly realizing automatic production. (4) Compared with manual grinding, it can effectively save the amount of workers used, shorten the working hours and reduce the cost.
附图说明Description of drawings
附图1是本发明的生产流水线示意图。Accompanying
附图2是本发明的第一种打磨装置原理示意图。Accompanying
附图3是本发明的第二种打磨装置原理示意图。Accompanying
附图4是本发明的第三种打磨装置原理示意图。Accompanying
具体实施方式 Detailed ways
下面结合附图及实施例进一步阐述本发明。The present invention will be further described below in conjunction with the accompanying drawings and embodiments.
附图1是本发明生产流水线的一种实施例示意图。其技术方案是:一种长方形工件侧边打磨机,包括输送装置和打磨装置,输送装置由均包含机架1、输送带2的输送线一I、输送线二II以及升降转向台12组成,输送线一I通过升降转向台12与输送线二II连接,打磨装置III布置于输送线一I、输送线二II的上方。Accompanying
附图2是本发明的第一种打磨装置原理示意图,它包括固定架4、打磨头5、主臂6、辅杆7、摇杆10、法兰8、压紧头9、定位块11,主臂6与固定架4以转动副一E连接后,又以球副F连接辅杆7的一端,辅杆7另一端的丝杆部分又与固定在摇杆10一端的螺母G构成丝杆螺纹传动,而摇杆10的另一端与固定架4以转动副二D连接,打磨头5通过法兰8连接在主臂6的末端;长方形工件3在放置于对称两侧的输送带2的定位块11上定位后,再用压紧头9压紧。Accompanying
附图3是本发明的第二种打磨装置原理示意图,它包括固定架4、打磨头5、主臂6、辅杆7、滑块13、法兰8、压紧头9、定位块11,主臂6与固定架4以转动副一E连接后,又以转动副二F连接辅杆7的一端,辅杆7的另一端以转动副三G连接滑块13,而滑块13与固定架4构成移动副P;打磨头5通过法兰8连接在主臂6的末端;长方形工件3在放置于对称两侧的输送带2的定位块11上定位后,再用压紧头9压紧。Accompanying
附图4是本发明的第三种打磨装置原理示意图,它包括固定架4、打磨头5、主臂6、辅杆7、摇杆14、法兰8、压紧头9、定位块11,主臂6与固定架4以转动副一E连接后,又以转动副二F连接辅杆7的一端,辅杆7的另一端以转动副三G连接摇杆14的一端,而摇杆14的另一端与固定架4再用转动副四M连接;打磨头5通过法兰8连接在主臂6末端;长方形工件3在放置于对称两侧的输送带2的定位块11上定位后,再用压紧头9压紧。Accompanying
进一步,上述三种长方形工件侧边打磨机中,输送线一I、输送线二II左右两侧的打磨装置结构相同,两个打磨头5中心点之间的距离ab可视长方形工件的长宽比不同而不同。Further, in the above-mentioned three kinds of side grinding machines for rectangular workpieces, the grinding devices on the left and right sides of conveyor line I and conveyor line II have the same structure, and the distance ab between the center points of the two
工作原理:需要打磨测边或倒角的长方形工件3,通过输送线一I上的输送带2传送到A位置,进行纵向二侧边的打磨,完成后通过传送带2输送到B位置,在该位置上通过升降转向台12将长方形工件3落到输送线二II的输送带2上,运行到C位置进行宽向二侧边的打磨。这样,就完成了四条边的打磨。如需提高工件测边或倒角的打磨精度要求,可适当增加打磨头的数量、打磨的次数或输送带2的输送速度。Working principle: The
进一步,在第一、第二、第三种打磨装置中,对不同角度的倒角或侧边,可分别通过转动辅杆7的丝杆螺纹、改变滑块13的位置、摆动摇杆14的位置来调节打磨头5的姿态,以实现不同加工件的打磨加工要求。Further, in the first, second, and third grinding devices, for chamfering or side edges at different angles, the screw thread of the
这种长方形工件侧边打磨机结构简单、制造容易,控制方便,可保证打磨量均匀、打磨效率高,长方形工件侧边打磨、倒角适应性好。The side grinding machine for a rectangular workpiece has a simple structure, is easy to manufacture, and is convenient to control, can ensure uniform grinding amount, high grinding efficiency, and has good adaptability for grinding and chamfering the side of a rectangular workpiece.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012103076179A CN102825518A (en) | 2012-08-23 | 2012-08-23 | Side polisher for rectangular workpiece |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012103076179A CN102825518A (en) | 2012-08-23 | 2012-08-23 | Side polisher for rectangular workpiece |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN102825518A true CN102825518A (en) | 2012-12-19 |
Family
ID=47328937
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012103076179A Pending CN102825518A (en) | 2012-08-23 | 2012-08-23 | Side polisher for rectangular workpiece |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102825518A (en) |
Cited By (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104589175A (en) * | 2014-11-26 | 2015-05-06 | 安庆潜山永大木业有限公司 | Sliding plate face edge polishing machine |
| CN105033802A (en) * | 2015-07-25 | 2015-11-11 | 安徽卡塔门窗有限公司 | Multi-dimensionally adjustable deburring device for window frames |
| CN105922101A (en) * | 2016-06-20 | 2016-09-07 | 苏州华徕光电仪器有限公司 | Polishing device used for lens |
| CN107225462A (en) * | 2017-05-05 | 2017-10-03 | 广州市奇虎实业有限公司 | A kind of polishing machine of automatic removing burr |
| CN107617961A (en) * | 2017-10-19 | 2018-01-23 | 德清县凌鹰电器有限公司 | Grinding workpieces equipment |
| CN108340272A (en) * | 2018-02-02 | 2018-07-31 | 深圳市嘉力强电子设备有限公司 | A kind of full-automatic sanding line of automatic charging, automatically grinding, self-emptying |
| CN108406533A (en) * | 2018-04-26 | 2018-08-17 | 黄山市古城歙砚有限公司 | One kind inhaling inkstone and produces adjustable grinding device |
| CN110509150A (en) * | 2019-08-06 | 2019-11-29 | 嘉兴学院 | A chain plate transmission and grinding machine |
| CN110919509A (en) * | 2019-11-26 | 2020-03-27 | 安徽枫雅轩科技信息服务有限公司 | Shifting fork rod double-end chamfering device |
| CN111300233A (en) * | 2020-03-17 | 2020-06-19 | 陈紫璇 | Precision grinding machine for double end faces of workpiece |
| CN112171414A (en) * | 2020-08-29 | 2021-01-05 | 盐城工学院 | Grooving line chamfering and deburring equipment |
| CN113231694A (en) * | 2021-06-04 | 2021-08-10 | 邵东智能制造技术研究院有限公司 | Workpiece groove machining and polishing equipment |
| CN114311170A (en) * | 2022-01-20 | 2022-04-12 | 佛山市顺德区佳顺隆机械有限公司 | Octagonal milling production line |
| CN115256095A (en) * | 2022-09-26 | 2022-11-01 | 安徽新境界自动化技术有限公司 | An intelligent compensation system for grinding errors based on multi-sensor fusion |
| CN117600952A (en) * | 2024-01-23 | 2024-02-27 | 常州凯旺金属材料有限公司 | Stainless steel high-hardness high-wear-resistance machining device and machining process thereof |
| CN118663863A (en) * | 2024-07-01 | 2024-09-20 | 安徽恒龙光电科技有限公司 | Notebook backboard die casting die capable of removing edge burrs |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2675786A1 (en) * | 1991-04-29 | 1992-10-30 | Heitz Maurice | Device for pivoting panels or similar square or rectangular articles passing by in a manufacturing line |
| CN2902570Y (en) * | 2005-11-03 | 2007-05-23 | 佛山市汉诺普机械有限公司 | All drying type edger |
| CN201324999Y (en) * | 2008-11-17 | 2009-10-14 | 广东科达机电股份有限公司 | Polishing production line of ceramic ultra-large ultra-thin sheet |
| CN101941167A (en) * | 2009-07-08 | 2011-01-12 | 王文庭 | Automatic edging device |
| CN102310348A (en) * | 2010-07-07 | 2012-01-11 | 马安 | Structure of novel polishing machine |
-
2012
- 2012-08-23 CN CN2012103076179A patent/CN102825518A/en active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2675786A1 (en) * | 1991-04-29 | 1992-10-30 | Heitz Maurice | Device for pivoting panels or similar square or rectangular articles passing by in a manufacturing line |
| CN2902570Y (en) * | 2005-11-03 | 2007-05-23 | 佛山市汉诺普机械有限公司 | All drying type edger |
| CN201324999Y (en) * | 2008-11-17 | 2009-10-14 | 广东科达机电股份有限公司 | Polishing production line of ceramic ultra-large ultra-thin sheet |
| CN101941167A (en) * | 2009-07-08 | 2011-01-12 | 王文庭 | Automatic edging device |
| CN102310348A (en) * | 2010-07-07 | 2012-01-11 | 马安 | Structure of novel polishing machine |
Non-Patent Citations (1)
| Title |
|---|
| 邓小明: "磨边机磨边对角线误差分析", 《佛山陶瓷》, vol. 15, no. 12, 31 December 2005 (2005-12-31) * |
Cited By (22)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104589175A (en) * | 2014-11-26 | 2015-05-06 | 安庆潜山永大木业有限公司 | Sliding plate face edge polishing machine |
| CN105033802A (en) * | 2015-07-25 | 2015-11-11 | 安徽卡塔门窗有限公司 | Multi-dimensionally adjustable deburring device for window frames |
| CN105922101A (en) * | 2016-06-20 | 2016-09-07 | 苏州华徕光电仪器有限公司 | Polishing device used for lens |
| CN107225462A (en) * | 2017-05-05 | 2017-10-03 | 广州市奇虎实业有限公司 | A kind of polishing machine of automatic removing burr |
| CN107617961A (en) * | 2017-10-19 | 2018-01-23 | 德清县凌鹰电器有限公司 | Grinding workpieces equipment |
| CN107617961B (en) * | 2017-10-19 | 2024-04-12 | 浦江求精五金工具有限公司 | Workpiece polishing equipment |
| CN108340272A (en) * | 2018-02-02 | 2018-07-31 | 深圳市嘉力强电子设备有限公司 | A kind of full-automatic sanding line of automatic charging, automatically grinding, self-emptying |
| CN108340272B (en) * | 2018-02-02 | 2024-03-15 | 深圳市嘉力强电子设备有限公司 | Automatic feeding, automatic polishing and automatic discharging full-automatic polishing line |
| CN108406533A (en) * | 2018-04-26 | 2018-08-17 | 黄山市古城歙砚有限公司 | One kind inhaling inkstone and produces adjustable grinding device |
| CN108406533B (en) * | 2018-04-26 | 2023-08-15 | 黄山市古城歙砚有限公司 | Adjustable polishing device for she inkstone production |
| CN110509150A (en) * | 2019-08-06 | 2019-11-29 | 嘉兴学院 | A chain plate transmission and grinding machine |
| CN110919509A (en) * | 2019-11-26 | 2020-03-27 | 安徽枫雅轩科技信息服务有限公司 | Shifting fork rod double-end chamfering device |
| CN111300233A (en) * | 2020-03-17 | 2020-06-19 | 陈紫璇 | Precision grinding machine for double end faces of workpiece |
| CN111300233B (en) * | 2020-03-17 | 2021-06-18 | 东台市双厦工具有限公司 | Precision grinding machine for double end faces of workpiece |
| CN112171414A (en) * | 2020-08-29 | 2021-01-05 | 盐城工学院 | Grooving line chamfering and deburring equipment |
| CN113231694B (en) * | 2021-06-04 | 2022-09-16 | 邵东智能制造技术研究院有限公司 | Workpiece groove machining and polishing equipment |
| CN113231694A (en) * | 2021-06-04 | 2021-08-10 | 邵东智能制造技术研究院有限公司 | Workpiece groove machining and polishing equipment |
| CN114311170A (en) * | 2022-01-20 | 2022-04-12 | 佛山市顺德区佳顺隆机械有限公司 | Octagonal milling production line |
| CN115256095A (en) * | 2022-09-26 | 2022-11-01 | 安徽新境界自动化技术有限公司 | An intelligent compensation system for grinding errors based on multi-sensor fusion |
| CN117600952A (en) * | 2024-01-23 | 2024-02-27 | 常州凯旺金属材料有限公司 | Stainless steel high-hardness high-wear-resistance machining device and machining process thereof |
| CN117600952B (en) * | 2024-01-23 | 2024-03-19 | 常州凯旺金属材料有限公司 | Stainless steel high-hardness high-wear-resistance machining device and machining process thereof |
| CN118663863A (en) * | 2024-07-01 | 2024-09-20 | 安徽恒龙光电科技有限公司 | Notebook backboard die casting die capable of removing edge burrs |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105538111B (en) | Automatic grinding and polishing device and processing method thereof | |
| CN208179225U (en) | A kind of tup grinding apparatus of carrying machine people | |
| CN204603995U (en) | Conveyor Belt Grinder | |
| CN206855197U (en) | A kind of conveyer belt type equipment for grinding | |
| CN206277233U (en) | A kind of robot pneumatic polishing floating installation | |
| CN206123290U (en) | Valve body class product processing equipment of cutter integration | |
| CN206366816U (en) | A finishing machine for machining metal workpieces | |
| CN106625151B (en) | A kind of multiple degrees of freedom mixed connection polishing system | |
| CN105798738A (en) | A continuous conveying polishing wire drawing machine | |
| CN206326477U (en) | A kind of die casting multirobot cooperates with sanding apparatus | |
| CN206567953U (en) | A kind of bearing outer ring polishing machining production line | |
| CN203887664U (en) | Sand mill for special-shaped workpieces | |
| CN207289682U (en) | A kind of spring automatic chamfering machine | |
| CN205415222U (en) | Dedicated grinding device of machine part | |
| CN205497177U (en) | Crystal bar processing equipment and be used for main shaft mechanism of this equipment | |
| CN220881700U (en) | Scrap metal aftertreatment burr subassembly of polishing | |
| CN205588113U (en) | A fully automatic metal mobile phone case polishing line | |
| CN209256530U (en) | A kind of cylindrical part end face grinding device | |
| CN207189394U (en) | A kind of copper angle valve sanding and polishing system | |
| CN207104576U (en) | A kind of Superfinishing machine | |
| CN206677718U (en) | A kind of abrasive belt grinding machine that can keep grinding accuracy and grinding efficiency | |
| CN105328525A (en) | Single-workpiece horizontal double-end-surface grinding machine | |
| CN205630170U (en) | Plane automatic Sanda machine | |
| CN212578310U (en) | Single crystal grinding device and single crystal grinding all-in-one machine | |
| CN106625157A (en) | Piston processing production line |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20121219 |