CN102814964A - Flow-adjustable multi-stage shunting pipe extruding die - Google Patents
Flow-adjustable multi-stage shunting pipe extruding die Download PDFInfo
- Publication number
- CN102814964A CN102814964A CN2012102673806A CN201210267380A CN102814964A CN 102814964 A CN102814964 A CN 102814964A CN 2012102673806 A CN2012102673806 A CN 2012102673806A CN 201210267380 A CN201210267380 A CN 201210267380A CN 102814964 A CN102814964 A CN 102814964A
- Authority
- CN
- China
- Prior art keywords
- shunt head
- dies
- die
- branch outlet
- consicous
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 239000002002 slurry Substances 0.000 claims abstract description 8
- 238000001125 extrusion Methods 0.000 claims description 22
- 238000004519 manufacturing process Methods 0.000 abstract description 4
- 238000005516 engineering process Methods 0.000 description 2
- 239000011324 bead Substances 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000007795 chemical reaction product Substances 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 230000002950 deficient Effects 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 238000004513 sizing Methods 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
Images

Landscapes
- Extrusion Moulding Of Plastics Or The Like (AREA)
Abstract
The invention relates to a flow-adjustable multi-stage shunting pipe extruding die, comprising at least two grading dies, wherein each grading die comprises a cylindrical opening die extending transversely, and a columnar core die arranged in the opening mould, wherein a tubular gap between the opening die and the core die becomes a slurry channel; a core shaft extending transversely is arranged on an axial line of the core die; columnar support rods for connecting the core shaft with the opening die are arranged in the middle of an axial direction; an inlet end of the extruding die is provided with at least one shunting head; an end of the shunting head is provided with an inlet, and is divided into at least two branches at the inlet; corresponding branch outlets are respectively formed on the other one end of the shunting head; the inlet end of each grading die is communicated with a branch outlet of a shunting head; various branch outlet of the shunting head is connected with an inlet end of the grading die or an inlet of a shunting head. The extruding die provided by the invention can shunt pipe slurry, can be respectively communicated with the grading dies, and can simultaneously perform extruding processes so as to exponentially increase production efficiency.
Description
Technical field
The present invention relates to a kind of production equipment of plastic pipe, relate in particular to a kind of extrusion die that is used to make plastic pipe.
Background technology
Plastic pipe is just made through the vacuum sizing device typing behind the one-step forming via extrusion die by the tubing slip again; Wherein, Extrusion die is the critical component of tube forming, because common extrusion die only has the single single class-consicous dies of passage, the tubing slip gets into from the entrance point of these single class-consicous dies; The port of export leaves, and the tubing slip that the flow that provides for entrance point is bigger causes waste to a certain degree to reduce production efficiency.
Summary of the invention
The present invention has overcome the deficiency of prior art, provides a kind of simple in structure, and multi-stage diffluence, makes full use of the tubing slip at reasonable distribution, enhances productivity, and scalable branch flow simultaneously improves the extrusion die of pipe workpiece quality.
For achieving the above object; The technical scheme that the present invention adopts is: a kind of multi-stage diffluence tubing extrusion die of adjustable flow; It is characterized in that: comprise at least two class-consicous dies, each class-consicous dies comprises the tubular mouth mould and the column core of being located in mouthful mould of horizontal expansion, and the tubulose gap between mouthful mould and the core becomes slurry channel; The axis of said core is provided with the mandrel of horizontal expansion; Axially the middle part is provided with the columnar stays bar that connects mandrel and mouthful mould, and the entrance point of said extrusion die is provided with one or more shunt heads, shunts first end and is inlet; And be divided into two branches at least in the porch; Form corresponding branch outlet respectively at the other end, the entrance point of each class-consicous dies is connected with a branch outlet of a shunt head, and each branch outlet of said shunt head links to each other with an entrance point of class-consicous dies or links to each other with the inlet of a shunt head.
In preferred embodiment of the present invention, further comprise in the path of said at least one branch being provided with choke valve.
In preferred embodiment of the present invention, comprise that further said entrance point is provided with a shunt head, the branch outlet quantity of shunt head equates with class-consicous dies quantity, each branch outlet with and only corresponding class-consicous dies entrance point with one be connected.
In preferred embodiment of the present invention; Comprise that further said entrance point is provided with elementary shunt head and secondary shunt head; Elementary shunting first; The branch outlet quantity of elementary shunt head equals secondary shunt head quantity, and the branch outlet of each elementary shunt head is connected with the inlet of a corresponding secondary shunt head respectively; The branch outlet of each secondary shunt head is connected with the entrance point of corresponding class-consicous dies respectively.
In preferred embodiment of the present invention, comprising that further the branch outlet quantity of said shunt head equals the quantity of class-consicous dies, is two.
In preferred embodiment of the present invention, further comprise in the path of each branch outlet of said secondary shunt head being respectively equipped with choke valve.
In preferred embodiment of the present invention, comprising that further the branch outlet quantity of said elementary shunt head equals secondary shunt head quantity, is two, and each secondary shunt head has two branch outlets, and corresponding class-consicous dies quantity is four.
The invention solves the defective that exists in the background technology, extrusion die of the present invention is shunted the tubing slip, is communicated with class-consicous dies respectively, extrudes operation simultaneously, significantly improves production efficiency.Can be further in the path of the branch of shunt head, choke valve be set, regulates and each branch flow of balance,, improve stability to guarantee the tubing end product quality.
Description of drawings
Below in conjunction with accompanying drawing and embodiment the present invention is further specified.
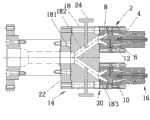
Fig. 1 is the structural representation of the preferred embodiments of the present invention 1;
Fig. 2 is the structural representation of the preferred embodiments of the present invention 2;
Among the figure: 2, class-consicous dies, 4, mouthful mould, 6, core, 8, slurry channel, 10, mandrel, 12, support bar; 14, entrance point, 16, the port of export, 18, shunt head, 181, inlet, 182, branch, 183, branch outlet; 20, entrance point, 22, flange, 24, choke valve, 26, elementary shunt head, 261, inlet, 263, branch outlet; 28, secondary shunt head, 281, inlet, 282, branch, 283, branch outlet, 30, flange.
The specific embodiment
Combine accompanying drawing and embodiment that the present invention is done further detailed explanation now, these accompanying drawings are the sketch map of simplification, basic structure of the present invention only is described in a schematic way, so it only show the formation relevant with the present invention.
Embodiment 1: as shown in Figure 1, the multi-stage diffluence tubing extrusion die of a kind of adjustable flow of the present invention comprises two class-consicous dies 2; Each classification mould 2 tool comprises the tubular mouth mould 4 and the column core of being located in mouthful mould 46 of horizontal expansion; Tubulose gap between mouth mould 4 and the core 6 becomes slurry channel 8, and the axis of said core 6 is provided with the mandrel 10 of horizontal expansion, and axially the middle part is provided with the columnar stays bar 12 that connects mandrel 10 and mouth mould 4; The horizontal two ends of said extrusion die are respectively the entrance point 14 and the port of export 16; Said entrance point 14 places are provided with a shunt head 18, shunt head 18 1 ends for the inlet 181, and the inlet 181 punishment be two branches 182; The entrance point 20 that forms corresponding 183, two class-consicous dies 2 of branch outlet at the other end respectively is connected with corresponding branch outlet 183 respectively.Said shunt head 18 is provided with flange 22 towards an end of extrusion die entrance point 14, is used for linking to each other with corresponding miscellaneous equipment.To support bar 12 directions, the slurry channel 8 annulus width of arbitrary section vertically equates that the internal radius of arbitrary section increases gradually along said entrance point 20.To the said port of export 16 directions, slurry channel 8 is divided into two sections along support bar 12, is bordering on a section of support bar 12, and the annulus width of arbitrary section reduces gradually, and the internal radius of arbitrary section also reduces gradually; Be bordering on a section of the said port of export 16, the annulus width of arbitrary section equates that the internal radius of arbitrary section equates.Said support bar 12 is 4; Bead mould 4 cross sections circumferentially evenly distribute; And each support bar 12 axis direction is parallel in the path of mouthful mould 4 cross sections, described two branches 182 and is respectively equipped with choke valve 24, and shunt head 18 outer walls are stretched out in the manual adjustable side of choke valve 24.
During work, the tubing slip gets into from shunt head 18 inlets 181, is divided into two from branch outlet 183 outflows, flows into corresponding class-consicous dies 2, extrusion molding simultaneously.
Embodiment 2: as shown in Figure 2; Embodiments of the invention 2 are with the difference part of embodiment 1: said entrance point is provided with elementary shunt head 26 and secondary shunt head 28; 26 1 of elementary shunt heads; 28 two of secondary shunt heads, the branch outlet 263 of elementary shunt head 26 also is two, the branch outlet 263 of each elementary shunt head 26 is connected with the inlet 281 of a corresponding secondary shunt head 28 respectively; The branch outlet 283 of secondary shunt head 28 is two, and said class-consicous dies 2 are 4, and the branch outlet 283 of each secondary shunt head 28 is connected with the entrance point 20 of corresponding class-consicous dies 2 respectively.Be respectively equipped with choke valve 24 in the path of the branch 282 of said 4 secondary shunt heads 28.One end of two secondary shunt head 28 inlets 281 is respectively equipped with flange 22, is connected with the respective branches outlet 263 of elementary shunt head 26 through flange 22.One end of elementary shunt head 26 inlets 261 also is provided with flange 30, is used for linking to each other with corresponding miscellaneous equipment.
During work, the tubing slip gets into from elementary shunt head 26 inlets 261, is divided into two from branch outlet 263 outflows; Flow into corresponding secondary shunt head 28 inlets 281 simultaneously; Each is divided into two again, totally four, is flowed out by secondary shunt head 28 branch outlets 283 respectively; Get into corresponding class-consicous dies 2, extrusion molding.
Above foundation desirable embodiment of the present invention is enlightenment, and through above-mentioned description, the related personnel can carry out various change and modification fully in the scope that does not depart from this invention technological thought.The technical scope of this invention is not limited to the content on the specification, must confirm technical scope according to the claim scope.
Claims (7)
1. the multi-stage diffluence tubing extrusion die of an adjustable flow; It is characterized in that: comprise at least two class-consicous dies, each class-consicous dies comprises the tubular mouth mould and the column core of being located in mouthful mould of horizontal expansion, and the tubulose gap between mouthful mould and the core becomes slurry channel; The axis of said core is provided with the mandrel of horizontal expansion; Axially the middle part is provided with the columnar stays bar that connects mandrel and mouthful mould, and the entrance point of said extrusion die is provided with one or more shunt heads, shunts first end and is inlet; And be divided into two branches at least in the porch; Form corresponding branch outlet respectively at the other end, the entrance point of each class-consicous dies is connected with a branch outlet of a shunt head, and each branch outlet of said shunt head links to each other with an entrance point of class-consicous dies or links to each other with the inlet of a shunt head.
2. the multi-stage diffluence tubing extrusion die of a kind of adjustable flow according to claim 1 is characterized in that: be provided with choke valve in the path of said at least one branch.
3. the multi-stage diffluence tubing extrusion die of a kind of adjustable flow according to claim 2; It is characterized in that: said entrance point is provided with a shunt head; The branch outlet quantity of shunt head equates with class-consicous dies quantity, each branch outlet with and only corresponding class-consicous dies entrance point with one be connected.
4. the multi-stage diffluence tubing extrusion die of a kind of adjustable flow according to claim 2; It is characterized in that: said entrance point is provided with elementary shunt head and secondary shunt head; Elementary shunting first; The branch outlet quantity of elementary shunt head equals secondary shunt head quantity, and the branch outlet of each elementary shunt head is connected with the inlet of a corresponding secondary shunt head respectively; The branch outlet of each secondary shunt head is connected with the entrance point of corresponding class-consicous dies respectively.
5. the multi-stage diffluence tubing extrusion die of a kind of adjustable flow according to claim 3, it is characterized in that: the branch outlet quantity of said shunt head equals the quantity of class-consicous dies, is two.
6. the multi-stage diffluence tubing extrusion die of a kind of adjustable flow according to claim 4 is characterized in that: be respectively equipped with choke valve in the path of each branch outlet of said secondary shunt head.
7. the multi-stage diffluence tubing extrusion die of a kind of adjustable flow according to claim 6; It is characterized in that: the branch outlet quantity of said elementary shunt head equals secondary shunt head quantity; Be two, each secondary shunt head has two branch outlets, and corresponding class-consicous dies quantity is four.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012102673806A CN102814964A (en) | 2012-07-31 | 2012-07-31 | Flow-adjustable multi-stage shunting pipe extruding die |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012102673806A CN102814964A (en) | 2012-07-31 | 2012-07-31 | Flow-adjustable multi-stage shunting pipe extruding die |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN102814964A true CN102814964A (en) | 2012-12-12 |
Family
ID=47299580
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012102673806A Pending CN102814964A (en) | 2012-07-31 | 2012-07-31 | Flow-adjustable multi-stage shunting pipe extruding die |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102814964A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106032053A (en) * | 2015-03-17 | 2016-10-19 | 亚申科技研发中心(上海)有限公司 | Extrusion molding apparatus |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN201685439U (en) * | 2010-04-13 | 2010-12-29 | 张家港联冠新材料有限公司 | One mould and multiple production extruded pipe mould head for ultra high molecular weight polyethylene |
| CN201792476U (en) * | 2010-03-20 | 2011-04-13 | 永高股份有限公司 | Extrusion die for hollow muffling spiral pipe |
| CN202180586U (en) * | 2011-07-15 | 2012-04-04 | 永高股份有限公司 | Multi-output PVC water supply pipe extrusion die |
| US20120119409A1 (en) * | 2007-12-21 | 2012-05-17 | American Maplan Corporation | Swept Leg Spider For An Extrusion Apparatus |
| CN202685282U (en) * | 2012-07-31 | 2013-01-23 | 昆山圣源机械有限公司 | Flow-adjustable multistage flow-split extrusion mold of pipe |
-
2012
- 2012-07-31 CN CN2012102673806A patent/CN102814964A/en active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20120119409A1 (en) * | 2007-12-21 | 2012-05-17 | American Maplan Corporation | Swept Leg Spider For An Extrusion Apparatus |
| CN201792476U (en) * | 2010-03-20 | 2011-04-13 | 永高股份有限公司 | Extrusion die for hollow muffling spiral pipe |
| CN201685439U (en) * | 2010-04-13 | 2010-12-29 | 张家港联冠新材料有限公司 | One mould and multiple production extruded pipe mould head for ultra high molecular weight polyethylene |
| CN202180586U (en) * | 2011-07-15 | 2012-04-04 | 永高股份有限公司 | Multi-output PVC water supply pipe extrusion die |
| CN202685282U (en) * | 2012-07-31 | 2013-01-23 | 昆山圣源机械有限公司 | Flow-adjustable multistage flow-split extrusion mold of pipe |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106032053A (en) * | 2015-03-17 | 2016-10-19 | 亚申科技研发中心(上海)有限公司 | Extrusion molding apparatus |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2589481B1 (en) | Device for continuously manufacturing a composite pipe with connection sleeve | |
| EP4010166B1 (en) | Melt distributor | |
| CN201998407U (en) | Two-layer extruder head | |
| CN202685282U (en) | Flow-adjustable multistage flow-split extrusion mold of pipe | |
| CN206242461U (en) | A kind of two layers of coextru-lamination pipe mold | |
| CN101357376A (en) | Novel aluminum circular tube sector diffuence-hole spiral bridge hot-extrusion mold | |
| DE102010043786B4 (en) | Device for producing pipes made of thermoplastic material | |
| CN108177320B (en) | Composite extrusion device and extrusion method for fiber-reinforced circular tubular material | |
| CN202685283U (en) | Foam pipe extruding mold with good layering effect | |
| EP2448742B1 (en) | Device and method for cooling plastic profiles | |
| CN209176140U (en) | The three-layer co-extruded spiral mould of PE tubing | |
| CN211467408U (en) | A color-coded extrusion die for a plastic extruder | |
| CN102814963B (en) | A kind of foaming tube extrusion die of adjustable feed rate | |
| CN204429876U (en) | The extruding drawing mould of pipe | |
| CN221187480U (en) | Multi-cavity tube forming die | |
| CN217021378U (en) | Novel multilayer pipe extrusion tooling | |
| CN105269787A (en) | High-assembling-accuracy double-layer-co-extrusion double-color-wire machine head | |
| CN109291394A (en) | PE pipe three-layer co-extrusion screw die and its feed distribution method | |
| CN106608034B (en) | The multi-layer co-extruded extrusion die of continuous tow | |
| DE69007530T2 (en) | Double preform extruder head for multi-layer blow molding. | |
| CN101398137B (en) | Manufacture equipment of rainbow tube | |
| CN1046435A (en) | Dripping irrigation pipe and manufacture method thereof with decompressing and continuous conduit | |
| CN223890439U (en) | PVC tubular product extrusion tooling | |
| CN203157090U (en) | Extrusion die head | |
| CN220742077U (en) | A scraper strip rapid extrusion molding die |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C12 | Rejection of a patent application after its publication | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20121212 |