CN102563610A - Energy saving system for boiler - Google Patents
Energy saving system for boiler Download PDFInfo
- Publication number
- CN102563610A CN102563610A CN2011103250931A CN201110325093A CN102563610A CN 102563610 A CN102563610 A CN 102563610A CN 2011103250931 A CN2011103250931 A CN 2011103250931A CN 201110325093 A CN201110325093 A CN 201110325093A CN 102563610 A CN102563610 A CN 102563610A
- Authority
- CN
- China
- Prior art keywords
- heat exchanger
- flue gas
- boiler
- demineralized water
- water heat
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 117
- UGFAIRIUMAVXCW-UHFFFAOYSA-N Carbon monoxide Chemical compound [O+]#[C-] UGFAIRIUMAVXCW-UHFFFAOYSA-N 0.000 claims abstract description 84
- 239000003546 flue gas Substances 0.000 claims abstract description 84
- 239000003245 coal Substances 0.000 claims abstract description 12
- 230000008676 import Effects 0.000 claims description 14
- 238000010612 desalination reaction Methods 0.000 claims description 12
- 229910000831 Steel Inorganic materials 0.000 claims description 8
- 239000002253 acid Substances 0.000 claims description 8
- 239000010959 steel Substances 0.000 claims description 8
- 238000010521 absorption reaction Methods 0.000 claims description 5
- 239000000463 material Substances 0.000 claims description 5
- 239000007789 gas Substances 0.000 abstract description 19
- 238000010438 heat treatment Methods 0.000 abstract description 14
- 238000005260 corrosion Methods 0.000 abstract description 13
- 230000007797 corrosion Effects 0.000 abstract description 13
- 238000000034 method Methods 0.000 abstract description 7
- CURLTUGMZLYLDI-UHFFFAOYSA-N Carbon dioxide Chemical compound O=C=O CURLTUGMZLYLDI-UHFFFAOYSA-N 0.000 abstract description 6
- 230000008569 process Effects 0.000 abstract description 6
- 238000006477 desulfuration reaction Methods 0.000 abstract description 5
- 230000023556 desulfurization Effects 0.000 abstract description 4
- 238000001704 evaporation Methods 0.000 abstract description 4
- 229910002092 carbon dioxide Inorganic materials 0.000 abstract description 3
- 239000001569 carbon dioxide Substances 0.000 abstract description 3
- 230000003134 recirculating effect Effects 0.000 abstract description 3
- 239000002918 waste heat Substances 0.000 abstract description 3
- 230000003247 decreasing effect Effects 0.000 abstract 2
- 238000012938 design process Methods 0.000 abstract 1
- 239000012716 precipitator Substances 0.000 abstract 1
- 239000000446 fuel Substances 0.000 description 7
- QAOWNCQODCNURD-UHFFFAOYSA-N Sulfuric acid Chemical compound OS(O)(=O)=O QAOWNCQODCNURD-UHFFFAOYSA-N 0.000 description 6
- 238000005516 engineering process Methods 0.000 description 6
- 238000013461 design Methods 0.000 description 5
- 230000001105 regulatory effect Effects 0.000 description 5
- 238000012546 transfer Methods 0.000 description 5
- 230000008901 benefit Effects 0.000 description 4
- 239000003638 chemical reducing agent Substances 0.000 description 4
- 238000002485 combustion reaction Methods 0.000 description 3
- 238000006392 deoxygenation reaction Methods 0.000 description 3
- 238000010586 diagram Methods 0.000 description 3
- 239000000428 dust Substances 0.000 description 3
- RAHZWNYVWXNFOC-UHFFFAOYSA-N Sulphur dioxide Chemical compound O=S=O RAHZWNYVWXNFOC-UHFFFAOYSA-N 0.000 description 2
- 235000019504 cigarettes Nutrition 0.000 description 2
- 230000001276 controlling effect Effects 0.000 description 2
- 238000004134 energy conservation Methods 0.000 description 2
- 230000008020 evaporation Effects 0.000 description 2
- 239000013505 freshwater Substances 0.000 description 2
- 239000002737 fuel gas Substances 0.000 description 2
- 239000003517 fume Substances 0.000 description 2
- 230000006872 improvement Effects 0.000 description 2
- 239000007788 liquid Substances 0.000 description 2
- 238000002156 mixing Methods 0.000 description 2
- 239000000126 substance Substances 0.000 description 2
- 230000009466 transformation Effects 0.000 description 2
- 235000003283 Pachira macrocarpa Nutrition 0.000 description 1
- NINIDFKCEFEMDL-UHFFFAOYSA-N Sulfur Chemical compound [S] NINIDFKCEFEMDL-UHFFFAOYSA-N 0.000 description 1
- 241001083492 Trapa Species 0.000 description 1
- 235000014364 Trapa natans Nutrition 0.000 description 1
- 150000008065 acid anhydrides Chemical class 0.000 description 1
- 230000002421 anti-septic effect Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000009835 boiling Methods 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000002242 deionisation method Methods 0.000 description 1
- 230000003009 desulfurizing effect Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000005611 electricity Effects 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 238000001556 precipitation Methods 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000002407 reforming Methods 0.000 description 1
- 235000009165 saligot Nutrition 0.000 description 1
- 239000002893 slag Substances 0.000 description 1
- 239000000779 smoke Substances 0.000 description 1
- 238000013517 stratification Methods 0.000 description 1
- 229910052717 sulfur Inorganic materials 0.000 description 1
- 239000011593 sulfur Substances 0.000 description 1
- AKEJUJNQAAGONA-UHFFFAOYSA-N sulfur trioxide Inorganic materials O=S(=O)=O AKEJUJNQAAGONA-UHFFFAOYSA-N 0.000 description 1
- -1 sulfur trioxide sulfides Chemical class 0.000 description 1
- 230000035900 sweating Effects 0.000 description 1
- 230000026676 system process Effects 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
- 230000001131 transforming effect Effects 0.000 description 1
- 238000009834 vaporization Methods 0.000 description 1
- 230000008016 vaporization Effects 0.000 description 1
- 238000005406 washing Methods 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
- 239000003643 water by type Substances 0.000 description 1
Images

Landscapes
- Control Of Steam Boilers And Waste-Gas Boilers (AREA)
Abstract
The invention discloses an energy saving system for a boiler, which is characterized in that a flue gas/desalted water heat exchanger is mounted between an electric precipitator and an induced-draft fan of a boiler tail flue, waste heat of flue gas is used for heating desalted water, steam consumption for heating of a deaerator is reduced, consumption of desulfurization process water is reduced, and the exhaust gas temperature of the flue gas is reduced. A recirculating pump is used for controlling inlet water temperature of a cold end of a heat exchanger to be not lower than 60 DEG C, so that the problem of corrosion of the cold end is prevented. By taking a 130t/h boiler as an example, heating steam for the deaerator is decreased by 4.58t/h accounting for 23.1% of the amount of the heating steam for the deaerator at rated evaporating capacity. Equivalently, standard coal is saved by 0.44t/h, and emission of carbon dioxide is reduced by 1.24t/h. At the rated evaporating capacity, the amount of the desulfurization process water can be decreased by 4.12t/h accounting for 30.2% of the amount of design process water.
Description
Technical field
The present invention relates to a kind of energy saver of boiler, particularly a kind of demineralized water of the flue gas heat heating boiler that utilizes boiler is with the energy conserving system of the boiler that reduces oxygen-eliminating device heating steam and consume.
Background technology
In occupation of important position, its evaporation capacity differs in size from 35t/h to 2000t/h modern boiler in national economy, and exhaust gas temperature between 140 ℃-180 ℃, is widely used in heat, electricity and chemical industry greatly.Main chemical energy/thermal power transfer equipment as has in the world had nearly bicentenary development history, and its thermal efficiency it is conventionally believed that its thermal efficiency reaches capacity between 87-94%.
Yet; Because boiler main fuel coal, oil etc. are sulfurous fuels; The sulfur dioxide that produces during burning, sulfur trioxide sulfides combine to form sulfuric acid vapor with steam; The set point that is lower than sulfuric acid vapor when the wall surface temperature of Boiler Metallic parts will form liquid sulfuric acid (being called dewfall) on its surface when (being called acid dew point).Be the corrosion that prevents that the boiler tail parts from causing owing to dewfall; When causing various in the world boiler design; Have to adopt higher exhaust gas temperature to alleviate the generation of dewfall phenomenon, the part boiler is because operation adjustment and fuel change have caused the actual exhaust gas temperature phenomenon higher than design temperature, and the exhaust gas temperature of boiler is greatly between 140 ℃-180 ℃; This just certainly will cause partial heat energy along with flue gas is discharged, and causes the waste of the energy.According to calculating, 16~20 ℃ of the every reductions of large-sized boiler exhaust gas temperature, boiler thermal output can improve 1%.
Because it is more to influence the factor of acid dew-point temperature, causes the acid corrosion of boiler tail equipment for preventing low exhaust gas temperature, at present, exhaust gas temperature is generally between 140 ℃ to 180 ℃ during the boiler oepration at full load.But the analysis of based on fuel and flue gas; The flue-gas temperature that gets into desulphurization system can be controlled at and be unlikely to cause the afterbody obvious corrosion in the 90-110 ℃ of scope; Particularly for the wet method fume desulfurizing system of not establishing GGH (former flue gas-clean flue gas heat exchange device); Too high former flue-gas temperature has just increased the consumption of fresh water (FW), just in vain the loss of this part heat.Therefore, also there is the decline space about 30-70 ℃ in the temperature of the flue gas of boiler.Can on flue, increase heat exchanger fully this part fume afterheat is reclaimed, thereby obtain energy-conservation benefit, can also reduce the technology water yield that flue gas desulphurization system consumes simultaneously.The key of transforming is the temperature (being exhaust gas temperature) that actual conditions are reasonably confirmed and control gets into the flue gas of desulphurization system of based on fuel and flue gas.
In addition; Owing to contain the moisture of 7-11% (volume ratio) in the flue gas; If the surface temperature of this part moisture element when touching the element of heat exchanger cold junction is lower than the dew point of moisture in the flue gas, will make the cold junction element surface adhere to aqueous water at the surface sweating of element; This part water will absorb the acid anhydrides in the flue gas, and these liquid acid will cause the corrosion of heat exchanger cold end surface.Therefore must control the surface temperature of cold junction element, avoid surface temperature low excessively.The surface temperature of cold junction element depends on the temperature (inlet temperature of heat exchanger demineralized water) of medium in the element, and relevant with the form of heat exchange element.Adopt the cryogenic heat exchanger of fin form can improve heat transfer coefficient and surface temperature.Result through corrosion test shows that when adopting this form heat exchanger, the replacing life-span of ND steel and Kao Dun steel was above 10 years.Therefore, adopt heat transfer coefficient higher fin or finned tube and have the ND steel and the Kao Dun steel of certain acid resistance, and control cold junction medium temperature just can satisfy the requirement of heat exchanger corrosion-resistant.
Summary of the invention
The objective of the invention is existing steam generator system to be transformed in order to solve above-mentioned technical problem; And the waste heat heating demineralized water that utilizes flue gas that proposes; Reduce the steam consumption of oxygen-eliminating device heating; And reduce desulfurization and use the technology water consumption, reduce a kind of energy conserving system of boiler of the exhaust gas temperature of flue gas simultaneously.And utilize recirculation pump control heat exchanger cold junction inflow temperature to be not less than 60 ℃, to prevent the problem of cold end corrosion.
Technical scheme of the present invention
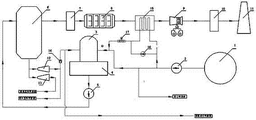
A kind of energy conserving system of boiler, comprise boiler, air preheater, electric cleaner, oxygen-eliminating device, sweet-water tank,Desalination water pump, air-introduced machine, absorption tower, chimney also comprise flue gas/demineralized water heat exchanger, control valve and recirculation pump, and described flue gas/demineralized water heat exchanger is installed on the boiler back end ductwork,
Between preferred electric cleaner and the air-introduced machine
The outlet of said sweet-water tank is gone into oxygen-eliminating device through pipeline through the desalination water pump is laggard; On the outlet conduit of desalination water pump back, be provided with a lateral and link to each other with the pipeline of the import of above-mentioned flue gas/demineralized water heat exchanger, the outlet conduit of flue gas/demineralized water heat exchanger is through get into oxygen-eliminating device behind the control valve with after the pipeline merging of the import of oxygen-eliminating device in the lump; Being provided with a lateral at the outlet of flue gas/demineralized water heat exchanger and control valve merges through the pipeline of the import of recirculation pump and flue gas/demineralized water heat exchanger and gets into flue gas/demineralized water heat exchanger in the lump;
Size through regulating control valve opening also partly is returned to flue gas/demineralized water heat exchanger import with about 90 ℃ hot water of flue gas/demineralized water heat exchanger exit and mixes with normal temperature demineralized water before getting into flue gas/demineralized water heat exchanger through recirculation pump; Thereby promptly be not less than 60 ℃ of dew-point temperature height that guarantee the cold junction temperatures of flue gas/demineralized water heat exchangers than flue gas with the cold junction inflow temperature of controlling flue gas/demineralized water heat exchanger, avoided the corrosion of cold junction element through control valve control recirculating mass.
Described flue gas/demineralized water heat exchanger can adopt the prior art heat exchanger, preferred " H " type extended surface tube heat exchanger that adopts; Because of advantages such as its abrasionproof performance, dust stratification with more extended surface area, excellence lack, existing higher heat transfer performance can prevent ash deposit and slag buildup again; H type fin is divided into several little zones to the space simultaneously; Air-flow is had the current-sharing effect, and therefore under the identical situation of other condition, wear-out life can improve 3-4 doubly.And on its material, select the acid-resistant steel material that possesses certain antiseptic power for use.Like ND steel etc.
The energy conserving system of above-mentioned a kind of boiler, its groundwork situation is following:
On boiler back end ductwork, increase a flue gas/demineralized water heat exchanger; Its concrete position can be selected by field condition; Preferred arrangements is on the electric precipitation exhaust pass; Except the location and layout of conveniently carrying out flue gas/demineralized water heat exchanger, can also reduce obstruction and the wearing and tearing of dust like this, and dwindle the coverage of cooling back flue gas flue gas/demineralized water heat exchanger.
The demineralized water that gets into oxygen-eliminating device is divided into two-way; One tunnel normal-temperature water directly gets into oxygen-eliminating device; Another part gets into oxygen-eliminating device through flue gas/demineralized water heat exchanger after being heated to 90 ℃; This part water yield is through the separate regulating valve control water yield, and the while has also been controlled the exhaust gas temperature behind flue gas/demineralized water heat exchanger.
Inflow temperature for control flue gas/demineralized water heat exchanger; Through size of regulating controlling opening of valve and the cold section temperature that mixes to guarantee flue gas/demineralized water heat exchanger mutually through normal temperature demineralized water before recirculation pump adjusting entering flue gas/demineralized water heat exchanger and that part of 90 ℃ hot water of getting back to outlet through recirculation pump is 60 ℃; Owing to kept former demineralized water pipeline and system; When the reforming equipment fault, system can return to former mode and move.Its concrete control principle is following:
Because the different often corresponding different exhaust gas temperature of load of boiler; Therefore when causing when variation such as load and environment temperature that exhaust gas temperature is corresponding and changing; Because exhaust gas temperature must not be lower than 90 degree, this numerical value gets into the unit centralized control system, when it departs from setting value; Through regulating the aperture size of pitch; Thereby regulate the flow of the flue gas/demineralized water heat exchanger partial deionization water of flowing through, the heat of corresponding increase/minimizing flue gas all maintains 90 ℃ with exhaust gas temperature and flue gas/demineralized water heat exchanger exit water temperature.Recirculation pump is a VFC; Control according to normal-temperature water and water temperature from 90 ℃ the mixed mixing water of hot water of flue gas/demineralized water heat exchanger exit; When this mixing temperature departs from 60 ℃ setting value; With the output pressure that changes recirculation pump, drive minimizing/increase and be back to the internal circulating load of 90 ℃ of hot water of flue gas/demineralized water heat exchanger import department, thereby keep 60 ℃ inflow temperature.
Beneficial effect of the present invention
The present invention is through increasing flue gas/demineralized water heat exchanger in original boiler back end ductwork, the waste heat that has reclaimed flue gas is used to heat demineralized water, the flue gas of original higher exhaust gas temperature is reduced to 90-110 ℃, and can cause the acid corrosion of boiler tail equipment.Be used to heat the middle pressure steam that demineralized water heats deoxygenation in the oxygen-eliminating device thereby reduced, promptly when using equivalent fuel, increased the quantity of steam of external heat supply, can realize considerable energy-saving benefit thus.Boiler with 130t/h is an example, can get according to calculating, and oxygen-eliminating device heating steam minimizing 4.58t/h accounts for 23.1% of oxygen-eliminating device heating steam amount under rated capacity.Be equivalent to save mark coal 0.44t/h, reducing emission of carbon dioxide 1.24 t/h.
In addition, exhaust gas temperature will reduce the technology water yield that desulfurization consumes after reducing.Boiler with 130t/h is an example, can get according to calculating, and under rated capacity, can reduce sulfur removal technology water yield 4.12t/h and account for 30.2% of the design technology water yield.
In addition, adopted the mode of setting up recirculation pump among the present invention first, 90 ℃ the hot water that will pass through heating is back to the heat exchanger import, thereby has guaranteed that inlet water temperature is not less than 60 ℃, has avoided the problem of cold end corrosion.
Description of drawings
The process flow diagram of the preceding system of pulverized-coal fired boiler transformation of Fig. 1, embodiment 1 described Natural Circulation, wherein 1 is that sweet-water tank, 2 is that desalination water pump, 3 is that oxygen-eliminating device, 4 is that deaerator storage tank, 5 is that feed pump, 6 is that boiler, 7 is that air preheater, 8 is that electric cleaner, 9 is that air-introduced machine, 10 is that absorption tower, 11 is that chimney, 12 is that middle pressure temperature-decreased pressure reducer, 13 is that high pressure attemperator, 14 is a pressure-reducing valve;
The process flow diagram of system after the pulverized-coal fired boiler transformation of Fig. 2, embodiment 1 described Natural Circulation; Wherein 1 is that sweet-water tank, 2 is that desalination water pump, 3 is that oxygen-eliminating device, 4 is that deaerator storage tank, 5 is that feed pump, 6 is that boiler, 7 is that air preheater, 8 is that electric cleaner, 9 is that air-introduced machine, 10 is that absorption tower, 11 is that chimney, 12 is that middle pressure temperature-decreased pressure reducer, 13 is that high pressure attemperator, 14 is that pressure-reducing valve, 15 is flue gas/demineralized water heat exchanger; 16 is recirculation pump, and 17 is control valve.
The specific embodiment
Below through embodiment and combine accompanying drawing that the present invention is further set forth, but do not limit the present invention.
Recirculation pump is that Shanghai China good pump industry Co., Ltd produces, and model is the one step single sucking Piping Centrifugal Pumps of IHG80-100, and 10 meters of lifts, power are 1.83kW.
Used H type fin tubular type flue gas/demineralized water heat exchanger is the conventional heat exchanger that lattice water chestnut power-equipment (China) Co., Ltd produces, and technical parameter is seen table 1.
Table 1, design of heat exchanger parameter
| Title | Unit | Numerical value |
| Rated power | MW | 3.07 |
| Rated operating pressure | MPa | 1.25 |
| Inlet water temperature | ℃ | 60 |
| The outlet water temperature | ℃ | 90 |
| Discharge | t/h | 87.8 |
| Import cigarette temperature | ℃ | 140 |
| Outlet cigarette temperature | ℃ | 90 |
| Flue gas flow | Nm 3/h | 160000 |
| Flue gas resistance | Pa | 497 |
Embodiment 1
With the pulverized-coal fired boiler of Natural Circulation commonly used, like the UG-130/5.7-M type, rated capacity is 130t/h, and half open-air ∏ type is arranged; The boiler of single drum, common downcomer is an example, and its system process sketch is seen shown in Figure 1, and 1 is sweet-water tank among the figure, and 2 is the desalination water pump; 3 is oxygen-eliminating device, and 4 is deaerator storage tank, and 5 is feed pump; 6 is boiler, and 7 is air preheater, and 8 is electric cleaner; 9 is air-introduced machine, and 10 is the absorption tower, and 11 is that chimney, 12 is that middle pressure temperature-decreased pressure reducer, 13 is that high pressure attemperator, 14 is pressure-reducing valve.
The operating path of the pulverized-coal fired boiler of the Natural Circulation of above-mentioned UG-130/5.7-M type; Be that boiler 6 uses demineralized water as working medium; Demineralized water in the sweet-water tank 1 is delivered in the oxygen-eliminating device 3 by desalination water pump 2 and is heated with steam, the boiling deoxygenation, and the demineralized water after the deoxygenation gets into deaerator storage tank 4 after feed pump 5 is delivered to boiler 6; After the fuel combustion in the boiler 6; Water in the boiler 6 absorb the steam that produces certain parameter after the fuel combustion heat of vaporization, insert respectively through high pressure attemperator 13 and middle pressure temperature-decreased pressure reducer 12 that the female pipe of high pressure heat supply network (like 5MPa) and middle pressure heat supply network are female manages (like 3.5MPa), heating network user.Oxygen-eliminating device 3 used heating steams be provided in a side of a branched pipe on the female pipe of middle pressure heat supply of Boiler Steam through steam reducing valve 14 step-downs after, get into oxygen-eliminating device 3.
Fuel the flue gas of discharging after boiler 6 internal combustion during then through air preheater 7 with the combustion-supporting air of the heat of flue gas, reduced the temperature of flue gas simultaneously.Through this heat transfer process to improve boiler efficiency.Flue gas gets into electric cleaner 8 and removes the dust in the flue gas then, and the flue gas after the dedusting is sent into desulfuration absorbing tower 10 washing desulphurizations through air-introduced machine 9 after chimney 11 is discharged.
The present invention transforms through the pulverized-coal fired boiler in the Natural Circulation of UG-130/5.7-M type, forms a kind of energy-conservation steam generator system, during its concrete process flow diagram is as shown in Figure 2.Promptly increase heat exchange area on electric cleaner 8 in the pulverized-coal fired boiler of the Natural Circulation of former UG-130/5.7-M type and the flue between the air-introduced machine 9 and be H type fin tubular type flue gas/demineralized water heat exchanger 15 of 1940 square metres;
On the outlet conduit of desalination water pump 2, being provided with a lateral links to each other with the pipeline of the import of described H type fin tubular type flue gas/demineralized water heat exchanger 15; The outlet conduit of described H type fin tubular type flue gas/demineralized water heat exchanger 15 is through get into oxygen-eliminating device 3 behind the control valve 17 and after the merging of the pipeline of the import of oxygen-eliminating device 3 in the lump; Simultaneously, between the outlet of H type fin tubular type flue gas/demineralized water heat exchanger 15 and control valve 17, being provided with a lateral merges through the pipeline of recirculation pump 16 and the import of flue gas/demineralized water heat exchanger 15 and gets into H type fin tubular type flue gas/demineralized water heat exchanger 15 in the lump;
Above-mentioned improvement and design, promptlyOriginally the demineralized water that got into oxygen-eliminating device 3 is divided into two tunnel, one tunnel normal-temperature water gets into oxygen-eliminating device 3 through original system, another part is through H type fin tubular type flue gas/demineralized water
Heat exchanger 15Be heated to about 90 ℃ after control valve 17 backs get into oxygen-eliminating device 3; This part desalination water yield is regulated control separately through control valve 17; Meanwhile also controlled the exhaust gas temperature behind flue gas/demineralized water heat exchanger 15; Guarantee that exhaust gas temperature under different evaporation capacity and flue-gas temperature condition about 90~110 ℃, prevents the afterbody corrosion on Equipment.
In addition; About 90 ℃ hot water of flue gas/demineralized water heat exchanger 15 outlets partly is returned to the import of flue gas/demineralized water heat exchanger 15 and mixes through recirculation pump 16 with normal temperature demineralized waters before getting into flue gas/demineralized water heat exchanger 15; Pass through the size of the aperture of adjusting control valve 17 simultaneously; Thereby the cold junction inflow temperature of common control flue gas/demineralized water heat exchanger is not less than 60 ℃ of dew-point temperature height that guarantee the cold junction temperatures of flue gas/demineralized water heat exchanger than flue gas, and then has avoided the corrosion of cold junction element.The about 46.7t/h of the preferred recirculating mass of present embodiment.
40t/h to 90 ℃ of the demineralized water that the heat of the H type fin tubular type flue gas/demineralized water heat exchanger boiler smoke capable of using of above-mentioned increase is 25 ℃ practiced thrift steam 4.58t/h, accounts for 23.1% of oxygen-eliminating device heating steam amount.Be equivalent to save mark coal 0.44t/h, reducing emission of carbon dioxide 1.24 t/h.
Below only basic principle of the present invention, principal character and advantage of the present invention are set forth with the example that transform as of the pulverized-coal fired boiler of the Natural Circulation of UG-130/5.7-M type.Those skilled in the art should understand; The present invention is not restricted to the described embodiments; What describe in the foregoing description and the specification is principle of the present invention; The present invention also has various changes and modifications under the prerequisite that does not break away from spirit and scope of the invention, and these variations and improvement all fall in the scope of the present invention that requires protection.
Claims (6)
1. the energy conserving system of a boiler; Comprise boiler, air preheater, electric cleaner, oxygen-eliminating device, sweet-water tank, desalination water pump, air-introduced machine, absorption tower, chimney; It is characterized in that also comprising flue gas/demineralized water heat exchanger; Control valve and recirculation pump, described flue gas/demineralized water heat exchanger is installed on the flue of boiler back;
The outlet of sweet-water tank is gone into oxygen-eliminating device through pipeline through the desalination water pump is laggard; On the outlet conduit of desalination water pump back, be provided with a lateral and link to each other with the pipeline of the import of above-mentioned flue gas/demineralized water heat exchanger, the outlet conduit of flue gas/demineralized water heat exchanger is through get into oxygen-eliminating device behind the control valve with after the pipeline merging of the import of oxygen-eliminating device in the lump;
Being provided with a lateral at the outlet of flue gas/demineralized water heat exchanger and control valve merges through the pipeline of the import of recirculation pump and flue gas/demineralized water heat exchanger and gets into flue gas/demineralized water heat exchanger in the lump.
2. the energy conserving system of a kind of boiler as claimed in claim 1 is characterized in that described flue gas/demineralized water heat exchanger preferably is installed between electric cleaner and the air-introduced machine.
3. the energy conserving system of a kind of boiler as claimed in claim 2 is characterized in that preferred " H " type extended surface tube heat exchanger of described flue gas/demineralized water heat exchanger.
4. the energy conserving system of a kind of boiler as claimed in claim 3 is characterized in that its material of described " H " type extended surface tube heat exchanger selects acid-resistant steel material for use.
5. the energy conserving system of a kind of boiler as claimed in claim 4 is characterized in that its material of described " H " type extended surface tube heat exchanger selects the ND steel for use.
6. the energy conserving system like claim 1,2,3, the described a kind of boiler of 4 or 5 arbitrary claims is applicable to pulverized-coal fired boiler.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011103250931A CN102563610A (en) | 2011-10-24 | 2011-10-24 | Energy saving system for boiler |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011103250931A CN102563610A (en) | 2011-10-24 | 2011-10-24 | Energy saving system for boiler |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN102563610A true CN102563610A (en) | 2012-07-11 |
Family
ID=46409752
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2011103250931A Pending CN102563610A (en) | 2011-10-24 | 2011-10-24 | Energy saving system for boiler |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102563610A (en) |
Cited By (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102767819A (en) * | 2012-07-13 | 2012-11-07 | 浙江工商大学 | Multi-stage biomass boiler flue gas and air heat recovery system and heat recovery method thereof |
| CN105066093A (en) * | 2015-09-06 | 2015-11-18 | 中国五环工程有限公司 | Gas-fire boiler |
| CN106382619A (en) * | 2016-11-09 | 2017-02-08 | 北京京诚科林环保科技有限公司 | Deep recovery system for flue gas waste heat of gas-fired boiler |
| CN107940439A (en) * | 2017-10-25 | 2018-04-20 | 河南中烟工业有限责任公司 | A kind of boiler smoke heat energy recycling system |
| CN108087902A (en) * | 2017-12-13 | 2018-05-29 | 华北电力大学(保定) | Steam latent heat and water reclamation system and its recovery method and control method in power-plant flue gas |
| CN108444304A (en) * | 2018-05-17 | 2018-08-24 | 山东焦化技术咨询服务有限公司 | A kind of waste heat of coke oven crude gas recycling system |
| CN111022926A (en) * | 2019-12-20 | 2020-04-17 | 河南开祥精细化工有限公司 | Steam balancing device and using method thereof |
| CN112984486A (en) * | 2021-02-26 | 2021-06-18 | 西安西热锅炉环保工程有限公司 | Energy-saving and emission-reducing system and method for small and medium-sized natural gas boilers |
| CN114353052A (en) * | 2021-12-30 | 2022-04-15 | 上海磬能装备有限公司 | Low-temperature deoxidization system for recycling flue gas heat |
| CN114526473A (en) * | 2021-12-28 | 2022-05-24 | 杭州华电能源工程有限公司 | Deep peak regulation heat supply system based on furnace water cooler and thermoelectric decoupling control method |
| CN114890596A (en) * | 2022-04-18 | 2022-08-12 | 湖南麦思克科技有限公司 | Method and system for adjusting externally supplied steam of thermal power plant |
| CN116518399A (en) * | 2023-06-09 | 2023-08-01 | 焦作市华康糖醇科技有限公司 | Cold end corrosion flue gas waste heat recycling system of low-temperature economizer |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2005207259A (en) * | 2004-01-21 | 2005-08-04 | Mitsui Eng & Shipbuild Co Ltd | Combined power plant |
| CN1979051A (en) * | 2005-12-05 | 2007-06-13 | 梁锡武 | Boiler smoke after-heat utilizing device |
| CN101140072A (en) * | 2007-10-25 | 2008-03-12 | 上海外高桥第三发电有限责任公司 | Desulfurization flue gas waste heat recovery system applied to coal-fired power generation units |
| CN101520172A (en) * | 2009-04-03 | 2009-09-02 | 上海晟煜科贸有限公司 | Energy-saving reclaiming process for residual heat of fume in boiler |
| CN201475979U (en) * | 2009-08-19 | 2010-05-19 | 赵永权 | A device that directly utilizes the exhaust waste heat of a power plant for heating |
-
2011
- 2011-10-24 CN CN2011103250931A patent/CN102563610A/en active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2005207259A (en) * | 2004-01-21 | 2005-08-04 | Mitsui Eng & Shipbuild Co Ltd | Combined power plant |
| CN1979051A (en) * | 2005-12-05 | 2007-06-13 | 梁锡武 | Boiler smoke after-heat utilizing device |
| CN101140072A (en) * | 2007-10-25 | 2008-03-12 | 上海外高桥第三发电有限责任公司 | Desulfurization flue gas waste heat recovery system applied to coal-fired power generation units |
| CN101520172A (en) * | 2009-04-03 | 2009-09-02 | 上海晟煜科贸有限公司 | Energy-saving reclaiming process for residual heat of fume in boiler |
| CN201475979U (en) * | 2009-08-19 | 2010-05-19 | 赵永权 | A device that directly utilizes the exhaust waste heat of a power plant for heating |
Non-Patent Citations (1)
| Title |
|---|
| 武勇 等: "某电厂锅炉排烟余热利用系统改造", 《锅炉制造》 * |
Cited By (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102767819A (en) * | 2012-07-13 | 2012-11-07 | 浙江工商大学 | Multi-stage biomass boiler flue gas and air heat recovery system and heat recovery method thereof |
| CN102767819B (en) * | 2012-07-13 | 2015-03-25 | 浙江工商大学 | Multi-stage biomass boiler flue gas and air heat recovery system and heat recovery method thereof |
| CN105066093A (en) * | 2015-09-06 | 2015-11-18 | 中国五环工程有限公司 | Gas-fire boiler |
| CN106382619A (en) * | 2016-11-09 | 2017-02-08 | 北京京诚科林环保科技有限公司 | Deep recovery system for flue gas waste heat of gas-fired boiler |
| CN107940439A (en) * | 2017-10-25 | 2018-04-20 | 河南中烟工业有限责任公司 | A kind of boiler smoke heat energy recycling system |
| CN108087902A (en) * | 2017-12-13 | 2018-05-29 | 华北电力大学(保定) | Steam latent heat and water reclamation system and its recovery method and control method in power-plant flue gas |
| CN108444304A (en) * | 2018-05-17 | 2018-08-24 | 山东焦化技术咨询服务有限公司 | A kind of waste heat of coke oven crude gas recycling system |
| CN111022926A (en) * | 2019-12-20 | 2020-04-17 | 河南开祥精细化工有限公司 | Steam balancing device and using method thereof |
| CN112984486A (en) * | 2021-02-26 | 2021-06-18 | 西安西热锅炉环保工程有限公司 | Energy-saving and emission-reducing system and method for small and medium-sized natural gas boilers |
| CN114526473A (en) * | 2021-12-28 | 2022-05-24 | 杭州华电能源工程有限公司 | Deep peak regulation heat supply system based on furnace water cooler and thermoelectric decoupling control method |
| CN114526473B (en) * | 2021-12-28 | 2024-04-26 | 杭州华电能源工程有限公司 | Deep peak shaving heat supply system based on furnace water cooler and thermal decoupling control method |
| CN114353052A (en) * | 2021-12-30 | 2022-04-15 | 上海磬能装备有限公司 | Low-temperature deoxidization system for recycling flue gas heat |
| CN114890596A (en) * | 2022-04-18 | 2022-08-12 | 湖南麦思克科技有限公司 | Method and system for adjusting externally supplied steam of thermal power plant |
| CN116518399A (en) * | 2023-06-09 | 2023-08-01 | 焦作市华康糖醇科技有限公司 | Cold end corrosion flue gas waste heat recycling system of low-temperature economizer |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102252339B (en) | System for reducing discharge smoke temperature of power station boiler | |
| CN103644648B (en) | A kind of Large Copacity Circulating Fluidized Bed Hot Water Boiler of forced water circulation | |
| CN202177093U (en) | Multi-level efficient displacement type fume waste-heat utilization system | |
| CN106500127B (en) | Bypass air preheater heat recovery system and method | |
| CN102444901A (en) | Coal power plant combined type heat pipe flue gas waste heat recovery system and method | |
| CN207006114U (en) | A kind of energy conserving system of boiler | |
| CN104165351A (en) | Emission reduction and energy conservation system without GGH | |
| CN203744221U (en) | Emission reduction system for smoke and dust of power plant boiler | |
| CN101261008B (en) | Liquid phase intermediate medium heat exchanging type heat exchanger | |
| CN105135468B (en) | Smoke waste heat utilization system | |
| CN104676622A (en) | Flue gas treatment system and flue gas reheating method based on fluoroplastic heat exchanger | |
| CN100593683C (en) | Automatic control system for wall temperature of boiler discharged smoke heat recovery heat exchanger | |
| CN212361988U (en) | Flue gas waste heat utilization system | |
| CN201844388U (en) | Flue-gas waste heat recovery device | |
| CN103115377B (en) | A kind of sub-control phase transformation air preheating system and air preheat method | |
| CN201764488U (en) | Low pressure coal saving device with automatic temperature control system | |
| CN111895442A (en) | Flue gas treatment system of power plant | |
| CN201206829Y (en) | Liquid phase intermediate medium heat exchanging type heat exchanger | |
| CN201344553Y (en) | Water-borne type gas heat-exchanging device | |
| CN202630747U (en) | Waste heat recovery system capable of improving efficiency of electric dust collector | |
| CN103836636B (en) | A kind of device reducing heat primary air cold wind incorporation efficiency | |
| CN208735652U (en) | The eliminating white smoke system that a kind of heat exchanger and air preheater combine | |
| CN207936055U (en) | Biomass recirculating fluidized bed boiler anticorrosion self compensation cryogenic heat exchanger system | |
| CN202203927U (en) | Economizer with energy-saving circulation system | |
| CN104728826A (en) | Constant temperature economizer |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20120711 |