CN102514054A - Processing method for manufacturing laminated wood board core board from spruce branch tips and laminated wood board - Google Patents
Processing method for manufacturing laminated wood board core board from spruce branch tips and laminated wood board Download PDFInfo
- Publication number
- CN102514054A CN102514054A CN2011104504140A CN201110450414A CN102514054A CN 102514054 A CN102514054 A CN 102514054A CN 2011104504140 A CN2011104504140 A CN 2011104504140A CN 201110450414 A CN201110450414 A CN 201110450414A CN 102514054 A CN102514054 A CN 102514054A
- Authority
- CN
- China
- Prior art keywords
- blockboard
- fir
- core
- board
- spruce
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000003672 processing method Methods 0.000 title claims abstract description 15
- 239000002023 wood Substances 0.000 title claims abstract description 11
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 8
- 241000218657 Picea Species 0.000 title abstract 8
- 239000003292 glue Substances 0.000 claims abstract description 33
- 241000219000 Populus Species 0.000 claims abstract description 21
- 238000001035 drying Methods 0.000 claims abstract description 18
- 238000000034 method Methods 0.000 claims abstract description 15
- 230000008569 process Effects 0.000 claims abstract description 8
- 238000003825 pressing Methods 0.000 claims abstract description 5
- 244000050510 Cunninghamia lanceolata Species 0.000 claims description 15
- 238000007731 hot pressing Methods 0.000 claims description 14
- GZCGUPFRVQAUEE-SLPGGIOYSA-N aldehydo-D-glucose Chemical compound OC[C@@H](O)[C@@H](O)[C@H](O)[C@@H](O)C=O GZCGUPFRVQAUEE-SLPGGIOYSA-N 0.000 claims description 13
- NLXLAEXVIDQMFP-UHFFFAOYSA-N Ammonia chloride Chemical compound [NH4+].[Cl-] NLXLAEXVIDQMFP-UHFFFAOYSA-N 0.000 claims description 10
- 229920001807 Urea-formaldehyde Polymers 0.000 claims description 9
- 239000003795 chemical substances by application Substances 0.000 claims description 6
- 235000019270 ammonium chloride Nutrition 0.000 claims description 5
- 235000013312 flour Nutrition 0.000 claims description 5
- 244000166124 Eucalyptus globulus Species 0.000 claims description 3
- 238000001816 cooling Methods 0.000 claims description 3
- 238000010008 shearing Methods 0.000 claims description 3
- 239000007787 solid Substances 0.000 claims description 3
- 238000003756 stirring Methods 0.000 claims description 3
- 230000032683 aging Effects 0.000 claims description 2
- 238000007711 solidification Methods 0.000 claims description 2
- 230000008023 solidification Effects 0.000 claims description 2
- 239000000463 material Substances 0.000 abstract description 8
- 238000012545 processing Methods 0.000 abstract description 5
- 238000005520 cutting process Methods 0.000 abstract description 3
- 239000002699 waste material Substances 0.000 abstract description 3
- 239000011248 coating agent Substances 0.000 abstract 1
- 238000000576 coating method Methods 0.000 abstract 1
- 238000005034 decoration Methods 0.000 abstract 1
- 238000005452 bending Methods 0.000 description 3
- 238000010586 diagram Methods 0.000 description 3
- 238000005516 engineering process Methods 0.000 description 3
- 230000003068 static effect Effects 0.000 description 3
- 238000010276 construction Methods 0.000 description 2
- 238000011161 development Methods 0.000 description 2
- 230000018109 developmental process Effects 0.000 description 2
- 230000006872 improvement Effects 0.000 description 2
- 230000035515 penetration Effects 0.000 description 2
- 239000002994 raw material Substances 0.000 description 2
- QGZKDVFQNNGYKY-UHFFFAOYSA-O Ammonium Chemical compound [NH4+] QGZKDVFQNNGYKY-UHFFFAOYSA-O 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000007689 inspection Methods 0.000 description 1
- 238000003801 milling Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 238000010998 test method Methods 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
Images
Landscapes
- Dry Formation Of Fiberboard And The Like (AREA)
Abstract
Description
技术领域 technical field
本发明具体涉及利用杉木梢头制造细木工板芯板及细木工板的加工方法。 The invention specifically relates to a processing method for making core boards of blockboards and blockboards by using fir tips.
背景技术 Background technique
随着我国30多年来经济的高速发展和人民群众生活水平的不断提高,人民群众对居住条件的改善的要求也越来越强烈,带动市场对建筑板材的需求逐年扩大;我国森林资源十分贫乏,一方面,用于传统的细木工细木工板材生产的杉木原材料已经无法满足市场的需要;另一方面,作为山场废弃物的杉木梢头大量丢弃,给我们国家经济上造成了很大浪费。一些地方的民众也曾经尝试着用杉木梢头生产杉木芯条(制造杉木细木工板的原材料),因杉木梢头存在直径小,尖削度大的问题,生产的杉木芯条质量长期无法保证,严重地影响了成品杉木细木工板的内在质量和使用范围。 With the rapid development of my country's economy for more than 30 years and the continuous improvement of people's living standards, the people's requirements for the improvement of living conditions have become increasingly strong, driving the market's demand for building panels to expand year by year; my country's forest resources are very poor, On the one hand, the Chinese fir raw materials used in the production of traditional joinery boards can no longer meet the needs of the market; on the other hand, a large number of Chinese fir tips are discarded as mountain waste, which has caused great waste to our country's economy. People in some places have also tried to use fir tips to produce fir core strips (the raw material for making fir blockboards). Because of the small diameter and sharpness of the fir tips, the quality of the produced fir core strips cannot be guaranteed for a long time. It affects the intrinsic quality and range of use of the finished fir blockboard.
因此,如何合理利用长期遭到忽视的杉木梢头资源,改良杉木细木工板的生产工艺,做到材尽其用、小材大用、劣材优用,提高杉木的利用率和使用价值,是我国木材工业所面临的首要问题,它既可改善森林状况,又能促进新材料的发展。因此,如何采用新工艺,开发新产品,扩大新用途,增加杉木产品的附加值,成为摆在我们林业科技工作者面前的首要工作任务。 Therefore, how to rationally utilize the long-neglected fir tip resources, improve the production process of fir blockboard, make the best use of the materials, use the small materials to make the best use of the inferior materials, and improve the utilization rate and use value of the Chinese fir. The primary problem facing my country's timber industry, it can not only improve forest conditions, but also promote the development of new materials. Therefore, how to adopt new technology, develop new products, expand new uses, and increase the added value of fir products has become the primary task for our forestry science and technology workers.
发明内容 Contents of the invention
为了解决上述问题,本发明提供了利用杉木梢头制造细木工板芯板及细木工板的加工方法,该发明能够有效的利用资源丰富,价格低廉的杉木梢头资源,解决杉木梢头加工中出材率低的问题。 In order to solve the above problems, the present invention provides a processing method for making blockboard core boards and blockboards by using Chinese fir tops. This invention can effectively utilize the resources of abundant and cheap Chinese fir tops to solve the problem of material yield in the processing of Chinese fir tops. low problem.
本发明首先提供了一种利用杉木梢头制造细木工板芯的加工方法,包括以下步骤: The present invention at first provides a kind of processing method utilizing fir tip to manufacture blockboard core, comprises the following steps:
步骤1:清理杉木梢头上的杂物,通过横截锯裁成0.4-0.6米长度的杉木棍; Step 1: Clean up the debris on the tip of the Chinese fir, and cut it into 0.4-0.6 meter long Chinese fir sticks by cross-cut sawing;
步骤2:将截断的杉木棍按小头直径进行分类,分类好的杉木棍送入木材干燥窑干燥,干燥温度为100~120℃,干燥时间为15~30小时,干燥后杉木棍的含水率控制在8~10%; Step 2: Classify the truncated fir sticks according to the diameter of the small head. The sorted fir sticks are sent to the wood drying kiln for drying. The drying temperature is 100-120°C and the drying time is 15-30 hours. Control at 8~10%;
步骤3:将干燥后的杉木棍加工成正六棱柱,正六棱柱内截圆的直径为2mm、4mm或6mm; Step 3: process the dried fir sticks into regular hexagonal prisms, and the diameter of the truncated circle inside the regular hexagonal prisms is 2mm, 4mm or 6mm;
步骤4:将内截圆直径相同的正六棱柱取出,涂刷地板胶,涂胶量200-260g/M2,陈化2-4小时后组坯,放入冷压机内加压固化;冷压机正压压力为1.2Mpa,侧压压力为0.8-1.0Mpa, 冷压时间为24小时; Step 4: Take out the regular hexagonal prism with the same diameter as the inner truncated circle, and apply floor glue with an amount of 200-260g/M 2 , after aging for 2-4 hours, put it into a cold press to press and solidify; The positive pressure of the press is 1.2Mpa, the side pressure is 0.8-1.0Mpa, and the cold pressing time is 24 hours;
步骤5:将完全固化的杉木组坯件取出,放置24小时后,加工制成规格为440mm×440mm×500mm的杉木方材; Step 5: Take out the fully solidified fir group blank, place it for 24 hours, and process it into a fir square with a size of 440mm×440mm×500mm;
步骤6:将杉木方材截断,制成规格为440mm×440mm×13mm的杉木板材,得到细木工板芯。 Step 6: cut off the Chinese fir square to make a Chinese fir board with a specification of 440mm×440mm×13mm to obtain a blockboard core.
由上述的加工方法制得的细木工板芯也在本发明的保护范围内。 Blockboard cores made by the above-mentioned processing method are also within the protection scope of the present invention.
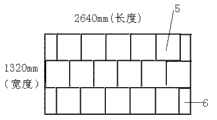
本发明还提供了一种用于细木工板的芯板,由上述的细木工板芯组坯而成,组坯方式为:每片芯板由18片规格为440mm×440mm×13mm的细木工板芯组成,18片的细木工板芯的排列就要求缝隙必须错开,排成三排;首先将2片规格为440mm×440mm×13mm的细木工板芯锯成4片220mm×440mm×13mm的板芯,第一排和第三排均由五片规格为440mm×440mm×13mm的细木工板芯以及两侧2片220mm×440mm×13mm的板芯组成,第二排由六片规格为440mm×440mm×13mm的细木工板芯组成。如图3所示。 The present invention also provides a core board for blockboards, which is formed by assembling the above-mentioned blockboard cores. Composed of board cores, the arrangement of 18 blockboard cores requires that the gaps must be staggered and arranged in three rows; first, two blockboard cores with a specification of 440mm×440mm×13mm are sawed into 4 pieces of 220mm×440mm×13mm Board cores, the first and third rows are composed of five blockboard cores with a size of 440mm×440mm×13mm and two pieces of board cores with a size of 220mm×440mm×13mm on both sides, and the second row is composed of six pieces with a size of 440mm ×440mm×13mm blockboard core. As shown in Figure 3.
本发明还保护了一种细木工板,包含上述的细木工板芯。 The present invention also protects a blockboard, comprising the blockboard core mentioned above.
本发明还提供了一种细木工板,包含所述的芯板。其加工方法包括以下步骤: The present invention also provides a blockboard, comprising the core board. Its processing method comprises the following steps:
步骤1:将杨木截成1.35m长的原木段,在旋切机上加工成厚度为2.2 mm的连续杨木单板带,再送入单板连续干燥机干燥,最终杨木单板带的含水率控制在8%以下; Step 1: Cut the poplar into 1.35m long logs, process it into a continuous poplar veneer belt with a thickness of 2.2 mm on a rotary cutter, and then send it to a continuous veneer dryer for drying. Finally, the moisture content of the poplar veneer The rate is controlled below 8%;
步骤2:将杨木单板带送入单板剪板机,剪成规格为1320mm×530mm×2.2 mm的杨木单板,备用; Step 2: Send the poplar veneer belt into the veneer shearing machine, and cut it into poplar veneer with a specification of 1320mm×530mm×2.2 mm, and set aside;
步骤3:将脲醛树脂胶倒入涂胶机,再加入占脲醛树脂胶重量1-3%的氯化铵固化剂和10-20%的面粉,搅拌均匀后开始涂胶,杨木单板的涂胶量控制在240-300g/m2; Step 3: Pour the urea-formaldehyde resin glue into the glue applicator, then add ammonium chloride curing agent accounting for 1-3% of the weight of the urea-formaldehyde resin glue and 10-20% flour, and start to apply glue after stirring evenly. The amount of glue applied is controlled at 240-300g/m 2 ;
步骤4:将规格为2640mm×1320mm×0.7mm的柳桉面板、杨木单板、权利要求3所述的芯板进行组坯后热压,热压压力1.0-1.2Mpa, 热压温度100-120℃,热压时间15-20分钟,完全固化后取出堆放,冷却24-48小时后取出锯板,制成规格为2440mm×1220mm×18mm的细木工板。
Step 4: Hot pressing the eucalyptus panel, poplar veneer, and the core board described in
上述步骤3中使用的脲醛树脂胶为改性脲醛树脂胶,胶的固含量为55-65%,PH值7.2,粘度500-700厘泊。
The urea-formaldehyde resin glue used in the
本发明的优点在于:采用本发明的加工方法能够生产出低成本、高品质的杉木梢头细木工板。能够有效的利用资源丰富,价格低廉的杉木梢头资源,生产出低成本、高品质的杉木梢头细木工板,可以满足建筑行业生产日益增长的板材需求。 The invention has the advantages that: the processing method of the invention can produce low-cost, high-quality fir tip blockboards. The method can effectively utilize abundant resources and low-priced fir top resources to produce low-cost, high-quality fir top blockboards, which can meet the increasing demand for boards produced in the construction industry.
附图说明 Description of drawings
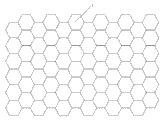
图1为本发明杉木梢头六棱柱组坯示意图;其中1、单一杉木梢头正六棱柱; Fig. 1 is the schematic diagram of the hexagonal prism assembly of the fir tip of the present invention; wherein 1, a single regular hexagonal prism of the fir tip;
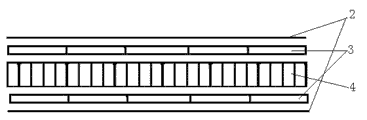
图2为本发明杉木梢头细木工板组坯示意图;其中2、柳桉面板;3、杨木单板;4、杉木梢头六棱柱芯板; Fig. 2 is the block diagram of the present invention's fir tip blockboard; wherein 2, meranti panel; 3, poplar veneer; 4, fir tip hexagonal prism core board;
图3为本发明杉木梢头细木工板芯板组坯示意图;其中5、规格为440mm×440mm×13mm的细木工板芯;6、规格为220mm×440mm×13mm的细木工板芯。 Fig. 3 is the schematic diagram of core board assembly of Chinese fir tip blockboard of the present invention; wherein 5, the blockboard core whose specification is 440mm * 440mm * 13mm; 6, the blockboard core whose specification is 220mm * 440mm * 13mm.
具体实施方式 Detailed ways
利用杉木梢头制造细木工板芯板及细木工板的加工方法的具体步骤为: The specific steps of the processing method of utilizing fir tip to manufacture blockboard core board and blockboard are:
步骤1:将收集来的杉木梢头及时清理树皮、枝丫及其它杂物,通过横截锯裁成0.5米长度的杉木棍; Step 1: Clean up the bark, branches and other sundries from the collected fir tips in time, and cut them into fir sticks with a length of 0.5 meters by cross-cut sawing;
步骤2:将截断的杉木棍按小头直径进行必要的分类,分类好的杉木棍送入木材干燥窑干燥,干燥温度为100~120℃,干燥时间为15~30小时,干燥后杉木棍的含水率控制在8~10%; Step 2: Necessarily classify the truncated fir sticks according to the diameter of the small head. The sorted fir sticks are sent to the wood drying kiln for drying. The drying temperature is 100-120°C and the drying time is 15-30 hours. The moisture content is controlled at 8~10%;
步骤3:将干燥后的杉木棍送入木材成型铣床加工成正六棱柱,正六棱柱内截圆的直径定为2mm、4mm或6mm; Step 3: send the dried Chinese fir sticks into a wood forming milling machine to be processed into a regular hexagonal prism, and the diameter of the inner truncated circle of the regular hexagonal prism is set at 2mm, 4mm or 6mm;
步骤4:将内截圆直径相同的正六棱柱取出,涂刷泰尔地板胶,涂胶量200-260g/M2,陈化2-4小时后,按照图1的要求组坯后,放入冷压机内加压固化;为了保证杉木组坯件胶合紧密(各六棱柱胶合面无间隙),冷压机需具备侧压装置;冷压机正压压力为1.2Mpa,侧压压力为0.8-1.0Mpa, 冷压时间为24小时; Step 4: Take out the regular hexagonal prism with the same diameter as the inner truncated circle, and apply Thiel floor glue with an amount of 200-260g/M 2 . The cold press is pressurized and solidified; in order to ensure that the fir group blanks are glued tightly (there is no gap between the glued surfaces of each hexagonal column), the cold press must be equipped with a side pressure device; the positive pressure of the cold press is 1.2Mpa, and the side pressure is 0.8 -1.0Mpa, cold pressing time is 24 hours;
步骤5:将完全固化的冷压杉木六棱柱组坯件(杉木组坯件)取出,放置24小时后,经细木工小带锯、平刨、压刨等木工机械的加工处理,制成规格为440mm×440mm×500mm(长×宽×高)杉木六棱柱方材(杉木方材); Step 5: Take out the completely solidified cold-pressed fir hexagonal prism blank (fir blank), and after 24 hours, process it with woodworking machinery such as small joinery band saws, plane planers, and pressure planers to make specifications 440mm×440mm×500mm (length×width×height) fir hexagonal prism square (fir square);
步骤6:将杉木六棱柱方材放入细木工小带锯截断,制成规格为440mm×440mm×13mm(长×宽×高)的杉木六棱柱板材(杉木板材),备用; Step 6: Put the fir hexagonal prism square into a small joinery band saw and cut it to make a fir hexagonal prism plate (fir plate) with a specification of 440mm×440mm×13mm (length×width×height), and set aside;
步骤7:采购新鲜的意大利杨木,截成1.35m长的原木段,在旋切机上加工成厚度为2.2 mm的连续杨木单板带,再送入单板连续干燥机干燥,最终杨木单板带的含水率控制在8%以下; Step 7: Purchasing fresh Italian poplar, cutting it into 1.35m long logs, processing it into a continuous poplar veneer belt with a thickness of 2.2 mm on a rotary cutter, and then sending it to a continuous veneer dryer for drying, and finally poplar veneer The moisture content of the strip is controlled below 8%;
步骤8:将杨木单板带送入单板剪板机,剪成规格为1320mm×530mm×2.2 mm(长×宽×厚)的杨木单板,备用;同时外购规格为2640mm×1320mm×0.7mm(长×宽×厚)的东南亚进口柳桉面板,备用; Step 8: Send the poplar veneer belt into the veneer shearing machine, and cut it into poplar veneer with a specification of 1320mm×530mm×2.2 mm (length×width×thickness) for use; at the same time, the purchased specification is 2640mm×1320mm ×0.7mm (length×width×thickness) meranti panel imported from Southeast Asia, spare;
步骤9:先称取一定数量脲醛树脂胶倒入涂胶机,再加入脲醛树脂胶重量1-3%的氯化铵固化剂和10-20%的面粉,搅拌均匀后开始涂胶,杨木单板的涂胶量控制在240-300g/m2左右; Step 9: First weigh a certain amount of urea-formaldehyde resin glue and pour it into the glue applicator, then add ammonium chloride curing agent of 1-3% of the weight of urea-formaldehyde resin glue and 10-20% flour, and start to apply glue after stirring evenly. The amount of glue applied to the veneer is controlled at about 240-300g/ m2 ;
步骤10:将柳桉面板、杨木单板、组坯后的杉木梢头六棱柱板材按照图2设定好的组坯方式进行组坯后热压,热压压力1.0-1.2Mpa, 热压温度100-120℃,热压时间15-20分钟,待杉木梢头细木工板材完全固化后取出堆放,冷却24-48小时后取出锯板,杉木梢头细木工板材的规格尺寸为2440mm×1220mm×18mm,再经分等、检验工序,生产出满足质量要求的杉木梢头细木工板材。 Step 10: After assembling the eucalyptus veneer, poplar veneer, and hexagonal prism plate at the top of fir according to the method set in Figure 2, perform hot pressing after assembling. The hot pressing pressure is 1.0-1.2Mpa, and the hot pressing temperature 100-120°C, hot pressing time 15-20 minutes, take out and stack the fir tip blockboard after it is completely solidified, take out the saw board after cooling for 24-48 hours, the size of the fir tip blockboard is 2440mm×1220mm×18mm, After grading and inspection procedures, fir top joinery boards that meet the quality requirements are produced.
所述步骤1中的杉木梢头为杉木采伐剩余物。 The fir tip in the step 1 is the fir felling residue.
所述步骤2中将截断的杉木棍按小头直径进行必要的分类,目的是提高杉木棍制造杉木六棱柱的出材率。 In the described step 2, the fir sticks truncated are classified according to the diameter of the small head, and the purpose is to improve the output rate of the fir sticks to make the hexagonal prisms of fir.
所述步骤3中将杉木六棱柱的内截圆直径定为2mm、4mm、6mm的目的是提高杉木棍制造杉木六棱柱的出材率。
In the described
所述步骤4中采用手工将六个棱面均匀涂刷泰尔地板胶,涂胶量200-260g/M2。 In the step 4, the six facets are evenly coated with Thiel floor glue by hand, and the amount of glue applied is 200-260g/M 2 .
所述步骤8中采用先干(干燥)后剪(截断)的单板加工工艺的目的是提高杨木单板尺寸的稳定性,减少成品杉木梢头细木工板材产生叠芯离缝的缺陷。 The purpose of adopting the veneer processing technology of first drying (drying) and then cutting (truncating) in the step 8 is to improve the dimensional stability of the poplar veneer and reduce the defects of core separation and seam in the finished fir tip blockboard.
所述步骤9中使用的脲醛树脂胶为改性脲醛树脂胶(改性脲醛树脂胶由福州人造板厂提供),胶的固含量为55-65%,PH值7.2,粘度500-700厘泊。 The urea-formaldehyde resin glue used in the step 9 is a modified urea-formaldehyde resin glue (modified urea-formaldehyde resin glue is provided by Fuzhou wood-based panel factory), the solid content of the glue is 55-65%, the pH value is 7.2, and the viscosity is 500-700 centipoise .
所述步骤9中氯化铵固化剂的添加量随季节和温度的变化而变化,夏、秋两季温度高,氯化铵固化剂的添加量可适当减少,控制在1%左右;春、冬两季温度低,化铵固化剂的添加量可适当增加,控制在3%左右;面粉的添加量可根据成品杉木梢头细木工板材的表面质量(透胶情况)加以确认,如成品杉木梢头细木工板材出现较为严重的透胶情况(板材表面发黑),就应该增加面粉的添加量,直至成品杉木梢头细木工板材的表面质量优良为止。 The addition amount of ammonium chloride solidifying agent changes with the change of season and temperature in the described step 9, and summer, two seasons of autumn temperature are high, and the addition amount of ammonium chloride solidifying agent can be suitably reduced, and is controlled at about 1%; When the temperature is low in winter and winter, the amount of ammonium curing agent can be appropriately increased and controlled at about 3%; the amount of flour added can be confirmed according to the surface quality (adhesive penetration) of the finished fir tip blockboard, such as the finished fir tip If the joinery board has serious glue penetration (the surface of the board is black), the amount of flour added should be increased until the surface quality of the finished fir tip joinery board is good.
所述步骤10中,为了保证成品杉木梢头细木工板材具有优良的物理力学特性,杉木六棱柱板材必须尊循图3设定好的组坯方式进行组坯。 In the step 10, in order to ensure that the finished fir tip joinery board has excellent physical and mechanical properties, the fir hexagonal prism board must be assembled in accordance with the method set in Figure 3.
制备的细木工板的密度按GB/T17657-1999中4.2密度测定规定进行;胶合性能按GB/T5849-2006中6.4.4胶合强度测定的试验方法进行。静曲强度试验按GB/T5849-2006中6.4.8静曲强度测定规定的方法进行;细木工板的密度0.45~0.50g/cm3,静曲强度﹥20MPa,胶合强度﹥1.5MPa。 The density of the prepared blockboard shall be carried out according to the provisions of 4.2 Density Determination in GB/T17657-1999; the glue performance shall be carried out according to the test method of 6.4.4 Determination of Bonding Strength in GB/T5849-2006. The static bending strength test shall be carried out according to the method specified in 6.4.8 Determination of static bending strength in GB/T5849-2006; the density of the blockboard is 0.45~0.50g/cm 3 , the static bending strength is >20MPa, and the bonding strength is >1.5MPa.
因此,通过本发明制备的细木工板,完全能满足作为杉木细木工板的使用要求。另外,采用本发明的生产工艺,能够有效的利用资源丰富,价格低廉的杉木梢头资源,生产出低成本、高品质的细木工板,可以满足建筑行业的需求。 Therefore, the blockboard prepared by the present invention can fully meet the requirements for use as a Chinese fir blockboard. In addition, by adopting the production process of the present invention, it is possible to effectively utilize abundant and cheap fir tip resources to produce low-cost, high-quality blockboards, which can meet the needs of the construction industry.
以上所述仅为本发明的较佳实施例,凡依本发明申请专利范围所做的均等变化与修饰,皆应属本发明的涵盖范围。 The above descriptions are only preferred embodiments of the present invention, and all equivalent changes and modifications made according to the scope of the patent application of the present invention shall fall within the scope of the present invention.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201110450414.0A CN102514054B (en) | 2011-12-29 | 2011-12-29 | Processing method for manufacturing laminated wood board core board from spruce branch tips and laminated wood board |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201110450414.0A CN102514054B (en) | 2011-12-29 | 2011-12-29 | Processing method for manufacturing laminated wood board core board from spruce branch tips and laminated wood board |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN102514054A true CN102514054A (en) | 2012-06-27 |
| CN102514054B CN102514054B (en) | 2014-06-25 |
Family
ID=46285257
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201110450414.0A Expired - Fee Related CN102514054B (en) | 2011-12-29 | 2011-12-29 | Processing method for manufacturing laminated wood board core board from spruce branch tips and laminated wood board |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102514054B (en) |
Cited By (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103317565A (en) * | 2013-04-08 | 2013-09-25 | 赵杰 | Solid wood cross section integrated plate and processing integration method thereof |
| CN103341890A (en) * | 2013-07-29 | 2013-10-09 | 南京林业大学 | Method for preparing large-size sheet by using small-diameter wood |
| CN103600404A (en) * | 2013-10-28 | 2014-02-26 | 黄山市永锦工艺品有限公司 | Production technology for producing core board by using leftover material plates |
| CN104097238A (en) * | 2013-04-02 | 2014-10-15 | 赵杰 | Solid wood cross section integrated board and processing integrating method thereof |
| CN104128981A (en) * | 2014-06-06 | 2014-11-05 | 遂川县洪林木业有限公司 | Cellular-structure laminated wood and production method thereof |
| CN106493805A (en) * | 2015-03-05 | 2017-03-15 | 南京林业大学 | A kind of pressurization splicing method of big cross section hexagonal prism integrated timber |
| CN107009451A (en) * | 2017-05-13 | 2017-08-04 | 福建和其昌树脂科技有限公司 | A kind of fast-growing woods structural panel and preparation method thereof |
| CN109676734A (en) * | 2018-12-29 | 2019-04-26 | 南宁市邦得力木业有限责任公司 | Method for preparing hexagonal plate blank base material by using eucalyptus core |
| CN111098367A (en) * | 2019-12-31 | 2020-05-05 | 江西兴创木业有限责任公司 | Wood core lengthening process |
| CN111571736A (en) * | 2020-06-01 | 2020-08-25 | 怀化市祺鑫木业股份有限公司 | Fireproof flame-retardant environment-friendly core-board with fir core and preparation method thereof |
| CN113400421A (en) * | 2021-07-06 | 2021-09-17 | 江西圣金源科技板材有限公司 | Hexagonal splice plate and processing method thereof |
| CN117841118A (en) * | 2024-02-27 | 2024-04-09 | 千年舟新材科技集团股份有限公司 | Fir three-layer structure substrate and furniture ecological plate prepared based on same |
Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2065991U (en) * | 1989-12-20 | 1990-11-21 | 韦善付 | Wood decorative board |
| CN1086224A (en) * | 1993-08-20 | 1994-05-04 | 山东省鱼台县合成胶厂 | A kind of modified urea-formaldehyde resin and production technique thereof |
| CN1177992A (en) * | 1995-03-09 | 1998-04-01 | 鲍塔复合材料公司 | Blockboard |
| JPH11291202A (en) * | 1998-04-08 | 1999-10-26 | Hirano Kirizai Kk | Paulownia plywood |
| CN1389330A (en) * | 2001-06-01 | 2003-01-08 | 浙江林学院 | Prepn. of core board for fine woodworker's board |
| JP2005199557A (en) * | 2004-01-15 | 2005-07-28 | Fuji Kankyo System Kk | Plywood and its production method |
| CN101058197A (en) * | 2006-04-17 | 2007-10-24 | 戴武兵 | Formaldehydeless fine wooden board and its preparing method |
| CN101270270A (en) * | 2008-04-28 | 2008-09-24 | 赵学开 | Modified environment protection type urea formaldehyde resin adhesive |
| CN201385341Y (en) * | 2009-02-13 | 2010-01-20 | 中国林业科学研究院木材工业研究所 | A solid wood composite board made of ultra-thick rotary-cut veneer |
| JP2010017956A (en) * | 2008-07-11 | 2010-01-28 | Koyo Sangyo Co Ltd | Laminated material manufacturing method |
| CN102528861A (en) * | 2012-03-05 | 2012-07-04 | 辽宁久久木业有限责任公司 | Production method and manufacturing process for environmentally-friendly decorative board |
-
2011
- 2011-12-29 CN CN201110450414.0A patent/CN102514054B/en not_active Expired - Fee Related
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2065991U (en) * | 1989-12-20 | 1990-11-21 | 韦善付 | Wood decorative board |
| CN1086224A (en) * | 1993-08-20 | 1994-05-04 | 山东省鱼台县合成胶厂 | A kind of modified urea-formaldehyde resin and production technique thereof |
| CN1177992A (en) * | 1995-03-09 | 1998-04-01 | 鲍塔复合材料公司 | Blockboard |
| JPH11291202A (en) * | 1998-04-08 | 1999-10-26 | Hirano Kirizai Kk | Paulownia plywood |
| CN1389330A (en) * | 2001-06-01 | 2003-01-08 | 浙江林学院 | Prepn. of core board for fine woodworker's board |
| JP2005199557A (en) * | 2004-01-15 | 2005-07-28 | Fuji Kankyo System Kk | Plywood and its production method |
| CN101058197A (en) * | 2006-04-17 | 2007-10-24 | 戴武兵 | Formaldehydeless fine wooden board and its preparing method |
| CN101270270A (en) * | 2008-04-28 | 2008-09-24 | 赵学开 | Modified environment protection type urea formaldehyde resin adhesive |
| JP2010017956A (en) * | 2008-07-11 | 2010-01-28 | Koyo Sangyo Co Ltd | Laminated material manufacturing method |
| CN201385341Y (en) * | 2009-02-13 | 2010-01-20 | 中国林业科学研究院木材工业研究所 | A solid wood composite board made of ultra-thick rotary-cut veneer |
| CN102528861A (en) * | 2012-03-05 | 2012-07-04 | 辽宁久久木业有限责任公司 | Production method and manufacturing process for environmentally-friendly decorative board |
Non-Patent Citations (1)
| Title |
|---|
| 吴智慧: "细木工板生产工艺技术(三)", 《建筑人造板》, no. 1, 25 March 1994 (1994-03-25) * |
Cited By (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104097238A (en) * | 2013-04-02 | 2014-10-15 | 赵杰 | Solid wood cross section integrated board and processing integrating method thereof |
| CN103317565A (en) * | 2013-04-08 | 2013-09-25 | 赵杰 | Solid wood cross section integrated plate and processing integration method thereof |
| CN103341890A (en) * | 2013-07-29 | 2013-10-09 | 南京林业大学 | Method for preparing large-size sheet by using small-diameter wood |
| CN103600404A (en) * | 2013-10-28 | 2014-02-26 | 黄山市永锦工艺品有限公司 | Production technology for producing core board by using leftover material plates |
| CN104128981A (en) * | 2014-06-06 | 2014-11-05 | 遂川县洪林木业有限公司 | Cellular-structure laminated wood and production method thereof |
| CN106493805A (en) * | 2015-03-05 | 2017-03-15 | 南京林业大学 | A kind of pressurization splicing method of big cross section hexagonal prism integrated timber |
| CN107009451A (en) * | 2017-05-13 | 2017-08-04 | 福建和其昌树脂科技有限公司 | A kind of fast-growing woods structural panel and preparation method thereof |
| CN109676734A (en) * | 2018-12-29 | 2019-04-26 | 南宁市邦得力木业有限责任公司 | Method for preparing hexagonal plate blank base material by using eucalyptus core |
| CN111098367A (en) * | 2019-12-31 | 2020-05-05 | 江西兴创木业有限责任公司 | Wood core lengthening process |
| CN111098367B (en) * | 2019-12-31 | 2021-10-22 | 江西兴创木业有限责任公司 | Wood core lengthening process |
| CN111098367B8 (en) * | 2019-12-31 | 2021-12-21 | 江西兴创木业有限责任公司 | Wood core lengthening process |
| CN111571736A (en) * | 2020-06-01 | 2020-08-25 | 怀化市祺鑫木业股份有限公司 | Fireproof flame-retardant environment-friendly core-board with fir core and preparation method thereof |
| CN113400421A (en) * | 2021-07-06 | 2021-09-17 | 江西圣金源科技板材有限公司 | Hexagonal splice plate and processing method thereof |
| CN117841118A (en) * | 2024-02-27 | 2024-04-09 | 千年舟新材科技集团股份有限公司 | Fir three-layer structure substrate and furniture ecological plate prepared based on same |
Also Published As
| Publication number | Publication date |
|---|---|
| CN102514054B (en) | 2014-06-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102514054B (en) | Processing method for manufacturing laminated wood board core board from spruce branch tips and laminated wood board | |
| CN101698311B (en) | Production process for finger jointing laminated wood board | |
| CN101863058B (en) | Novel laminated wood and manufacturing method thereof | |
| CN100548603C (en) | The manufacture method of high-strength anti-corrosion integrated material | |
| CN102371603A (en) | Process for manufacturing high-strength laminated wood board | |
| CN104084997B (en) | Continuously shaped composite construction material and manufacture method thereof | |
| CN101983851A (en) | Technology for making small-diameter logs into laminated wood | |
| CN101712170A (en) | Method for manufacturing mechanical and electrical packaging high-strength laminated veneer lumber | |
| CN104493942B (en) | The manufacture method of Eucalyptus timber substrate | |
| CN100387413C (en) | Method for manufacturing large-sheet particle-laminated lumber | |
| CN100354087C (en) | Small-diameter wood sheared integrating timber production method | |
| CN201078093Y (en) | Novel building mould | |
| CN103586955B (en) | Method for using inferior small firewood to produce resin recombination wood component | |
| CN201931506U (en) | Composite manmade panel | |
| CN203331157U (en) | Sandwich structure bamboo and wood composite recombinant structure material | |
| CN204172143U (en) | A kind of real-wood integrated material of new structure | |
| CN201217882Y (en) | Minor caliber trapezoid-shape laminated wood | |
| CN103331795A (en) | Fabrication method of cedar floor | |
| CN102359227A (en) | Plantation thin plate strip integrated wood | |
| CN102126236B (en) | Method for improving recovery ratio by directly polishing and mould-pressing sawn timber tip of engineered wood | |
| CN101961880A (en) | Manufacturing method of laminated particle board | |
| CN202428500U (en) | Core-blockboard manufactured by utilizing fir top wood | |
| CN104708686A (en) | Integrated solid wood panel of embedded structure | |
| CN103358367A (en) | Preparation process of laminated wood for solid wood door and window frame | |
| CN104552494A (en) | Manufacturing method for low-carbon and environmental-protection anti-deformation solid wood composite door frame |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20140625 Termination date: 20161229 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |