CN102476423A - Injection molding process for guide rail of heavy numerical control machine tool - Google Patents
Injection molding process for guide rail of heavy numerical control machine tool Download PDFInfo
- Publication number
- CN102476423A CN102476423A CN2010105533165A CN201010553316A CN102476423A CN 102476423 A CN102476423 A CN 102476423A CN 2010105533165 A CN2010105533165 A CN 2010105533165A CN 201010553316 A CN201010553316 A CN 201010553316A CN 102476423 A CN102476423 A CN 102476423A
- Authority
- CN
- China
- Prior art keywords
- guide rail
- injecting glue
- workbench
- machine tool
- molding process
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000001746 injection moulding Methods 0.000 title claims abstract description 10
- 239000003292 glue Substances 0.000 claims abstract description 80
- 239000000853 adhesive Substances 0.000 claims abstract description 19
- 230000001070 adhesive effect Effects 0.000 claims abstract description 19
- 239000011248 coating agent Substances 0.000 claims abstract description 13
- 238000000576 coating method Methods 0.000 claims abstract description 13
- 230000003068 static effect Effects 0.000 claims abstract description 9
- 238000000465 moulding Methods 0.000 claims abstract description 8
- 239000003795 chemical substances by application Substances 0.000 claims abstract description 7
- 239000007921 spray Substances 0.000 claims abstract description 4
- 238000005516 engineering process Methods 0.000 claims description 17
- 238000007789 sealing Methods 0.000 claims description 13
- 239000007788 liquid Substances 0.000 claims description 4
- 229910000831 Steel Inorganic materials 0.000 claims description 3
- 230000015572 biosynthetic process Effects 0.000 claims description 3
- 238000004140 cleaning Methods 0.000 claims description 3
- 239000012530 fluid Substances 0.000 claims description 3
- 239000010959 steel Substances 0.000 claims description 3
- 238000000034 method Methods 0.000 abstract description 10
- 238000002347 injection Methods 0.000 abstract description 6
- 239000007924 injection Substances 0.000 abstract description 6
- 239000002184 metal Substances 0.000 abstract description 3
- 229910052751 metal Inorganic materials 0.000 abstract description 3
- 238000004519 manufacturing process Methods 0.000 description 5
- 230000002706 hydrostatic effect Effects 0.000 description 4
- 238000007493 shaping process Methods 0.000 description 3
- 229910001018 Cast iron Inorganic materials 0.000 description 2
- 230000007547 defect Effects 0.000 description 2
- 230000002950 deficient Effects 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 239000000758 substrate Substances 0.000 description 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 1
- 239000002131 composite material Substances 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 239000010949 copper Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 239000011148 porous material Substances 0.000 description 1
- 238000007790 scraping Methods 0.000 description 1
Images

Landscapes
- Coating Apparatus (AREA)
Abstract
A guide rail injection molding process of a heavy numerical control machine tool is characterized in that after the assembly precision of a machine tool body guide rail meets the requirement and a workbench is machined, a static pressure oil cavity is manufactured on the surface of the machine tool body guide rail, two supporting edges for supporting the workbench are respectively arranged on the two sides of the surface of the machine tool body guide rail corresponding to glue to be injected, and the workbench is provided with a plurality of holes for injecting glue and exhausting gas; the core of the method is to construct a glue injection cavity, and uniformly spray a release agent on the contact surface of the lathe bed guide rail and the adhesive during glue injection, so as to ensure one-step molding of the molding guide rail. The invention provides an injection molding process of a guide rail of a heavy numerical control machine tool workbench, wherein a coating of the injection molding process is strong in binding affinity with metal and good in adhesion; the guide rail has the characteristics of good forming precision, good quality, high guide rail forming efficiency and long service life.
Description
Technical field
The present invention relates to a kind of heavy type numerical control machine tool guideway injection molding process, belong to numerically controlled machine guide rail field shaping technique, particularly, relate to a kind of guide rail and make forming technique through the Friction-Reducing Coating injection moulding.
Background technology
As lathe, especially secondary bonding plate, the soft band of adopting usually of the slip of heavy type numerical control machine tool motion component or hydrostatic slideway made or made through adopting the guide rail coating to duplicate forming technique at present.
Bonding plate technology is to use wider a kind of guide rail manufacturing technology at present.Plate processing back uses adhesive to be bonded on the cast iron guide pass; Use a great deal of screw fastening; Change again on the heavy duty machine tools after fastening guide rail is carried out fine finishining, cast iron/glue/plate MULTILAYER COMPOSITE in addition, bond and substrate combinating strength are not high; And, also need carry out just can the finish the work guide pass of platform of hand scraping to bonding numerous sheet-metal components and make because of guide pass requires than higher precision.Make efficiency is very low, and the production cycle is long.
Softly be with bonding mainly being used for to make small dimension part guide rails such as slide carriage, slide, do not adopt this kind technology for large-scale workpiece.
Guide rail coating duplicating forming technique at present at home, abroad a lot of producers have obtained using well.This kind technology be adopt artificial with the Friction-Reducing Coating blade coating on workbench guide pass to be made, then workbench is fastened on the making of the platform guide rail of finishing the work on the bed ways.Adopt the guide rail of this kind fabrication techniques to be easy to generate local shrinkage porosite, the phenomenon of pore occurs.Because the preliminary firm time of Friction-Reducing Coating has only 1 hour,, must in l hour time, accomplish the guide rail of large-scale workpiece and make in addition, need operating personnel's quantity many in order to guarantee the quality of coating guide rail.
Occurred injecting glue profiled guide rail technology at present, utilized the injecting glue forming technique to make the scheme of guide rail, made the defective that guide rail exists to solve such scheme.Wherein State Intellectual Property Office disclosed the assembly method that a name is called the hydrostatic slideway of " a kind of assembly method of hydrostatic slideway " on July 27th, 2005; It at first opens an injecting glue agent hand-hole on take-up housing, injecting glue, curing then, slide block and take-up housing are fixed.Owing to when injection moulding industry injecting glue, require the injecting glue agent to have certain injection pressure, so need structure to have the near closed hollow ring of hole for injecting glue and air-vent, this invention is the position of clear and definite hole for injecting glue only, how to construct the near closed hollow ring with air-vent and does not relate to.With regard to the structure of present workbench, small-sized workbench is exactly top said version with slide block and take-up housing in addition, and its guide rail forming method is not suitable for large-scale workbench.
Summary of the invention
The present invention provides a kind of heavy type numerical control machine tool guideway injection molding process in order to overcome the defective of prior art described in the background technology, and its coating and metal binding affinity are strong, and cementability is good; The guide rail formed precision is good, and quality is good, has guide rail shaping efficiency height, the characteristics of long service life.
For realizing the object of the invention, the present invention adopts following technical scheme:
It is after the bed ways assembly precision reaches requirement and workbench completion of processing; Make the static pressure oil pocket at the bed ways face; Corresponding to treating that injecting glue face both sides respectively are provided with a support edge that is used to support said workbench, said workbench is provided with a plurality of holes that are used for injecting glue and exhaust on the said bed ways; This technology is further comprising the steps of:
1) with technology plug shutoff hydraulic fluid port;
The steel pipe of injecting glue face is respectively treated in connection when 2) making has the multiple row guide rail;
3) contact-making surface of bed ways and adhesive evenly sprays releasing agent;
4) said workbench is treated that injecting glue face periphery adopts static pressure liquid sealing rank to seal;
5) the lifting workbench is on lathe bed, and the adjustment workbench makes said structure treat that the sealing strip that seals around the injecting glue face cooperates formation injecting glue die cavity with said support edge and baffle plate;
6) select the part in said hole to carry out injecting glue as hole for injecting glue;
7) treat adhesive, after promptly Friction-Reducing Coating is solidified, molding;
8) cleaning sealing strip.
Preferably, said hole for injecting glue is provided with two at least.
Preferably, said hole for injecting glue during greater than 2 meters, at least evenly is provided with three holes at the injecting glue face on workbench.
Preferably, hole for injecting glue and steam vent are selected at interval according to the adhesive distance of flow in said hole.
Preferably, said technology plug adopts soft technology plug.
Preferably, said injecting glue step begins injecting glue from the middle part of workbench, treat that facing hole for injecting glue mutually begins plastic emitting after, with first hole for injecting glue shutoff, respectively from facing hole for injecting glue mutually, stop during to the plastic emitting of table slide face then successively to the both sides injecting glue.
Preferably, the said injecting glue face of treating is the injecting glue face with comb structure.
Design of the present invention is by means of the adhesive injection mo(u)lding; Make slip or the secondary one-shot forming of hydrostatic slideway as the heavy machine tool moving component; Saving is carried out heavy duty machine tools fine finishining and is changeed the preface stand-by period, saves and carries out the manual amendment step, reduces operator's labour intensity; Improve the contact precision of guide pass, improve bond and moving component high base strength, improve the quality, reduce production costs, enhance productivity.
The present invention at first is to have designed the Feng plastic structure; Constructed the injecting glue die cavity; Wherein workbench treats that the part face of injecting glue face and bed ways constitutes upper and lower surfaces, treats that then injecting glue face support edge then constitutes all the other two faces, seals with structure injecting glue die cavity through sealing strip then; Because of injecting glue needs certain pressure, so its sealing at first will reach the liquid sealing requirement under this state.And because the face that contacts with adhesive all scribbles releasing agent on the bed ways, after the adhesive cures, direct molding, then because of the bonding of itself and workbench and with the disengaging of bed ways, and the making of the disposable platform guide rail of finishing the work.Because this injecting glue molding mode belongs to imitative type production method mechanically, has improved the contact precision and the quality of injecting glue profiled guide rail face and bed ways face, has improved the guide rail shaping efficiency greatly.And the guide rail that this mode is made and the substrate combinating strength of workbench are higher, and improve service life greatly.
The tentative making in border factually, the present invention can be practiced thrift 2/3 material cost with respect to copper spare adhesive board moulding scheme from material, save plate machining period 100% simultaneously, save for 2/3 workbench fine finishining man-hour again.And compare with the duplicating of guide rail coating, the guide pass precision is high, and quality is good.Need the workman of operation few.For the workbench of big more specification, the effect of its efficient aspect is remarkable more.
For a plurality of holes that are used for that are provided with on the said workbench; Hole for injecting glue can be done in this hole, also can do steam vent, and starting point is the distance of flow of adhesive; Avoid the mobile of long-distance, prevent that its adhesive cooling that flows into the injecting glue die cavity earlier is too fast and cause injection defect.
Description of drawings
Specify principle of the present invention below in conjunction with Figure of description.
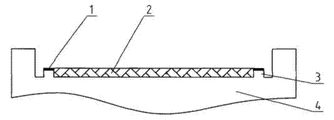
Wherein Fig. 1 is a table slide structure chart in the embodiment of the invention.
Fig. 2 is a static pressure oil pocket structural representation in the embodiment of the invention.
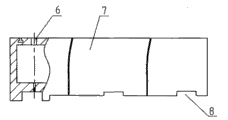
Fig. 3 is a comb structure sketch map in the embodiment of the invention.
Among the figure: 1, sealing strip, 2, treat the injecting glue face, 3, the support edge, 4, bed ways, 5, the static pressure oil pocket, 6, the hole, 7, workbench, 8, broach.
The specific embodiment
1. with reference to Figure of description; Present embodiment is after reaching requirement and workbench 7 completion of processing at bed ways 4 assembly precisions; Make static pressure oil pocket 5 at the bed ways face; Corresponding to treating that injecting glue face 2 both sides respectively are provided with a support edge 3 that is used to support said workbench, said workbench is provided with a plurality of holes 6 that are used for injecting glue and exhaust on the said bed ways; This technology is further comprising the steps of:
L) with technology plug shutoff hydraulic fluid port;
The steel pipe of injecting glue face is respectively treated in connection when 2) making has the multiple row guide rail;
3) contact-making surface of bed ways and adhesive evenly sprays releasing agent;
4) said workbench is treated that injecting glue face periphery adopts static pressure liquid sealing rank to seal;
5) the lifting workbench is on lathe bed, and the adjustment workbench makes said structure treat that the sealing strip 1 that seals around the injecting glue face cooperates formation injecting glue die cavity with said support edge and baffle plate;
6) select the part in said hole to carry out injecting glue as hole for injecting glue;
7) treat adhesive, after promptly Friction-Reducing Coating is solidified, molding;
8) cleaning sealing strip.
Said hole for injecting glue is provided with two at least, and that is to say to have a hole for injecting glue and a steam vent at least, could satisfy the needs of injecting glue and exhaust like this.And for long guide rail, just said hole for injecting glue during greater than 2 meters, at least evenly is provided with three holes at the injecting glue face on workbench; If three holes are set; If a kind of room hole for injecting glue, then adhesive flow maximum distance the time 1/2 treat injecting glue face length degree, and if be hole for injecting glue with the sky of both sides; Distance of flow is the same, and injecting glue speed can be fast.In like manner, for the guide rail of treating that the injecting glue face is long, then select more steam vent to help reducing injection defect.Certainly, for a plurality of hole for injecting glue, only selection is that hole for injecting glue and steam vent are selected at interval according to the adhesive distance of flow in said hole.
For for the technology plug that prevents adhesive entering oilhole preferably adopts soft technology plug, be convenient to dismounting.
Said injecting glue step begins injecting glue from the middle part of workbench, treat that facing hole for injecting glue mutually begins plastic emitting after, with first hole for injecting glue shutoff, respectively from facing hole for injecting glue mutually, stop during to the plastic emitting of table slide face then successively to the both sides injecting glue.Can guarantee that like this injecting glue is even, the adhesive distance of flow is the shortest.
The said injecting glue face of treating is the injecting glue face with comb structure, and profiled guide rail and workbench are combined closely.
Claims (1)
1. heavy type numerical control machine tool guideway injection molding process; It is after the bed ways assembly precision reaches requirement and workbench completion of processing; Make the static pressure oil pocket at the bed ways face; It is characterized in that: corresponding to treating that injecting glue face both sides respectively are provided with a support edge that is used to support said workbench, said workbench is provided with a plurality of holes that are used for injecting glue and exhaust on the said bed ways; This technology is further comprising the steps of:
1) with technology plug shutoff hydraulic fluid port;
The steel pipe of injecting glue face is respectively treated in connection when 2) making has the multiple row guide rail;
3) contact-making surface of bed ways and adhesive evenly sprays releasing agent;
4) said workbench is treated that injecting glue face periphery adopts static pressure liquid sealing rank to seal;
5) the lifting workbench is on lathe bed, and the adjustment workbench makes said structure treat that the sealing strip (1) that seals around the injecting glue face cooperates formation injecting glue die cavity with said support edge and baffle plate;
6) select the part in said hole to carry out injecting glue as hole for injecting glue;
7) treat adhesive, after promptly Friction-Reducing Coating is solidified, molding;
8) cleaning sealing strip.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2010105533165A CN102476423A (en) | 2010-11-22 | 2010-11-22 | Injection molding process for guide rail of heavy numerical control machine tool |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2010105533165A CN102476423A (en) | 2010-11-22 | 2010-11-22 | Injection molding process for guide rail of heavy numerical control machine tool |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN102476423A true CN102476423A (en) | 2012-05-30 |
Family
ID=46089257
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2010105533165A Pending CN102476423A (en) | 2010-11-22 | 2010-11-22 | Injection molding process for guide rail of heavy numerical control machine tool |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102476423A (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104690883A (en) * | 2015-01-27 | 2015-06-10 | 周正英 | Injection molding process of sliding-seat guide rail |
| CN109605660A (en) * | 2018-10-16 | 2019-04-12 | 广东长盈精密技术有限公司 | Camera bearing shell, manufacturing method thereof and mobile terminal applying camera bearing shell |
| CN114434706A (en) * | 2021-12-23 | 2022-05-06 | 杭州宏华数码科技股份有限公司 | A method for manufacturing a beam of a digital printing machine |
| CN114932384A (en) * | 2022-06-29 | 2022-08-23 | 武汉武重机床有限公司 | Machining method of hobbing machine tool rest guide rail assembly |
| CN117359326A (en) * | 2023-10-25 | 2024-01-09 | 安徽新诺精工股份有限公司 | A closed encircling saddle and ram combination mechanism for machine tools |
-
2010
- 2010-11-22 CN CN2010105533165A patent/CN102476423A/en active Pending
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104690883A (en) * | 2015-01-27 | 2015-06-10 | 周正英 | Injection molding process of sliding-seat guide rail |
| CN109605660A (en) * | 2018-10-16 | 2019-04-12 | 广东长盈精密技术有限公司 | Camera bearing shell, manufacturing method thereof and mobile terminal applying camera bearing shell |
| CN109605660B (en) * | 2018-10-16 | 2020-12-01 | 广东长盈精密技术有限公司 | Camera carrying case, method for making the same, and mobile terminal using the same |
| CN114434706A (en) * | 2021-12-23 | 2022-05-06 | 杭州宏华数码科技股份有限公司 | A method for manufacturing a beam of a digital printing machine |
| CN114932384A (en) * | 2022-06-29 | 2022-08-23 | 武汉武重机床有限公司 | Machining method of hobbing machine tool rest guide rail assembly |
| CN114932384B (en) * | 2022-06-29 | 2024-06-07 | 武汉武重机床有限公司 | Machining method of cutter rest guide rail assembly of gear hobbing machine |
| CN117359326A (en) * | 2023-10-25 | 2024-01-09 | 安徽新诺精工股份有限公司 | A closed encircling saddle and ram combination mechanism for machine tools |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN101786237B (en) | Fixture used for processing small moving blade in turbine and processing method thereof | |
| CN103028906B (en) | Fixed clamping block processing technology | |
| CN203509563U (en) | Numerically controlled turning and milling compound machine tool | |
| CN203209699U (en) | Piston composite machining lathe | |
| CN102328231A (en) | Flexible clamp for numerical-control processing and application thereof | |
| CN101905341B (en) | Method for processing double-sided inclined plane of part on one station | |
| CN205520443U (en) | Deep hole drilling and mill integrative digit control machine tool | |
| CN103144224B (en) | A kind of 45 ° of O RunddichtringO moulds and processing method thereof | |
| CN105478603B (en) | A kind of fractionation processing technology of automobile die | |
| CN204639722U (en) | Generator support Combined hydraulic fixture | |
| CN103464817B (en) | The method of arc square hole cutting apparatus and processing arc square hole | |
| CN101380799B (en) | Guide-rail injection molding technique of heavy numerically controlled machine | |
| CN104439896B (en) | The processing method that eccentric excircle has the section tube of flange arrangement with boss two ends | |
| CN201785453U (en) | Suspension type inner gear ring high-frequency quenching machine | |
| CN201350492Y (en) | Digital processing equipment for large and medium-sized sand mold | |
| CN204183298U (en) | Fork shaft series products machining center universal clipping system | |
| CN205966884U (en) | Servo double pump numerical control bender of electricity liquid | |
| CN204195275U (en) | Lathe hydraulic fixture | |
| CN103465077A (en) | Automatic positioning device of double-station cylinder sleeve | |
| CN104227451A (en) | Lathe hydraulic clamp | |
| CN210997586U (en) | Clamp for numerical control machine tool | |
| CN113547285A (en) | Method for machining multi-section ultrathin annular piece | |
| CN202015856U (en) | Linkage compression-type multi-hole drilling tool | |
| CN207127544U (en) | A kind of c-type iron core fixture device | |
| CN202715862U (en) | Numerically-controlled planer type milling machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20120530 |