CN102371288A - Preparation method of high-precision and high-strength titanium alloy seamless tube - Google Patents
Preparation method of high-precision and high-strength titanium alloy seamless tube Download PDFInfo
- Publication number
- CN102371288A CN102371288A CN2010102655419A CN201010265541A CN102371288A CN 102371288 A CN102371288 A CN 102371288A CN 2010102655419 A CN2010102655419 A CN 2010102655419A CN 201010265541 A CN201010265541 A CN 201010265541A CN 102371288 A CN102371288 A CN 102371288A
- Authority
- CN
- China
- Prior art keywords
- titanium alloy
- strength titanium
- preparation
- bar
- rolling
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 229910001069 Ti alloy Inorganic materials 0.000 title claims abstract description 79
- 238000002360 preparation method Methods 0.000 title claims abstract description 26
- 238000010438 heat treatment Methods 0.000 claims abstract description 24
- 238000005097 cold rolling Methods 0.000 claims abstract description 22
- 238000005096 rolling process Methods 0.000 claims abstract description 20
- 238000005242 forging Methods 0.000 claims abstract description 19
- 238000009785 tube rolling Methods 0.000 claims abstract description 7
- 238000000034 method Methods 0.000 claims description 14
- 238000012545 processing Methods 0.000 claims description 14
- 238000005266 casting Methods 0.000 claims description 10
- 230000003287 optical effect Effects 0.000 claims description 10
- 238000000137 annealing Methods 0.000 claims description 6
- 230000008569 process Effects 0.000 claims description 6
- 238000004519 manufacturing process Methods 0.000 abstract description 10
- 230000008901 benefit Effects 0.000 abstract description 4
- 239000000463 material Substances 0.000 abstract description 4
- 238000003754 machining Methods 0.000 abstract 3
- 101000666657 Homo sapiens Rho-related GTP-binding protein RhoQ Proteins 0.000 description 8
- 102100038339 Rho-related GTP-binding protein RhoQ Human genes 0.000 description 8
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 description 6
- 238000012360 testing method Methods 0.000 description 6
- 229910045601 alloy Inorganic materials 0.000 description 5
- 239000000956 alloy Substances 0.000 description 5
- 229910052739 hydrogen Inorganic materials 0.000 description 5
- 239000001257 hydrogen Substances 0.000 description 5
- UFHFLCQGNIYNRP-UHFFFAOYSA-N Hydrogen Chemical compound [H][H] UFHFLCQGNIYNRP-UHFFFAOYSA-N 0.000 description 4
- 238000013459 approach Methods 0.000 description 4
- 238000001125 extrusion Methods 0.000 description 4
- 238000009413 insulation Methods 0.000 description 4
- 230000003647 oxidation Effects 0.000 description 4
- 238000007254 oxidation reaction Methods 0.000 description 4
- 230000003746 surface roughness Effects 0.000 description 3
- 101100366060 Caenorhabditis elegans snap-29 gene Proteins 0.000 description 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 2
- 239000010949 copper Substances 0.000 description 2
- 229910052802 copper Inorganic materials 0.000 description 2
- 238000005336 cracking Methods 0.000 description 2
- 230000005496 eutectics Effects 0.000 description 2
- 238000004381 surface treatment Methods 0.000 description 2
- 208000037656 Respiratory Sounds Diseases 0.000 description 1
- 239000002253 acid Substances 0.000 description 1
- 239000000654 additive Substances 0.000 description 1
- 230000000996 additive effect Effects 0.000 description 1
- 230000004888 barrier function Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 238000012937 correction Methods 0.000 description 1
- 230000007797 corrosion Effects 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 238000003912 environmental pollution Methods 0.000 description 1
- 150000002431 hydrogen Chemical class 0.000 description 1
- 238000005461 lubrication Methods 0.000 description 1
- 238000005554 pickling Methods 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 230000008439 repair process Effects 0.000 description 1
- 238000005482 strain hardening Methods 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 239000010936 titanium Substances 0.000 description 1
- 229910052719 titanium Inorganic materials 0.000 description 1
Images

Landscapes
- Forging (AREA)
Abstract
The invention relates to a preparation method of a high-precision and high-strength titanium alloy seamless tube, and belongs to the field of material machining. The preparation method comprises the following steps: (1) heating and forging a high-strength titanium alloy ingot to obtain a high-strength titanium alloy bar; (2) heating the obtained high-strength titanium alloy bar to 580-620 DGE C, and then finishing and straightening the heated bar by a bar and tube straightening machine; (3) machining the straightened high-strength titanium alloy bar into a smooth bar, and then machining a through hole along the length direction of the smooth bar to obtain high-strength titanium alloy tube blank; (4) carrying out multi-pass cold rolling on the obtained high-strength titanium alloy tube blank on a tube rolling mill, and carrying out heat treatment once in every pass of rolling to obtain a high-strength titanium alloy tube; and (5) finishing and straightening the high-strength titanium alloy tube to finally obtain the finished product of the high-precision and high-strength titanium alloy seamless tube. The preparation method has the advantages of simple production process and low labor intensity of workers; and the product obtained by the preparation method has the advantages of high dimensional accuracy, high surface quality and high comprehensive properties, thus the finished product yield is obviously improved.
Description
Technical field
The present invention relates to a kind of manufacturing approach of titanium alloy seamless tubular goods, particularly a kind of preparation method of high accuracy high-strength titanium alloy seamless tubular goods belongs to material processing field.
Background technology
The high-strength titanium alloy seamless tubular goods has characteristics such as intensity height, density are low, corrosion resistance/good heat resistance, is the ideal material of field key positions such as Aeronautics and Astronautics, oil, chemical industry, boats and ships.But because the deformation at room temperature drag of high-strength titanium alloy is big, work hardening is remarkable, the cold cracking that becomes different; Oxidation takes place and inhales hydrogen in hot procedure easily, makes processing have certain-length and wall thickness and high accuracy high-strength titanium alloy pipes with good mechanical property has suitable difficulty.
At present, the method for making the high-strength titanium alloy seamless tubular goods has two kinds of roll piercing pipe rolling and extrusion tube blank rollings.(1) perforation pipe rolling: at first titan alloy casting ingot is forged into bar, send into two rollers after the bar heating or the three high cross piercing machine is worn into pipe, pipe is handled obtaining finished product tubing again through rolling, the annealing of multi-pass and finishing.This method have stock utilization height, tool and mould consumption less, advantage such as production efficiency is high, cost is low, the pipe surface quality is good; But because the pipe of roll piercing preparation is easy to generate tangible wall unevenness and off-centre; And follow-up rolling mill practice is limited to the correction capability of high-strength titanium alloy pipes wall unevenness and off-centre; The dimensional accuracy that causes final tubing, particularly wall thickness accuracy are not high; The wall thickness of roll piercing pipe is bigger usually, is not suitable for producing the less tubing of wall thickness; In addition; Oxidation takes place and inhales hydrogen in titanium alloy easily in heating, insulation and perforation procedure; Make tensile strength raising, the plasticity of pipe reduce, can cause titanium alloy pipe generation hydrogen embrittlement under the serious situation, cause the follow-up rolling deformation difficulty of titanium alloy pipe to increase; Occur crackle and cracking easily, and the comprehensive mechanical property of goods reduces.If under inert atmosphere or vacuum state, carry out the heating of titanium alloy pipe, perforation,, will increase production cost greatly to reduce oxidation and to inhale hydrogen.(2) extrusion tube blank rolling: with the heating of titan alloy casting ingot or excellent base, send into extruder then and be squeezed into pipe, pipe is carried out inside and outside surface treatment after, handle through rolling, the annealing of multi-pass and finishing again and obtain finished product tubing.But the extruding difficulty of high-strength titanium alloy pipes is big; Be mainly reflected in and be difficult to realize good technological lubrication; Cause pipe surfaces externally and internally poor quality, scratch seriously, not only increase follow-up pipe surface treatment greatly and repair and hinder workload; And the dimensional accuracy of end article and surface quality be difficult to guarantee, causes yield rate to reduce; As adopt the copper-clad cover to push; Because eutectic reaction takes place in titanium and copper about 880 ℃; Generate the eutectic brittle phase, the difficult quality guarantee of extrusion tube blank also needs a large amount of copper material of additive decrementation, to increase the back work amount big simultaneously; And need a large amount of acid solutions carry out pickling when removing copper-clad, cause environmental pollution; In addition, the tubing for big specification needs the large-tonnage extruder to push, and invests hugely, and cost is higher.
Therefore, provide the manufacturing approach that is used for high accuracy high-strength titanium alloy seamless tubular goods that a kind of manufacturing procedure is less, yield rate is higher just to become the technical barrier that this technical field is badly in need of solution.
Summary of the invention
The object of the invention is exactly the deficiency to prior art, and the preparation method of the high accuracy high-strength titanium alloy seamless tubular goods that a kind of manufacturing procedure is less, yield rate is higher is provided.
Above-mentioned purpose of the present invention reaches through following technical scheme:
A kind of preparation method of high accuracy high-strength titanium alloy seamless tubular goods, its step is following:
(1) preparation of high-strength titanium alloy bar: the high-strength titanium alloy ingot casting through heating, forging, is obtained the high-strength titanium alloy bar;
(2) aligning: step (1) gained high-strength titanium alloy bar is heated to 580~620 ℃, adopts bar and tube straightening machine to carry out the finishing aligning;
(3) preparation of high-strength titanium alloy pipe: the high-strength titanium alloy bar behind step (2) the gained aligning is machined to optical wand, along the length direction machined through hole of optical wand, obtains the high-strength titanium alloy pipe then;
(4) tube rolling and heat treatment: step (3) gained high-strength titanium alloy pipe is carried out the cold rolling processing of multi-pass on pipe mill, every rolling a time is heat-treated once, obtains high-strength titanium alloy pipes;
(5) finishing aligning: with obtaining finished product tubing behind step (4) the gained high-strength titanium alloy pipes process finishing aligning.
A kind of optimal technical scheme is characterized in that: forge described in the said step (1) on fast forging machine and carry out, and the forging deformation amount is 80%~98%.
A kind of optimal technical scheme is characterized in that: machined through hole described in the said step (3) is at the enterprising row of high accuracy depth drill lathe.
A kind of optimal technical scheme is characterized in that: the cold rolling processing described in the said step (4) is to adopt three roller cold-rolling pilger mills, to guarantee the tube rolling precision; The pass deformation of said cold rolling processing is 8%~15%, and the total deformation from pipe to finished product tubing is 45%~80%.
A kind of optimal technical scheme is characterized in that: the heat treatment described in the said step (4) comprises intermediate annealing and finished products, all adopt the tubing vacuum annealing furnace to carry out, and vacuum is lower than 1.33 * 10
-1Pa.
A kind of optimal technical scheme is characterized in that: the heat treatment described in the said step (4) is for being incubated 90~120min down at 780~800 ℃.
The forging of high-strength titanium alloy bar is being carried out on fast forging machine, and the forging deformation amount is 80%~98%, can improve the bar comprehensive quality; Bar machined through hole at the enterprising row of high accuracy depth drill lathe, can guarantee the dimensional accuracy of pipe; Pipe is through further rolling and annealing in process, and the tubing of required appearance and size and surface quality high-quality can not only be provided, and further improved the structure property of tubing.
Beneficial effect:
The present invention adopts and forges rod boring-cold rolling processing technology; Relatively roll piercing pipe rolling has the following advantages with the extrusion tube blank rolling: production technology simply, labor strength reduction greatly, product's dimensional precision and surface quality be very high; Can produce have medium caliber, certain length and the high accuracy high-strength titanium alloy seamless tubular goods of wall thickness, and it is high to significantly improve the tubing yield rate.The present invention has avoided the oxidation and suction hydrogen phenomenon of titanium alloy in hot procedures such as roll piercing or extruding; Can also effectively reduce and control the wall unevenness and the off-centre of pipe; Significantly reduce owing to wall unevenness and the eccentric follow-up work intensity that is caused, improve the dimensional accuracy of goods.
Below in conjunction with the accompanying drawing and the specific embodiment the present invention is further specified, but and do not mean that restriction protection domain of the present invention.
Description of drawings
Fig. 1 is the manufacturing approach flow chart of high accuracy high-strength titanium alloy seamless tubular goods of the present invention.
The specific embodiment
Embodiment 1
Selecting diameter for use is the TC10 high-strength titanium alloy ingot casting of 300mm, and desire is processed into the tubing with high accuracy, great surface quality and excellent comprehensive performance of
through " it is cold rolling that forging---is forged rod boring---" process route.Fig. 1 is the manufacturing approach flow chart of high accuracy high-strength titanium alloy seamless tubular goods of the present invention, and the concrete operations step is following:
1, bar preparation: adopt 2500 tons of fast forging machines, the TC10 titan alloy casting ingot of Φ 300mm is forged at 820 ℃~1050 ℃, obtain the TC10 titanium alloy rod bar of Φ 68 * 2400mm, the forging deformation amount is 94.9%.
2, WIRE FINISHING LINE aligning: the TC10 titanium alloy rod bar that forging is obtained is heated to 580 ℃ of insulation 90min, adopts Φ 25~horizontal straightener of 75 7 rollers to align then.
3, pipe preparation: the TC10 titanium alloy rod bar after at first will aligning is machined to the optical wand of φ 60mm on lathe; Adopt ZK2160D depth drill lathe then; Length direction machined through hole along optical wand; Obtain high accuracy TC10 titanium alloy pipe: φ 60 ± 0.05mm * φ 46 ± 0.05mm * 2400mm, the surfaces externally and internally roughness of pipe≤0.8 μ m.
4, tube rolling and heat treatment: the TC10 titanium alloy pipe of φ 60 ± 0.05mm * φ 46 ± 0.05mm * 2400mm carries out the cold rolling processing of 4 passages on LD60 three roller cold-rolling pilger mills; Every rolling a time is carried out vacuum heat once, obtains the tubing of
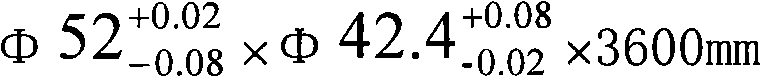 .Total deformation from pipe to finished product tubing is 46.3%.Concrete rolling and Technology for Heating Processing is as shown in table 1.
Table 1

5, finishing aligning: the tubing through after the above-mentioned cold rolling and heat treatment obtains finished product tubing after Φ 25~the horizontal straightener of 75 7 rollers is aligned.
Testing result to finished product tubing is following: the linearity of tubing is superior to 1000: 0.2, and tube wall thickness is poor≤± 0.1mm, surface roughness Ra≤0.8 μ m, tensile strength sigma
bBe 1070MPa, percentage elongation δ
5Be 13.5%.Testing result shows: the TC10 high-strength titanium alloy pipes that adopts this method to produce has good dimensional accuracy and good comprehensive performances.
Embodiment 2
Selecting diameter for use is the TA15 titan alloy casting ingot of 280mm, and desire is processed into the tubing with high accuracy, great surface quality and excellent comprehensive performance of
 through " it is cold rolling that forging---is forged rod boring---" process route.The concrete operations step is following:
1, bar preparation: adopt 2500 tons of fast forging machines, the TA15 high-strength titanium alloy ingot casting of Φ 280mm is forged at 850 ℃~1150 ℃, obtain the TA15 high-strength titanium alloy bar of Φ 52 * 2100mm, the forging deformation amount is 96.6%.
2, WIRE FINISHING LINE aligning: the TA15 titanium alloy rod bar that forging is obtained is heated to 620 ℃ of insulation 90min, adopts Φ 25~horizontal straightener of 75 7 rollers to align then.
3, pipe preparation: the TA15 titanium alloy rod bar after will aligning earlier is machined to the optical wand of φ 45mm on lathe; Adopt ZK2160D depth drill lathe then; Length direction machined through hole along optical wand; Obtain high accuracy TA15 titanium alloy pipe: φ 45 ± 0.05mm * φ 30 ± 0.05mm * 2100mm, the surfaces externally and internally roughness of pipe≤0.8 μ m.
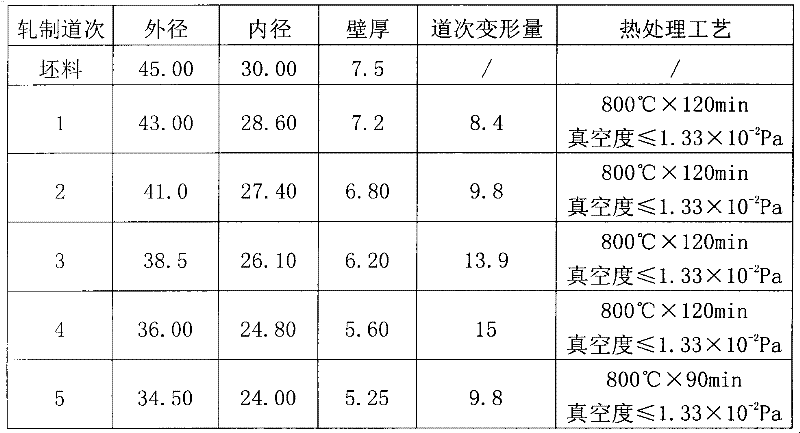
4, tube rolling and heat treatment: the TA15 titanium alloy pipe of φ 45 ± 0.05mm * φ 30 ± 0.05mm * 2100mm carries out the cold rolling processing of 5 passages on LD60 three roller cold-rolling pilger mills; Every rolling a time is carried out vacuum heat once, obtains the tubing of
 .Total deformation from pipe to finished product tubing is 56.8%.Concrete rolling and Technology for Heating Processing is as shown in table 2.
Table 2
5, finishing aligning: the tubing through after the above-mentioned cold rolling and heat treatment obtains finished product tubing after Φ 25~the horizontal straightener of 75 7 rollers is aligned.
Testing result to finished product tubing is following: the linearity of tubing is superior to 1000: 0.2, and tube wall thickness is poor≤± 0.1mm, surface roughness Ra≤0.8 μ m, tensile strength sigma
bBe 1010MPa, percentage elongation δ
5Be 15%.Testing result shows: the TA15 high-strength titanium alloy pipes that adopts this method to produce has good dimensional accuracy and good comprehensive performances.
Embodiment 3
Selecting diameter for use is the TA15 titan alloy casting ingot of 105mm, and desire is processed into the tubing with high accuracy, great surface quality and excellent comprehensive performance of
 through " it is cold rolling that forging---is forged rod boring---" process route.The concrete operations step is following:
1, bar preparation: adopt 2500 tons of fast forging machines, the TA15 high-strength titanium alloy ingot casting of Φ 105mm is forged at 850 ℃~1150 ℃, obtain the TA15 high-strength titanium alloy bar of Φ 45 * 2000mm, the forging deformation amount is 81.6%.
2, WIRE FINISHING LINE aligning: the TA15 titanium alloy rod bar that forging is obtained is heated to 620 ℃ of insulation 90min, adopts Φ 25~horizontal straightener of 75 7 rollers to align then.
3, pipe preparation: the TA15 titanium alloy rod bar after will aligning earlier is machined to the optical wand of φ 40mm on lathe; Adopt ZK2160D depth drill lathe then; Length direction machined through hole along optical wand; Obtain high accuracy TA15 titanium alloy pipe: φ 40 ± 0.05mm * φ 28 ± 0.05mm * 2000mm, the surfaces externally and internally roughness of pipe≤0.8 μ m.
4, tube rolling and heat treatment: the TA15 titanium alloy pipe of φ 40 ± 0.05mm * φ 28 ± 0.05mm * 2000mm carries out the cold rolling processing of 7 passages on LD60 three roller cold-rolling pilger mills; Every rolling a time is carried out vacuum heat once, obtains the tubing of
 .Total deformation from pipe to finished product tubing is 79.1%.Concrete rolling and Technology for Heating Processing is as shown in table 3.
Table 3

5, finishing aligning: the tubing through after the above-mentioned cold rolling and heat treatment obtains finished product tubing after Φ 25~the horizontal straightener of 75 7 rollers is aligned.
Testing result to finished product tubing is following: the linearity of tubing is superior to 1000: 0.2, and tube wall thickness is poor≤± 0.1mm, surface roughness Ra≤0.8 μ m, tensile strength sigma
bBe 1015MPa, percentage elongation δ
5Be 16%.Testing result shows: the TA15 high-strength titanium alloy pipes that adopts this method to produce has good dimensional accuracy and good comprehensive performances.
Claims (6)
1. the preparation method of a high accuracy high-strength titanium alloy seamless tubular goods, its step is following:
(1) preparation of high-strength titanium alloy bar: the high-strength titanium alloy ingot casting through heating, forging, is obtained the high-strength titanium alloy bar;
(2) aligning: step (1) gained high-strength titanium alloy bar is heated to 580~620 ℃, adopts bar and tube straightening machine to carry out the finishing aligning;
(3) preparation of high-strength titanium alloy pipe: the high-strength titanium alloy bar behind step (2) the gained aligning is machined to optical wand, along the length direction machined through hole of optical wand, obtains the high-strength titanium alloy pipe then;
(4) tube rolling and heat treatment: step (3) gained high-strength titanium alloy pipe is carried out the cold rolling processing of multi-pass on pipe mill, every rolling a time is heat-treated once, obtains high-strength titanium alloy pipes;
(5) finishing aligning: with obtaining finished product tubing behind step (4) the gained high-strength titanium alloy pipes process finishing aligning.
2. the preparation method of high accuracy high-strength titanium alloy seamless tubular goods according to claim 1 is characterized in that: forge described in the said step (1) on fast forging machine and carry out, and the forging deformation amount is 80%~98%.
3. the preparation method of high accuracy high-strength titanium alloy seamless tubular goods according to claim 1 is characterized in that: machined through hole described in the said step (3) is at the enterprising row of high accuracy depth drill lathe.
4. the preparation method of high accuracy high-strength titanium alloy seamless tubular goods according to claim 1; It is characterized in that: cold rolling being processed as described in the said step (4) adopted three roller cold-rolling pilger mills; The pass deformation of cold rolling processing is 8%~15%, and the total deformation from pipe to finished product tubing is 45%~80%.
5. the preparation method of high accuracy high-strength titanium alloy seamless tubular goods according to claim 1 is characterized in that: heat treatment described in the said step (4) is carried out for adopting vacuum annealing furnace, and vacuum is lower than 1.33 * 10
-1Pa.
6. the preparation method of high accuracy high-strength titanium alloy seamless tubular goods according to claim 5 is characterized in that: described heat treatment is for being incubated 90~120min down at 780~800 ℃.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2010102655419A CN102371288A (en) | 2010-08-27 | 2010-08-27 | Preparation method of high-precision and high-strength titanium alloy seamless tube |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2010102655419A CN102371288A (en) | 2010-08-27 | 2010-08-27 | Preparation method of high-precision and high-strength titanium alloy seamless tube |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN102371288A true CN102371288A (en) | 2012-03-14 |
Family
ID=45790835
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2010102655419A Pending CN102371288A (en) | 2010-08-27 | 2010-08-27 | Preparation method of high-precision and high-strength titanium alloy seamless tube |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102371288A (en) |
Cited By (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102909237A (en) * | 2012-11-22 | 2013-02-06 | 宁夏东方钽业股份有限公司 | Preparation method of TA18 thick-wall tube |
| CN103358100A (en) * | 2013-07-26 | 2013-10-23 | 江南工业集团有限公司 | Forging and molding process method for titanium alloy tubular piece |
| CN103894441A (en) * | 2014-03-20 | 2014-07-02 | 宝鸡拓普达钛业有限责任公司 | Machining method of TC4 titanium alloy thick-wall tubular product |
| CN104561912A (en) * | 2013-10-15 | 2015-04-29 | 宁波江丰电子材料股份有限公司 | Production method of titanium focus ring |
| CN104624713A (en) * | 2014-12-17 | 2015-05-20 | 北京有色金属研究总院 | Fabrication method of small precise thin-wall seamless titanium alloy tube |
| CN105478523A (en) * | 2015-11-27 | 2016-04-13 | 宝鸡市利泰有色金属有限公司 | Preparation technology for medical beta type titanium alloy capillary tubes |
| CN105568195A (en) * | 2015-12-25 | 2016-05-11 | 北京有色金属研究总院 | Preparation method for high-accuracy and high-strength titanium alloy seamless tubes |
| CN106282867A (en) * | 2016-09-05 | 2017-01-04 | 攀钢集团攀枝花钢铁研究院有限公司 | TA2 thin-wall titanium alloy seamless steel pipe and preparation method thereof |
| CN107738070A (en) * | 2017-09-29 | 2018-02-27 | 宝鸡市金海源钛标准件制品有限公司 | A kind of preparation method of titanium alloy seamless pipe |
| CN108188196A (en) * | 2017-12-04 | 2018-06-22 | 中国科学院金属研究所 | A kind of FeCrAl/Zr composite bimetal pipes and preparation method thereof |
| CN109513766A (en) * | 2018-11-15 | 2019-03-26 | 南通金尼新材料科技有限公司 | A kind of manufacturing method of high concentricity martensitic stainless steel seamless pipe material |
| CN111014337A (en) * | 2019-12-01 | 2020-04-17 | 重庆金世利航空材料有限公司 | Preparation method of non-porous extruded titanium alloy pipe |
| CN112605123A (en) * | 2020-11-30 | 2021-04-06 | 西北有色金属研究院 | Preparation method of low-cost high-toughness titanium alloy pipe for ocean engineering |
| CN113458176A (en) * | 2021-06-30 | 2021-10-01 | 浙江久立特材科技股份有限公司 | Manufacturing method of high-precision outer hexagonal and inner circular seamless tube with special-shaped cross section for nuclear power |
| CN115846456A (en) * | 2022-12-14 | 2023-03-28 | 安徽宝泰特种材料有限公司 | Manufacturing method of TA18 titanium alloy seamless small-caliber pipe |
| CN116656994A (en) * | 2023-07-25 | 2023-08-29 | 成都先进金属材料产业技术研究院股份有限公司 | Method for improving shrinkage strain ratio of TA18 titanium alloy seamless tube and TA18 titanium alloy seamless tube |
| CN116921491A (en) * | 2023-07-14 | 2023-10-24 | 中国航发北京航空材料研究院 | Preparation method of high-strength titanium alloy pipe |
| CN116984833A (en) * | 2023-07-06 | 2023-11-03 | 中国航发哈尔滨东安发动机有限公司 | Processing method of nickel-based superalloy pipe |
| CN118437767A (en) * | 2024-07-08 | 2024-08-06 | 西安稀有金属材料研究院有限公司 | Preparation method of high-precision ultra-large caliber thin-wall Ti35 titanium alloy pipe |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3698070A (en) * | 1969-09-25 | 1972-10-17 | Cefilac | Method of fabricating seamless steel pipes |
| US4991419A (en) * | 1988-11-18 | 1991-02-12 | Sumitomo Metal Industries, Ltd. | Method of manufacturing seamless tube formed of titanium material |
| DE4019117A1 (en) * | 1990-06-12 | 1991-12-19 | Mannesmann Ag | Titanium (alloy) tubing prodn. - by welding together strip, cold rolling and recrystallisation annealing |
| CN1370640A (en) * | 2001-02-17 | 2002-09-25 | Sms米尔股份有限公司 | Seamless copper tube cold rolling process |
| JP2006122932A (en) * | 2004-10-27 | 2006-05-18 | Jfe Steel Kk | Manufacturing method of low yield ratio ERW steel pipe for line pipe |
| CN101704035A (en) * | 2009-11-26 | 2010-05-12 | 北京有色金属研究总院 | Processing method of high-strength titanium alloy thin-walled tube stock |
| CN101708511A (en) * | 2007-12-13 | 2010-05-19 | 攀钢集团四川长城特殊钢有限责任公司 | Method for manufacturing pure titanium seamless tubes |
-
2010
- 2010-08-27 CN CN2010102655419A patent/CN102371288A/en active Pending
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3698070A (en) * | 1969-09-25 | 1972-10-17 | Cefilac | Method of fabricating seamless steel pipes |
| US4991419A (en) * | 1988-11-18 | 1991-02-12 | Sumitomo Metal Industries, Ltd. | Method of manufacturing seamless tube formed of titanium material |
| DE4019117A1 (en) * | 1990-06-12 | 1991-12-19 | Mannesmann Ag | Titanium (alloy) tubing prodn. - by welding together strip, cold rolling and recrystallisation annealing |
| CN1370640A (en) * | 2001-02-17 | 2002-09-25 | Sms米尔股份有限公司 | Seamless copper tube cold rolling process |
| JP2006122932A (en) * | 2004-10-27 | 2006-05-18 | Jfe Steel Kk | Manufacturing method of low yield ratio ERW steel pipe for line pipe |
| CN101708511A (en) * | 2007-12-13 | 2010-05-19 | 攀钢集团四川长城特殊钢有限责任公司 | Method for manufacturing pure titanium seamless tubes |
| CN101704035A (en) * | 2009-11-26 | 2010-05-12 | 北京有色金属研究总院 | Processing method of high-strength titanium alloy thin-walled tube stock |
Cited By (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102909237B (en) * | 2012-11-22 | 2015-09-09 | 宁夏东方钽业股份有限公司 | A kind of preparation method of TA18 thick-wall tube |
| CN102909237A (en) * | 2012-11-22 | 2013-02-06 | 宁夏东方钽业股份有限公司 | Preparation method of TA18 thick-wall tube |
| CN103358100A (en) * | 2013-07-26 | 2013-10-23 | 江南工业集团有限公司 | Forging and molding process method for titanium alloy tubular piece |
| CN103358100B (en) * | 2013-07-26 | 2015-07-01 | 江南工业集团有限公司 | Forging and molding process method for titanium alloy tubular piece |
| CN104561912B (en) * | 2013-10-15 | 2017-10-13 | 宁波江丰电子材料股份有限公司 | The preparation method of titanium focusing ring |
| CN104561912A (en) * | 2013-10-15 | 2015-04-29 | 宁波江丰电子材料股份有限公司 | Production method of titanium focus ring |
| CN103894441A (en) * | 2014-03-20 | 2014-07-02 | 宝鸡拓普达钛业有限责任公司 | Machining method of TC4 titanium alloy thick-wall tubular product |
| CN103894441B (en) * | 2014-03-20 | 2016-06-29 | 宝鸡拓普达钛业有限责任公司 | The processing method of TC4 titanium alloy thick-wall pipe material |
| CN104624713A (en) * | 2014-12-17 | 2015-05-20 | 北京有色金属研究总院 | Fabrication method of small precise thin-wall seamless titanium alloy tube |
| CN105478523A (en) * | 2015-11-27 | 2016-04-13 | 宝鸡市利泰有色金属有限公司 | Preparation technology for medical beta type titanium alloy capillary tubes |
| CN105568195A (en) * | 2015-12-25 | 2016-05-11 | 北京有色金属研究总院 | Preparation method for high-accuracy and high-strength titanium alloy seamless tubes |
| CN106282867B (en) * | 2016-09-05 | 2018-08-14 | 攀钢集团攀枝花钢铁研究院有限公司 | TA2 thin-wall titanium alloy seamless steel pipes and preparation method thereof |
| CN106282867A (en) * | 2016-09-05 | 2017-01-04 | 攀钢集团攀枝花钢铁研究院有限公司 | TA2 thin-wall titanium alloy seamless steel pipe and preparation method thereof |
| CN107738070A (en) * | 2017-09-29 | 2018-02-27 | 宝鸡市金海源钛标准件制品有限公司 | A kind of preparation method of titanium alloy seamless pipe |
| CN108188196A (en) * | 2017-12-04 | 2018-06-22 | 中国科学院金属研究所 | A kind of FeCrAl/Zr composite bimetal pipes and preparation method thereof |
| CN108188196B (en) * | 2017-12-04 | 2019-10-11 | 中国科学院金属研究所 | A kind of FeCrAl/Zr bimetal composite pipe and its preparation method |
| CN109513766A (en) * | 2018-11-15 | 2019-03-26 | 南通金尼新材料科技有限公司 | A kind of manufacturing method of high concentricity martensitic stainless steel seamless pipe material |
| CN111014337A (en) * | 2019-12-01 | 2020-04-17 | 重庆金世利航空材料有限公司 | Preparation method of non-porous extruded titanium alloy pipe |
| CN111014337B (en) * | 2019-12-01 | 2024-02-09 | 重庆金世利航空材料有限公司 | Preparation method of nonporous extruded titanium alloy pipe |
| CN112605123B (en) * | 2020-11-30 | 2022-03-15 | 西北有色金属研究院 | Preparation method of low-cost high-toughness titanium alloy pipe for ocean engineering |
| CN112605123A (en) * | 2020-11-30 | 2021-04-06 | 西北有色金属研究院 | Preparation method of low-cost high-toughness titanium alloy pipe for ocean engineering |
| CN113458176A (en) * | 2021-06-30 | 2021-10-01 | 浙江久立特材科技股份有限公司 | Manufacturing method of high-precision outer hexagonal and inner circular seamless tube with special-shaped cross section for nuclear power |
| CN115846456A (en) * | 2022-12-14 | 2023-03-28 | 安徽宝泰特种材料有限公司 | Manufacturing method of TA18 titanium alloy seamless small-caliber pipe |
| CN116984833A (en) * | 2023-07-06 | 2023-11-03 | 中国航发哈尔滨东安发动机有限公司 | Processing method of nickel-based superalloy pipe |
| CN116921491A (en) * | 2023-07-14 | 2023-10-24 | 中国航发北京航空材料研究院 | Preparation method of high-strength titanium alloy pipe |
| CN116656994A (en) * | 2023-07-25 | 2023-08-29 | 成都先进金属材料产业技术研究院股份有限公司 | Method for improving shrinkage strain ratio of TA18 titanium alloy seamless tube and TA18 titanium alloy seamless tube |
| CN116656994B (en) * | 2023-07-25 | 2023-10-13 | 成都先进金属材料产业技术研究院股份有限公司 | Method for improving shrinkage strain ratio of TA18 titanium alloy seamless tube and TA18 titanium alloy seamless tube |
| CN118437767A (en) * | 2024-07-08 | 2024-08-06 | 西安稀有金属材料研究院有限公司 | Preparation method of high-precision ultra-large caliber thin-wall Ti35 titanium alloy pipe |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105568195A (en) | Preparation method for high-accuracy and high-strength titanium alloy seamless tubes | |
| CN112404163B (en) | A preparation method of high-performance difficult-to-deform metal precision seamless pipe | |
| CN102836895B (en) | A kind of manufacture method of special-shaped seamless steel pipe | |
| CN102294579B (en) | Method for manufacturing thin-wall and ultra-long nickel-copper alloy pipes | |
| CN107052076B (en) | A kind of method of collet plug hot rolling heavy caliber titanium or titanium alloy thin-wall seamless pipe | |
| CN103846305B (en) | The preparation processing method of a kind of major diameter tubing and special piece | |
| CN113695417B (en) | Preparation method of large-caliber high-performance titanium alloy pipe and product thereof | |
| CN103170797B (en) | The Compound Extrusion preparation method of a kind of major diameter high-quality pipe or ring base | |
| CN112044978B (en) | Preparation method of high temperature and pressure resistant titanium alloy small size thick wall pipe | |
| CN101176882A (en) | Process technique of high-strength titanium alloy pipes | |
| CN102463272A (en) | Short-process preparation method of small-caliber nickel-based alloy thin-wall pipe | |
| CN101708511A (en) | Method for manufacturing pure titanium seamless tubes | |
| CN107649531A (en) | A kind of processing method of titanium alloy large-calibre seamless thin-wall pipes | |
| CN101352796A (en) | Novel technique for producing mandrel bar | |
| CN105499920B (en) | A kind of manufacturing method of heavy caliber thick wall seamless niobium tubing material | |
| CN106425317A (en) | Preparation method of Ti-B19 high-strength titanium alloy large-caliber thick wall pipe | |
| CN102632175A (en) | Radial forging process of cast-state magnesium alloy tube | |
| CN103817168A (en) | Drawing production process of monel alloy pipe | |
| CN113976659A (en) | Method for manufacturing metal pipe based on external field auxiliary additive | |
| CN102873126B (en) | Manufacturing method of large-aperture thin-walled seamless steel tube for nuclear power plant | |
| CN105441713A (en) | A titanium alloy seamless tube and a manufacturing method thereof | |
| CN104551547A (en) | Processing process of high-intensity titanium alloy pipe fittings | |
| CN104759849A (en) | Manufacturing method for flange component for controlling automobile exhaust | |
| CN110340148A (en) | A kind of roll piercing method of ocean diphasic titanium alloy seamless tube blank | |
| CN114260314B (en) | Manufacturing method of titanium alloy seamless tube blank with diameter-thickness ratio larger than 20 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20120314 |