CN101920437A - A flat knurling process for the inner and outer surfaces of sputtered tantalum rings - Google Patents

A flat knurling process for the inner and outer surfaces of sputtered tantalum rings Download PDF

Info

Publication number
CN101920437A
CN101920437A CN 201010258810 CN201010258810A CN101920437A CN 101920437 A CN101920437 A CN 101920437A CN 201010258810 CN201010258810 CN 201010258810 CN 201010258810 A CN201010258810 A CN 201010258810A CN 101920437 A CN101920437 A CN 101920437A
Authority
CN
China
Prior art keywords
annular knurl
tantalum
dull
internally
surfaces externally
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Granted
Application number
CN 201010258810
Other languages
Chinese (zh)
Other versions
CN101920437B (en
Inventor
李桂鹏
张春恒
同磊
赵兵
王莉
汪凯
赵红运
李兆博
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
Ningxia Orient Tantalum Industry Co Ltd
National Engineering Research Center for Special Metal Materials of Tantalim and Niobium
Original Assignee
Ningxia Orient Tantalum Industry Co Ltd
National Engineering Research Center for Special Metal Materials of Tantalim and Niobium
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by Ningxia Orient Tantalum Industry Co Ltd, National Engineering Research Center for Special Metal Materials of Tantalim and Niobium filed Critical Ningxia Orient Tantalum Industry Co Ltd
Priority to CN 201010258810 priority Critical patent/CN101920437B/en
Publication of CN101920437A publication Critical patent/CN101920437A/en
Application granted granted Critical
Publication of CN101920437B publication Critical patent/CN101920437B/en
Expired - Fee Related legal-status Critical Current
Anticipated expiration legal-status Critical

Links

Images

Landscapes

  • Physical Vapour Deposition (AREA)

Abstract

本发明涉及一种溅射钽环件内外表面的平板滚花工艺,其工艺过程为:首先制备钽条,圆弧铣削,上下表面滚花,圆周滚花,卷圆即可。通过本发明可实现开口溅射钽环件的内外表面及侧边形成均匀一致的80TPI凸菱形花纹,从而满足半导体用户的使用要求。

Figure 201010258810

The invention relates to a flat plate knurling process for the inner and outer surfaces of a sputtered tantalum ring. The process is as follows: firstly prepare a tantalum bar, arc milling, knurling on the upper and lower surfaces, knurling on the circumference, and rolling into a circle. The invention can realize the uniform and consistent 80TPI convex diamond pattern on the inner and outer surfaces and sides of the open sputtering tantalum ring, thereby meeting the use requirements of semiconductor users.

Figure 201010258810

Description

A kind of dull and stereotyped annular knurl technology of sputtering tantalum ring surfaces externally and internally
Technical field
The invention belongs to the mechanical processing technique of tantalum material, particularly relate to a kind of dull and stereotyped annular knurl technology of sputtering tantalum ring surfaces externally and internally.
Background technology
Physical vapor deposition (PVD) is one of technology of most critical in the semiconductor chip production process, its objective is the form of the compound of metal or metal with film deposited on silicon chip or other the substrate, and, finally form distribution structure complicated in the semiconductor chip subsequently by the cooperating of technologies such as photoetching and corrosion.Physical vapour deposition (PVD) is finished by the sputter board, and sputtering tantalum ring is exactly a very important crucial consumptive material that is used for above-mentioned technology.
The main effect of sputtering tantalum ring in semiconductor technology has 2 points:
First: the movement locus of constraint sputtering particle, play the effect of focusing;
Second: the big particle that produces in the absorption sputter procedure, play the effect of purification.
Since the special environment for use of sputtering tantalum ring, thereby its requirement to surface knurling is very strict, and be specially: surface knurling is the rhombus that 80TPI protrudes, and 80 road decorative patterns had both been arranged in one inch scope, and annular knurl is even, the no visual flat spot in surface.But, in actual production, there is following difficult point:
First: ring is the opening ring, and surface knurling not only requires the lines unanimity, and requires depth unanimity:
Second: the ring side is a circular arc;
The 3rd: circular arc requires annular knurl consistent with surface knurling.
At present, the annular knurl of sputtering tantalum ring surfaces externally and internally can only be produced abroad, and domestic also do not have relevant mature technology to exist.
Summary of the invention
The objective of the invention is to overcome the defective of above-mentioned prior art, provide a kind of and can produce the volume circle electroplating equipment wielding machine annular knurl technology that texture structure satisfies the sputtering tantalum ring surfaces externally and internally of semiconductor user instructions for use.
For achieving the above object, the present invention adopts following technical proposals:
A kind of dull and stereotyped annular knurl technology of sputtering tantalum ring surfaces externally and internally is characterized in that technical process is: at first prepare the tantalum bar, and the circular arc milling, the upper and lower surface annular knurl, the circumference annular knurl, the volume circle gets final product;
The tantalum bar flatness≤0.15mm of above-mentioned preparation, the tantalum bar with plate poor≤0.127mm;
Adopt the mode of vacuum cup to locate the tantalum bar during above-mentioned circular arc milling, used milling cutter is a circular arc milling cutter;
Above-mentioned upper and lower surface annular knurl is to roll on the furling plate round machine two to finish, and wherein the up-down rollers of this furling plate round machine is the roller of band lines;
Adopt the mode of vacuum cup to locate the tantalum bar during above-mentioned circumference annular knurl, used knurling tool is the circular arc knurling tool;
The drafts of the each moulding of above-mentioned volume bowlder is finished by 5~7 moulding less than 1mm;
Above-mentioned volume bowlder is controlled circularity≤1.0mm at the upper and lower surface pad rubber skin of tantalum bar.
Can realize the protruding Argyle of 80TPI of the formation uniformity of the surfaces externally and internally of opening sputtering tantalum ring and side by the present invention, thereby satisfy semiconductor user's instructions for use.
Description of drawings
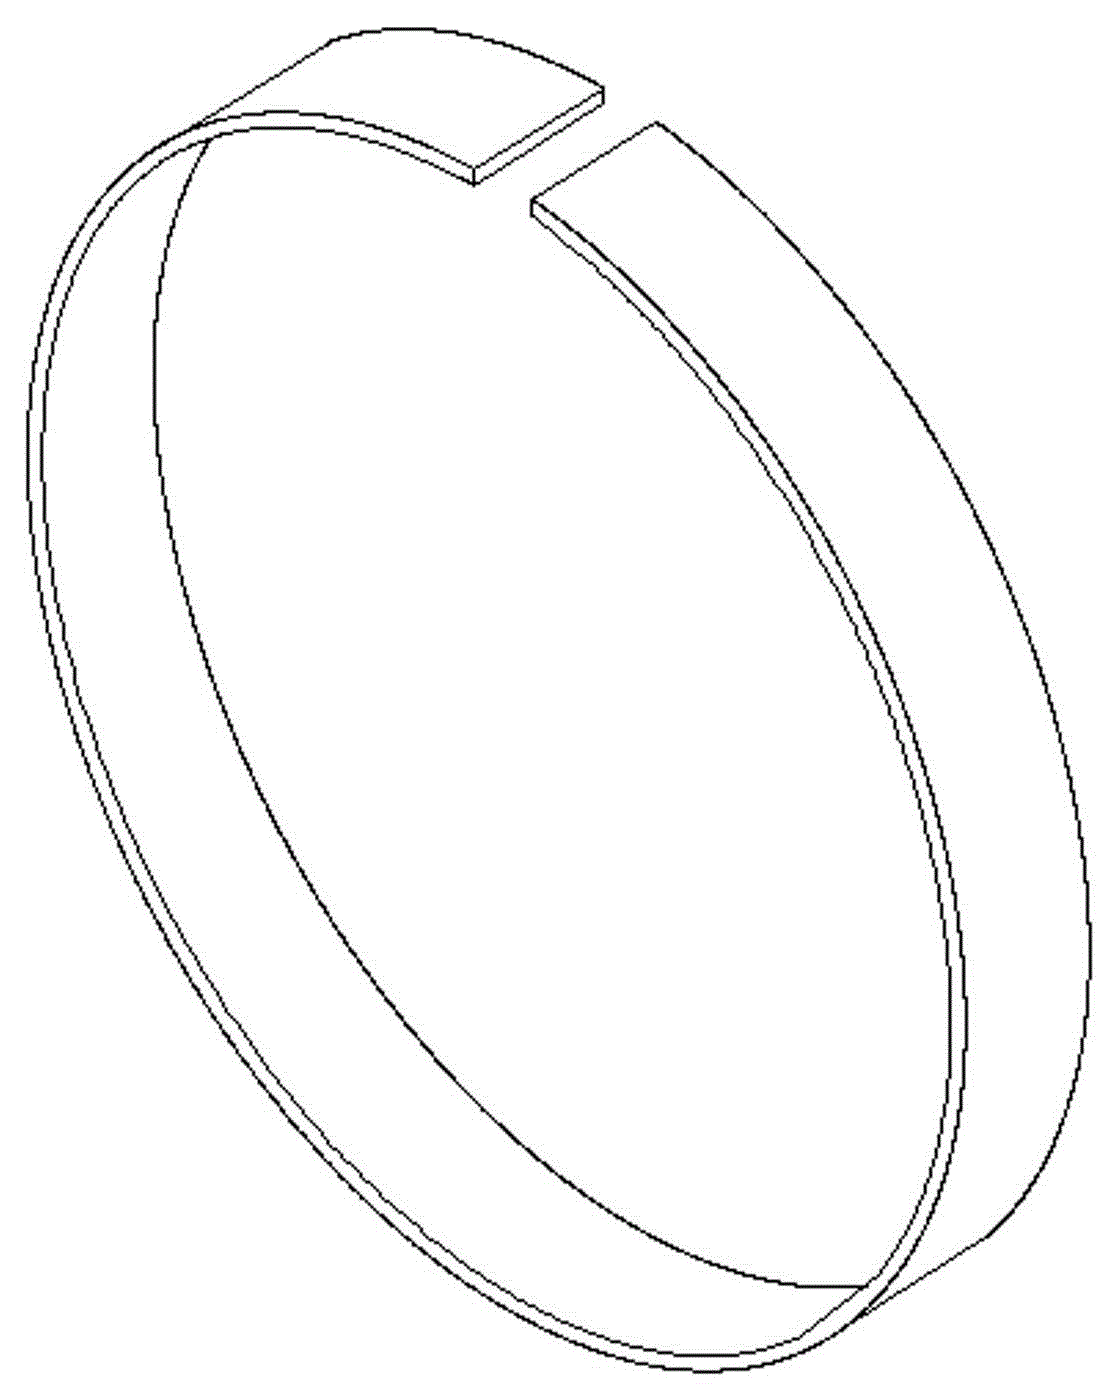
Fig. 1 is the structural representation of opening sputtering tantalum ring of the present invention;
Fig. 2 is the texture schematic diagram of the surfaces externally and internally of Fig. 1;
Fig. 3 is a side texture schematic diagram among Fig. 1.
The specific embodiment
The concrete processing step of the board joint annular knurl of sputtering tantalum ring surfaces externally and internally of the present invention is as follows:
1, tantalum bar preparation
In order to satisfy carrying out smoothly of subsequent technique, the preparation of tantalum bar must be satisfied two essential conditions: the first, and tantalum bar flatness≤0.15mm; The second, the tantalum bar with plate poor≤0.127mm.Because when the tantalum bar is smoothed, all can produce the folding line that to smooth, the existence of this folding line in the termination of charging, have a strong impact on the flatness of whole tantalum bar, so length is reserved 50mm more when blanking, after smoothing, termination creasy sawing is removed, guarantee flatness; Handle by whole tantalum bar surface finish, the tantalum bar is met the requirements with the plate difference.
2, circular arc milling
In order to realize tantalum bar side circular arc milling uniformity all around, must guarantee that tantalum bar clamping is straight, otherwise circular arc can misrun occur or circular arc molding is not in place, this defective user is receptible anything but.Because tantalum does not have magnetic,, not only can guarantee the straight of tantalum bar, and can realize clamping No. one time that one-shot forming avoids occurring connecing tool marks so adopt the mode of vacuum cup to locate workpiece.Milling cutter adopts special-purpose circular arc milling cutter.
3, upper and lower surface annular knurl
The upper and lower surface annular knurl rolls furling plate round machine special-purpose two and finishes, and the down roller of furling plate round machine changes the roller of band lines into.This frock must possess following some requirement: the first, and the gap of two rollers up and down, left and right sides error≤0.05mm; The second, must interlock about when regulating the gap; The 3rd, positioning and guiding is arranged.
4, circumference annular knurl
Installation way adopts special-purpose circular arc knurling tool with step 2.
5, volume circle
When the circularity of volume bowlder after guaranteeing moulding met the demands, more crucial was to guarantee that decorative pattern is excellent, defectives such as line can not occur down.For this reason, the volume circle adopts repeatedly moulding of light reduction, and promptly the drafts of each moulding is finished by 5~7 moulding less than 1mm.Must fill up the thick white glues skin of 5mm about the tantalum bar simultaneously when moulding, rubber promptly cancelled not reproducible use after every collar member was finished the volume circle.
Claims (7)

1. the dull and stereotyped annular knurl technology of a sputtering tantalum ring surfaces externally and internally is characterized in that technical process is: at first prepare the tantalum bar, and the circular arc milling, the upper and lower surface annular knurl, the circumference annular knurl, the volume circle gets final product.
2. according to the dull and stereotyped annular knurl technology of the described sputtering tantalum ring surfaces externally and internally of claim 1, it is characterized in that: the tantalum bar flatness≤0.15mm of above-mentioned preparation, the tantalum bar with plate poor≤0.127mm.
3. according to the dull and stereotyped annular knurl technology of the described sputtering tantalum ring surfaces externally and internally of claim 1, it is characterized in that: adopt the mode of vacuum cup to locate the tantalum bar during above-mentioned circular arc milling, used milling cutter is a circular arc milling cutter.
4. according to the dull and stereotyped annular knurl technology of the described sputtering tantalum ring surfaces externally and internally of claim 1, it is characterized in that: above-mentioned upper and lower surface annular knurl is to roll on the furling plate round machine two to finish, and wherein the up-down rollers of this furling plate round machine is the roller of band lines.
5. according to the dull and stereotyped annular knurl technology of the described sputtering tantalum ring surfaces externally and internally of claim 1, it is characterized in that: adopt the mode of vacuum cup to locate the tantalum bar during above-mentioned circumference annular knurl, used knurling tool is the circular arc knurling tool.
6. according to the dull and stereotyped annular knurl technology of the described sputtering tantalum ring surfaces externally and internally of claim 1, it is characterized in that: the drafts of the each moulding of above-mentioned volume bowlder is finished by 5~7 moulding less than 1mm.
7. according to the dull and stereotyped annular knurl technology of claim 1 or 6 described sputtering tantalum ring surfaces externally and internallies, it is characterized in that: above-mentioned volume bowlder is controlled circularity≤1.0mm at the upper and lower surface pad rubber skin of tantalum bar.
CN 201010258810 2010-08-20 2010-08-20 Flat knurling process for sputtering inner and outer surfaces of tantalum ring Expired - Fee Related CN101920437B (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN 201010258810 CN101920437B (en) 2010-08-20 2010-08-20 Flat knurling process for sputtering inner and outer surfaces of tantalum ring

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN 201010258810 CN101920437B (en) 2010-08-20 2010-08-20 Flat knurling process for sputtering inner and outer surfaces of tantalum ring

Publications (2)

Publication Number Publication Date
CN101920437A true CN101920437A (en) 2010-12-22
CN101920437B CN101920437B (en) 2011-09-07

Family

ID=43335788

Family Applications (1)

Application Number Title Priority Date Filing Date
CN 201010258810 Expired - Fee Related CN101920437B (en) 2010-08-20 2010-08-20 Flat knurling process for sputtering inner and outer surfaces of tantalum ring

Country Status (1)

Country Link
CN (1) CN101920437B (en)

Cited By (5)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN104439889A (en) * 2014-12-09 2015-03-25 贵州红林机械有限公司 Method of sinusoidal curve knurling by four-axis linkage
CN105695942A (en) * 2014-11-28 2016-06-22 宁波江丰电子材料股份有限公司 Ring part structure and manufacturing method thereof
CN106493525A (en) * 2016-12-23 2017-03-15 有研亿金新材料有限公司 A kind of preparation method of sputtering titanacycle
CN107717462A (en) * 2016-08-11 2018-02-23 宁波江丰电子材料股份有限公司 Annular element fracture knurling device and annular element fracture rose work method
CN106475728B (en) * 2015-08-24 2018-05-18 宁波江丰电子材料股份有限公司 A kind of repairing and reusing method of column handle on tantalum ring

Citations (5)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
WO2005038079A1 (en) * 2003-09-25 2005-04-28 Honeywell International Inc. Pvd component and coil refurbishing methods
CN101565819A (en) * 2009-06-04 2009-10-28 西北稀有金属材料研究院 Magnetic controlled sputtering ring
CN101574780A (en) * 2009-06-04 2009-11-11 西北稀有金属材料研究院 Production method and press tool for tantalum umbo body used by magnetic-control sputtering ring piece
CN101574766A (en) * 2009-06-04 2009-11-11 西北稀有金属材料研究院 Flexible rose work method and cutter for ring body surface used by magnetic-control sputtering ring piece
CN201538814U (en) * 2009-11-12 2010-08-04 宁波江丰电子材料有限公司 Component of tantalum sputtering ring

Patent Citations (5)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
WO2005038079A1 (en) * 2003-09-25 2005-04-28 Honeywell International Inc. Pvd component and coil refurbishing methods
CN101565819A (en) * 2009-06-04 2009-10-28 西北稀有金属材料研究院 Magnetic controlled sputtering ring
CN101574780A (en) * 2009-06-04 2009-11-11 西北稀有金属材料研究院 Production method and press tool for tantalum umbo body used by magnetic-control sputtering ring piece
CN101574766A (en) * 2009-06-04 2009-11-11 西北稀有金属材料研究院 Flexible rose work method and cutter for ring body surface used by magnetic-control sputtering ring piece
CN201538814U (en) * 2009-11-12 2010-08-04 宁波江丰电子材料有限公司 Component of tantalum sputtering ring

Cited By (7)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN105695942A (en) * 2014-11-28 2016-06-22 宁波江丰电子材料股份有限公司 Ring part structure and manufacturing method thereof
CN105695942B (en) * 2014-11-28 2020-07-17 宁波江丰电子材料股份有限公司 Ring piece structure and manufacturing method thereof
CN104439889A (en) * 2014-12-09 2015-03-25 贵州红林机械有限公司 Method of sinusoidal curve knurling by four-axis linkage
CN106475728B (en) * 2015-08-24 2018-05-18 宁波江丰电子材料股份有限公司 A kind of repairing and reusing method of column handle on tantalum ring
CN107717462A (en) * 2016-08-11 2018-02-23 宁波江丰电子材料股份有限公司 Annular element fracture knurling device and annular element fracture rose work method
CN107717462B (en) * 2016-08-11 2019-07-30 宁波江丰电子材料股份有限公司 Annular element fracture knurling device and annular element fracture rose work method
CN106493525A (en) * 2016-12-23 2017-03-15 有研亿金新材料有限公司 A kind of preparation method of sputtering titanacycle

Also Published As

Publication number Publication date
CN101920437B (en) 2011-09-07

Similar Documents

Publication Publication Date Title
CN109824249A (en) A kind of 3D glass making procedures
WO2019041828A1 (en) Roll for rolling surface topography of steel plate and method for manufacturing same
CN102886381A (en) Thick plate rolling method
CN105149662B (en) A kind of glass steel material cone circle shell pieces class method of processing parts
CN105946432A (en) Deep-drawing production technique for stainless steel shuttle-shaped artware
CN101434026A (en) High-melting metal arc spraying rapid die-manufacturing method
CN102157714B (en) Method for machining battery cover, battery cover and mobile terminal of battery cover
CN101920437B (en) Flat knurling process for sputtering inner and outer surfaces of tantalum ring
CN103602981B (en) SMT ladder template fabrication
CN102069359A (en) Method for processing defensive move plate structure
CN101920438B (en) Coiling machine continuous knurling technique on inner and outer surfaces of sputtering tantalum ring
CN105506533A (en) Production technology of printing roll
CN204934205U (en) A kind of Combined hard-alloy composite ring
CN101906656B (en) Electrolysis vehicle tool cathode
CN105522335A (en) Machining method for large-size stainless steel rotary screen
CN101920439A (en) A round welding knurling process for the inner and outer surfaces of sputtered tantalum rings
CN105345405B (en) A kind of agricultural machinery rim for automobile wheel contour roll forming technique
TWI382914B (en) Method for manufacture of roller printing molds
CN102974874B (en) The processing method of a kind of golf iron scope of attack and scope of attack duct
CN108581391A (en) The processing method of slot grinding after a kind of groove milling of machine tap elder generation
CN107745231A (en) A kind of preparation method of high-precision titanium copper composite bar
CN112658865A (en) Grooving method for resin grinding wheel
CN207806647U (en) A Composite Forming Tool for Rough and Finish Machining
CN105690481A (en) Die cutting rule roller with cutting edge made of two-dimensional gradient material
CN207288993U (en) A kind of new high rigidity ball knife

Legal Events

Date Code Title Description
C06 Publication
PB01 Publication
C10 Entry into substantive examination
SE01 Entry into force of request for substantive examination
C14 Grant of patent or utility model
GR01 Patent grant
CF01 Termination of patent right due to non-payment of annual fee

Granted publication date: 20110907

Termination date: 20180820