CN101862845A - Eccentric rapid clamping fixture - Google Patents
Eccentric rapid clamping fixture Download PDFInfo
- Publication number
- CN101862845A CN101862845A CN201010120026A CN201010120026A CN101862845A CN 101862845 A CN101862845 A CN 101862845A CN 201010120026 A CN201010120026 A CN 201010120026A CN 201010120026 A CN201010120026 A CN 201010120026A CN 101862845 A CN101862845 A CN 101862845A
- Authority
- CN
- China
- Prior art keywords
- eccentric
- clamping fixture
- rapid clamping
- base plate
- fixture according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- NJPPVKZQTLUDBO-UHFFFAOYSA-N novaluron Chemical compound C1=C(Cl)C(OC(F)(F)C(OC(F)(F)F)F)=CC=C1NC(=O)NC(=O)C1=C(F)C=CC=C1F NJPPVKZQTLUDBO-UHFFFAOYSA-N 0.000 claims description 20
- 230000001105 regulatory effect Effects 0.000 claims description 3
- 238000005553 drilling Methods 0.000 abstract description 2
- 239000000758 substrate Substances 0.000 abstract 3
- 238000000034 method Methods 0.000 description 5
- 238000005516 engineering process Methods 0.000 description 2
- 238000003754 machining Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000000295 complement effect Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000004080 punching Methods 0.000 description 1
Images


Landscapes
- Drilling And Boring (AREA)
Abstract
The invention provides an eccentric rapid clamping fixture which comprises a machine frame and a substrate, wherein the machine frame is used for loading workpieces, and a drilling duct for processing workpieces is arranged on the top of the machine frame; and the substrate is movably arranged on a bottom plate of the machine frame, an eccentric roller for supporting the workpieces and a control component for adjusting the eccentric roller to rotate are supported on the substrate. Compared with the prior art, the invention has the advantages of simple operation, convenient processing and lower processing cost.
Description
Technical field
The present invention relates to a kind of eccentric rapid clamping fixture, especially a kind of eccentric rapid clamping fixture that workpiece is holed of being used for.
Background technology
Processing for workpiece, sometimes need on workpiece, process inclined hole, but in the actual job process, for guaranteeing drilling quality, generally all the drill bit direction is set to level or vertical, so that processing boring in minimal error, and such setting, make when needs are processed inclined hole on workpiece, existing process technology be difficult to realize, can only just avoid designing inclined hole when design, and is other form structures in the partial design that needs inclined hole, but a lot of such replacing designs all can cause the raising of manufacturing cost, the complexity of machining tool, influence whole work-piece processing.
Summary of the invention
In order to solve above-mentioned technical problem, the object of the present invention is to provide a kind of conveniently eccentric rapid clamping fixture of processing inclined hole on workpiece.
Purpose of the present invention is achieved through the following technical solutions:
A kind of eccentric rapid clamping fixture, comprise that one loads the frame of workpiece, described frame top is provided with a drill pipe that is used for processing work, wherein, described eccentric rapid clamping fixture comprises that also one is movably set in the pedestal on the described framework soleplate, described base support has one to be used for the eccentric cylinder of holding workpieces, and the control piece of adjusting described eccentric cylinder rotation.
Further, described frame comprises that also one is supported on the support and the template that is supported on described support of described base plate.
Described workpiece setting is between described eccentric cylinder and described template.
Described drill pipe is arranged in the described template.
Also be provided with a locating part that is used for spacing workpiece on the described template.
Again further, described eccentric rapid clamping fixture comprises that also one regulates the adjustment screw of described pedestal and described base plate relative position.
Also be provided with a metallic channel on the described base plate, described pedestal is provided with the guide pad of the described gathering sill of a cooperation.
Described adjustment screw is regulated described guide pad and is slided in described gathering sill.
Further, described pedestal and described base plate comprise one first relative position and one second relative position.
Described workpiece comprises a mass axis, and described mass axis is the 2-5 degree at the differential seat angle of described pedestal and described base plate first relative position and second relative position.
Compared with prior art, the invention has the beneficial effects as follows: simple to operate, easy to process, and processing cost is lower.
Description of drawings
Below in conjunction with accompanying drawing technical solution of the present invention is described further:
Fig. 1 is the schematic perspective view according to the best mode for carrying out the invention eccentric rapid clamping fixture.
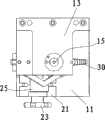
Fig. 2 is the partial perspective front view according to the best mode for carrying out the invention eccentric rapid clamping fixture.
Fig. 3 is the front view according to the best mode for carrying out the invention eccentric rapid clamping fixture.
Fig. 4 is the vertical view according to the best mode for carrying out the invention eccentric rapid clamping fixture.
The specific embodiment
The present invention is further detailed explanation below in conjunction with the drawings and specific embodiments:
As shown in Figures 1 to 4, eccentric rapid clamping fixture in best mode for carrying out the invention comprises a frame, described frame comprises base plate 11, is supported on the support 12 of described base plate 11, and the template 13 that is supported on described support 12, wherein, described base plate 11, support 12, template 13 can be fixedly connected, also plastic in one, described template 13 tops offer one and are used to guide drill bit to the hole drill pipe 15 of processing of workpiece, and described template 13 bottom surfaces also are provided with one and are used for carrying out spacing location fork 17 to desiring processing work.
At described base plate 11 upper supports one pedestal 21 is arranged, described pedestal 21 can with described base plate 11 relative slips.Wherein, described pedestal 21 vertical two ends convex with two support members, one eccentric cylinder 25 is installed between described two support members, in the described support member outside, also be provided with a handwheel 23, described eccentric cylinder 25 1 ends connect described handwheel 23, and can be by described handwheel 23 driven rotary, to adjust the maximum height of described eccentric cylinder 25.
Can put into workpiece 30 at described eccentric cylinder 25 and 13 of described templates, the end face of this workpiece 30 is complementary is arranged at described template 13 bottom surfaces, as shown in Figure 2, described workpiece 30 comprises a mass axis A, after workpiece 30 is installed on described eccentric rapid clamping fixture, drill bit can be directed downwards punching at vertical ground by drill pipe 15, on workpiece 30, process boring 31, these boring 31 relative workpiece 30 then are obliquely installed, so its relative workpiece 30 is an inclined hole, thereby has reached processing purpose.
Preferably, also be provided with a gathering sill 19 on the described base plate 11, described gathering sill 19 can cooperate the guide pad 29 that is provided with on the described pedestal 21, make described pedestal 21 to slide by described relatively base plate 11, end at described pedestal 21 also is provided with an adjustment screw 27, this adjustment screw 27 can be regulated the relative position of described pedestal 21 and described base plate 11, thereby regulates the relative position of eccentric cylinder 25 with respect to described pedestal 21.
Using eccentric rapid clamping fixture of the present invention that workpiece is added man-hour, at first, described workpiece 30 is positioned on the described eccentric cylinder 25, and adjusts its height, make described workpiece 30 be clamped between described eccentric cylinder 25 and described template 13 bottom surfaces by described handwheel 23; Reconcile described adjustment screw 27 again, make the described eccentric cylinder 25 and the contact point propelling of described workpiece 30 be the peak of described eccentric cylinder 25, and by described workpiece 30 positions, fork 17 location, described location, this moment, described workpiece 30 mass axis A were in second relative position of pedestal and base plate, the differential seat angle that is in first relative position of pedestal and base plate with the preceding workpiece 30 mass axis A of adjusting is the 2-5 degree, at last, with drill bit by behind the described drill pipe 15, to the processing of holing of described workpiece 30, and after machining, loosen described workpiece 30 by adjustment screw 27 and handwheel 23, conveniently to take off described workpiece 30.
Although be the example purpose, preferred implementation of the present invention is disclosed, but those of ordinary skill in the art will recognize that under situation about not breaking away from by the disclosed scope and spirit of the present invention of appending claims, various improvement, increase and replacement are possible.
Claims (10)
1. eccentric rapid clamping fixture, comprise that one loads the frame of workpiece, described frame top is provided with a drill pipe that is used for processing work, it is characterized in that: described eccentric rapid clamping fixture comprises that also one is movably set in the pedestal on the base plate of described frame, described base support has one to be used for the eccentric cylinder of holding workpieces, and the control piece of adjusting described eccentric cylinder rotation.
2. eccentric rapid clamping fixture according to claim 1 is characterized in that: described frame comprises that also one is supported on the support and the template that is supported on described support of described base plate.
3. eccentric rapid clamping fixture according to claim 2 is characterized in that: described workpiece setting is between described eccentric cylinder and described template.
4. eccentric rapid clamping fixture according to claim 3 is characterized in that: described drill pipe is arranged in the described template.
5. eccentric rapid clamping fixture according to claim 4 is characterized in that: also be provided with a locating part that is used for spacing workpiece on the described template.
6. eccentric rapid clamping fixture according to claim 1 is characterized in that: described eccentric rapid clamping fixture comprises that also one regulates the adjustment screw of described pedestal and described base plate relative position.
7. eccentric rapid clamping fixture according to claim 6 is characterized in that: also be provided with a gathering sill on the described base plate, described pedestal is provided with the guide pad of the described gathering sill of a cooperation.
8. eccentric rapid clamping fixture according to claim 7 is characterized in that: described adjustment screw is regulated described guide pad and is slided in described gathering sill.
9. eccentric rapid clamping fixture according to claim 1 is characterized in that: described pedestal and described base plate comprise one first relative position and one second relative position.
10. eccentric rapid clamping fixture according to claim 9 is characterized in that: described workpiece comprises a mass axis, and described mass axis is the 2-5 degree at the differential seat angle of described pedestal and described base plate first relative position and second relative position.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201010120026A CN101862845A (en) | 2010-02-09 | 2010-02-09 | Eccentric rapid clamping fixture |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201010120026A CN101862845A (en) | 2010-02-09 | 2010-02-09 | Eccentric rapid clamping fixture |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN101862845A true CN101862845A (en) | 2010-10-20 |
Family
ID=42954877
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201010120026A Pending CN101862845A (en) | 2010-02-09 | 2010-02-09 | Eccentric rapid clamping fixture |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN101862845A (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103158045A (en) * | 2011-12-19 | 2013-06-19 | 沈阳黎明航空发动机(集团)有限责任公司 | Universal composite swelling device for blade grind |
| CN103170850A (en) * | 2013-03-22 | 2013-06-26 | 苏州工业园区艺达精密机械有限公司 | Fast angle drilling jig |
| CN103240325A (en) * | 2013-05-17 | 2013-08-14 | 苏州创丰精密五金有限公司 | Inclined hole drilling fixture |
| CN107414550A (en) * | 2017-08-08 | 2017-12-01 | 格林精密部件(苏州)有限公司 | A kind of quick gripping mechanism of Novel workpiece |
| CN107717733A (en) * | 2017-09-29 | 2018-02-23 | 天津豪鑫精密模具有限公司 | One kind is used for the adjustable inclination frock of workpiece grinding |
-
2010
- 2010-02-09 CN CN201010120026A patent/CN101862845A/en active Pending
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103158045A (en) * | 2011-12-19 | 2013-06-19 | 沈阳黎明航空发动机(集团)有限责任公司 | Universal composite swelling device for blade grind |
| CN103170850A (en) * | 2013-03-22 | 2013-06-26 | 苏州工业园区艺达精密机械有限公司 | Fast angle drilling jig |
| CN103240325A (en) * | 2013-05-17 | 2013-08-14 | 苏州创丰精密五金有限公司 | Inclined hole drilling fixture |
| CN103240325B (en) * | 2013-05-17 | 2015-06-17 | 苏州创丰精密五金有限公司 | Inclined hole drilling fixture |
| CN107414550A (en) * | 2017-08-08 | 2017-12-01 | 格林精密部件(苏州)有限公司 | A kind of quick gripping mechanism of Novel workpiece |
| CN107717733A (en) * | 2017-09-29 | 2018-02-23 | 天津豪鑫精密模具有限公司 | One kind is used for the adjustable inclination frock of workpiece grinding |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| KR100971810B1 (en) | Adjustable jig | |
| CN202010900U (en) | Processing clamp for wire conveying supporting plate top surface holes | |
| CN103480886B (en) | A kind of full-automatic numerical control two station lock housing bores hoodle hole machine | |
| CN104385129A (en) | Mounting fixture special for drilling leveling of bottom surface of workpiece | |
| CN205291946U (en) | High -efficient marking machine of multistation | |
| CN203484699U (en) | Automatic numerically-controlled two-station lock case hoodle aperture drilling machine | |
| CN206263304U (en) | A kind of pipe connection method orchid boring grab | |
| CN201625875U (en) | Eccentric rapid clamping tool | |
| CN208743764U (en) | A kind of workpiece end face drilling tool | |
| CN106042103A (en) | Processing equipment of bamboo block and processing method thereof | |
| CN105772779B (en) | A kind of digital control drilling machine | |
| CN101623829A (en) | Boring machine and boring machine fixture | |
| CN201455704U (en) | Boring lathe and boring lathe clamp | |
| CN208929769U (en) | A workpiece tilt positioning tool based on bench drill | |
| CN201316916Y (en) | Drilling clamp | |
| CN205888134U (en) | Hull steel fabrication lathe | |
| CN206083901U (en) | Changeable drilling machine is found to simple and easy crouching | |
| CN201446255U (en) | Fine-tuned turning tool fixture | |
| CN103128560B (en) | Method for milling single-side slope inclined base plate on end face | |
| CN203817454U (en) | Clamp | |
| CN206425597U (en) | Edge milling machines | |
| CN215510098U (en) | Hydraulic auxiliary clamp suitable for longitudinal machining of special-shaped frame body workpiece | |
| CN103157840B (en) | Method for end milling of double-sided inclined workpiece | |
| CN207255734U (en) | A kind of drilling machine processing space hole clip tool | |
| CN208854239U (en) | A kind of fuel tank cap processing tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Open date: 20101020 |