Rotary indexing processing device of tubular workpiece
Technical field
The present invention relates to the machining equipment technical field, especially a kind of rotary indexing processing device of tubular workpiece.
Background technology
In machining, original tubular workpiece is owing to not having auxiliary equipment to process on work in-process heart equipment.
Summary of the invention
The deficiency that can't process in order to overcome existing tubular workpiece the invention provides a kind of rotary indexing processing device of tubular workpiece.
The technical solution adopted for the present invention to solve the technical problems is: a kind of rotary indexing processing device of tubular workpiece, comprise base and the panoramic table that is located on base, panoramic table is provided with the baseplane locating piece, the other adjustable support that is provided with of baseplane locating piece, one end of bolt is fixed on the upper plane of panoramic table, and the other end connects pressing plate.
According to another embodiment of the invention, comprise that further base and panoramic table are flexibly connected by the calibration alignment pin, base is fixedly connected with by the panoramic table pressing plate with panoramic table.
According to another embodiment of the invention, comprise that further the panoramic table pressing plate is by screw bolt and nut and base and panoramic table flexible connection.
According to another embodiment of the invention, comprise that further the calibration alignment pin is arranged on the lower plane of panoramic table.
According to another embodiment of the invention, comprise that further base is provided with locating hole one, locating hole two and locating hole three.
According to another embodiment of the invention, the plane that further comprises the baseplane locating piece is provided with 2 alignment pins.
The invention has the beneficial effects as follows, the present invention has realized the processing on tubular workpiece work in-process heart equipment efficiently, and is simple to operation, improved working (machining) efficiency.
Description of drawings
The present invention is further described below in conjunction with drawings and Examples.
Fig. 1 is structural representation of the present invention;
Fig. 2 is the schematic diagram of one embodiment of the invention;
Fig. 3 is the top view of Fig. 2;
Fig. 4 is the schematic diagram of tubular workpiece;
Fig. 5 is the schematic cross-section of tubular workpiece in Fig. 2;
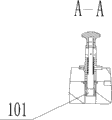
Fig. 6 is the A-A schematic diagram of calibration alignment pin.
1. bases in figure, 2. panoramic table, 3. panoramic table pressing plate, 4. calibration alignment pin, 5. baseplane locating piece, 6. adjustable support, 7. bolt, 8. pressing plate, 9. alignment pin, 101. locating hole one, 102. locating hole two, 103. locating holes three, 11 tubular workpieces, 121. workpiece machined surface one, 122. workpiece machined surface two, 123. workpiece machined surfaces three.
The specific embodiment
In conjunction with the accompanying drawings, the present invention is further detailed explanation.These accompanying drawings are the schematic diagram of simplification, basic structure of the present invention only is described in a schematic way, so it only show the formation relevant with the present invention.
Structural representation of the present invention as Fig. 1, a kind of rotary indexing processing device of tubular workpiece, this device comprises base 1 and the panoramic table 2 that is located on base 1, panoramic table 2 is provided with baseplane locating piece 5, the other adjustable support 6 that is provided with of baseplane locating piece 5, one end of bolt 7 is fixed on the upper plane of panoramic table 2, and the other end connects pressing plate 8.Base 1 and panoramic table 2 are flexibly connected by calibration alignment pin 4, and base 1 is fixedly connected with by panoramic table pressing plate 3 with panoramic table 2.The overall structure of this device is simple, practical, by inserting and extracting calibration alignment pin 4, can adjust easily the position of tubular workpiece 11.Baseplane locating piece 5 and adjustable hold 6 with the bottom of workpiece and lateral surface compressing location.Panoramic table pressing plate 3 is by screw bolt and nut and base 1 and panoramic table 2 flexible connections.Calibration alignment pin 4 is arranged on the lower plane of panoramic table 2.Base 1 is provided with locating hole 1 and locating hole 2 102 and locating hole 3 103.The plane of baseplane locating piece 5 is provided with 2 alignment pins 9.Panoramic table pressing plate 3 is with base 1 and panoramic table 2 is simple in structure, convenient disassembly, by baseplane locating piece 5 and 2 alignment pins 9, tubular workpiece 11 is reliably located on panoramic table; Locating hole 1 and locating hole 2 102 and locating hole 3 103 are used in conjunction with calibration alignment pin 4, process respectively each machined surface of tubular workpiece.
Be the schematic diagram of one embodiment of the invention as Fig. 2, do one side two finger settings with baseplane and two apertures on the baseplane of tubular workpiece 11, two pins are be used to preventing that workpiece from rotating; Compress with stay bolt 7 and pressing plate 8 on tubular workpiece 11 upper surfaces; Be useful on rotating calibration alignment pin 4 on panoramic table 2, realize the circumference graduation of this device, thereby complete the plane machining on tubular workpiece 11 circumference.By inserting and extracting calibration alignment pin 4, complete the revolution of tubular workpiece 11 on this device, simple to operation.The bottom surface of tubular workpiece 11 is placed on panoramic table 2, by baseplane locating piece 5 and 2 alignment pins 9, tubular workpiece 11 is reliably located on panoramic table, prevents that tubular workpiece 11 from rotating.
As shown in Figure 3, base 1 is provided with locating hole 1, locating hole 2 102 and locating hole 3 103, calibration alignment pin 4 inserts respectively in locating hole 1 and locating hole 2 102 and locating hole 3 103, and the workpiece machined surface 1 on tubular workpiece 11 circumference, workpiece machined surface 2 122 and workpiece machined surface 3 123 are processed respectively.This operation has realized the revolution of each face on tubular workpiece 11 circumference, has facilitated the reliable contraposition of machining center equipment and machined surface.
Operating process is as follows: first tubular workpiece 11 is done one side two finger settings on panoramic table 2, the bottom surface of tubular workpiece 11 is placed on panoramic table 2, by baseplane locating piece 5 and 2 alignment pins 9, tubular workpiece 11 is reliably located on panoramic table; Tubular workpiece 11 is set on stay bolt 7, and its upper surface compresses by pressing plate; Base 1 is connected with panoramic table by 3 connections of panoramic table pressing plate, panoramic table pressing plate 3 links into an integrated entity base 1 and panoramic table 2 by screw bolt and nut, panoramic table 2 is provided with locating hole, at first, calibration alignment pin 4 inserts in locating hole 101 (position shown in Figure 3), processing work face 1 is after machining; Extract calibration alignment pin 4, then unclamp panoramic table pressing plate 3, panoramic table 2 turns over 45 degree counterclockwise, calibration alignment pin 4 is inserted in locating hole 102, then compress panoramic table pressing plate 3, processing work machined surface 2 122; In like manner, clockwise rotate panoramic table 2, turn over 45 degree, calibration alignment pin 4 is inserted in locating hole 103, then compress panoramic table pressing plate 3, processing work machined surface 3 123.Aforesaid operations has been realized must processing tubular workpiece 11 each faces, and is simple to operation, improved operating efficiency.
Be the schematic diagram of tubular workpiece as Fig. 4, this device can be processed workpiece as shown in the figure, has versatility and practicality.Be the schematic cross-section of tubular workpiece in Fig. 2 as Fig. 5, this workpiece out-of-shape can't be processed with existing equipment, by design of the present invention, and successfully processing work machined surface 1, workpiece machined surface 2 122 and workpiece machined surface 3 123.Fig. 6 is the design of calibration alignment pin 4 of the present invention, makes simple, easy to operate.The present invention has realized the processing on tubular workpiece work in-process heart equipment efficiently, and is simple to operation, improved working (machining) efficiency.
Take above-mentioned foundation desirable embodiment of the present invention as enlightenment, by above-mentioned description, the relevant staff can in the scope that does not depart from this invention technological thought, carry out various change and modification fully.The technical scope of this invention is not limited to the content on specification, must determine its technical scope according to the claim scope.