CN101612706B - Clamp for end shield of air suction valve of numerical control machining air compressor - Google Patents
Clamp for end shield of air suction valve of numerical control machining air compressor Download PDFInfo
- Publication number
- CN101612706B CN101612706B CN2008100435351A CN200810043535A CN101612706B CN 101612706 B CN101612706 B CN 101612706B CN 2008100435351 A CN2008100435351 A CN 2008100435351A CN 200810043535 A CN200810043535 A CN 200810043535A CN 101612706 B CN101612706 B CN 101612706B
- Authority
- CN
- China
- Prior art keywords
- workpiece
- clamp
- clamp body
- suction valve
- air compressor
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003754 machining Methods 0.000 title claims abstract description 11
- 230000007246 mechanism Effects 0.000 claims abstract description 14
- 238000009434 installation Methods 0.000 claims description 4
- 238000000034 method Methods 0.000 description 4
- 238000010586 diagram Methods 0.000 description 2
- 235000000396 iron Nutrition 0.000 description 2
- 230000000284 resting effect Effects 0.000 description 2
- QNRATNLHPGXHMA-XZHTYLCXSA-N (r)-(6-ethoxyquinolin-4-yl)-[(2s,4s,5r)-5-ethyl-1-azabicyclo[2.2.2]octan-2-yl]methanol;hydrochloride Chemical compound Cl.C([C@H]([C@H](C1)CC)C2)CN1[C@@H]2[C@H](O)C1=CC=NC2=CC=C(OCC)C=C21 QNRATNLHPGXHMA-XZHTYLCXSA-N 0.000 description 1
- 238000010923 batch production Methods 0.000 description 1
- 239000002131 composite material Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
Images


Landscapes
- Structures Of Non-Positive Displacement Pumps (AREA)
- Jigs For Machine Tools (AREA)
Abstract
本发明公开了数控加工空压机吸气阀盖头夹具,其主要包括一夹具体和数个定位元件及夹紧机构,所述夹具体为一凸形长方体;夹具体通过定位键定位、螺栓固定于工作台的T形槽上,夹具体上与工件底面环形凸台对应处设有与凸台相接触的环形凸起面;夹具体两端与工件上孔对应处设有两个定位销;夹具体两侧面设有对工件对中夹紧的夹紧机构。本发明夹具能够快速定位对中夹紧,定位精度有很大的提高,且夹具在工作台上有确定的位置,则工件坐标系也完全确定,使工作效率大幅度提高。
The invention discloses a numerical control machining air compressor suction valve cover head clamp, which mainly includes a clamping body, several positioning elements and a clamping mechanism, the clamping body is a convex cuboid; the clamping body is positioned by positioning keys and fixed by bolts On the T-shaped groove of the workbench, there is an annular raised surface in contact with the boss at the position corresponding to the annular boss on the bottom surface of the workpiece; two positioning pins are arranged at the two ends of the clamp body and the corresponding holes on the workpiece; The two sides of the clamp body are provided with clamping mechanisms for centrally clamping the workpiece. The fixture of the invention can be quickly positioned and centered and clamped, and the positioning accuracy is greatly improved, and the fixture has a definite position on the workbench, so the coordinate system of the workpiece is also completely determined, so that the work efficiency is greatly improved.
Description
技术领域:Technical field:
本发明涉及一种数控加工机床夹具,特别涉及一种数控加工空压机吸气阀盖头的专用夹具。The invention relates to a fixture for a numerically controlled machining machine tool, in particular to a special fixture for numerically controlled machining the cover head of an air compressor suction valve.
背景技术:Background technique:
随着计算机技术的高速发展,传统的制造业发生了根本性的变革,利用数控机床加工,其产品加工的质量一致性好,加工精度和效率均比普通机床高出很多,尤其是在轮廓不规则、复杂的曲线或曲面、多工艺复合化加工和高精度要求的产品加工时,其优点是传统机床所无法比拟的。With the rapid development of computer technology, fundamental changes have taken place in the traditional manufacturing industry. Using CNC machine tools to process products has a good quality consistency, and the machining accuracy and efficiency are much higher than ordinary machine tools, especially when the contour is different. When processing regular, complex curves or curved surfaces, multi-process composite processing and products requiring high precision, its advantages are unmatched by traditional machine tools.
夹具是数控加工中心的重要组成部分,其作用是将工件固定在机床的准确位置上,完成对工件的各种加工,既要定位准确又要夹紧可靠,显然其结构的优劣对加工精度、加工效率有着至关重要的影响;The fixture is an important part of the CNC machining center. Its function is to fix the workpiece at the exact position of the machine tool and complete various processing of the workpiece. It must be positioned accurately and clamped reliably. Obviously, the advantages and disadvantages of its structure have a great impact on the machining accuracy. , Processing efficiency has a crucial impact;
空压机吸气阀盖头的结构复杂,其上存在多个圆形孔,同时还有多个凸起表面。要对其加工首先要解决对其的定位夹紧,但在数控机床上用于加工空压机吸气阀盖头的专用夹具很少,在资料和网上很难找到,一般都是把工件放在平口虎钳上,用百分表找正位置,再辅助用些垫铁、角铁定位,然后用平口虎钳夹紧。加工时还要测定和设置工件坐标系,工作效率低,且定位精度不高。The structure of the air compressor suction valve cap is complicated, there are many circular holes on it, and there are also many raised surfaces. To process it, we must first solve its positioning and clamping. However, there are few special fixtures for processing the air compressor suction valve cap on the CNC machine tool, and it is difficult to find it in the data and on the Internet. Generally, the workpiece is placed on the On the flat vise, use the dial indicator to find the correct position, and then use some pad irons and angle irons to position it, and then clamp it with the flat vise. It is necessary to measure and set the workpiece coordinate system during processing, so the work efficiency is low and the positioning accuracy is not high.
发明内容:Invention content:
本发明针对上述现有数控机床专用夹具所存在的问题,而提供一种用于数控机床或加工中心成批加工空压机吸气阀盖头时的一种专用夹具,其能够对工件快速定位侧面对中夹紧,且加工时不需测定工件坐标系。The present invention aims at the above-mentioned problems existing in the existing special fixtures for CNC machine tools, and provides a special fixture for CNC machine tools or machining centers to batch process air compressor suction valve cover heads, which can quickly position the side of the workpiece Centering clamping, and no need to determine the workpiece coordinate system during processing.
为达到上述目的,本发明提供的数控加工空压机吸气阀盖头夹具,其主要包括一夹具体和数个定位元件及夹紧机构,所述夹具体为一凸形长方体;夹具体通过定位键定位、螺栓固定于工作台的T形槽上,夹具体上与工件底面环形凸台对应处设有与凸台相接触的环形凸起面;夹具体两端与工件上孔对应处设有两个定位销;夹具体两侧面设有对工件对中夹紧的夹紧机构。In order to achieve the above object, the numerically controlled machining air compressor air compressor suction valve cover head fixture provided by the present invention mainly includes a clamp body and several positioning elements and clamping mechanisms, and the clamp body is a convex cuboid; The key is positioned and the bolt is fixed on the T-shaped groove of the workbench. On the clamp body, there is an annular raised surface in contact with the boss on the bottom surface of the workpiece; at both ends of the clamp body, there are Two positioning pins; the two sides of the clamp body are provided with a clamping mechanism for centering and clamping the workpiece.
所述两个定位销为一个圆柱定位销和一个菱形定位销。The two locating pins are a cylindrical locating pin and a diamond-shaped locating pin.
所述夹紧机构采用螺旋压板夹紧机构,该机构中的长螺栓横穿过夹具体,通过螺母使搭在工件侧面和夹具体侧面凸棱上的两压板对中夹紧工件;所述长螺栓两端均安放能够自动适应一批工件安装位置的球面垫圈和锥面垫圈。The clamping mechanism adopts a spiral clamping plate clamping mechanism. The long bolts in this mechanism traverse the clamping body, and the two clamping plates resting on the side of the workpiece and the ribs on the side of the clamping body are centered to clamp the workpiece through nuts; Both ends of the bolt are placed with spherical washers and conical washers that can automatically adapt to the installation positions of a batch of workpieces.
所述夹具体上在对应于工件的悬伸处设有辅助支承。The clamp body is actually provided with auxiliary supports at the overhang corresponding to the workpiece.
根据上述技术方案得到的本发明夹具与平口虎钳找正夹紧相比具有以下优点:能够快速定位对中夹紧,定位精度有很大的提高,且夹具在工作台上有确定的位置,则工件坐标系也完全确定,使工作效率大幅度提高。Compared with the straightening and clamping of the flat vise, the clamp of the present invention obtained according to the above technical solution has the following advantages: it can be quickly positioned and clamped, the positioning accuracy is greatly improved, and the clamp has a definite position on the workbench. Then the workpiece coordinate system is also completely determined, so that the work efficiency is greatly improved.
附图说明:Description of drawings:
以下结合附图和具体实施方式来进一步说明本发明。The present invention will be further described below in conjunction with the accompanying drawings and specific embodiments.
图1为本发明的主视图。Fig. 1 is the front view of the present invention.
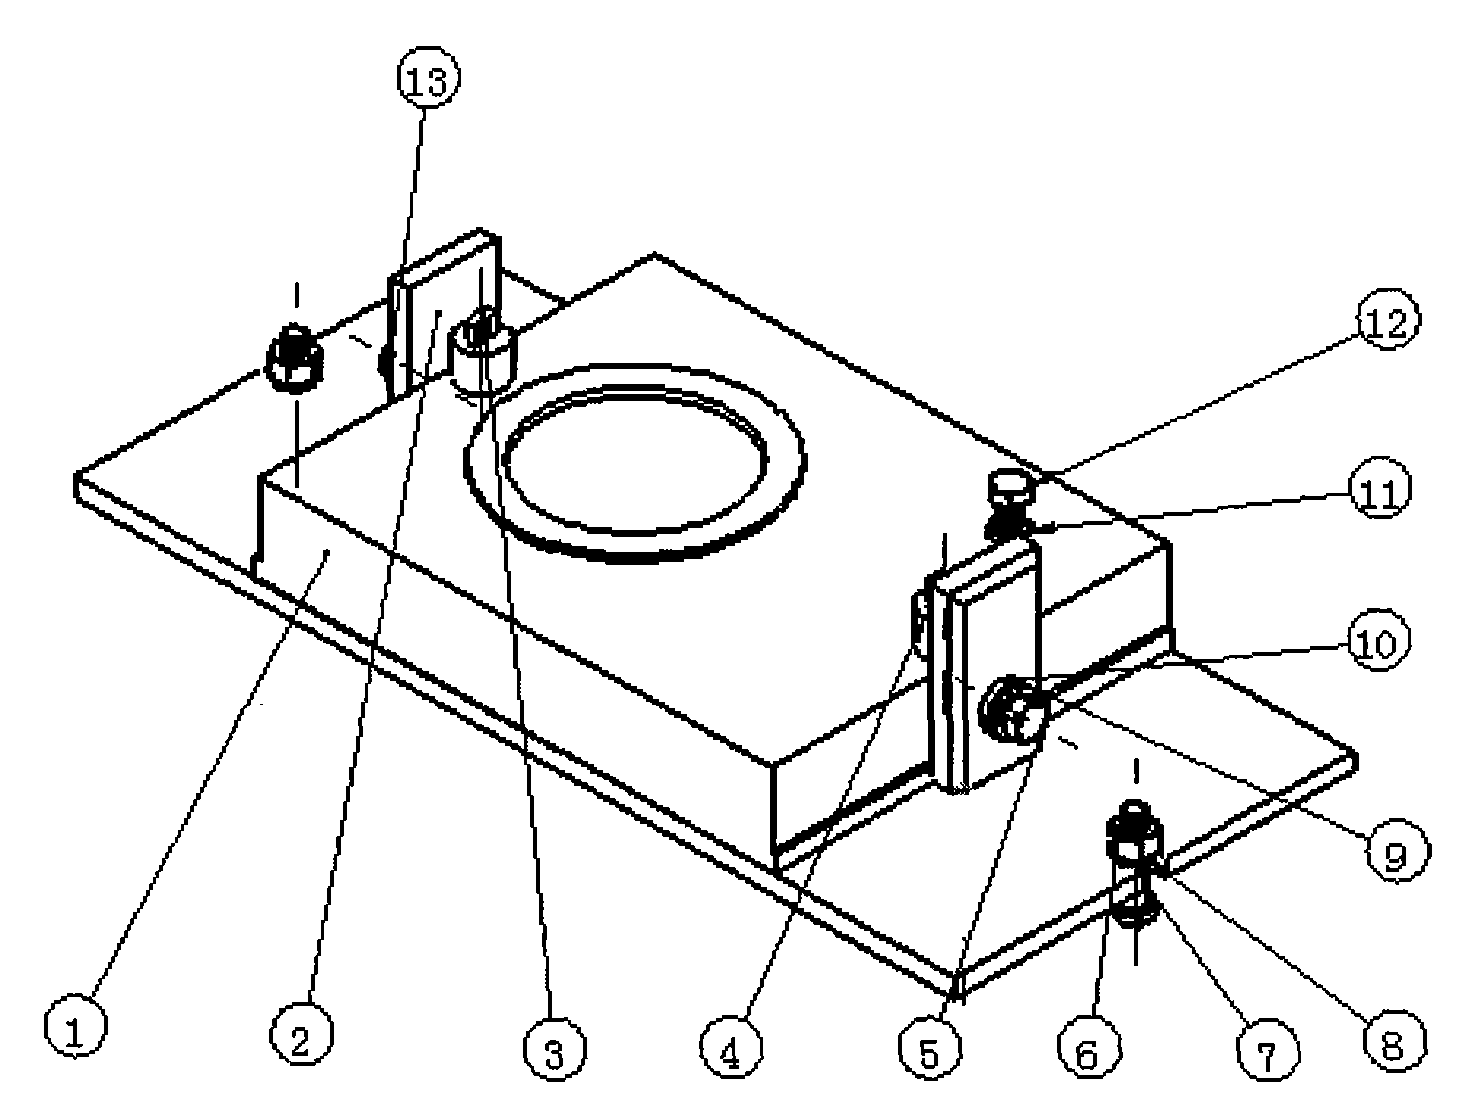
图2为本发明的轴侧图。Figure 2 is a perspective view of the present invention.
图3为本发明的侧视图。Figure 3 is a side view of the present invention.
图4为空压机吸气阀盖头结构示意图。Fig. 4 is a structural schematic diagram of the cover head of the suction valve of the air compressor.
图5为本发明使用时的结构示意图。Fig. 5 is a schematic structural diagram of the present invention in use.
具体实施方式:Detailed ways:
为了使本发明实现的技术手段、创作特征、达成目的与功效易于明白了解,下面结合具体图示,进一步阐述本发明。In order to make the technical means, creative features, goals and effects achieved by the present invention easy to understand, the present invention will be further described below in conjunction with specific illustrations.
空压机吸气阀盖头(如图4所示)结构复杂,存在多个圆形孔及多个凸台。数控机床在对其进行加工时,使用通用夹具对其进行定位夹紧时存在一定的困难。The cover head of the suction valve of the air compressor (as shown in Figure 4) has a complex structure, with multiple circular holes and multiple bosses. When CNC machine tools are processing it, there are certain difficulties in using general fixtures to position and clamp it.
本发明为解决这样的问题提供了一种专用夹具,其主要如图1和图2所示,该夹具主要包括一夹具体和数个定位元件及对中夹紧机构,该夹具体1为一凸形长方体,定位键14通过螺钉15固定在夹具体1底部并与T形槽形配合,将夹具体1定位在工作台上(图中未给出结构);将螺栓6穿过T形槽通过螺母8拧紧从而将夹具体1固定在工作台上。The present invention provides a special clamp to solve such problems, which is mainly shown in Figure 1 and Figure 2, the clamp mainly includes a clamp body, several positioning elements and a centering clamping mechanism, the
夹具体1上与空压机吸气阀盖头底面环形凸台对应处设有与凸台相接触的环形凸起面,这样当空压机吸气阀盖头通过底面与夹具体环形面接触时,就限制了一个移动自由度,两个旋转自由度。The
夹具体两端与空压机吸气阀盖头两端上孔对应处设有两个定位销,该定位销为一个圆柱定位销4和一个菱形定位销3,当空压机吸气阀盖头的对应孔插入到这两个定位销中,可限制其两个移动自由度,一个旋转自由度。There are two locating pins at the two ends of the clamp body and the upper holes at the two ends of the air compressor suction valve cover. The locating pins are a
夹具体1两侧面设有对空压机吸气阀盖头对中夹紧的夹紧机构,采用螺旋压板夹紧机构,该机构中的长螺栓5横穿过夹具体1,通过螺母13顶紧两块搭在工件侧面和夹具体侧面凸棱上的压板2,从而实现了对空压机吸气阀盖头侧面对中夹紧;该长螺栓5两端均依次安放锥面垫圈10和球面垫圈9,这样能够使夹具自动适应一批工件的安装位置。The two sides of
由于空压机吸气阀盖头悬伸较长,为提高刚度,在夹具体上对应于悬伸处加了辅助支承12。Because the overhang of the suction valve cap of the air compressor is longer, in order to improve the rigidity, an
根据上述技术原理得到的专用夹具,在使用时两个定位键14用螺钉15固定在夹具体底部与T形槽相配合,将夹具定位在工作台上。然后用螺栓6、螺母8、垫圈7将夹具固定在工作台上。According to the special fixture obtained according to the above-mentioned technical principle, two positioning keys 14 are fixed on the bottom of the fixture body with
空压机吸气阀盖头通过底面的环形凸台与夹具体上环形凸起面接触,限制了一个移动自由度,两个旋转自由度;通过一个圆柱定位销,一个菱形定位销插入空压机吸气阀盖头的对应孔中,可限制两个移动自由度,一个旋转自由度,即通过一面两销对空压机吸气阀盖头实现了完全定位。The cover head of the air compressor suction valve is in contact with the annular convex surface of the clamp body through the annular boss on the bottom surface, which limits one degree of freedom of movement and two degrees of freedom of rotation; it is inserted into the air compressor through a cylindrical positioning pin and a diamond-shaped positioning pin In the corresponding hole of the suction valve cap, two degrees of freedom of movement and one degree of freedom of rotation can be restricted, that is, the complete positioning of the suction valve cap of the air compressor is realized by two pins on one side.
用长螺栓、球面垫圈、锥面垫圈、螺母、压板以及夹具体侧面凸棱实现了对空压机吸气阀盖头侧面对中夹紧,球面垫圈与锥面垫圈相配可自动适应一批工件的安装位置。Using long bolts, spherical washers, conical washers, nuts, pressure plates and side ribs on the side of the clamp body, the centering and clamping of the side of the air compressor suction valve cover is realized. The matching of the spherical washer and the conical washer can automatically adapt to a batch of workpieces. installation location.
由于空压机吸气阀盖头悬伸较长,为提高刚度,在悬伸处加了辅助支承。Since the overhang of the suction valve cover of the air compressor is long, in order to improve the rigidity, an auxiliary support is added at the overhang.
以上显示和描述了本发明的基本原理和主要特征及本发明的优点。本行业的技术人员应该了解,本发明不受上述实施例的限制,上述实施例和说明书中描述的只是说明本发明的原理,在不脱离本发明精神和范围的前提下,本发明还会有各种变化和改进,这些变化和改进都落入要求保护的本发明范围内。本发明要求保护范围由所附的权利要求书及其等效物界定。The basic principles and main features of the present invention and the advantages of the present invention have been shown and described above. Those skilled in the industry should understand that the present invention is not limited by the above-mentioned embodiments. What are described in the above-mentioned embodiments and the description only illustrate the principle of the present invention. Without departing from the spirit and scope of the present invention, the present invention will also have Variations and improvements are possible, which fall within the scope of the claimed invention. The protection scope of the present invention is defined by the appended claims and their equivalents.
Claims (3)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2008100435351A CN101612706B (en) | 2008-06-23 | 2008-06-23 | Clamp for end shield of air suction valve of numerical control machining air compressor |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2008100435351A CN101612706B (en) | 2008-06-23 | 2008-06-23 | Clamp for end shield of air suction valve of numerical control machining air compressor |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN101612706A CN101612706A (en) | 2009-12-30 |
| CN101612706B true CN101612706B (en) | 2011-04-13 |
Family
ID=41492682
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2008100435351A Expired - Fee Related CN101612706B (en) | 2008-06-23 | 2008-06-23 | Clamp for end shield of air suction valve of numerical control machining air compressor |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN101612706B (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102699814A (en) * | 2012-06-13 | 2012-10-03 | 苏州市达圣机械有限公司 | Frock for adjustment sheet |
| CN102962645A (en) * | 2012-11-26 | 2013-03-13 | 天津台荣精密机械工业有限公司 | Convenient processing device and working method thereof |
Families Citing this family (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101912984B (en) * | 2010-08-10 | 2011-12-14 | 南车戚墅堰机车有限公司 | Equipment for machining side faces and side holes of large-size box type workpiece |
| CN102173258A (en) * | 2011-01-30 | 2011-09-07 | 黄丽汶 | Full-automatic numerical control woodworking, enchasing and forming machine |
| CN102198578B (en) * | 2011-05-07 | 2013-12-18 | 奇瑞重工股份有限公司 | Assembly tool for rethresher shell of harvester |
| CN102398168A (en) * | 2011-10-23 | 2012-04-04 | 芜湖华峰汽车部件有限责任公司 | Valve chamber cover clamp |
| CN102371521A (en) * | 2011-10-31 | 2012-03-14 | 苏州金牛精密机械有限公司 | Polishing tool of double tilting trays for axial plunger motor |
| CN102672488A (en) * | 2012-05-14 | 2012-09-19 | 昆山南方铸造有限公司 | Fixture for machining Unihub bracket of railing machine |
| CN103121173A (en) * | 2012-11-22 | 2013-05-29 | 上海小糸车灯有限公司 | Bolt-fixing type workpiece clamping support structure for computer numerical control (CNC) |
| CN105945608B (en) * | 2016-07-01 | 2018-10-19 | 中铁工程装备集团有限公司 | Polar coordinates positioning form large arm machines tooling and its processing method |
| CN113927328B (en) * | 2021-09-29 | 2024-05-31 | 青岛青特众力车桥有限公司 | Axle reduction gear shell boss structure and processing clamp thereof |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN87203995U (en) * | 1987-03-17 | 1988-03-02 | 昆明机床厂 | Fixture of cylinder bore treating with crankshaft hole allocation |
| CN1171319A (en) * | 1996-04-04 | 1998-01-28 | 朴胜夫 | Clamping device of machine tool |
| CN2880363Y (en) * | 2006-02-13 | 2007-03-21 | 许晓华 | Porous deformed plate milling drilling clamp |
-
2008
- 2008-06-23 CN CN2008100435351A patent/CN101612706B/en not_active Expired - Fee Related
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN87203995U (en) * | 1987-03-17 | 1988-03-02 | 昆明机床厂 | Fixture of cylinder bore treating with crankshaft hole allocation |
| CN1171319A (en) * | 1996-04-04 | 1998-01-28 | 朴胜夫 | Clamping device of machine tool |
| CN2880363Y (en) * | 2006-02-13 | 2007-03-21 | 许晓华 | Porous deformed plate milling drilling clamp |
Non-Patent Citations (1)
| Title |
|---|
| JP平1-222835A 1989.09.06 |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102699814A (en) * | 2012-06-13 | 2012-10-03 | 苏州市达圣机械有限公司 | Frock for adjustment sheet |
| CN102699814B (en) * | 2012-06-13 | 2016-04-13 | 苏州市达圣机械有限公司 | A kind of trimmer frock |
| CN102962645A (en) * | 2012-11-26 | 2013-03-13 | 天津台荣精密机械工业有限公司 | Convenient processing device and working method thereof |
Also Published As
| Publication number | Publication date |
|---|---|
| CN101612706A (en) | 2009-12-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109318000B (en) | A universal angle clamp for CNC center | |
| CN101612706A (en) | Clamp for end shield of air suction valve of numerical control machining air compressor | |
| CN101612707B (en) | Clamp for numerical control machining | |
| CN205834798U (en) | For processing the vertical machining centre flexible jig of the uniform screw of bearing block end face | |
| CN205852335U (en) | For processing the vertical numerical control fraise jig of water pump vane groove milling | |
| CN110774027A (en) | Boring clamp and operation method thereof | |
| CN105234712A (en) | Manual fixture of automobile steering knuckle | |
| CN110722379A (en) | A machine tool | |
| CN211760950U (en) | A casting positioning and clamping device | |
| CN106271777B (en) | Multistation fast pneumatic positions clamping tool | |
| CN205870047U (en) | A vertical numerical control milling machine fixture for processing square shoulder axis square head | |
| CN206662766U (en) | Aerial blade fixture | |
| CN105345552A (en) | Milling jig for machining four peripheral faces of lathe tool apron rack | |
| CN209919370U (en) | A multi-process machining clamping tool for a workpiece | |
| CN206123248U (en) | A quick pneumatic positioning and clamping device of multistation for processing aeroengine part | |
| CN209737092U (en) | A special fixture for milling dovetail slots on workpieces | |
| CN205798992U (en) | For processing the vertical process center fixture in the uniform hole of bearing block | |
| CN206343913U (en) | A kind of milling fixture for processing diplopore connecting rod medial launder | |
| CN215659073U (en) | A CNC clamping fixture for machining multi-faceted grooves | |
| CN106271776B (en) | For processing three station pneumatic positioning clamping devices of housing part | |
| CN110695735A (en) | a tooling fixture | |
| CN202356917U (en) | Typical curved part boring fixture | |
| CN214135017U (en) | A special fixture mechanism for special-shaped workpieces | |
| CN206305806U (en) | High accuracy multiaxis rotary tooling | |
| CN205201313U (en) | Quad slit abrasive machining anchor clamps |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20110413 Termination date: 20110623 |