CN101456745B - Calcining filler processing method and system - Google Patents
Calcining filler processing method and system Download PDFInfo
- Publication number
- CN101456745B CN101456745B CN2007101588059A CN200710158805A CN101456745B CN 101456745 B CN101456745 B CN 101456745B CN 2007101588059 A CN2007101588059 A CN 2007101588059A CN 200710158805 A CN200710158805 A CN 200710158805A CN 101456745 B CN101456745 B CN 101456745B
- Authority
- CN
- China
- Prior art keywords
- metallurgical coke
- sent
- screening
- screw conveyor
- equipment
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Landscapes
- Disintegrating Or Milling (AREA)
Abstract
本发明公开了一种焙烧填充料,尤其涉及适用于生产铝用阳极、阴极和电极的一种焙烧填充料加工方法及系统。一种焙烧填充料加工方法,包括下述步骤:将冶金焦送到筛分设备进行筛分,筛分粒度合格的冶金焦送到成品螺旋输送机,筛分粒度不合格的冶金焦送到处理设备进行处理,送到成品螺旋输送机的冶金焦再送到成品料槽。本发明采用上述焙烧填充料加工工艺,将冶金焦经破碎、筛分加工处理成粒级在0.5~6mm的具有可压缩性、吸附性和透气性的最佳配合填充料成品,提高了焙烧品的体积密度和机械强度,降低生坯的收缩速度。改善了生产操作环境。本发明有效解决了填充料原料选择性小、成本高,以及填充料在运送过程造成严重的环境污染和原料损失的技术问题。
The invention discloses a calcined filler, in particular to a calcined filler processing method and system suitable for producing aluminum anodes, cathodes and electrodes. A method for processing roasting filling materials, comprising the following steps: sending metallurgical coke to a screening device for screening, sending metallurgical coke with a qualified particle size to a finished product screw conveyor, and sending metallurgical coke with an unqualified particle size to be processed The equipment will process the metallurgical coke sent to the finished product screw conveyor and then sent to the finished product trough. The present invention adopts the above-mentioned roasting filling material processing technology, and crushes and sieves the metallurgical coke into the finished product of the optimally matched filling material with compressibility, adsorption and gas permeability at a particle size of 0.5-6mm, which improves the roasted product. The bulk density and mechanical strength reduce the shrinkage speed of the green body. Improved production operating environment. The invention effectively solves the technical problems of low selectivity of filler raw materials, high cost, and serious environmental pollution and raw material loss caused by the filler during transportation.
Description
技术领域technical field
本发明涉及一种填充料加工方法及系统,尤其涉及一种适用于生产铝用阳极、阴极和电极的焙烧填充料加工方法及系统。The invention relates to a filling material processing method and system, in particular to a roasting filling material processing method and system suitable for producing aluminum anodes, cathodes and electrodes.
背景技术Background technique
填充料是焙烧时用于覆盖生坯、填充间隙以防止生坯氧化、变形的散装颗粒料。填充料在生坯焙烧时的主要作用是:1.防止生坯与加热火焰直接接触氧化;2.固定生坯形状;3.将热量传导给生坯;4.保留生坯焙烧时挥发份的排出通道。焙烧填充料对生坯在焙烧过程中残炭率的大小有明显的作用,从而影响焙烧品的理化性能,所以填充料在焙烧过程中有很重要的作用。填充料一般要求具有良好的导热性、较小的吸附性、颗粒度适中、材料易获得、且价格便宜等。现在多数的炭素厂都采用冶金焦作为焙烧填充料,外购的冶金焦需经过加工处理后才能用作焙烧填充料。经过长期的生产实践和不断研究发现,填充料的颗粒度在生坯焙烧时发挥一定的影响,粒级在0.5~6mm的填充料具有可压缩性、吸附性和透气性的最佳配合。如填充料中小于0.5mm的粉料过多,将导致焙烧品烧损增加,残炭率降低。颗粒过大会影响焙烧品的表层结构。适用于铝用阳极、阴极和电极焙烧填充料的颗粒度是大于6mm的大颗粒和小于0.5mm粉料的数量都不要大于10%。现有生产炭素制品企业焙烧填充料加工方法一般采用在生制品生产车间的破碎筛分系统分离出粒度在0.5~6mm的部分物料后,用车辆运至焙烧车间的填充料存储区。该方法一方面造成原料选择性减小,它只能选择生制品生产所用原料作为填充料,成本高;另一方面造成填充料在运送过程造成严重的环境污染并造成原料损失。The filler is the bulk granular material used to cover the green body and fill the gap during firing to prevent the green body from oxidation and deformation. The main functions of fillers during green body roasting are: 1. Prevent the green body from being oxidized in direct contact with the heating flame; 2. Fix the shape of the green body; 3. Conduct heat to the green body; 4. Retain the volatile content of the green body during roasting discharge channel. The roasting filler has a significant effect on the carbon residue rate of the green body during the roasting process, thereby affecting the physical and chemical properties of the roasted product, so the filler plays an important role in the roasting process. Fillers are generally required to have good thermal conductivity, low adsorption, moderate particle size, easy access to materials, and cheap prices. Most carbon plants now use metallurgical coke as a roasting filler, and the purchased metallurgical coke needs to be processed before it can be used as a roasting filler. After long-term production practice and continuous research, it is found that the particle size of the filler has a certain influence on the green body roasting, and the filler with a particle size of 0.5-6 mm has the best combination of compressibility, adsorption and air permeability. If there is too much powder less than 0.5mm in the filling material, it will lead to increased burning loss of roasted products and reduced carbon residue rate. If the particles are too large, the surface structure of the baked product will be affected. The particle size suitable for aluminum anode, cathode and electrode firing fillers is that the amount of large particles greater than 6mm and powder less than 0.5mm should not exceed 10%. The existing processing methods of roasting fillers in carbon products enterprises generally use the crushing and screening system in the raw product production workshop to separate some materials with a particle size of 0.5-6 mm, and then transport them to the filler storage area in the roasting workshop by vehicles. On the one hand, this method reduces the selectivity of raw materials, and it can only choose the raw materials used in the production of raw products as fillers, which is costly; on the other hand, the fillers cause serious environmental pollution and loss of raw materials during transportation.
发明内容Contents of the invention
本发明就是为了解决上述技术问题,而提供一种焙烧填充料加工方法及系统,目的是有效解决填充料原料选择性小、成本高,以及填充料在运送过程造成严重的环境污染和原料损失的技术问题。In order to solve the above-mentioned technical problems, the present invention provides a method and system for processing roasted fillers, the purpose of which is to effectively solve the problems of low selectivity of filler raw materials, high cost, and serious environmental pollution and raw material loss caused by fillers during transportation. technical problem.
为了达到上述目的,本发明是采用如下技术方案实现的:一种焙烧填充料加工方法,它包括下述步骤:将冶金焦送到筛分设备进行筛分,筛分粒度合格的冶金焦送到成品螺旋输送机,筛分粒度不合格的冶金焦送到处理设备进行处理,送到成品螺旋输送机的冶金焦再送到成品料槽。In order to achieve the above object, the present invention is achieved by adopting the following technical scheme: a method for processing roasted filling materials, which includes the following steps: sending metallurgical coke to screening equipment for screening, and sending metallurgical coke with qualified screening particle size to The finished product screw conveyor, the metallurgical coke with unqualified screening particle size is sent to the processing equipment for processing, and the metallurgical coke sent to the finished product screw conveyor is then sent to the finished product trough.
所述的筛分粒度不合格的冶金焦送到处理设备进行处理包括下述步骤:将筛分粒度小于合格产品粒度的冶金焦送到粉料螺旋输送机;将筛分粒度大于合格产品粒度的冶金焦送到破碎机进行破碎。The metallurgical coke with an unqualified screening particle size is sent to the processing equipment for processing, including the following steps: sending the metallurgical coke with a screening particle size smaller than the qualified product particle size to the powder screw conveyor; The metallurgical coke is sent to the crusher for crushing.
所述的粉料螺旋输送机将小于合格产品粒度的冶金焦送到粉料仓。The powder screw conveyor sends the metallurgical coke with a particle size smaller than the qualified product to the powder bin.
所述的粉料仓内的粉料被送到装袋机进行装袋。The powder in the powder silo is sent to the bagging machine for bagging.
所述的大于合格产品粒度的冶金焦进行破碎后再送到筛分设备进行筛分。The metallurgical coke whose particle size is larger than the qualified product is crushed and then sent to the screening equipment for screening.
所述的将破碎机破碎的冶金焦先送到斗式提升机提升后再送到筛分设备。The metallurgical coke crushed by the crusher is first sent to the bucket elevator for lifting and then sent to the screening equipment.
所述的筛分设备所筛分的冶金焦先经过格筛料斗的筛选再送到筛分设备。The metallurgical coke screened by the screening equipment is first screened by the grizzly hopper and then sent to the screening equipment.
所述的格筛料斗筛选的冶金焦由给料设备送到斗式提升机提升后再送到筛分设备。The metallurgical coke screened by the grid sieve hopper is sent to the bucket elevator by the feeding equipment and then sent to the screening equipment.
所述的筛分设备设有双层筛,底层的冶金焦送到粉料螺旋输送机;中间层的冶金焦送到成品螺旋输送机;顶层的冶金焦送到破碎机。The screening equipment is equipped with double-layer screens, the metallurgical coke in the bottom layer is sent to the powder screw conveyor; the metallurgical coke in the middle layer is sent to the finished product screw conveyor; the metallurgical coke in the top layer is sent to the crusher.
所述的冶金焦合格的粒度为0.5~6mm。The qualified particle size of the metallurgical coke is 0.5-6mm.
一种焙烧填充料加工系统,它由下述结构构成:筛分设备底部出口与粉料螺旋输送机进口连接,筛分设备的中间层出口与成品螺旋输送机进口连接,筛分设备顶层出口与破碎机进口连接,粉料螺旋输送机出口与粉料仓进口连接,成品螺旋输送机出口与成口料槽连接,破碎机出口与筛分设备的进口连接。A roasting filling material processing system, which is composed of the following structure: the outlet at the bottom of the screening equipment is connected to the inlet of the powder screw conveyor, the outlet of the middle layer of the screening equipment is connected to the inlet of the screw conveyor for finished products, and the outlet of the top layer of the screening equipment is connected to the inlet of the screw conveyor for powder materials. The inlet of the crusher is connected, the outlet of the powder screw conveyor is connected with the inlet of the powder silo, the outlet of the finished product screw conveyor is connected with the mouth trough, and the outlet of the crusher is connected with the inlet of the screening equipment.
所述的粉料仓出口与装袋机连接。The outlet of the powder hopper is connected with a bagging machine.
所述的破碎机与筛分设备之间设有斗式提升机。A bucket elevator is provided between the crusher and the screening equipment.
所述的斗式提升机的进口与格筛料斗出口连接。The inlet of the bucket elevator is connected with the outlet of the grizzly hopper.
所述的斗式提升机与格筛料斗之间设有给料设备。Feeding equipment is provided between the bucket elevator and the grid sieve hopper.
所述的给料设备是电磁振动给料机或电机振动给料机。The feeding equipment is an electromagnetic vibrating feeder or a motor vibrating feeder.
所述的破碎机是反击式破碎机、对辊破碎机或锤式破碎机。The crusher is an impact crusher, a roller crusher or a hammer crusher.
所述的筛分设备是惯性振动筛或概率筛。The screening equipment is an inertial vibrating screen or a probability screen.
所述的筛分设备中间层的冶金焦粒度为0.5~6mm。The particle size of the metallurgical coke in the middle layer of the screening equipment is 0.5-6 mm.
本发明的优点和效果是:Advantage and effect of the present invention are:
采用上述焙烧填充料加工工艺,将冶金焦经破碎、筛分加工处理成粒级在0.5~6mm的具有可压缩性、吸附性和透气性的最佳配合填充料成品,以提高焙烧品的体积密度和机械强度,降低生坯的收缩速度。并将加工过程产生的小于0.5mm的粉料回收装袋,改善生产操作环境。本发明有效解决了填充料原料选择性小、成本高,以及填充料在运送过程造成严重的环境污染和原料损失的技术问题。Using the above-mentioned roasting filler processing technology, the metallurgical coke is crushed and screened into a finished filler product with the best combination of compressibility, adsorption and air permeability at a particle size of 0.5-6mm, so as to increase the volume of the roasted product Density and mechanical strength, reduce the shrinkage speed of the green body. And the powder less than 0.5mm produced during the processing is recycled and bagged to improve the production and operation environment. The invention effectively solves the technical problems of low selectivity of filler raw materials, high cost, and serious environmental pollution and raw material loss caused by the filler during transportation.
附图说明Description of drawings
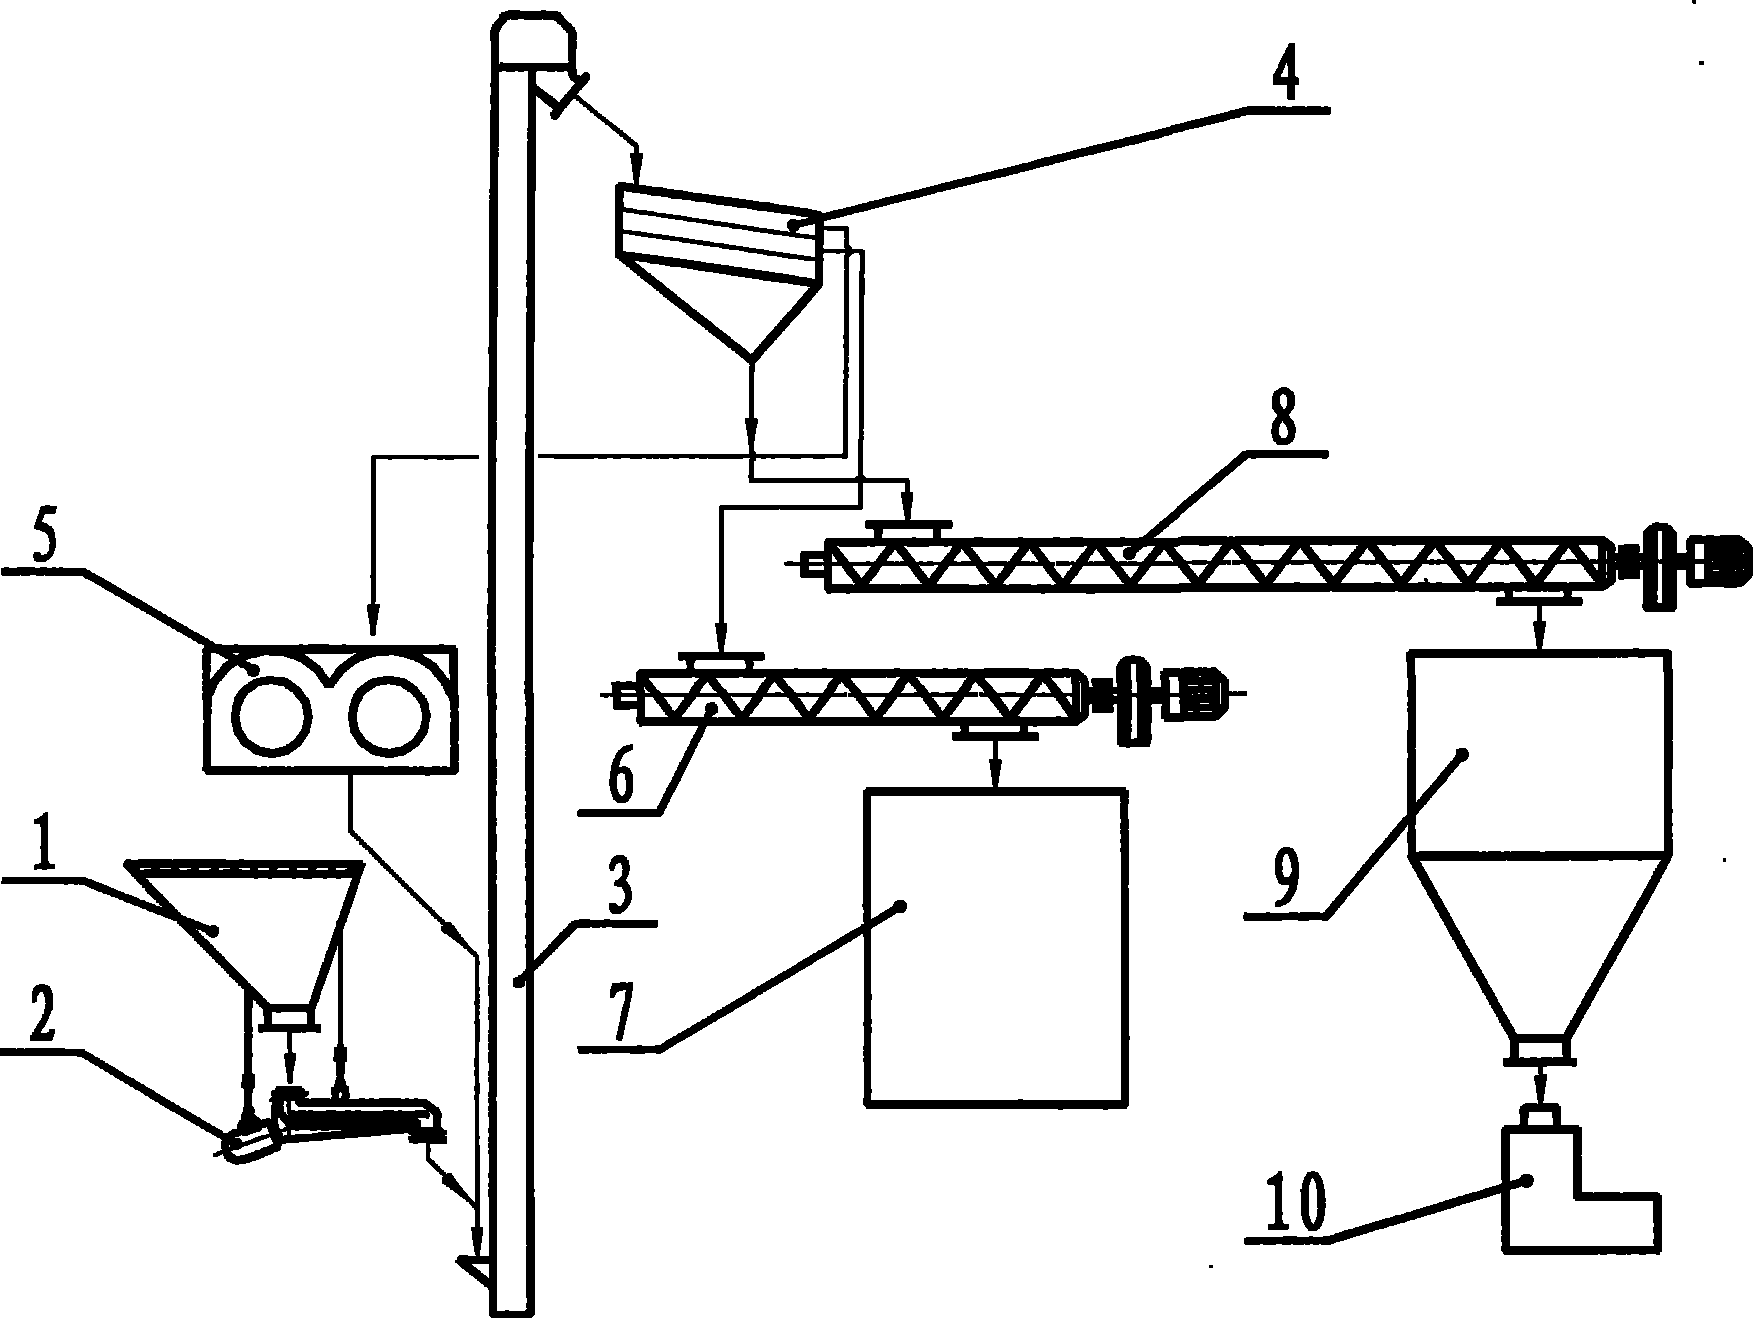
图1是本发明焙烧填充料加工及系统结构示意图。Fig. 1 is a schematic diagram of the processing and system structure of the roasting filling material of the present invention.
图中:1、格筛料斗,2、给料设备,3、斗式提升机,4、筛分设备,5、破碎机,6、成品螺旋输送机,7、成品料槽,8、粉料螺旋输送机,9、粉料仓,10、装袋机。In the figure: 1. Grid sieve hopper, 2. Feeding equipment, 3. Bucket elevator, 4. Screening equipment, 5. Crusher, 6. Finished product screw conveyor, 7. Finished product trough, 8. Powder Screw conveyor, 9, powder silo, 10, bagging machine.
具体实施方式Detailed ways
下面结合实施例对本发明做进一步详细描述,但本发明的保护范围不受实施例所限。The present invention will be further described in detail below in conjunction with the examples, but the protection scope of the present invention is not limited by the examples.
本发明一种焙烧填充料加工方法,它包括下述工艺步骤:将冶金焦送到筛分设备进行筛分,筛分设备所筛分的冶金焦先经过格筛料斗的筛选再送到筛分设备,格筛料斗筛选的冶金焦由给料设备送到斗式提升机提升后再送到筛分设备,筛分粒度合格的冶金焦送到成品螺旋输送机,筛分粒度不合格的冶金焦送到处理设备进行处理,所用筛分设备设有双层筛,底层的冶金焦送到粉料螺旋输送机;中间层的冶金焦送到成品螺旋输送机,冶金焦合格的粒度为0.5~6mm;顶层的冶金焦送到破碎机,送到成品螺旋输送机的冶金焦再送到成品料槽。The invention relates to a method for processing roasting filler, which comprises the following process steps: sending the metallurgical coke to a screening device for screening, and the metallurgical coke screened by the screening device is first screened by a grid sieve hopper and then sent to the screening device , the metallurgical coke screened by the grid sieve hopper is sent to the bucket elevator by the feeding equipment and then sent to the screening equipment. The processing equipment is used for processing. The screening equipment used is equipped with double-layer screens. The metallurgical coke in the bottom layer is sent to the powder screw conveyor; the metallurgical coke in the middle layer is sent to the finished product screw conveyor. The metallurgical coke is sent to the crusher, and the metallurgical coke sent to the finished screw conveyor is sent to the finished product trough.
筛分料度不合格的冶金焦送到处理设备进行处理是将筛分粒度小于合格产品粒度的冶金焦送到粉料螺旋输送机,粉料螺旋输送机将粒度小于0.5mm的冶金焦送到粉料仓,粉料仓内的粉料送到装袋机进行装袋;将筛分粒度大于6mm的冶金焦送到破碎机进行破碎,粒度大于6mm的冶金焦进行破碎后再送到筛分设备进行筛分,将破碎机破碎的冶金焦先送到斗式提升机提升后再送到筛分设备。The metallurgical coke with unqualified screening material size is sent to the processing equipment for processing. The metallurgical coke with a screening particle size smaller than the qualified product particle size is sent to the powder screw conveyor, and the powder screw conveyor sends the metallurgical coke with a particle size of less than 0.5mm to Powder silo, the powder in the powder silo is sent to the bagging machine for bagging; the metallurgical coke with a particle size greater than 6mm is sent to the crusher for crushing, and the metallurgical coke with a particle size larger than 6mm is crushed and then sent to the screening equipment For screening, the metallurgical coke crushed by the crusher is first sent to the bucket elevator for lifting and then sent to the screening equipment.
如图1所示,一种焙烧填充料加工系统,其结构如下:筛分设备4底部出口与粉料螺旋输送机8进口连接,筛分设备4的中间层出口与成品螺旋输送机6进口连接,筛分设备4顶层出口与破碎机5进口连接,粉料螺旋输送机8出口与粉料仓9进口连接,粉料仓9出口与装袋机10连接,成品螺旋输送机6出口与成口料槽7连接,破碎机5出口与筛分设备4的进口连接,破碎机5与筛分设备4之间设有斗式提升机3,斗式提升机3的进口与格筛料斗1出口连接,斗式提升机3与格筛料斗1之间设有给料设备2,给料设备2是电磁振动给料机或电机振动给料机,破碎机5是反击式破碎机、对辊破碎机或锤式破碎机,筛分设备4是惯性振动筛或概率筛,筛分设备中间层的冶金焦粒度为0.5~6mm。As shown in Figure 1, a roasting filling material processing system has the following structure: the outlet at the bottom of the screening device 4 is connected to the inlet of the powder screw conveyor 8, and the outlet of the middle layer of the screening device 4 is connected to the inlet of the finished product screw conveyor 6 , the top outlet of the screening equipment 4 is connected to the crusher 5 inlet, the powder screw conveyor 8 outlet is connected to the powder bin 9 inlet, the powder bin 9 outlet is connected to the bagging machine 10, and the finished product screw conveyor 6 outlet is connected to the mouth The trough 7 is connected, the outlet of the crusher 5 is connected to the inlet of the screening equipment 4, a bucket elevator 3 is arranged between the crusher 5 and the screening equipment 4, and the inlet of the bucket elevator 3 is connected to the outlet of the grizzly hopper 1 , there is a feeding device 2 between the bucket elevator 3 and the grid sieve hopper 1, the feeding device 2 is an electromagnetic vibrating feeder or a motor vibrating feeder, the crusher 5 is an impact crusher, a roller crusher Or a hammer crusher, the screening device 4 is an inertial vibrating screen or a probability screen, and the particle size of the metallurgical coke in the middle layer of the screening device is 0.5-6 mm.
本发明的工作过程如下:冶金焦加入格筛料斗1,其后给料设备2均匀给料至斗式提升机3,物料经提升至筛分设备4,筛上料顶层出口经物料溜管送至破碎机5,经破碎的物料进入斗式提升机3送入筛分设备4筛分,其中筛分的合格料经成品螺旋输送机6输送至成品料槽7,筛下底部出口粉料经粉料螺旋输送机8送至粉料仓9,粉料仓9后安装了装袋机10将产生的小于0.5mm的粉料装袋。加工过程中大于6mm的大颗粒物料始终循环破碎,产生的粉料回收。The working process of the present invention is as follows: metallurgical coke is added to the grid sieve hopper 1, then the feeding equipment 2 evenly feeds the material to the bucket elevator 3, the material is lifted to the screening equipment 4, and the top layer outlet of the screened material is sent through the material slide pipe To the crusher 5, the crushed material enters the bucket elevator 3 and is sent to the screening equipment 4 for screening, wherein the qualified material screened is transported to the finished product trough 7 by the finished product screw conveyor 6, and the powder exiting at the bottom of the screen passes through The powder material screw conveyor 8 is sent to the powder material bin 9, and a bagging machine 10 is installed behind the powder material bin 9 to bag the powder material less than 0.5mm produced. During the processing process, the large particle materials larger than 6mm are always crushed in a circular manner, and the resulting powder is recycled.
本发明的格筛料斗1是为筛选出颗粒度太大的冶金焦颗粒,以提高筛分设备4和破碎机5的筛分破碎效率,可根据购进冶金焦的颗粒度不同需用不同大小的筛格。给料设备2要求密封性好,可根据系统产能的不同选择不同规格型号的给料设备。筛分设备4为双层筛,可通过改变筛网孔径来改变成品粒度,以适应不同规格产品对填充料颗粒度的不同要求。The grid sieve hopper 1 of the present invention is to screen out the metallurgical coke particles with too large particle size, so as to improve the screening and crushing efficiency of the screening equipment 4 and the crusher 5, and different sizes can be used according to the particle size of the purchased metallurgical coke. grid. The feeding equipment 2 requires good sealing, and different specifications and models of feeding equipment can be selected according to the different production capacity of the system. The screening device 4 is a double-layer sieve, and the particle size of the finished product can be changed by changing the aperture of the screen to meet the different requirements for the particle size of the filler for products of different specifications.
Claims (13)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2007101588059A CN101456745B (en) | 2007-12-11 | 2007-12-11 | Calcining filler processing method and system |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2007101588059A CN101456745B (en) | 2007-12-11 | 2007-12-11 | Calcining filler processing method and system |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN101456745A CN101456745A (en) | 2009-06-17 |
| CN101456745B true CN101456745B (en) | 2011-12-21 |
Family
ID=40767905
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2007101588059A Expired - Fee Related CN101456745B (en) | 2007-12-11 | 2007-12-11 | Calcining filler processing method and system |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN101456745B (en) |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102390670A (en) * | 2011-07-06 | 2012-03-28 | 安阳市恒威石化设备有限责任公司 | Coke dry quenching electromagnetic vibration feeder |
| CN103276408B (en) * | 2013-05-16 | 2015-07-01 | 嘉峪关索通预焙阳极有限公司 | Preparation method of high-quality prebaked anode for 500KA electrolytic cell |
| CN104444186A (en) * | 2014-11-12 | 2015-03-25 | 宁夏嘉翔自控技术有限公司 | Waste carbon electrode paste utilizing system |
| CN106040415A (en) * | 2016-07-18 | 2016-10-26 | 山东省阳信万信生物制品开发有限公司 | Graded crushing device for large particles |
| CN110508383A (en) * | 2019-09-20 | 2019-11-29 | 鄂尔多斯市君正能源化工有限公司 | A crushing and screening device for silica raw material field |
| CN111620693B (en) * | 2020-06-08 | 2021-12-07 | 沈阳铝镁设计研究院有限公司 | Production method for roasting carbon blocks by vertical roasting furnace |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2134896Y (en) * | 1992-08-15 | 1993-06-02 | 马铁林 | High-efficient multi-layer vibrating screen |
| CN2155568Y (en) * | 1992-11-25 | 1994-02-09 | 鞍山钢铁公司 | Oscillating mechanical sieve for determination of coke strength |
| CN1284536A (en) * | 2000-09-01 | 2001-02-21 | 冶金工业部鞍山热能研究院 | Two-stage process for producing large-lump cold pressed coke briquette |
| CN2663024Y (en) * | 2003-11-13 | 2004-12-15 | 徐州市赫尔斯采制样设备有限公司 | Mechanical swinging sieve |
| CN1616610A (en) * | 2004-10-19 | 2005-05-18 | 沈阳戴维环保节能设备有限公司 | Waste water and coke powder mixed solid fuel and its preparing method |
| CN1765777A (en) * | 2005-09-12 | 2006-05-03 | 沈阳戴维环保节能设备有限公司 | Method for filtration adsorption for disposing industrial effluent and city effluent |
| CN201140098Y (en) * | 2007-12-18 | 2008-10-29 | 沈阳铝镁设计研究院 | Torrefaction filler process system |
-
2007
- 2007-12-11 CN CN2007101588059A patent/CN101456745B/en not_active Expired - Fee Related
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2134896Y (en) * | 1992-08-15 | 1993-06-02 | 马铁林 | High-efficient multi-layer vibrating screen |
| CN2155568Y (en) * | 1992-11-25 | 1994-02-09 | 鞍山钢铁公司 | Oscillating mechanical sieve for determination of coke strength |
| CN1284536A (en) * | 2000-09-01 | 2001-02-21 | 冶金工业部鞍山热能研究院 | Two-stage process for producing large-lump cold pressed coke briquette |
| CN2663024Y (en) * | 2003-11-13 | 2004-12-15 | 徐州市赫尔斯采制样设备有限公司 | Mechanical swinging sieve |
| CN1616610A (en) * | 2004-10-19 | 2005-05-18 | 沈阳戴维环保节能设备有限公司 | Waste water and coke powder mixed solid fuel and its preparing method |
| CN1765777A (en) * | 2005-09-12 | 2006-05-03 | 沈阳戴维环保节能设备有限公司 | Method for filtration adsorption for disposing industrial effluent and city effluent |
| CN201140098Y (en) * | 2007-12-18 | 2008-10-29 | 沈阳铝镁设计研究院 | Torrefaction filler process system |
Non-Patent Citations (1)
| Title |
|---|
| JP昭62-91412A 1987.04.25 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN101456745A (en) | 2009-06-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201140098Y (en) | Torrefaction filler process system | |
| CN203044321U (en) | Sorting and loading system of refractory brick raw materials | |
| CN204220251U (en) | Calcined coke deep processing device | |
| CN111617881A (en) | A kind of aluminum residual electrode cleaning and crushing production line | |
| CN103586254A (en) | PCB (Printed circuit board) smashing recovery device and processing method thereof | |
| CN208146063U (en) | Pollution-free breaking polycrystalline silicon screening system | |
| CN204236798U (en) | A kind of granular material compaction apparatus | |
| CN215694685U (en) | Limestone crushing and screening production system | |
| CN101456745A (en) | Calcining filler processing method and system | |
| CN203343159U (en) | PCB (printed circuit board) crushing recovery device | |
| CN204975338U (en) | Coal pulverizing system | |
| CN111298933A (en) | Multi-stage crushing method for blocky solids | |
| CN218359785U (en) | Environment-friendly limestone raw material treatment system | |
| CN107952785A (en) | A processing device and method for fused magnesium return material | |
| CN215088716U (en) | Zinc dross recovery plant | |
| CN204138680U (en) | A kind of orthoscopic blast furnace ore coke groove feeding system | |
| CN202498022U (en) | System for screening and recycling blast furnace return ore | |
| CN206716421U (en) | Coal material screening breaker | |
| CN108371974A (en) | Pollution-free breaking polycrystalline silicon screening system | |
| CN101050921A (en) | Classifying segregation distributing and material supply chute | |
| CN203663974U (en) | Feeding structure on mineral powder grinding machine | |
| CN207823108U (en) | A device for preventing secondary crushing of petroleum coke fines | |
| CN203044160U (en) | Refractory brick raw material vibrating screen | |
| CN208839775U (en) | A kind of filler crushing system for graphite electrode production | |
| CN205662106U (en) | Control lump coal product limit is storage, loading device of rate down |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20111221 |